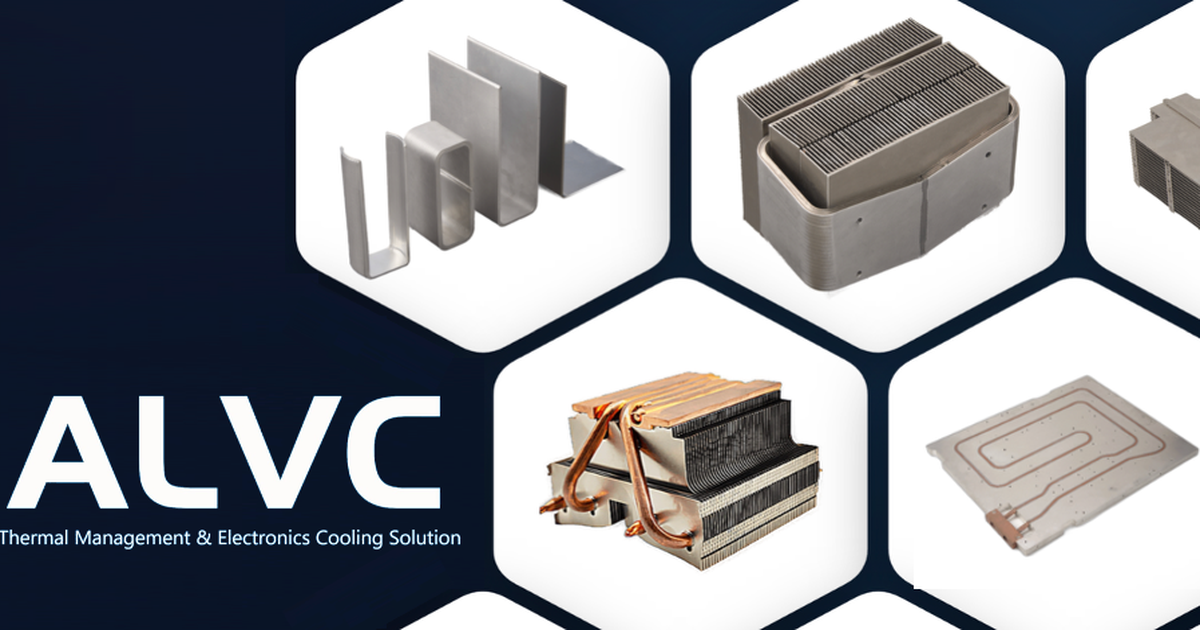
Passive 2-phase cooling systems, vapor chambers and heat sinks made of aluminium and copper – from prototype to high-volume series.
ALVC Europe GmbH
Stuttgart (Quellenstraße 7a, 70376)New on Amplifa
Thermal Management from Stuttgart
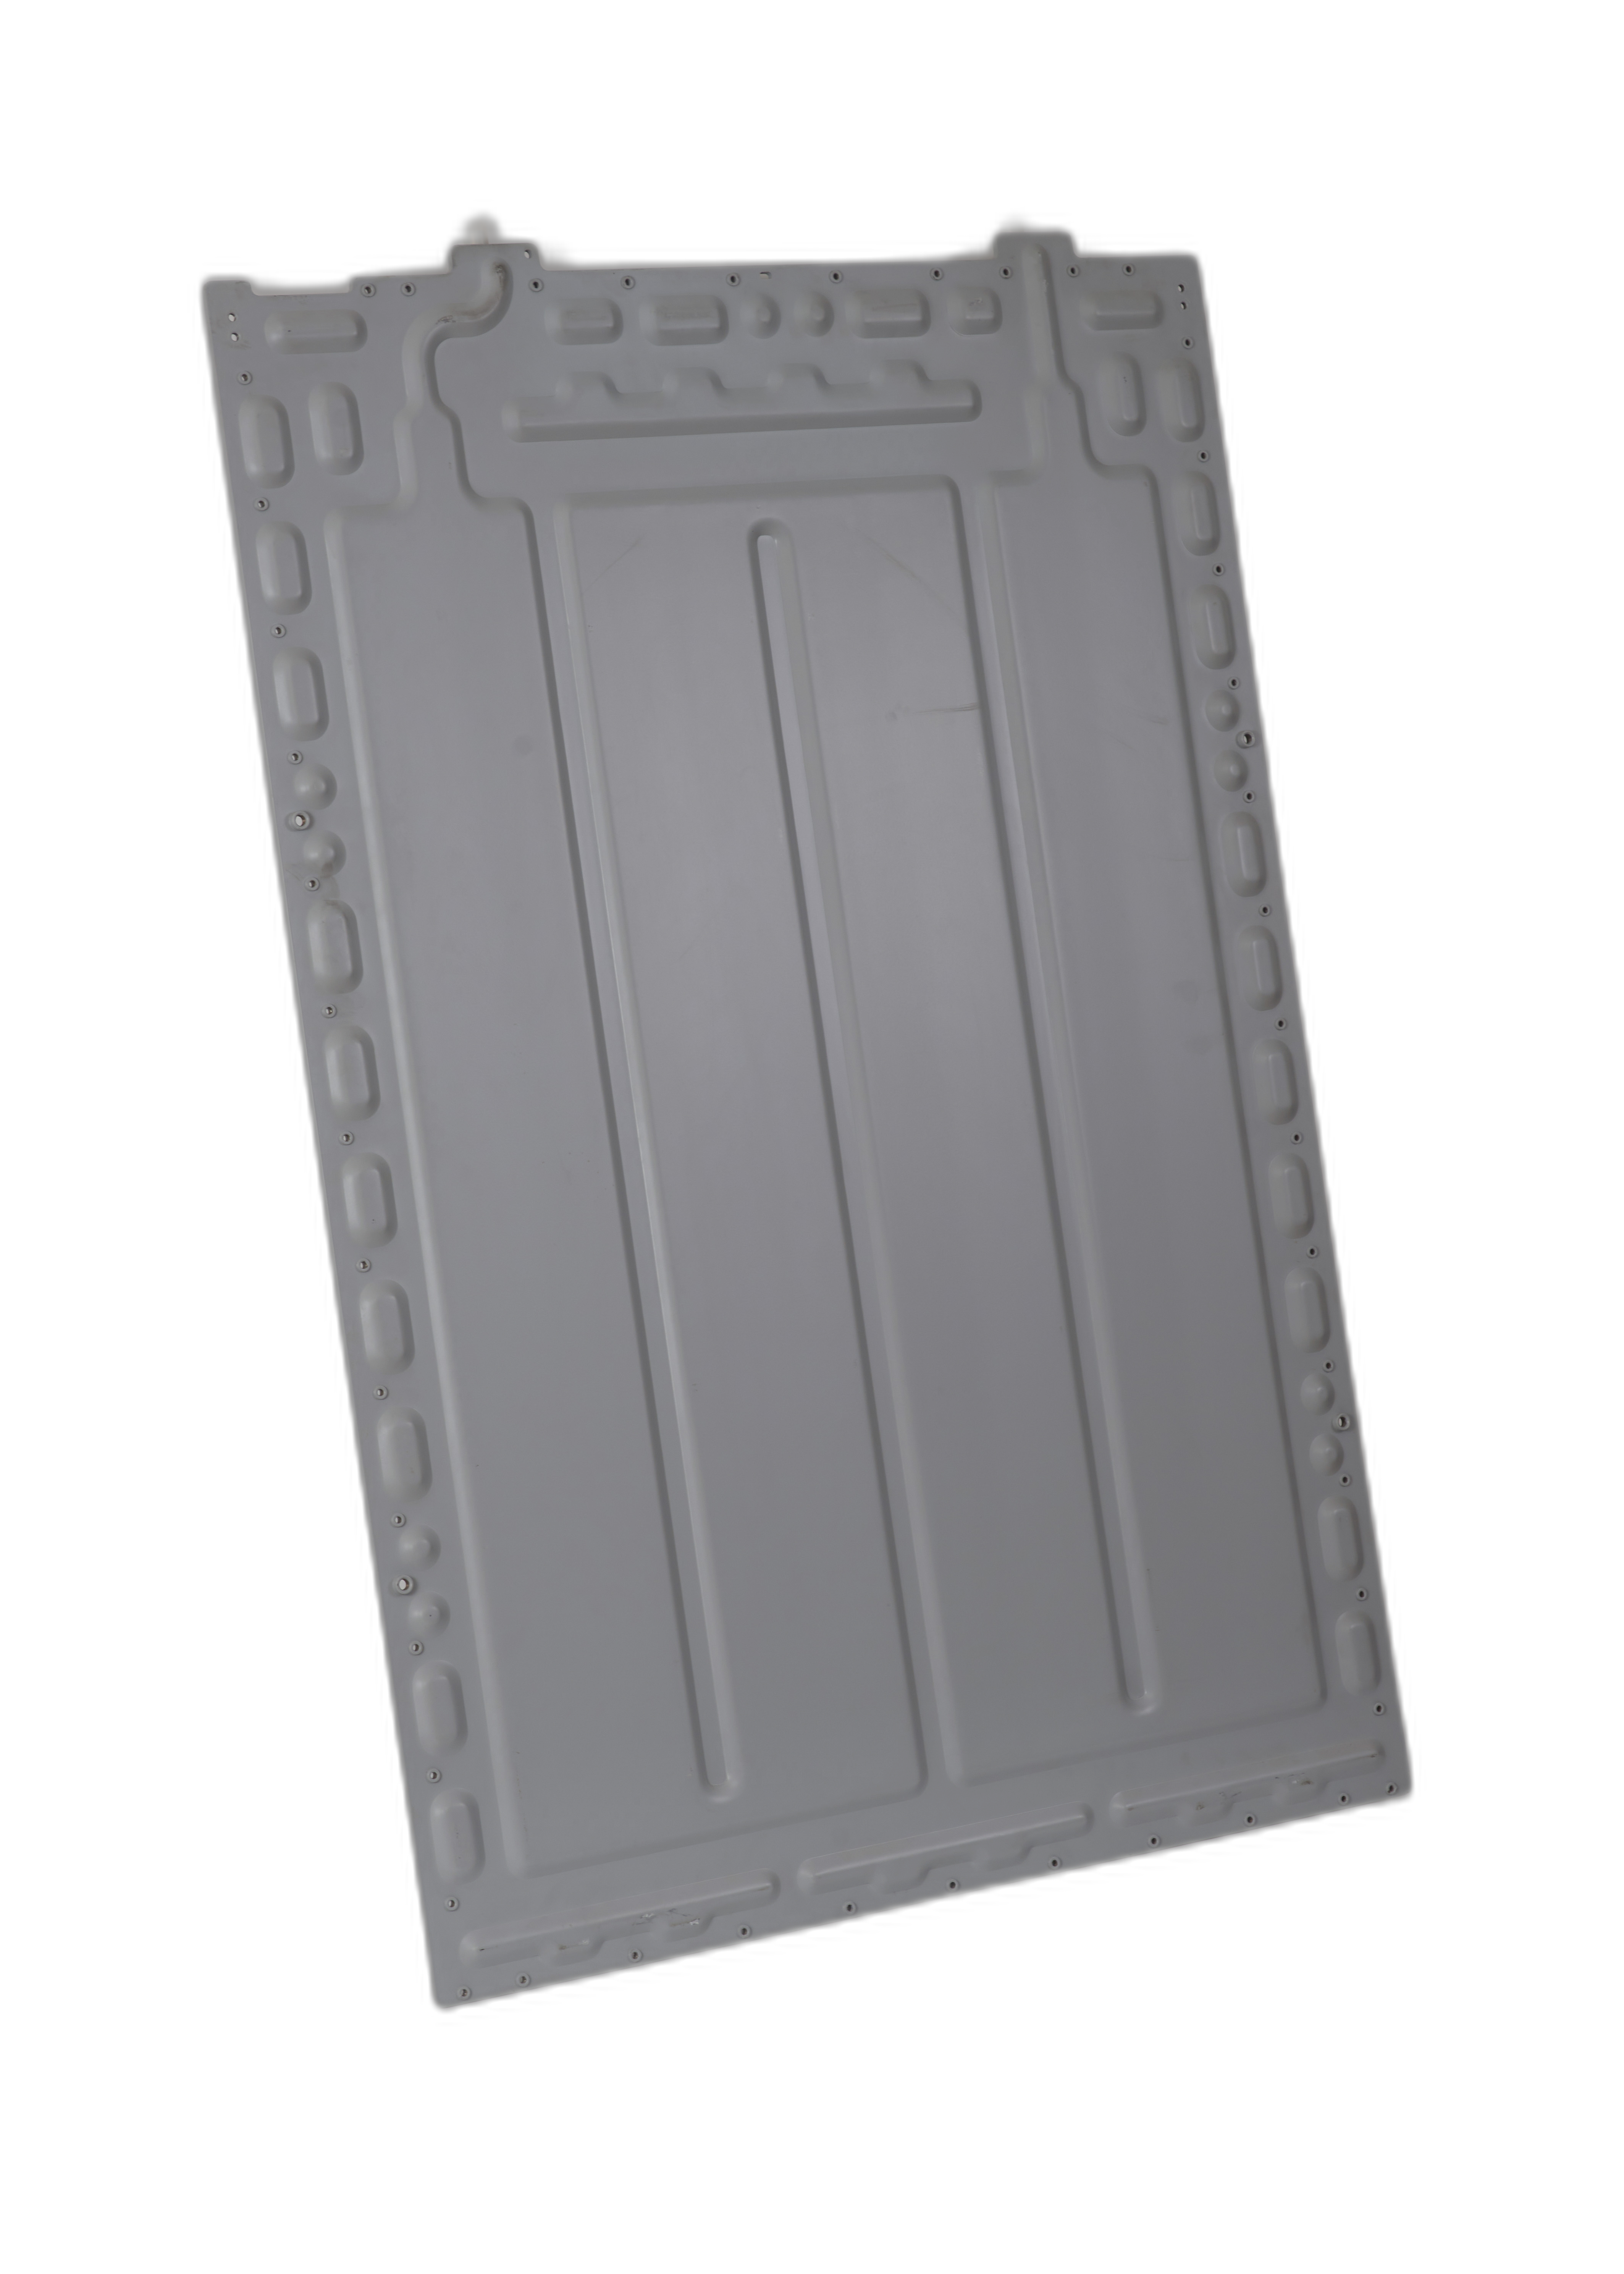
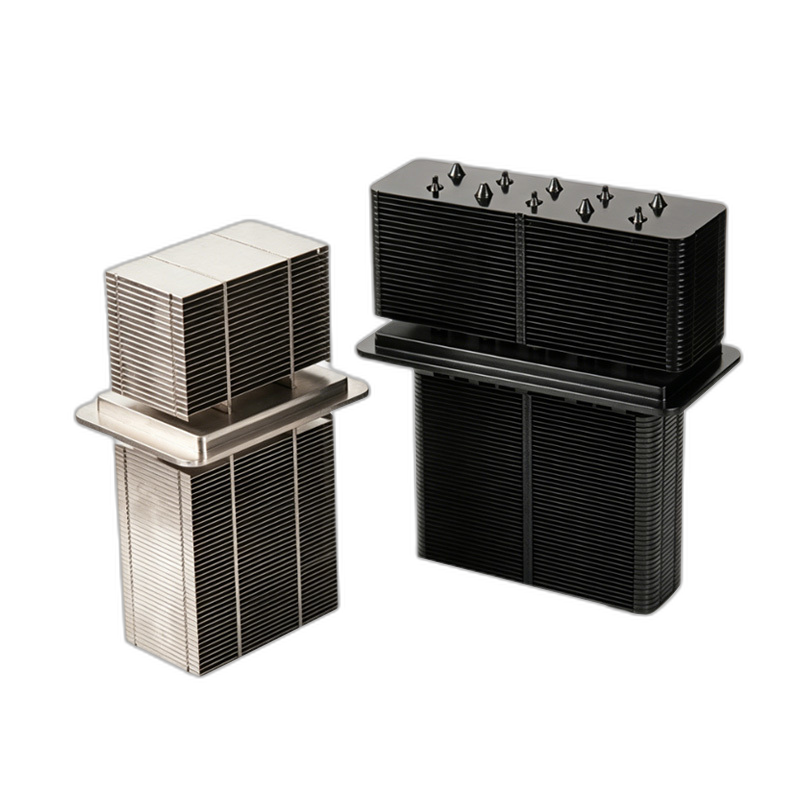
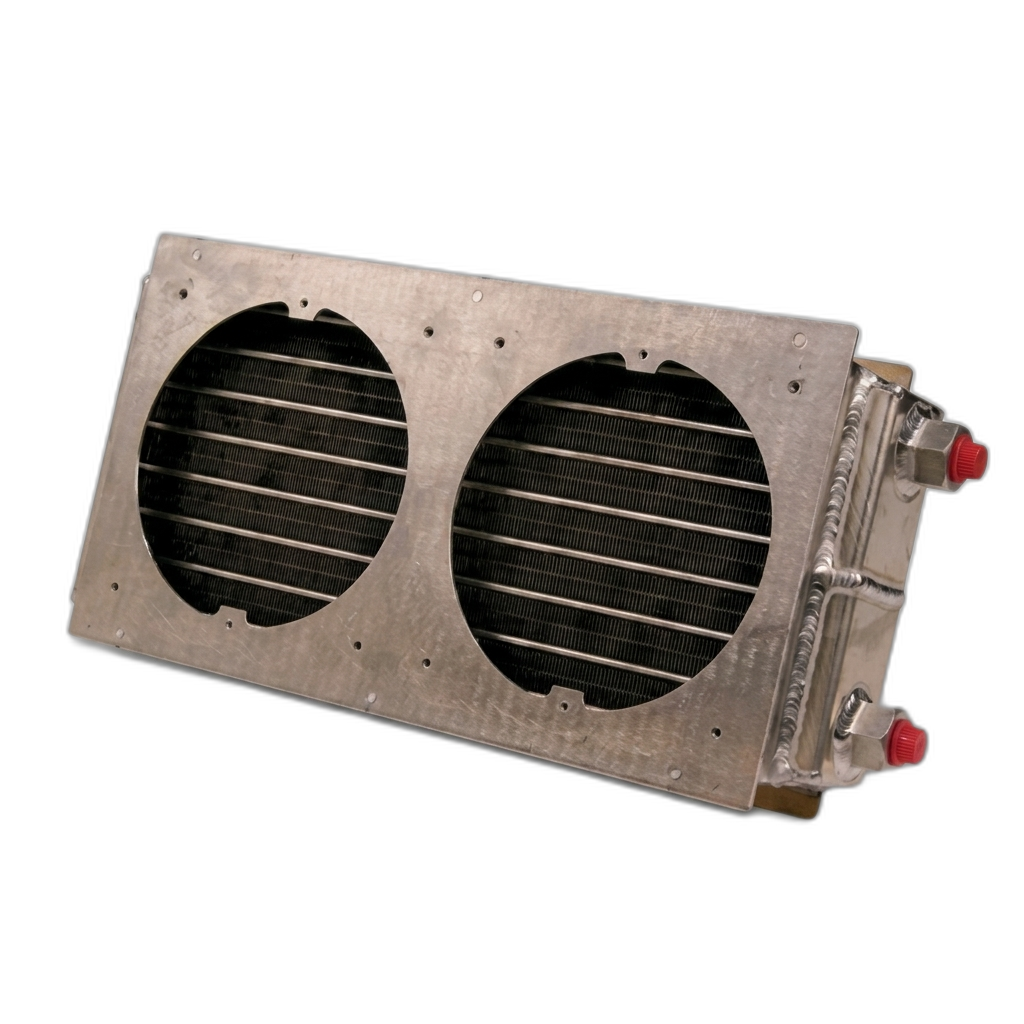
ALVC Europe GmbH, headquartered in Stuttgart, specialises in the development and series production of high-performance cooling solutions. The portfolio comprises passive closed 2-phase cooling systems such as vapor chambers, loop thermosiphon systems and pulsating heat pipes as well as liquid cold plates, heat sinks (extruded, milled, stacked, die-cast), heat pipe assemblies and air-to-air as well as air-to-water heat exchangers. Manufacturing is carried out in aluminium and copper, among other methods using extrusion, CNC profile machining, automated friction stir welding (FSW), vacuum brazing and vacuum-sealed filling of the hermetic systems with acetone. Services range from thermal simulation (CFD & FEA) and prototype construction within 10–14 working days to scaled series production of up to 200,000 units per year via a global ALVC production network. Customers come from power electronics, data centres and HPC, e-mobility, telecommunications, renewable energies, lighting and aerospace. Engineering, project management and quality inspection with a calorimeter test rig and helium leak tests are performed centrally in Stuttgart.
- Site
- Stuttgart
- Processes
- 2-phase cooling (passive vapor chamber/thermosiphon), Liquid Cold Plate (LCP) liquid cooling plate manufacturing, Heat sink manufacturing (extruded, milled, stacked, die-cast), Heat pipe heat sink (copper heat pipe assembly) with zipper/folded-fin fins, Loop thermosiphon cooling, Pulsating Heat Pipe (PHP), Air-to-air heat exchanger (2–5 kW), Air-to-water/liquid heat exchanger (5–12 kW; rear door up to 35 kW)
- Materials
- Aluminium, Copper, Acetone (refrigerant/working fluid), Acetone (working fluid), Extrusion, Friction Stir Welding (FSW), Vacuum Brazing, Die Casting
- Certificates
- ISO 9001, IATF 16949, ISO 14001
- Industries
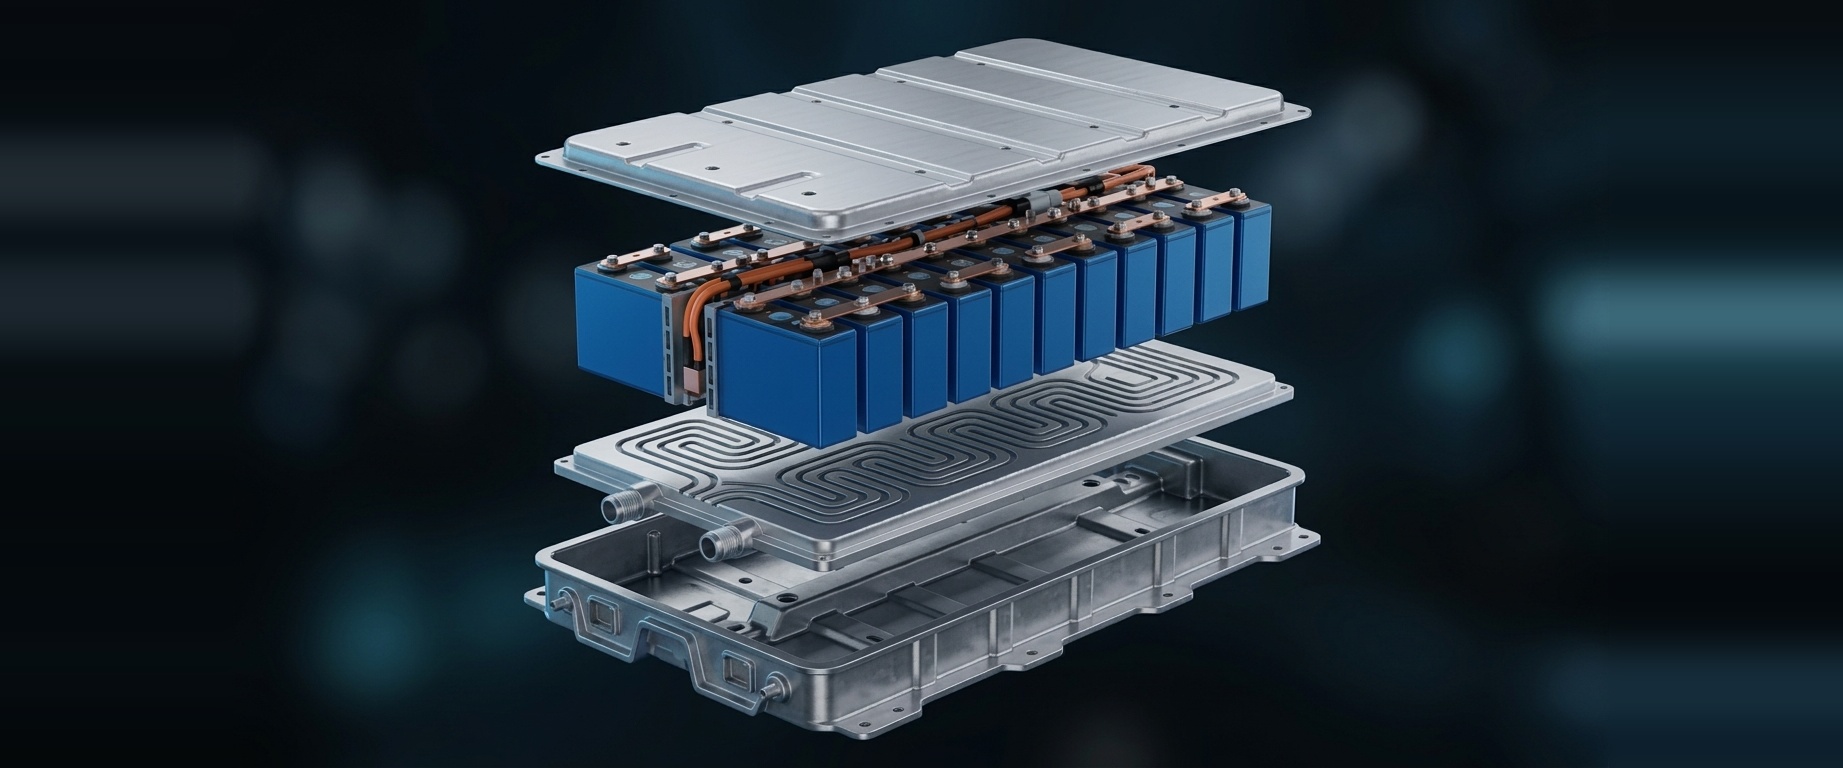
- IGBT & Power Electronics, Control Cabinets & IT Infrastructure, High-Performance Computing & AI Hardware, Battery Cooling & E-Mobility, Data Centre & Data Center Infrastructure, 5G Base Stations & Telecommunications
- 01
Requirements analysis & development/design (3D-CAD)
- 02
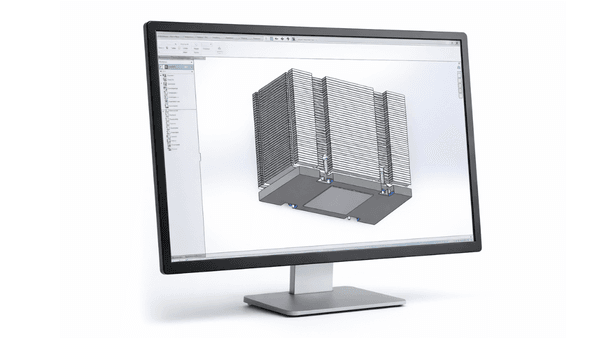
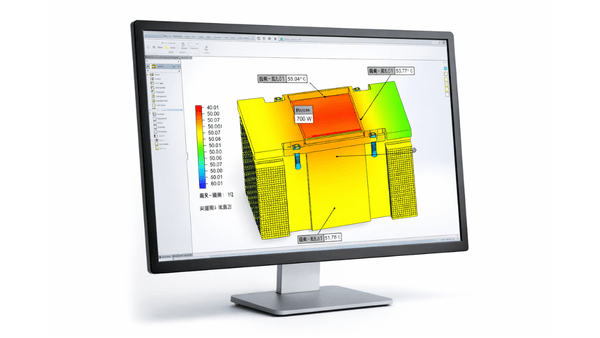
Thermal simulation (CFD & FEA)
- 03
Prototype construction (10–14 working days)
- 04
Testing & validation (calorimeter test rig, helium leak test)
- 05
Industrialisation & tooling (extrusion dies, FSW clamping fixtures)
- 06
Extrusion & CNC profile production (aluminium)
- 07
Automated FSW sealing
- 08
Robotic vacuum filling with acetone & 100 % inline helium testing
- 09
Quality control according to ISO 9001/14001
- 10
Series delivery, customs clearance & just-in-time logistics
Materials & Manufacturing Processes
Aluminium
Base material for vapor chambers, heat sinks, cold plates and heat exchangers in ultra-lightweight design.
Copper
Material for heat pipes, fins and precision-milled base plates with high thermal conductivity.
Acetone (working fluid)
Refrigerant for vacuum-sealed filling of hermetic 2-phase systems.
Extrusion
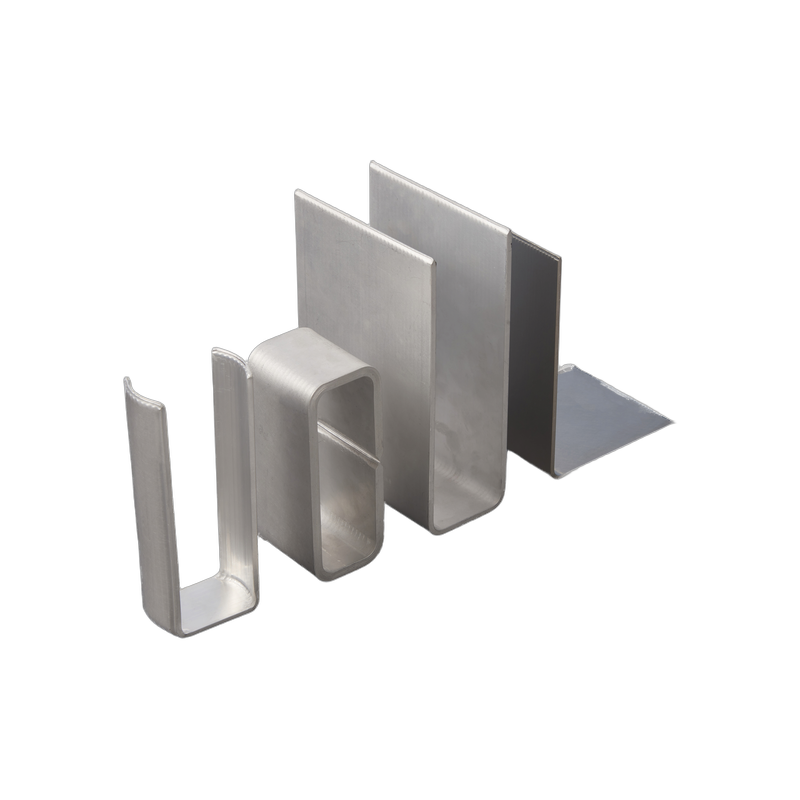
Series production of aluminium profiles with proprietary extrusion dies for heat sinks and cold plates.
Friction Stir Welding (FSW)
Automated, leak-tight FSW sealing of the profile ends in the series line.
Vacuum Brazing
Joining process with DFM expertise for tight component joints.
Die Casting
Process for die-cast aluminium heat sinks produced to drawing.
CNC Profile Machining (Milling)
Precision machining of aluminium profiles up to high-volume series.
Thermal Simulation (CFD & FEA)
Validation of transient heat flows and pressure losses before prototype construction.
Locations
Stuttgart
DEHeadquarters, engineering, laboratory/test field, quality management
- Lot size
- Prototypes from 1 piece; series up to 200,000 units/year
- Materials
- Aluminium, copper
- Calorimeter test rig
- Helium leak test rig
Components & Products
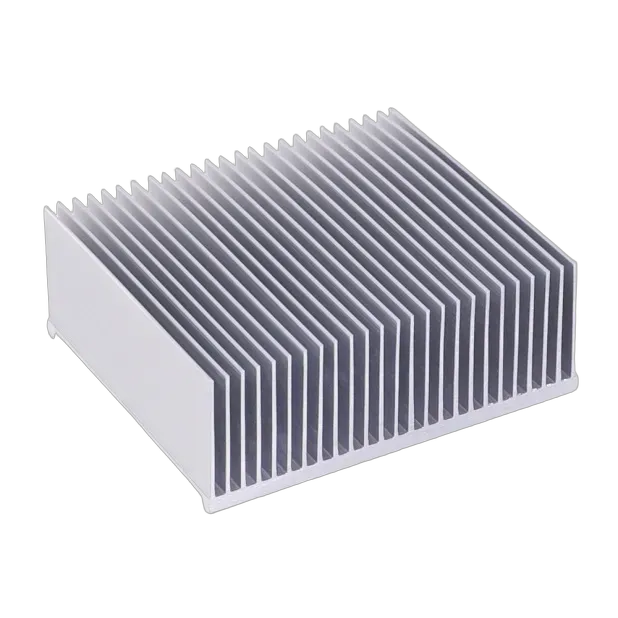
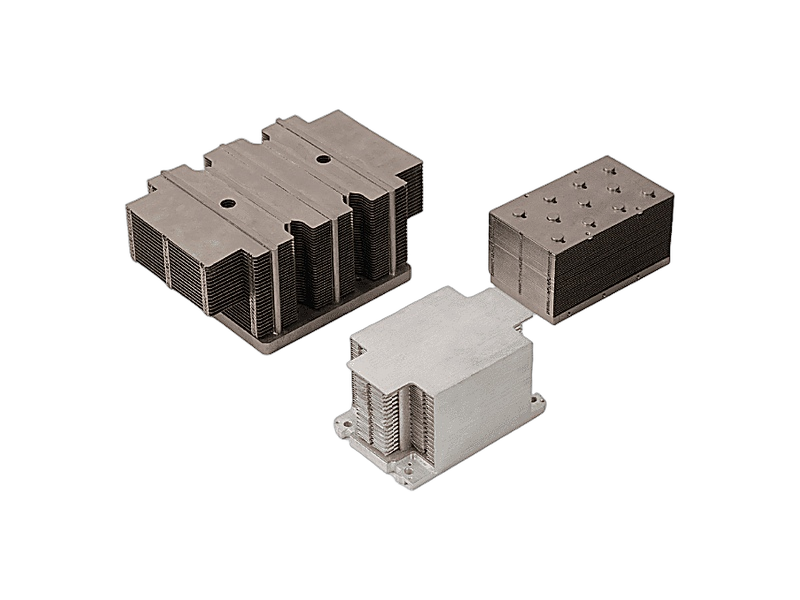
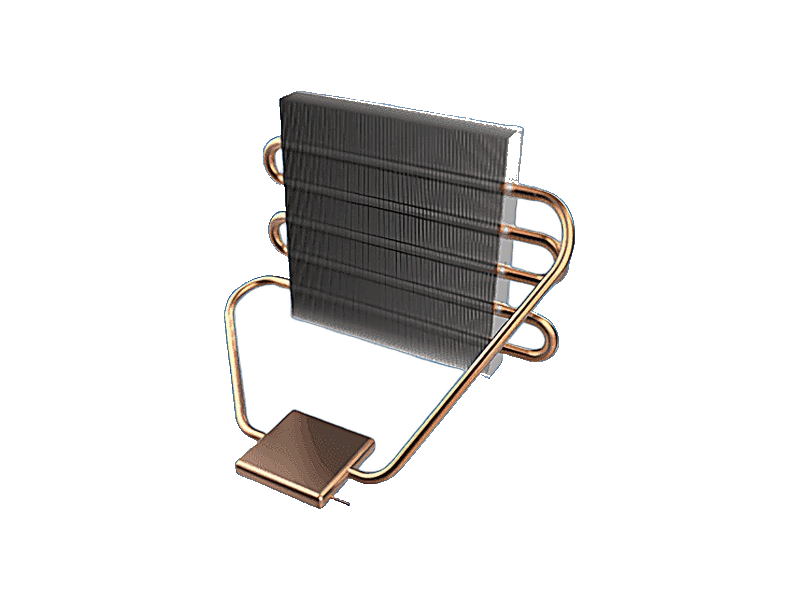
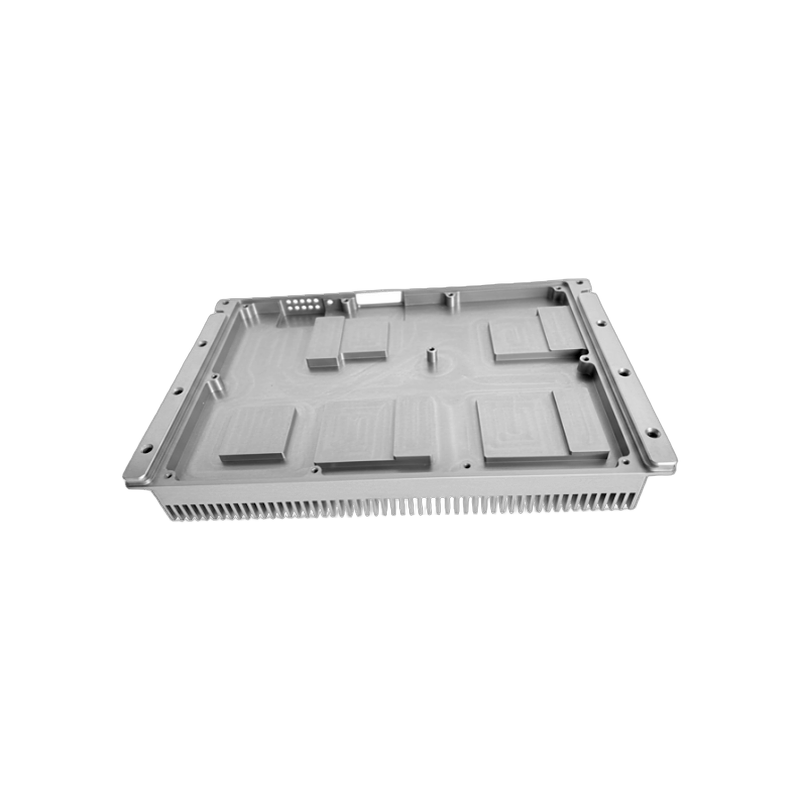
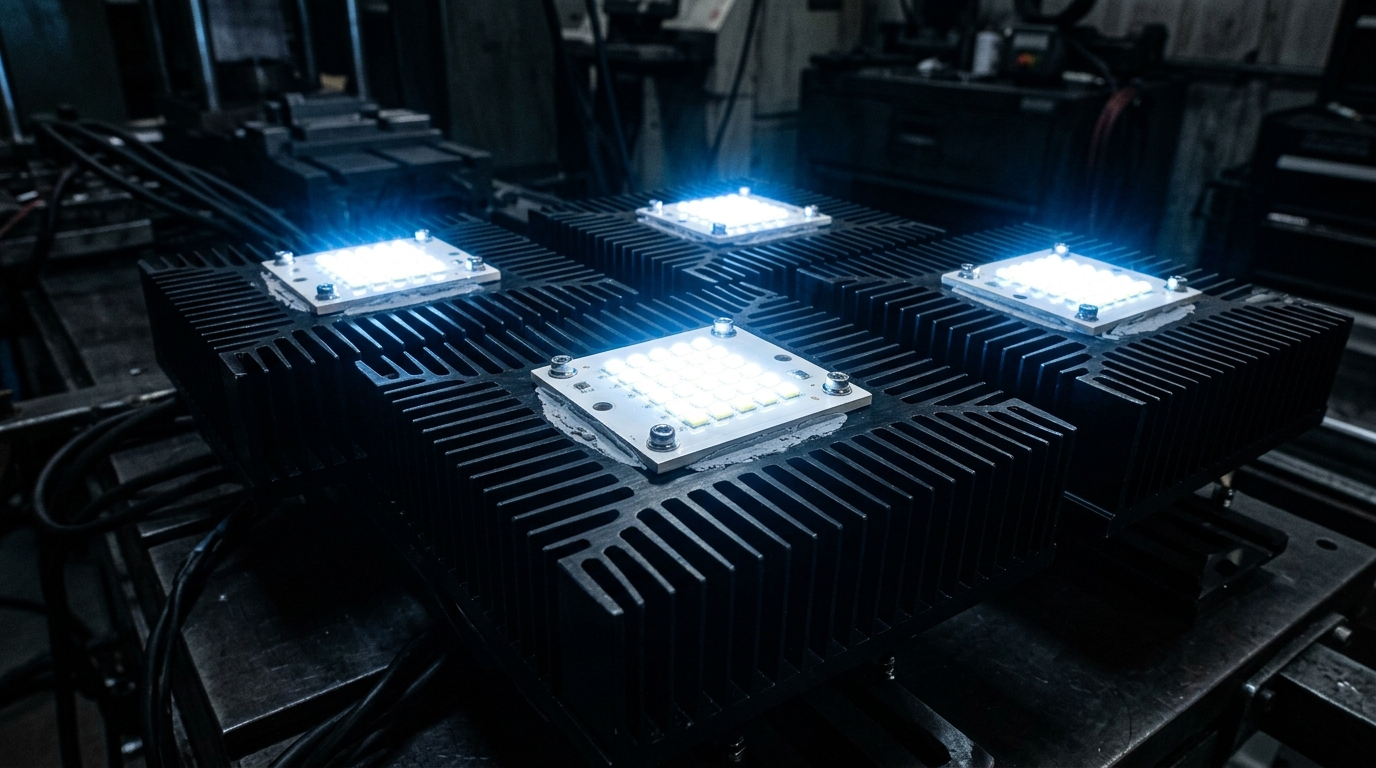
Inside the production
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| 2-phase cooling (passive vapor chamber/thermosiphon)Engineering | – | – | – | 1 piece | Aluminium, Copper |
| Liquid Cold Plate (LCP) liquid cooling plate manufacturingEngineering | – | – | – | 1 piece – 200,000 units per year | Aluminium, Copper |
| Heat sink manufacturing (extruded, milled, stacked, die-cast)Engineering | – | – | – | – | Aluminium, Copper |
| Heat pipe heat sink (copper heat pipe assembly) with zipper/folded-fin finsJoining | – | – | – | – | Copper, Aluminium |
| Loop thermosiphon coolingEngineering | – | – | – | – | Aluminium, Copper |
| Pulsating Heat Pipe (PHP)Engineering | – | – | – | – | Aluminium, Copper |
| Air-to-air heat exchanger (2–5 kW)Engineering | – | – | – | – | Aluminium |
| Air-to-water/liquid heat exchanger (5–12 kW; rear door up to 35 kW)Engineering | – | – | – | – | Aluminium, Copper |
| 3DVC vapor chamber heat sink (up to 2000 W heat dissipation per module)Engineering | – | – | – | – | Aluminium, Copper |
| Vacuum sealing / vacuum filling with acetone (hermetic systems)Joining | – | – | – | – | Aluminium, Copper |
| Development & design (thermal development, 3D-CAD)Engineering | – | – | – | – | – |
| Simulation (CFD & FEA)Engineering | – | – | – | – | – |
| Prototype construction (functional samples within 10–14 working days)Engineering | – | – | – | 1 piece | – |
| Testing & validation (calorimeter test rig, helium leak tests, reliability testing)Testing | – | – | – | – | – |
| FSW series line production (friction stir welding, automated, 100 % inline helium testing)Joining | – | – | – | 200,000 units per year | Aluminium |
| CNC profile production (machining of aluminium profiles)Machining | – | – | – | 200,000 units per year | Aluminium |
| Extrusion (series extrusion dies, aluminium profiles)Forming | – | – | – | – | Aluminium |
| Vacuum Brazing (vacuum brazing, DFM expertise)Joining | – | – | – | – | Aluminium, Copper |
| Die casting of heat sinksCasting | – | – | – | – | Aluminium |
| Design for Manufacturing (DFM) & Design-to-Cost (DTC)Engineering | – | – | – | – | – |
3 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| Automated FSW series line production (friction stir welding system) | – | – | – | – | global ALVC production network (Asia) |
| CNC machining (profile machining, milling) | – | – | – | – | – |
| Calorimeter test rig / helium leak test rig | – | – | – | – | Stuttgart |
Additional services
Reference customers
Quality Assurance
Engineering, project management and final quality inspection are performed centrally from Stuttgart with a calorimeter test rig, helium leak tests and reliability testing with test reports. In the series line, all systems are vacuum-sealed, filled with acetone by robots and subjected to 100 % inline helium leak testing.
| Evidence | Stuttgart |
|---|---|
| ISO 9001 | |
| ISO 14001 | |
| IATF 16949 |
History
Over 25 years of thermal engineering experience in closed 2-phase cooling systems (thermosiphon, vapor chamber, heat pipes)