Development, mould making and precision injection moulding of technical plastic parts and assemblies in Dachau
AMPER-PLASTIK R. Dittrich GmbH & Co. KG
DachauNew on Amplifa
About Amper-Plastik
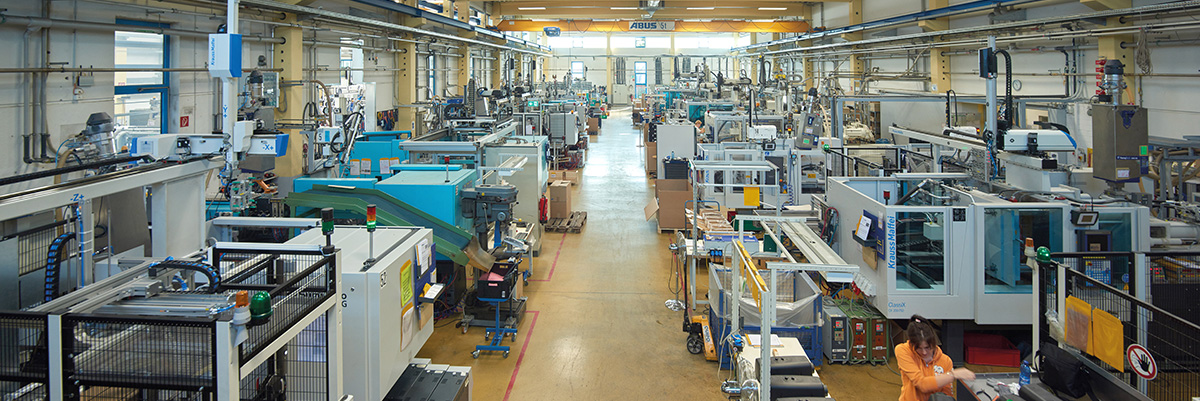
Amper-Plastik R. Dittrich GmbH & Co. KG is a family-owned company founded in 1960, owner-managed and based in Dachau, which manufactures technically demanding plastic products and injection moulds. Its value chain covers the development of plastic parts up to series maturity, mould making with CAD/CAM (VisiCAD) including prototypes and sample tools, as well as injection moulding production on around 37 machines with clamping forces from 150 to 5,000 kN. Precision injection moulding is produced with tolerances down to ±0.03 mm, including multi-component injection moulding, thin-wall injection moulding with wall thicknesses from 0.4 mm, insert moulding, high-gloss surfaces and light guides. More than 1,000 material types are processed – common thermoplastics and elastomers, high-performance materials such as PEEK, LCP, PPSU and PPS as well as WPC and bioplastics. The portfolio is complemented by assembly of sub-assemblies, ultrasonic welding, hot staking, finishing and 100% quality control. Customers come from mechanical engineering and the electrical industry, automation and sensor technology, electromobility and medical technology, including B. Braun, Siemens, GETT, Heitec and Captron.
- Site
- Dachau
- Processes
- Plastic injection moulding (technical precision injection moulding of thermoplastics), Multi-component injection moulding / two-component injection moulding (hard-hard, hard-soft,, Thin-wall injection moulding, Insert moulding (insert technology / overmoulding of metal or plastic inserts), Assembly injection moulding (automated overmoulding of inserts by robot), High-gloss surface injection moulding, Injection moulding of light guides / transparent parts with optical requirements, Design and manufacture of injection moulds (mould making including prototypes and sample tools,
- Materials
- Thermoplastics (all common types), Elastomers, PEEK, LCP (Liquid Crystal Polymer), PPSU, PPS, Wood-Plastic-Composite (WPC), Bioplastics (bio-based)
- Certificates
- ISO 9001:2015, UL Factory Inspections & UL Recognized Materials, Energy audit EN 16247-1 (SpaEfV), TecPart Code of Conduct, UL Factory Inspections, Energy audit EN 16247-1
- Founded
- 1960
- Employees
- over 100
- Industries
- Mechanical engineering and electrical industry, Automation and sensor technology, Electromobility, Medical technology, Communications technology, IT/computers (historical: keyboards, T-DSL modems)
- 01
Development of plastic parts up to series maturity
- 02
Design and mould making (CAD/CAM, prototypes, sample tools)
- 03
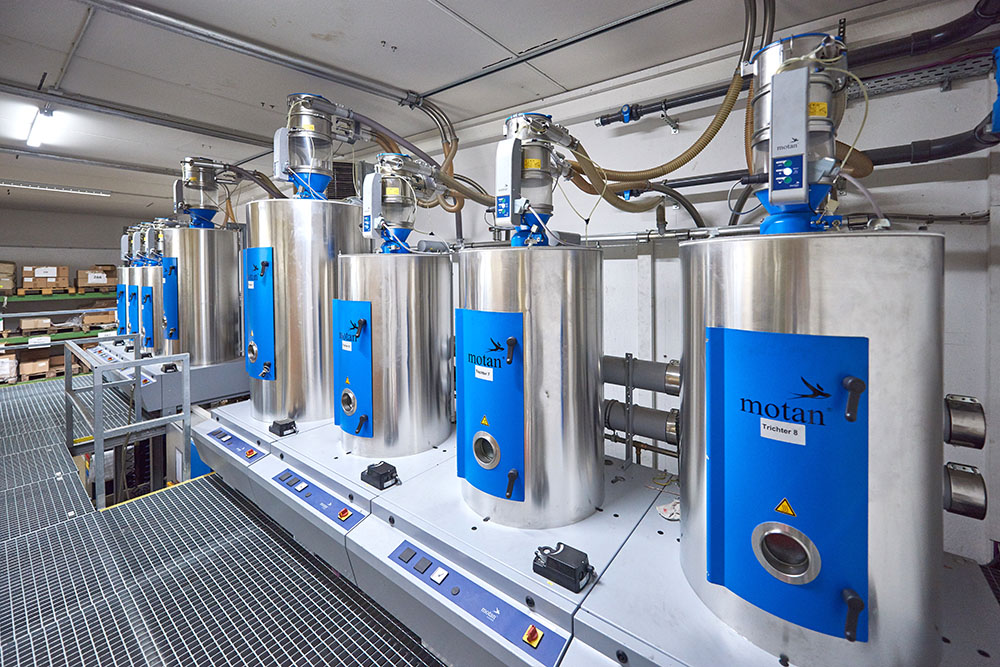
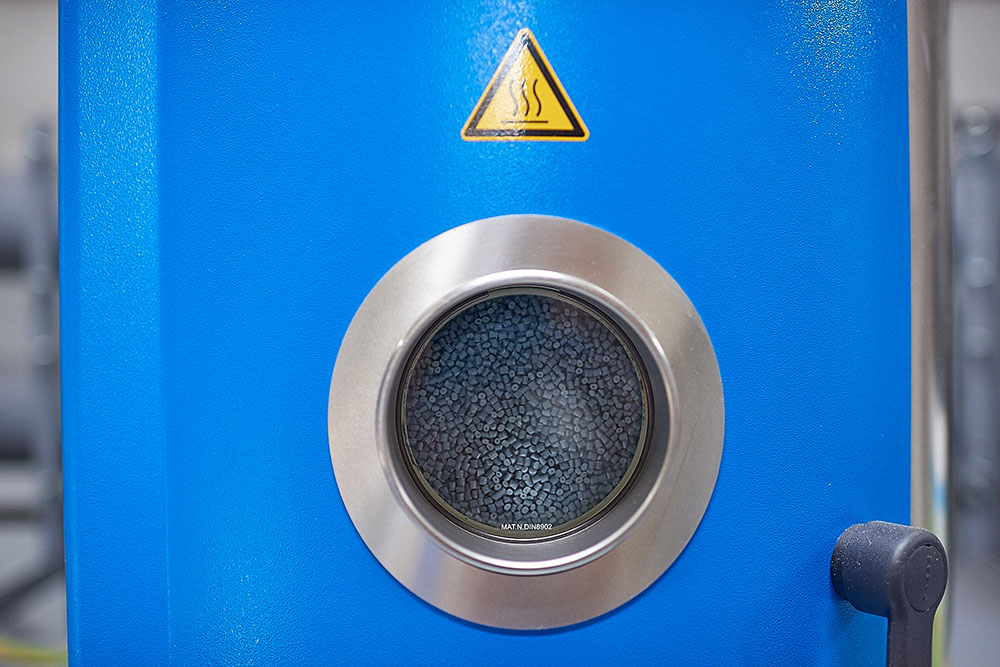
Raw material drying and material preparation
- 04
Precision injection moulding (1K/2K, insert moulding, thin-wall)
- 05
Joining and post-treatment (ultrasonic welding, hot staking, annealing)
- 06
Finishing (laser marking, printing, painting)
- 07
Assembly of sub-assemblies, including automated
- 08
Quality inspection and logistics (high-bay warehouse)
Materials and Production Technologies
Thermoplastics (all common types)
Basis of the technical injection-moulded parts for mechanical engineering, electrical, medical and mobility applications.
Elastomers
Used in multi-component injection moulding for soft functional areas and seals.
PEEK
High-performance material for technically demanding parts subject to high thermal and chemical loads.
LCP (Liquid Crystal Polymer)
High-performance plastic for filigree, precise connector and electronic components.
PPSU
High-temperature-resistant engineering plastic, among other things for medical applications.
PPS
High-performance material for electrically insulating, thermally stressed components.
Wood-Plastic-Composite (WPC)
Processing of renewable raw materials for sustainable plastic products.
Bioplastics (bio-based)
Over 20% of the raw material requirement is met with bio-based granulates.
Metal insert parts (insert moulding)
Automatically fed metal or plastic inserts are encapsulated in a form-fitting manner.
Multi-component injection moulding
Combinations of hard-hard, hard-soft and soft-soft up to 1 kg part weight.
Thin-wall injection moulding
Wall thicknesses from 0.4 mm for compact, filigree components.
Site
Dachau
DEMain site: development, mould making, injection moulding production, assembly
- Part weight / size
- 0.2 g to 1.5 kg part weight
- Lot size
- Small series to industrial mass production in the eight-figure annual range
- Materials
- Thermoplastics, elastomers, PEEK, LCP, PPSU, PPS, WPC, bioplastics
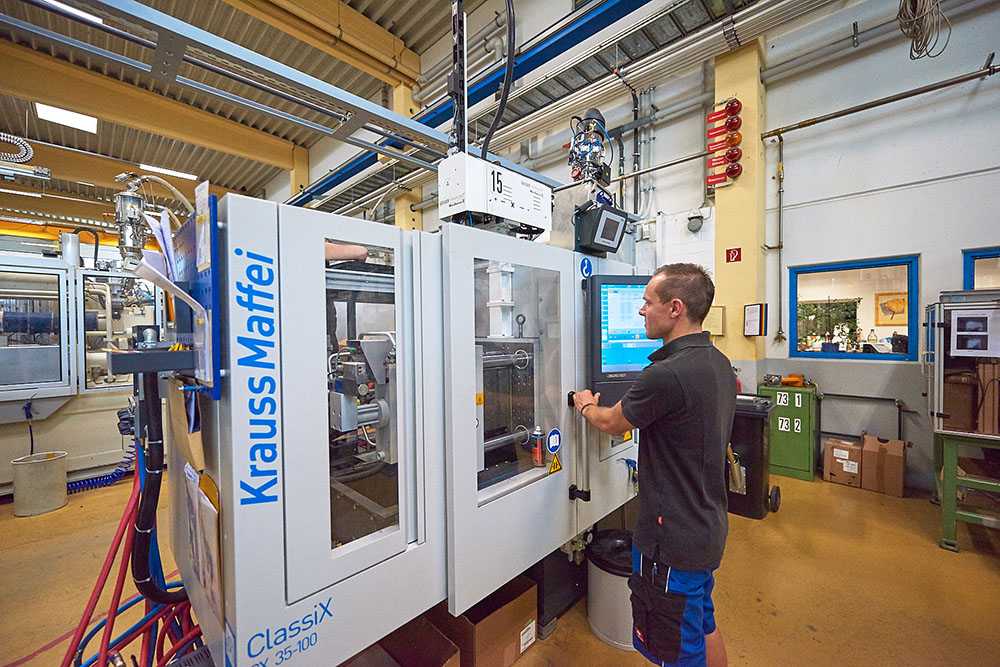
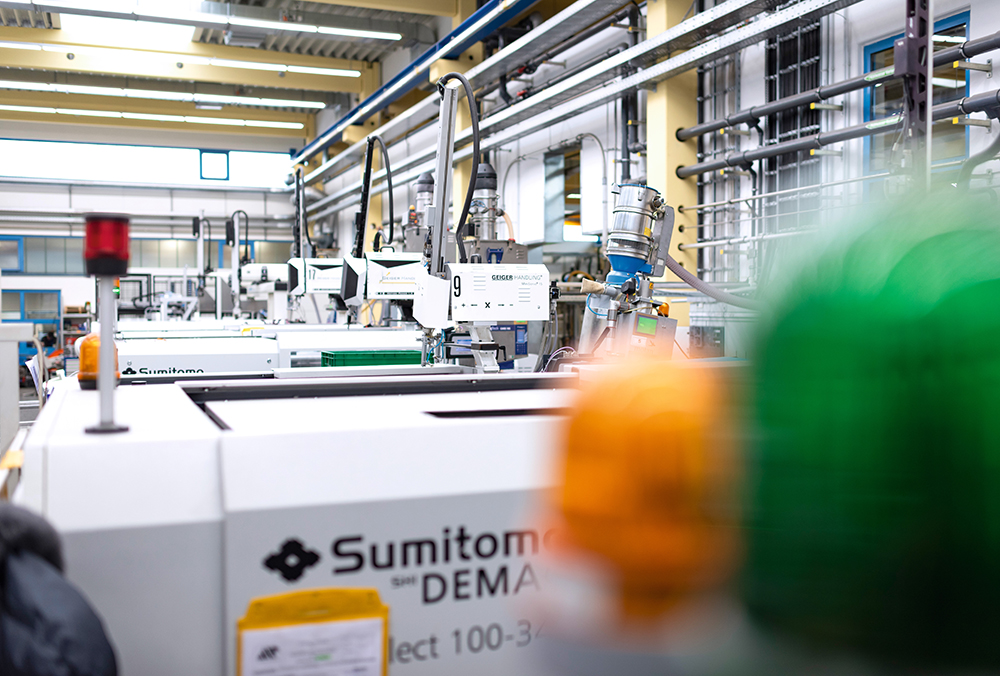
- 37 injection moulding machines (hydraulic and all-electric, 150–5,000 kN)
- Lathe WEILER
- Wire EDM machine Sodick
- Die-sinking EDM machine Sodick
- Milling machining centre Hermle
- CNC-controlled measuring machine
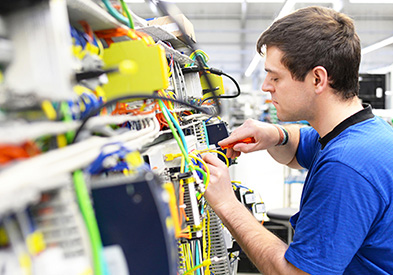
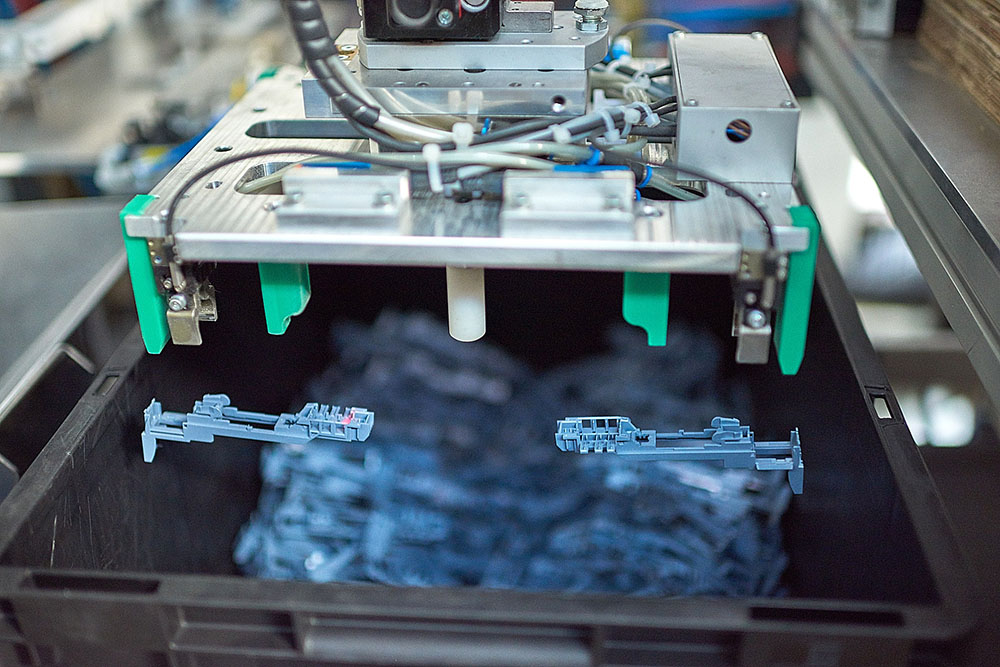
- Handling and assembly robots
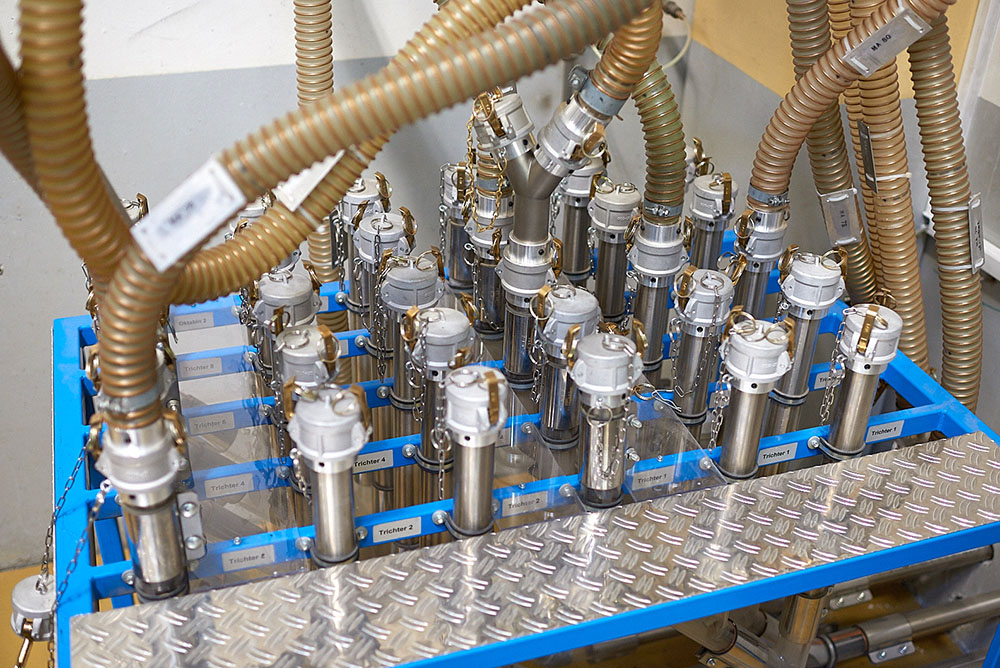
- Central material pre-drying station
- High-bay warehouse
Parts
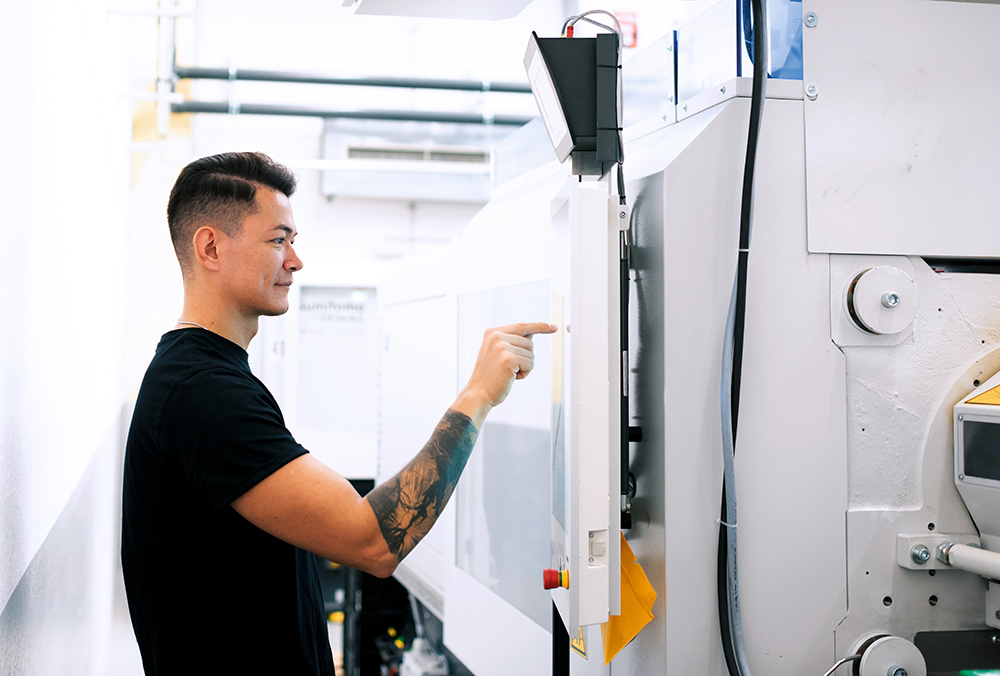
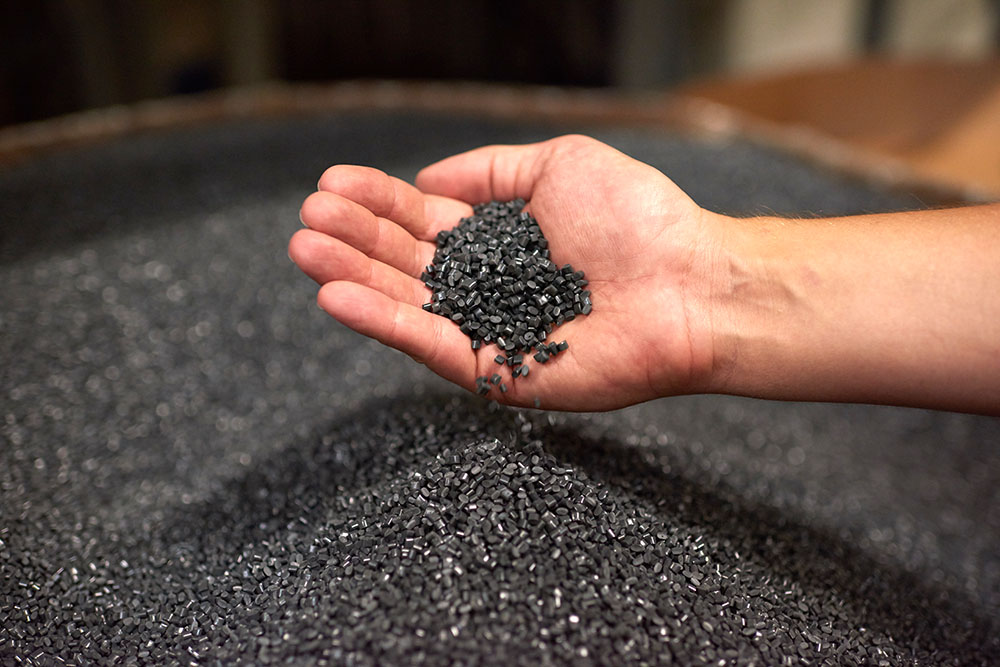
Inside the production
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Plastic injection moulding (technical precision injection moulding of thermoplastics)Plastics | ± 0.03 mm | – | 0.2 g – 1.5 kg | industrial mass production in the | Thermoplastics, Elastomers, High-performance materials (PEEK, LCP, PPSU, PPS), WPC, Bioplastics |
| Multi-component injection moulding / two-component injection moulding (hard-hard, hard-soft,Plastics | – | – | 1 kg (part weight) | – | Thermoplastics, Elastomers |
| Thin-wall injection mouldingPlastics | – | – | – | – | Thermoplastics |
| Insert moulding (insert technology / overmoulding of metal or plastic inserts)Plastics | – | – | – | – | Thermoplastics, Elastomers |
| Assembly injection moulding (automated overmoulding of inserts by robot)Plastics | – | – | – | – | Thermoplastics |
| High-gloss surface injection mouldingPlastics | High-gloss surfaces | – | – | – | Thermoplastics |
| Injection moulding of light guides / transparent parts with optical requirementsPlastics | – | – | – | – | Thermoplastics |
| Design and manufacture of injection moulds (mould making including prototypes and sample tools,Engineering | – | – | – | – | Steel (toolmaking, not further specified) |
| Jig and fixture building and automation (design and manufacture of fixtures for assembly,Engineering | – | – | – | – | – |
| Development of plastic parts up to series maturity (part development, manufacturing concepts)Engineering | – | – | – | – | – |
| Assembly of sub-assemblies (also automated, 100% quality control)Assembly | – | – | – | – | Plastic, Metal (inserts) |
| Ultrasonic welding (plastic joining technology)Joining | – | – | – | – | Thermoplastics |
| Hot staking (plastic joining technology)Joining | – | – | – | – | Thermoplastics |
| Laser marking (plastic marking)Surface | – | – | – | – | Plastic |
| Printing and painting techniques (decorative finishing of plastic parts)Surface | – | – | – | – | Plastic |
| Post-treatment of plastic parts: conditioning, annealing, coatingHeat treatment | – | – | – | – | Plastic |
| Quality inspection: CNC-controlled measuring machine, video and tactile measurement, roughnessTesting | – | – | – | – | – |
7 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| Injection moulding machines (hydraulic and all-electric) | – | 37 | Clamping forces 150–5,000 kN | – | Dachau |
| Lathe (mould making) | WEILER | – | – | – | Dachau |
| Wire EDM machine | Sodick | – | – | – | Dachau |
| Die-sinking EDM machine | Sodick | – | – | – | Dachau |
| Milling machining centre | Hermle | – | – | – | Dachau |
| CNC-controlled measuring machine | – | – | – | – | Dachau |
| Handling/assembly robots (part removal, packaging, assembly, inspection) | – | – | – | – | Dachau |
Additional services
Reference customers
Quality
Quality management has been certified to DIN EN ISO 9001 since 1997 and is supported by a CAQ system. Testing includes, among other things, CNC measuring machine, video and tactile measurement, roughness, tensile, compression and colour measurement as well as internal pressure sensors and camera inspection in three-shift operation, with 100% inspection for safety-relevant parts.
| Evidence | Dachau |
|---|---|
| ISO 9001:2015 | |
| UL Factory Inspections | |
| Energy audit EN 16247-1 | |
| TecPart Code of Conduct |
History
- 1960
Founded by Rudolf R. Dittrich on Ludwig-Thoma-Strasse in Dachau; first customers are the Braun camera works in Nuremberg and Kathrein in Rosenheim.
- 1965
Takeover of the Bay. Spritzgusswerke and relocation to the Floßlände in Dachau; first orders from the telephone division of Siemens Munich.
- 1972
Construction of the first building at Otto-Hahn-Str. 2 with 1,300 m² of factory floor space; mould making becomes an independent department.
- 1988
Production start of keycaps from a 48-cavity mould for Siemens Nixdorf.
- 1998
Amper-Plastik is the sole supplier of T-DSL modems for years; expansion with a central building, the site grows to 6,200 m².
- 2000
Opening up of medical and automotive engineering; start of development and production of Sinamics products for the Siemens device plant in Erlangen.
- 2012
Plant expansion to 9,600 m² of site area, doubling of the injection moulding area and construction of the high-bay warehouse.
- 2014
Doubling of the production area to 2,140 m².
- 2015
Siemens Over-All Award: for the second time after 2011, awarded best supplier of the Siemens Motion Control division.
- 2018
Entry into electromobility with the development of eCar products.
- 2021
End of the production of fully assembled PC keyboards after more than 25 years.
- 2023
Honorary award 16th Partnerstein 2023.
- 2024
First supplier day of Siemens Smart Infrastructure at the metering plant in Berlin; investment in modern laser technology.
- 2025
B. Braun Supplier Award Silver.