Manufactures and supplies gaskets, molded parts, profiles and polymer components to drawing – from prototype to large-scale series.
Berger S2B GmbH
Viernheim (Alfred-Nobel-Str. 17, visitor address) · Viernheim (Alfred-Nobel-Str. 19, goods receiving/shipping)New on Amplifa
About Berger S2B
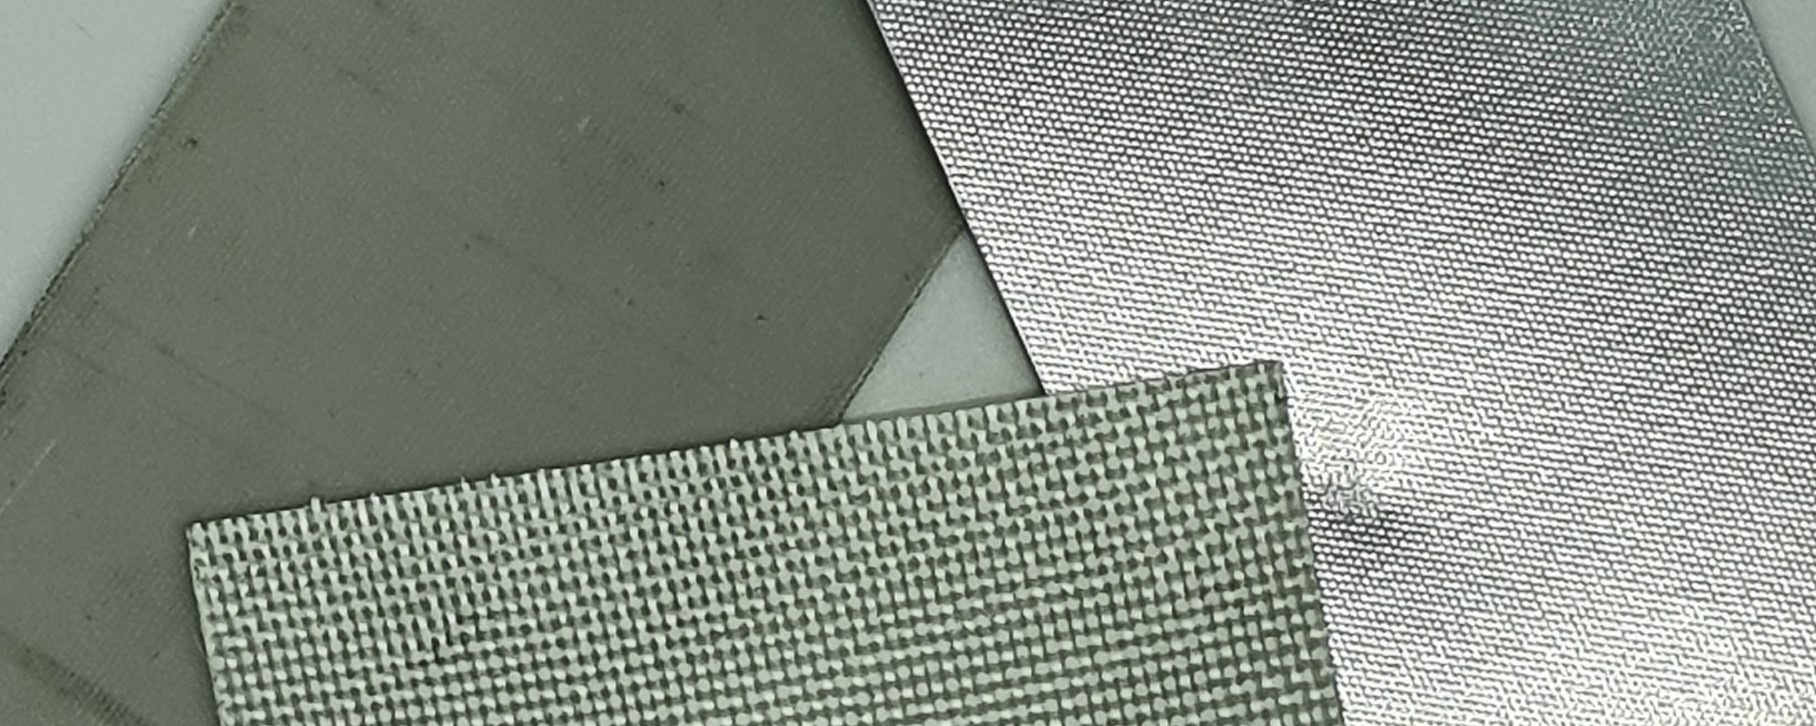
Berger S2B GmbH is a family-owned company in its third generation, headquartered in Viernheim. Founded in 1930 as a technical trading business in Mannheim, it has developed into a service and manufacturing company in polymer, elastomer and sealing technology. The company manufactures molded parts, flat gaskets, high-pressure gaskets, profiles, elbows, rubber-metal parts (bonded seals), stamped parts, waterjet cuts, dip-molded parts, FIPG liquid gaskets and 3D-printed parts to customer drawings. In its own production facility in Viernheim, a 3D waterjet cutting machine, a pure-water waterjet system with seven heads, plotters with oscillating cutting knife, a high-speed kiss-cut stamping press as well as bridge and double-column clicker presses are in use; machining tolerances of up to ±0.1 mm and 0.05 mm in stamping are achievable. In terms of materials, more than 85 special elastomer compounds (including EPDM, NBR, H-NBR, FKM, VMQ, FEPM) and multilayer composites with fabrics, graphite, cork, glass, ceramics and silicates are processed. Customers come from agricultural and construction machinery, transport and commercial vehicles, machinery and plant engineering, mobility/storage technology and electrical engineering; via the single-sourcing concept DichTec®, series suppliers worldwide (including Brazil, USA, China) are also supplied, including warehousing, EDI connection and component modularization.
- Site
- Viernheim
- Processes
- Waterjet cutting (also 3D head, abrasive, pure water), Plotter cutting with oscillating cutting knife, High-speed kiss-cut stamping press (endless material feed), Die cutting (bridge and double-column clicker presses, solid die/steel rule cutting), Molded part production by compression molding (CM), injection compression molding (ICM), transfer, Profile production (UHF, salt bath, shear head, hot air, fluid bed, IR radiation, autoclave), 3D printing (additive manufacturing) for prototypes and parts, Dip molding process for dip-molded parts
- Materials
- EPDM, NBR, H-NBR, ACM, CSM, FKM, FEPM, VMQ (Silicone)
- Certificates
- ISO 9001:2015, ISO 9001
- Founded
- 1930
- Industries
- Agricultural and construction machinery, Transport and commercial vehicles, Machinery and plant engineering, Mobility/Storage technology, Electrical engineering, Food industry
- 01
Application engineering consulting and like-for-like part analysis
- 02
Material and process selection
- 03
In-house production (waterjet, plotter, stamping press, die cutting) or sourcing
- 04
Component modularization (bonding, riveting, cleaning, finishing, packaging)
- 05
Warehousing and just-in-time/EDI delivery
Locations
Viernheim
DEHeadquarters with in-house production, goods receiving and shipping
- Lot size
- Prototypes to large-scale series
- Materials
- Elastomers, foams, fiber gasket materials, foams, thermoplastics, multilayers, soft metals
- 3D waterjet cutting machine (abrasive, 3D head)
- Pure-water waterjet system STM 2035 Premiumcut (7 heads)
- Plotter with oscillating cutting knife (1550 x 1550 mm)
- High-speed kiss-cut stamping press (parts up to 490 x 590 mm)
- Bridge and double-column clicker presses
- Testing laboratory
Components
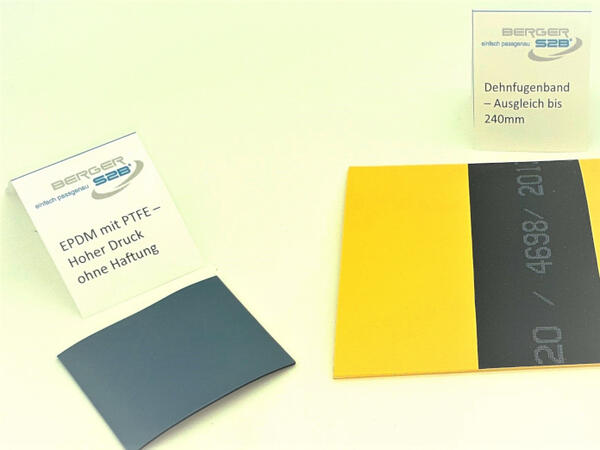
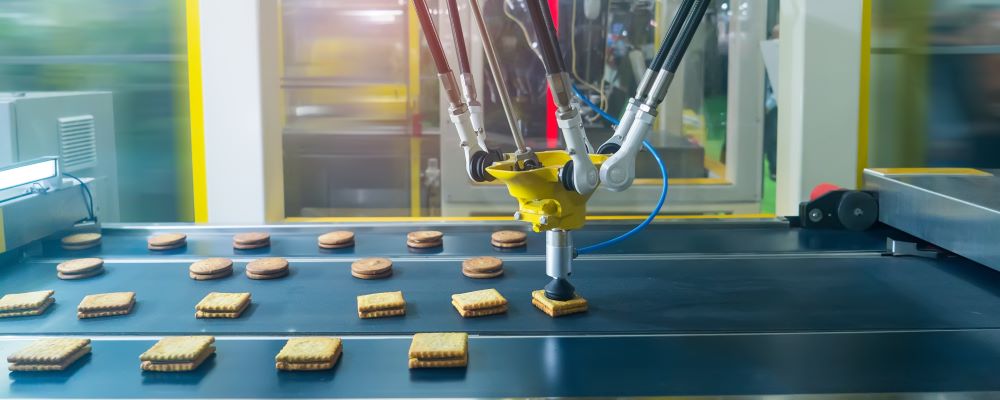
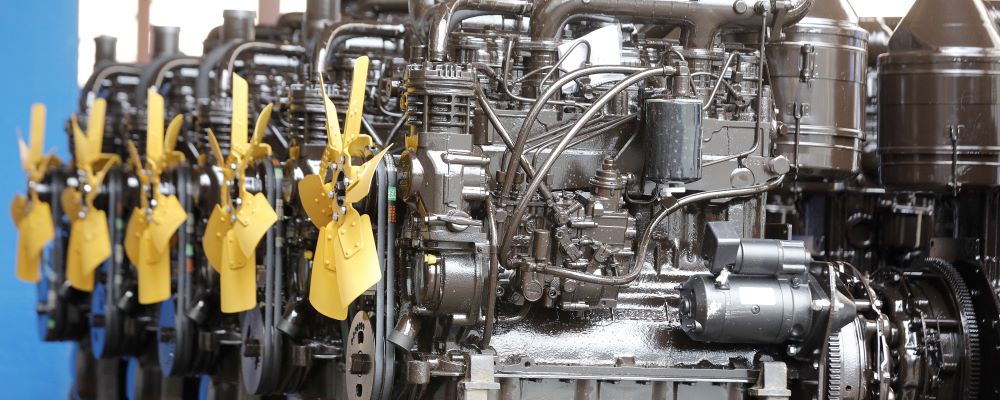
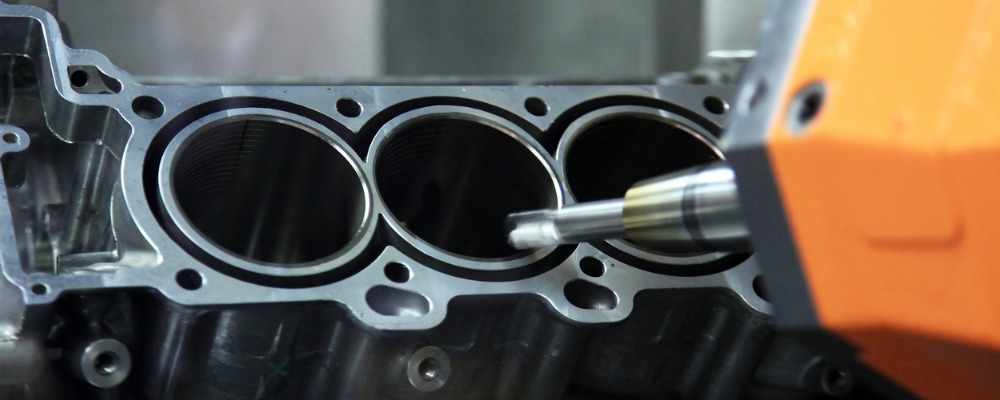
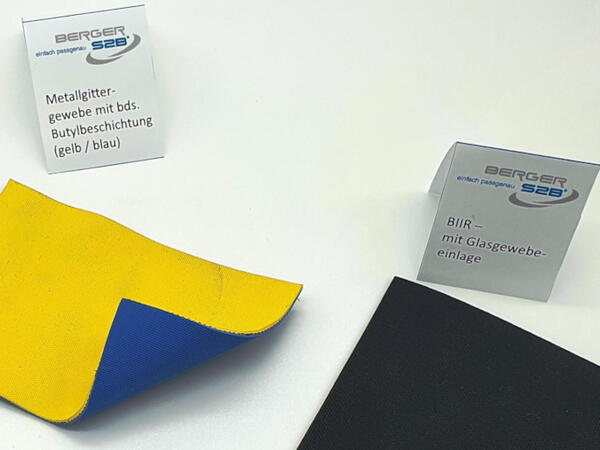
Inside the production
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Waterjet cutting (also 3D head, abrasive, pure water)Machining | ±0.1 mm | – | – | Prototypes/single parts – Large-scale series | – |
| Plotter cutting with oscillating cutting knifeMachining | ±0.1 mm | 1550 mm × Cutting height approx. 100 mm | – | Small series – medium quantities | Graphite (incl. stainless steel inserts up to 5 mm), Plastics, aramid-containing materials, Rubber, Foams, Felts |
| High-speed kiss-cut stamping press (endless material feed)Forming | Stamping accurate up to 0.05 mm | 590 mm × 490 mm | – | Large-scale series | Plastic foam, Foam material, Cellular rubber, soft elastomers, Multilayers, self-adhesive equipped materials |
| Die cutting (bridge and double-column clicker presses, solid die/steel rule cutting)Forming | tool-dependent according to DIN 7715 Part 5 P 2/3 | – | – | small quantities – medium quantities | Soft materials, Semi-finished products for flat gaskets |
| Molded part production by compression molding (CM), injection compression molding (ICM), transferPlastics | tightest tolerances (named) | – | – | Prototypes – Series | ACM, CSM, EPDM, NBR, H-NBR, VMQ/Silicone, NR, FKM, PUR, CR, IIR, IR, SBR, Thermoplastics (PTFE), Thermoplastic elastomers, Composite materials |
| Profile production (UHF, salt bath, shear head, hot air, fluid bed, IR radiation, autoclave)Plastics | – | – | – | – | ACM, CSM, EPDM, NBR, H-NBR, VMQ, Silicone, Silicone foam, NR, FKM, PUR, CR, IIR, IR, SBR, Soft PVC, TPE-S, TPE-V, Sponge rubber, Cellular rubber |
| 3D printing (additive manufacturing) for prototypes and partsAdditive | – | – | – | Prototypes/small quantities | Acrylic, Silicone, TPE, TPU, PEEK |
| Dip molding process for dip-molded partsPlastics | – | – | – | – | Polyurethane, Silicone, Latex, NR, CR |
| Formed in place gaskets (FIPG, liquid sealing systems)Joining | – | – | – | – | Silicone, Polyurethane, Acrylic |
| Rubber-metal bonds / Bonded Seals (thread and rubber-metal sealing rings)Joining | – | – | – | – | V2A, Brass, Aluminum, EPDM, FKM, NBR |
| Application engineering consulting / engineering (material and production process selection)Engineering | – | – | – | – | – |
| Component and part supply incl. bonding, riveting, cutting, cleaning, finishing, packagingAssembly | – | – | – | – | – |
| Insulating, isolating, fire/fire protection (heat protection products, multilayer flame barriers)Surface | – | – | – | – | Glass, Ceramics, Silicates, Elastomer foams, Plastic foams, FireStop polyolefin, Glass fabric, Mica, Thermal Patch, High-temperature boards (up to 1100 °C) |
7 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| 3D waterjet cutting machine (with 3D head, abrasive) | – | – | – | – | Viernheim |
| Pure-water waterjet system (7 heads) | STM 2035 Premiumcut | 1 | – | – | Viernheim |
| Plotter with oscillating cutting knife (incl. camera) | – | 1 | 1550 x 1550 mm | seit 2009 | Viernheim |
| High-speed kiss-cut stamping press (endless material feed) | – | – | Parts up to 490 x 590 mm | – | Viernheim |
| Bridge and double-column clicker presses | – | – | – | – | Viernheim |
| Die cutting shop (punching presses, historical) | – | – | – | historisch | – |
| Testing laboratory for quality assurance | – | 1 | – | seit 1985 | Viernheim |
Additional services
Reference customers
Quality
Berger S2B is certified by DQS according to DIN EN ISO 9001:2015 (first certified in 1997) and has had its own testing laboratory for quality assurance since 1985. The manufacturing processes in Viernheim are audited according to DIN EN ISO 9001:2015.
| Evidence | Viernheim |
|---|---|
| ISO 9001 |
History
- 1930
Founding of Karl Berger & Co. on 01.07.1930 by Karl and Maria Berger in Mannheim-Neuostheim; delivery of leather belts and gaskets to, among others, KSB, Heinrich Lanz, Karl Benz and MWM
- 1945
Concentration on distribution of rubber sheets, V-belts, conveyor belts, asbestos packings, cords, celluloid and stamped parts (KABECO)
- 1951
Sons Josef, Friedrich and Otto admitted as limited partners, succession second generation; new operating and warehouse building in the Schwetzinger Vorstadt
- 1954
Expansion of the building by three floors
- 1967
Move to new building in the Mühlfeld industrial area with 2,450 sqm of office, warehouse and production space
- 1980
Conversion to Gummi-Berger GmbH, entry of Karl-Friedrich Berger (third generation)
- 1985
Investment in testing laboratory for quality assurance, specialization in gasket and elastomer technology
- 1992
Investment in one of the first waterjet cutting systems in Germany
- 1994
Karl-Friedrich Berger becomes sole shareholder
- 1995
Distribution of the own brand AquaTerra® (porous rubber hose for underground irrigation)
- 1997
First certification according to ISO 9001 by DQS
- 1998
Discontinuation of AquaTerra distribution due to insolvency of the manufacturer
- 1999
Withdrawal from occupational safety/hose/valve distribution, focus on gasket and polymer technology; brands DichTec® and S2B® protected
- 2000
Self-conception as a service provider for gaskets and technical polymer products; single-sourcing processes incl. supply chain
- 2002
Renaming of Gummi-Berger to Berger S2B (January 2002)
- 2003
Award as top employer of the SME sector (ILAGO®); new ERP with EDI; certification according to DIN EN ISO 9001:2000
- 2009
Purchase of a plotter to expand single-part and small-series production
- 2010
Simon Treiber... (source incomplete)