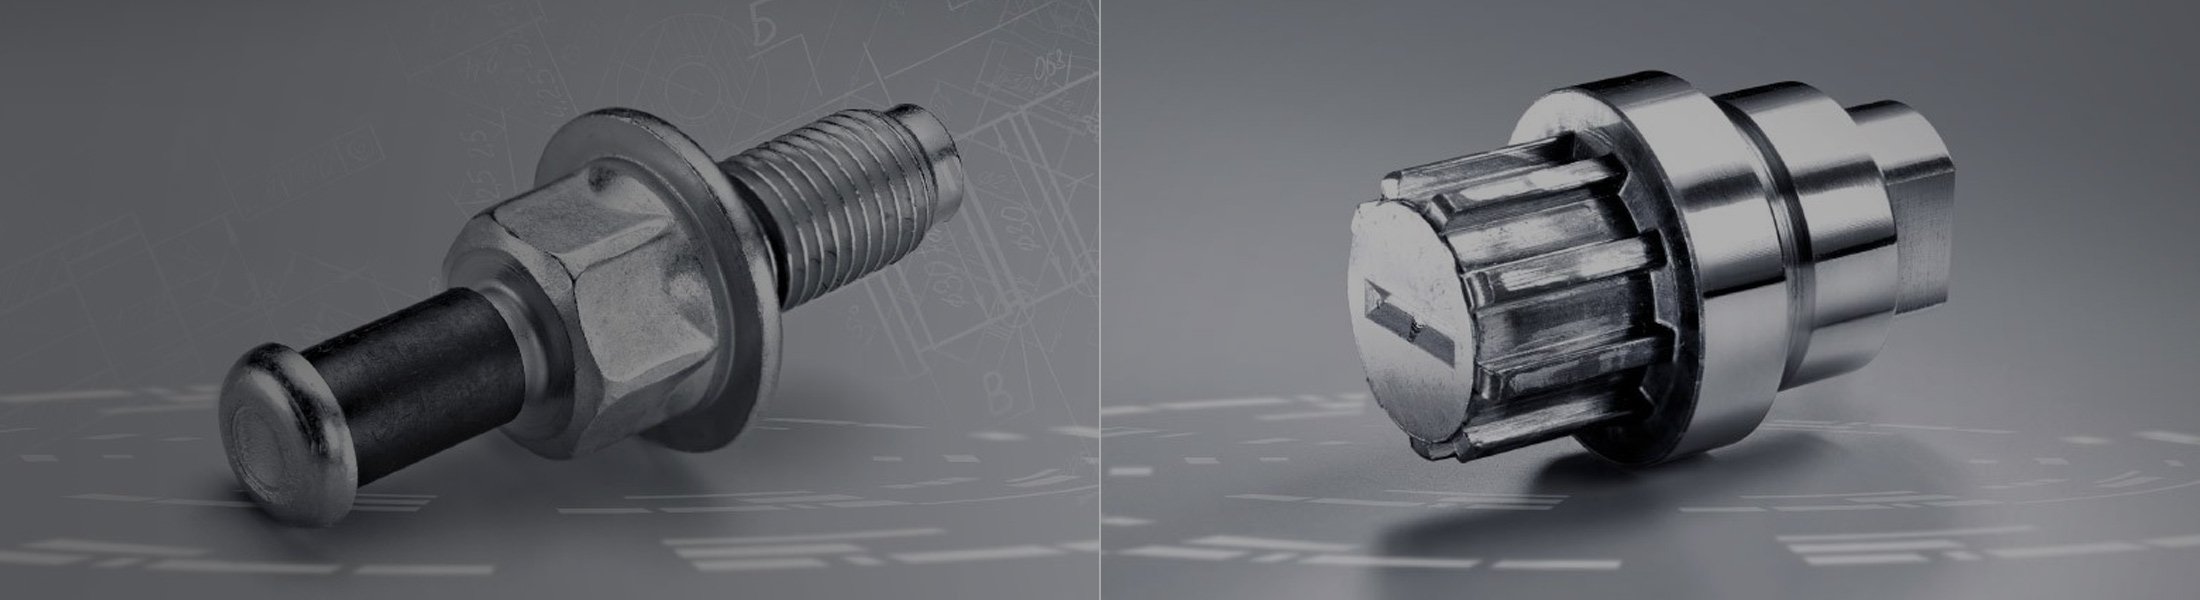
Manufacturer of custom cold-extruded parts, turned parts and metal closure screws for automotive, mechanical engineering and hydraulics.
Bilstein & Siekermann GmbH & Co. KG
54576 Hillesheim, GermanyNew on Amplifa
Development and manufacturing partner for complex formed parts
Bilstein & Siekermann (BSH) is an internationally oriented developer and manufacturer of metal formed parts based in Hillesheim in the Eifel region. The company produces custom and standard-like cold-extruded parts (BSH cold forming), turned parts (BSH turning) and closure screws up to M 60 as hot-forged parts with machining. Dimensions range from 5 to 60 mm; processed materials include all types of steel (including 35B2), aluminium, brass, copper and soft iron. In addition to manufacturing, BSH offers integrated services: heat treatment (quench and tempering, case hardening, nitriding, induction hardening, annealing), surface treatment and corrosion protection, thread rolling after coating, thread pre-coating, cleaning with a residual dirt laboratory, and pre-assembly of metallic and elastomer sealing rings and permanent magnets. Application engineering supports customers with manufacturability analyses and forming simulation from idea to mass production. Customers come from automotive, mechanical and plant engineering, hydraulics, the construction industry as well as trade and services, and are supplied worldwide. Around 125 employees produce on 12,000 m² of floor space; since 2003 the company has belonged to the INDUS Holding AG.
- Site
- Hillesheim
- Processes
- Cold forming (BSH cold forming®, cold extrusion), Turning (BSH turning®), Hot forging (closure screws up to M 60) with machining, Thread rolling after coating / thread recalibration (BSH flat®), Thread pre-coating (BSH sealing-T), Heat treatment: quench and tempering, Heat treatment: case hardening, Heat treatment: nitriding
- Materials
- Steel 35B2, Steel, Aluminium, Brass, Copper, Soft iron, Elastomer, Permanent magnets
- Certificates
- ISO 9001:2015, IATF 16949:2016, DIN EN ISO 14001:2015, DIN EN ISO 50001:2018, DIN ISO 45001:2023, TISAX Assessment, ISO 9001, IATF 16949, ISO 14001, ISO 50001, ISO 45001, Other (TISAX)
- Founded
- 1956
- Employees
- 125
- Industries
- Automotive, Mechanical and plant engineering, Hydraulics, Construction industry, Trade and services
- 01
Engineering (BSH engineering): manufacturability analysis, forming simulation,
- 02
Cold forming (BSH cold forming): cold extrusion on 4-, 5- and 6-station
- 03
Turning (BSH turning): machining on CNC and cam-controlled
- 04
Heat treatment (BSH solid): quench and tempering, case hardening, nitriding,
- 05
Surface treatment (BSH coating): galvanic finishing, corrosion protection,
- 06
Thread rolling after coating / recalibration (BSH flat)
- 07
Assembly (BSH integrated services): sealing rings, permanent magnets,
- 08
Cleaning (BSH clean): washing systems, residual dirt monitoring in the
- 09
Inspection and delivery
Materials and processes
Cold forming (cold extrusion)
Efficient process with minimized raw material consumption (e.g. 9 g chip portion instead of 105 g when turning) and high component cleanliness.
Turning
For prototypes, small to medium series and spare parts requirements; multi-spindle automatic lathes up to 51 mm, single-spindle automatic lathes up to 60 mm.
Heat treatment
Quench and tempering, case hardening, nitriding, nitrocarburizing, induction hardening, annealing and remanence annealing to adjust strength and magnetic properties.
Surface treatment
Galvanic surface finishing, surface zinc plating and corrosion protection for durable components.
Thread pre-coating
Thread pre-coating with sealing materials that seal and secure closure screws.
Thread rolling after coating
Recalibration of threads after surface finishing to avoid problems during screwing in.
Steel (including 35B2)
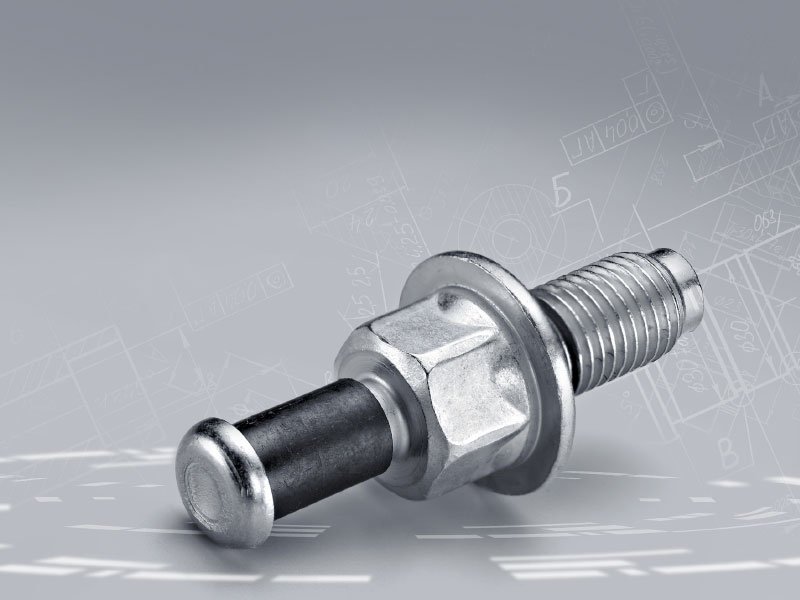
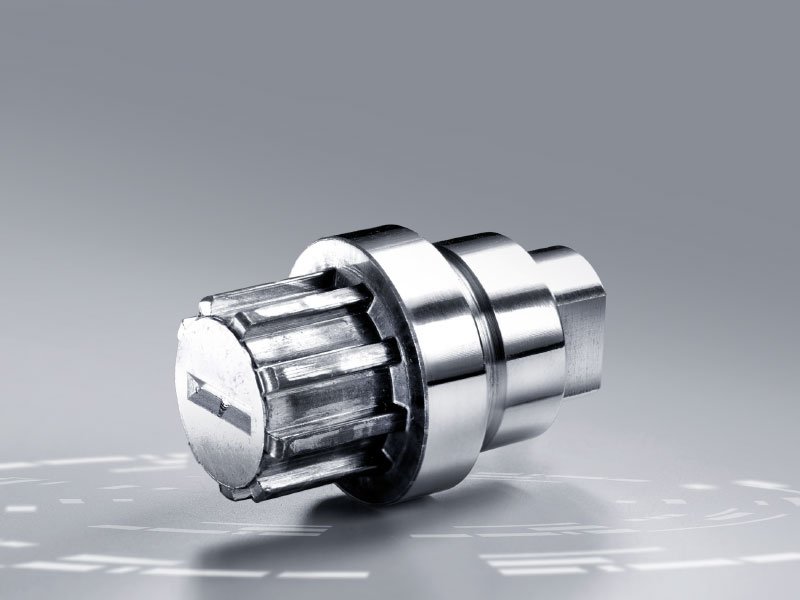
Base material for cold-extruded parts, locking bolts, detent screws and closure screws.
Aluminium
Lightweight pressed parts with low weight, corrosion resistance and high tensile strength, e.g. for the automotive industry.
Brass
Non-magnetic, spark-free pressed parts with good corrosion resistance as well as thermal and electrical conductivity.
Copper and soft iron
Materials for metallic sealing rings on closure screws.
Seal and magnet assembly
Pre-assembly of metallic sealing rings, elastomer seals and permanent magnets into ready-to-install assemblies.
Hillesheim site
Hillesheim
DEProduction and administration (headquarters)
- Lot size
- Prototype, small, medium and large series
- Materials
- Steel (including 35B2), aluminium, brass, copper, soft iron
- Multi-station presses (4-, 5- and 6-station cold formers, pressing force up to 3600 kN)
- Cold extrusion presses (max. wire diameter 28 mm or 22 mm)
- CNC lathes with robot loading
- CNC twin-spindle lathes
- Multi-spindle automatic lathes
- Cam-controlled lathes
- Washing systems
Products and components
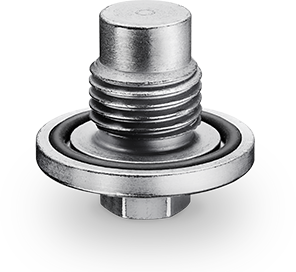
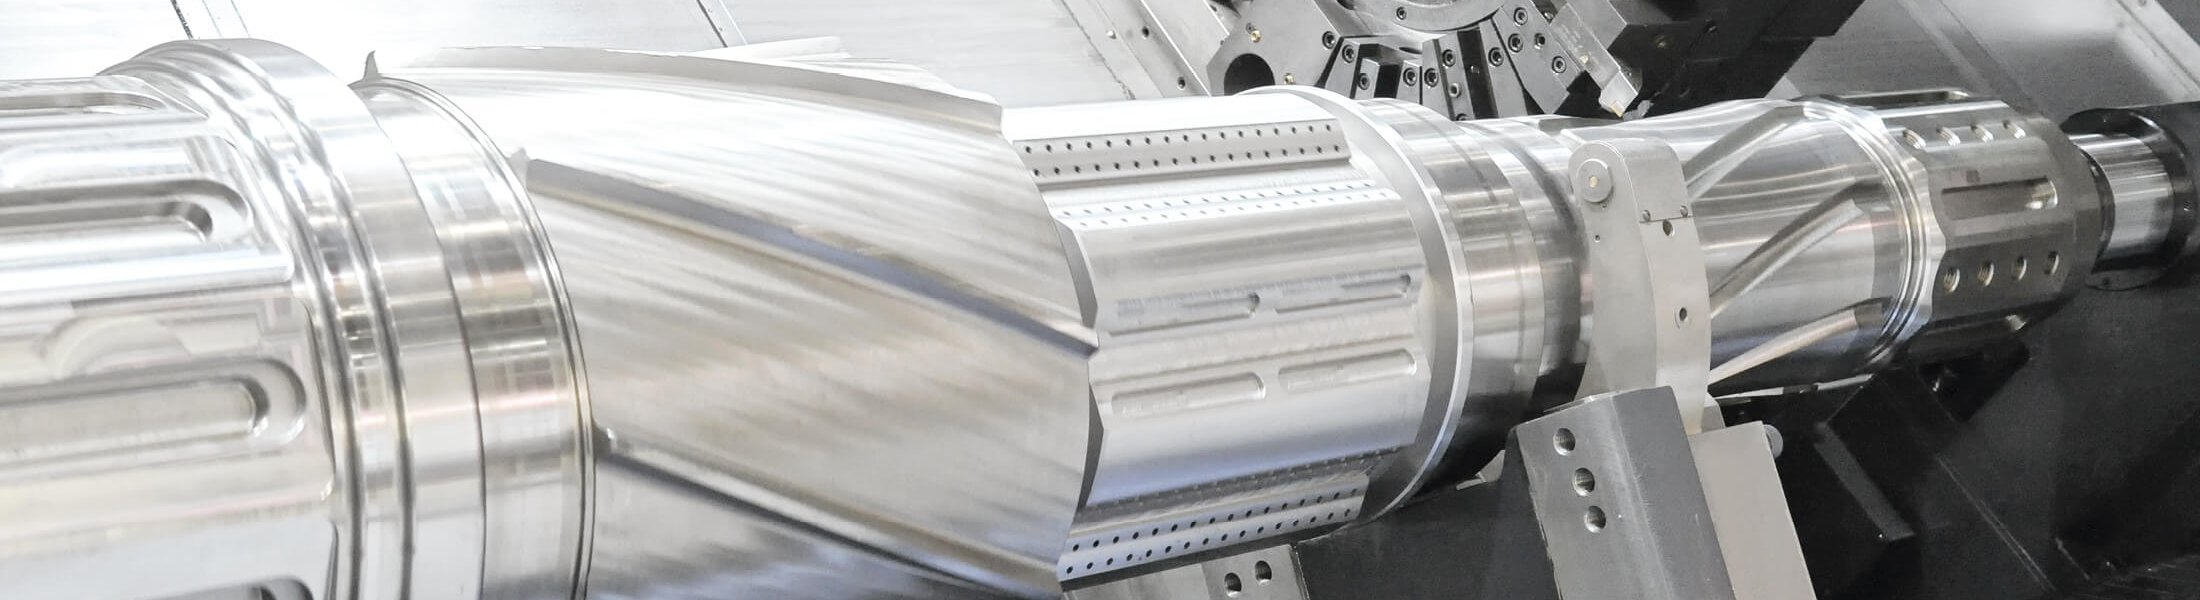
Inside the production
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Cold forming (BSH cold forming®, cold extrusion)Forming | tight tolerances | 60 mm × 60 mm (dimension range) | – | Mass production | Steel, Aluminium, Brass |
| Turning (BSH turning®)Machining | – | 60 mm | – | small to medium series – medium series | – |
| Hot forging (closure screws up to M 60) with machiningForming | – | – | – | – | – |
| Thread rolling after coating / thread recalibration (BSH flat®)Forming | – | – | – | – | – |
| Thread pre-coating (BSH sealing-T)Surface | – | – | – | – | – |
| Heat treatment: quench and temperingHeat treatment | – | – | – | – | Steel |
| Heat treatment: case hardeningHeat treatment | – | – | – | – | Steel |
| Heat treatment: nitridingHeat treatment | – | – | – | – | Steel |
| Induction hardening (screw head)Heat treatment | – | – | – | – | Steel 35B2 |
| Surface treatment: corrosion coating / galvanic surface finishing /Surface | – | – | – | – | – |
| Cleaning and monitoring of residual dirt levels in the laboratory (BSH clean®)Surface | – | – | – | – | – |
| Assembly / pre-assembly of sealing rings (BSH sealing-M® metallic, BSH sealing-E® elastomer)Assembly | – | – | – | – | Aluminium, Copper, Soft iron, Elastomer |
| Assembly of permanent magnets in closure screws (BSH magnetic)Assembly | – | – | – | – | Permanent magnet |
| Plastic coating (below the head)Surface | – | – | – | – | – |
| Design and development (BSH engineering), manufacturability analyses, forming simulationEngineering | – | – | – | – | – |
| Prototype manufacturing using machining processesMachining | – | – | – | – | – |
5 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| CNC lathes | – | – | – | – | Hillesheim |
| Cam-controlled lathes | – | – | – | – | Hillesheim |
| Multi-spindle automatic lathe | – | – | – | – | Hillesheim |
| Multi-station press system | – | – | – | – | Hillesheim |
| Washing systems | – | – | – | – | Hillesheim |
Additional services
Quality management
The IATF 16949-certified quality management inspects length, form and position tolerances in a well-equipped measuring room with a 3D coordinate measuring machine, contour measuring devices, form testers, hardness testers and projectors; measuring stations in production monitor quality at the machines. An in-house residual dirt laboratory controls technical component cleanliness according to the strict standards of the VDA 19 directive.
| Evidence | Hillesheim |
|---|---|
| ISO 9001 | |
| IATF 16949 | |
| ISO 14001 | |
| ISO 50001 | |
| ISO 45001 | |
| Other (TISAX) |
Company history
- 1954
Ferdinand Bilstein and Arnold Siekermann decide to establish a company in the Eifel region.
- 1956
Construction of the first production hall in Hillesheim; production start in September with five employees, ceremonial opening on 3 October under the name Bilstein & Siekermann.
- 1967
Death of co-founder Ferdinand Bilstein on 11 May; Rolf Bilstein takes over responsibility.
- 1971
Conversion into a GmbH & Co. KG with managing directors Rolf Bilstein and Arnold Siekermann; expansion of the automatic turning shop and cold pressing shop.
- 1976
Expansion of the management team to include Bernd Clever.
- 1982
Dieter Siekermann succeeds his father Arnold Siekermann on the management board.
- 2001
Completion of a new production and warehouse hall; total of 12,000 m² of floor space.
- 2003
Sale of shares to the INDUS Holding AG.
- 2005
Investment in a new 5-station cold former.
- 2006
Bruno Hirtz becomes managing director in Hillesheim; Bernd Clever retires after 30 years.
- 2010
Investment in a new six-station cold extrusion press (max. wire diameter 28 mm, pressing force 3600 kN).
- 2011
Two lines with three CNC lathes each with robot loading go into operation.
- 2013
Second six-station cold extrusion press (max. wire diameter 22 mm, pressing force 2750 kN) with NC-controlled transfer carriage.
- 2014
Investment in CNC twin-spindle lathes.
- 2017
International registration of the product brands BSH cold forming®, BSH flat®, BSH sealing-M®, BSH sealing-E® and BSH clean®.
- 2019
Expansion of the product and service portfolio with further brands: BSH turning, BSH engineering, BSH plug, BSH integrated services, BSH sealing-T, BSH coating, BSH magnetic, BSH solid.