Manufacturing of precision springs, micro turned parts, stamped and bent parts and plastic composite parts for precision engineering, medical and automotive technology.
CARL HAAS GmbH
Schramberg (Headquarters, Production)New on Amplifa
About CARL HAAS
CARL HAAS GmbH, based in Schramberg, is a precision engineering specialist in wire and strip processing as well as plastic joining technology. The company manufactures spiral springs, technical precision springs made from wire and strip, micro turned parts with diameters from 0.2 to 4.0 mm, stamped and bent parts and flat form springs, as well as plastic parts and complex plastic composite parts produced by injection moulding. The value chain extends from in-house developed drawing and rolling of ultra-fine wires with tolerances of ±0.1 µm, through heat treatment, laser welding and electroplated surface treatment, to component cleaning according to technical cleanliness criteria and customer-specific packaging. As the plastics competence centre of the KERN-LIEBERS group, CARL HAAS supplies system suppliers to the automotive industry, medical technology, measurement and control technology as well as the watch and electrical industries. The company employs around 230 people including its foreign production companies and has been active in Schramberg since 1904; effective 1 July 2026, it will be renamed KERN LIEBERS Lienberg GmbH.
- Site
- Schramberg
- Processes
- Spring Technology (springs from wire and strip: winding, coiling, grinding), Winding (CNC-controlled winding machines with rotating winding mandrels), Grinding of spring ends (compression springs), Heat treatment (incl. protective gas and vacuum annealing), Manufacturing of micro turned parts, Injection moulding (plastic parts and plastic composite parts), Stamped and bent technology (stamped and bent parts, form springs, plastic hybrid parts), Resistance welding, thread forming and riveting (sub-processes of stamped and bent technology)
- Materials
- NIVAROX, Stainless steel 1.4305, Stainless steel 1.4104, Aluminium, Brass, Free-cutting steel, Silver steel, CuSn alloy (bronze)
- Certificates
- DIN EN ISO 9001, IATF 16949, DIN EN ISO 13485, DIN EN ISO 14001, DIN EN ISO 50001, ISO 9001, ISO 13485, ISO 14001, ISO 50001
- Founded
- 1904
- Employees
- 230 (incl. foreign
- Industries
- Automotive, Medical technology, Measurement and control technology, Watch industry, Precision engineering/Precision technology, Electrical engineering
- 01
Engineering/Development
- 02
Drawing and rolling of ultra-fine wires
- 03
Springs from wire and strip (winding, coiling, grinding)
- 04
Stamped and bent technology
- 05
Micro turned parts manufacturing
- 06
Injection moulding/plastic composite parts
- 07
Laser welding technology
- 08
Heat treatment
- 09
Surface treatment
- 10
Component cleaning
- 11
Quality assurance
- 12
Customer-specific packaging/assembly
Materials & Processes
NIVAROX
Alloy patented in 1928, temperature-independent, for balance hairsprings in watchmaking technology.
Stainless steel 1.4305
Stainless steel for micro turned parts with corrosion and machinability requirements.
Stainless steel 1.4104
Stainless steel for micro turned parts with improved machinability.
Free-cutting steel / silver steel
Machining materials for precision turned parts in precision engineering and medical technology.
Spring steel
Proven material for wire, strip and form springs.
CuSn, CuBe, CuZn and CuFe alloys
Copper alloys for current-carrying stamped and bent parts, current-measuring springs and contact springs.
Brass
Material for micro turned parts and stamped and bent components.
Aluminium
Light metal for micro turned parts.
Bimetals
Material for spiral coiled springs for temperature measurement from -40 °C to 500 °C.
Special alloys
For spiral springs in measurement technology with special spring characteristics.
Plastic
Injection moulding material for plastic parts and plastic composite parts (hybrid, insert and reel-to-reel parts).
Sites
Schramberg
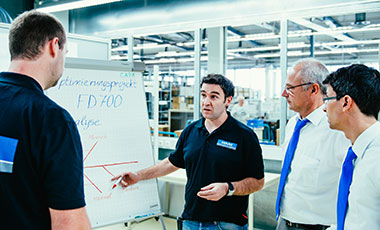
DEHeadquarters and production (springs, micro turned parts, stamped and bent, injection moulding and laser welding
- Materials
- Spring steel, copper alloys, stainless steel 1.4305/1.4104, bimetals, plastic
- CNC-controlled winding machines with rotating winding mandrels
- Automatic CNC winding machines
- Bihler machines
- Stamping and bending cells (reel-to-reel, punching force 0.5–30 t)
- Injection moulding machines
- Laser welding systems
- In-house developed drawing machines and rolling mills (±0.1 µm)
- Heat treatment systems (protective gas/vacuum annealing)
- Testing machines with force-displacement measurement and camera-based geometry inspection
- Optical and tactile 2D/3D measuring systems
Parts
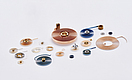
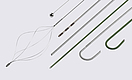
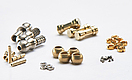
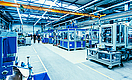
Inside the production
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Spring Technology (springs from wire and strip: winding, coiling, grinding)Forming | – | – | – | – | Spring steel, Copper alloys, Nivarox |
| Winding (CNC-controlled winding machines with rotating winding mandrels)Forming | – | – | – | – | Spring wire |
| Grinding of spring ends (compression springs)Surface | – | – | – | – | Metallic materials |
| Heat treatment (incl. protective gas and vacuum annealing)Heat treatment | – | – | – | – | Spring wire, Wire springs |
| Manufacturing of micro turned partsMachining | – | – | – | Any lot size | 1.4305, 1.4104, Aluminium, Brass, Free-cutting steel, Silver steel |
| Injection moulding (plastic parts and plastic composite parts)Plastics | – | – | – | – | Plastic |
| Stamped and bent technology (stamped and bent parts, form springs, plastic hybrid parts)Forming | Slot and web widths down to 0.1 mm; radii down to 0.05 mm | Max. strip width 100 mm × Material thickness 0.05-1 mm | – | High-volume production | CuSn alloys, CuBe alloys, CuZn alloys, CuFe alloys, Steel and spring steel |
| Resistance welding, thread forming and riveting (sub-processes of stamped and bent technology)Joining | – | – | – | – | Stamped and bent part alloys |
| Laser welding technology (spot and seam welds)Joining | – | – | – | – | – |
| Surface treatment (electroplating with precious metals, greasing, zinc flake coating)Surface | – | – | – | – | – |
| Electroplated surface treatment (gold plating, silver plating, nickel plating, tin plating, zincSurface | – | – | – | – | – |
| Phosphating, zinc flake coating (Delta Seal), PTFE coatingSurface | – | – | – | – | – |
| Oiling and greasing (corrosion protection)Surface | – | – | – | – | – |
| Blasting (sand blasting and shot blasting)Surface | – | – | – | – | – |
| Tumbling / vibratory finishing (deburring, polishing)Surface | – | – | – | – | – |
| PolishingSurface | – | – | – | – | – |
| PaintingSurface | – | – | – | – | – |
| Component cleaning (technical cleanliness, inline micro-phase cleaning)Surface | – | – | – | – | – |
| Drawing and rolling (round and flat wires)Forming | ±0.0001 mm (±0.1 µm) | – | – | – | Round and flat wires |
| Engineering / Development (design support for components)Engineering | – | – | – | – | – |
| Customer-specific packaging (bulk, blister, reel, magazines)Assembly | – | – | – | – | – |
| Assembly and fitting (incl. inline assembly of plastic parts)Assembly | – | – | – | – | – |
| Quality assurance (100% inspection, force-displacement measurement, geometry, residual dirtTesting | – | – | – | – | – |
| Manufacturing of spiral springs for measuring instrumentsForming | – | Strip width up to 4 mm × Strip thickness from 0.01 mm | – | Small series/Prototyping – Fully automatic spring production | Copper alloys, Stainless spring steel, Special alloys |
| Manufacturing of deflection springsForming | – | – | – | – | Copper alloys, Spring steel |
| Manufacturing of spiral coiled springs (bimetal)Forming | – | Strip width from 1 mm × Strip thickness from 0.05 mm | – | – | all commercially available bimetals |
10 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| CNC-controlled winding machines with rotating winding mandrels | – | – | – | – | Schramberg |
| Automatic CNC winding machines | – | – | – | – | Schramberg |
| Bihler machines (stamped and bent/form spring production) | Bihler | – | – | – | Schramberg |
| Stamping and bending cells (reel-to-reel technology, punching force 0.5-30 t) | – | – | Max. strip width 100 mm, max. feed 150 mm, material thickness 0.05-1 mm | – | Schramberg |
| Injection moulding machines / injection moulding tools | – | – | – | – | Schramberg |
| Laser welding systems | – | – | – | – | Schramberg |
| Drawing machines and rolling mills (in-house developed, tolerance ±0.0001 mm) | CARL HAAS (in-house developed) | – | – | – | Schramberg |
| Heat treatment systems (protective gas and vacuum annealing) | – | – | – | – | Schramberg |
| Testing machines for springs (force-displacement measurement, geometry measurement via camera | – | – | – | – | Schramberg |
| Optical and tactile 2D and 3D measuring systems (inline inspections, image processing) | – | – | – | – | Schramberg |
Additional services
Quality
An integrated management system for quality, environment and energy safeguards process and product quality; optical and tactile 2D/3D measuring methods and computer-aided image processing systems are integrated into production as inline inspections. Inspection services include 100% geometry and force-displacement measurements, residual dirt analysis in accordance with VDA Volume 19 as well as customer-specific fatigue and endurance tests.
| Evidence | Schramberg |
|---|---|
| ISO 9001 | |
| IATF 16949 | |
| ISO 13485 | |
| ISO 14001 | |
| ISO 50001 |
History
- 1904
Foundation of CARL HAAS in Schramberg; start of production of balance hairsprings for mechanical watches.
- 1928
Development and patenting of the temperature-independent material alloy NIVAROX.
- 1949
Expansion of the production programme to include spiral springs for electrical measuring instruments.
- 1971–1992
Market leadership of the HAAS-LASER brand in the watch and precision engineering industry.
- 2026
Announced renaming of CARL HAAS to KERN LIEBERS Lienberg GmbH effective 1 July 2026.