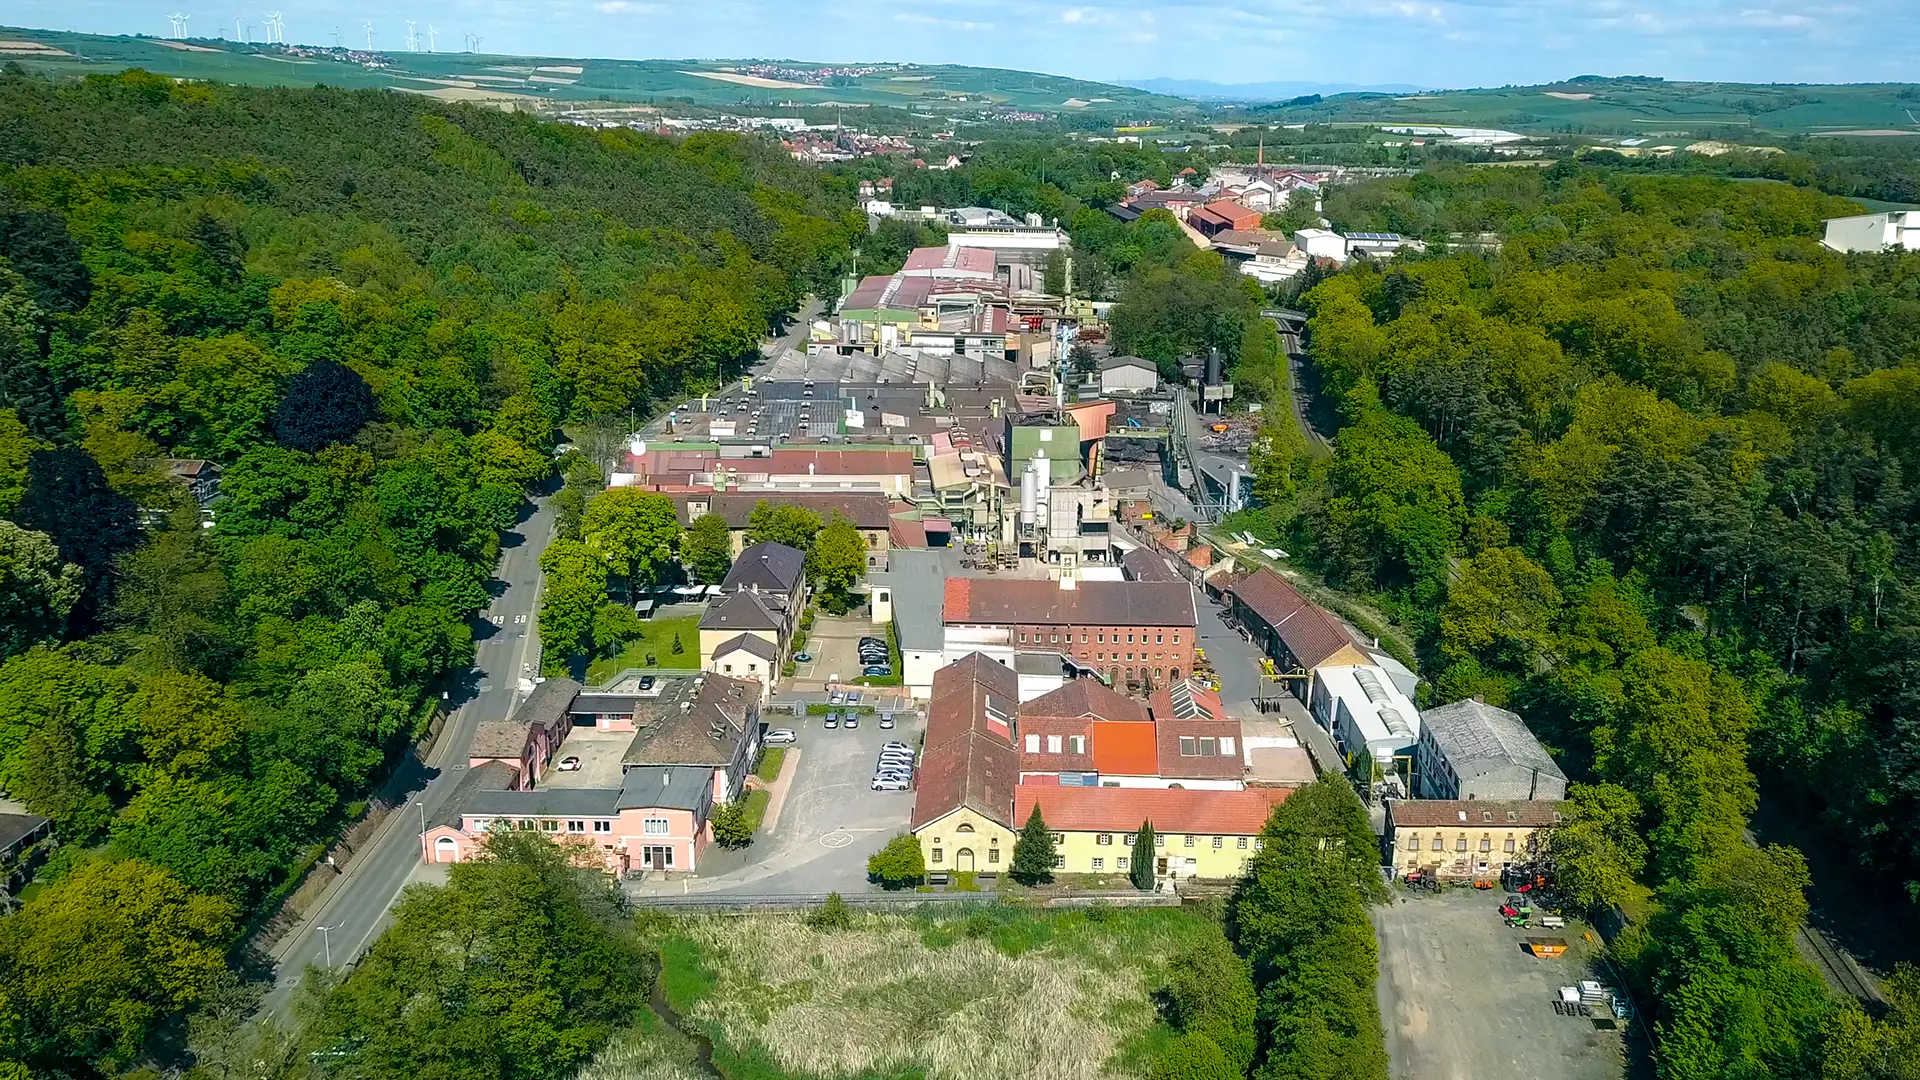
Complete cast iron solutions from recycling through machine and hand moulding casting to machining, finishing and assembly
DIHAG Gienanth GmbH
Eisenberg (Palatinate), GermanyNew on Amplifa
About DiHAG Gienanth
DIHAG Gienanth GmbH manufactures highly complex cast iron components in Eisenberg (Palatinate) and covers the entire process in a closed material cycle: from the recycling of steel scrap and casting scrap through melting and casting to machining, surface finishing and pre-assembly of ready-to-install solutions. Production includes grey cast iron with lamellar graphite (GJL), vermicular graphite (GJV) and spheroidal graphite (GJS), including special materials. Machine moulding casting on five vertical moulding lines serves part weights up to 30 kg in medium and large series, while hand moulding casting covers single parts and small series up to 5 t. The melting operation achieves a maximum output of 197,000 t of liquid iron per year. Customer industries include passenger cars, commercial vehicles, agricultural machinery, mechanical engineering, decentralised power supply, data centres, railways and marine. The company is part of the internationally active DiHAG Integrated Foundry Group and has been recognised multiple times by customers such as MTU/Rolls-Royce Power Systems and Schaeffler.
- Site
- Eisenberg (Palatinate)
- Processes
- Hand moulding casting, Machine moulding casting (vertical moulding lines), Machining (cutting), Surface finishing / painting / coating, Assembly / pre-assembly (ready-to-install product solutions), Recycling (steel scrap, casting scrap, recycled material), Design & simulation (Siemens NX CAD/CAM/CAE, Magmasoft), 3D printing / rapid prototyping
- Materials
- Grey cast iron with lamellar graphite (GJL), Cast iron with vermicular graphite (GJV), Cast iron with spheroidal graphite (GJS), Special GJS materials, Pig iron, Steel scrap, Casting scrap, Hand moulding casting
- Certificates
- Certified standards in all processes, 100% inspection of the finest tolerances, Optical measuring methods / sampling, CNC tactile metrology, Robot-assisted QA for large castings
- Founded
- 1735
- Industries
- Passenger cars (automotive industry), Commercial vehicles, Agricultural machinery, Mechanical engineering, Decentralised power supply, Data centres
- 01
Recycling (steel scrap, casting scrap, recycled material)
- 02
Melting (cupola furnace, induction furnaces)
- 03
Casting (machine moulding / hand moulding casting)
- 04
Machining
- 05
Surface finishing / painting
- 06
Assembly / pre-assembly
- 07
Just-in-sequence delivery of ready-to-install solutions
Materials & Processes
Grey cast iron with lamellar graphite (GJL)
Standard material for machine and hand moulding casting across all industries.
Cast iron with vermicular graphite (GJV)
Material with increased strength, among other things for large engine components.
Cast iron with spheroidal graphite (GJS)
Tough casting material for highly stressed components in automotive and mechanical engineering.
Special GJS materials
Individually developed material solutions for specific customer requirements.
Hand moulding casting
For single parts and small series with part weights up to 5 t.
Machine moulding casting (vertical moulding lines)
Automated production of parts up to 30 kg for series and spare parts supply.
Design & Simulation (Siemens NX, Magmasoft)
Casting-optimised design and simulation of mould filling, solidification and component stress.
Rapid Prototyping / 3D printing
Fast samples and testing of new geometries during development.
Locations
Eisenberg (Palatinate)
DEHeadquarters / Foundry / Machining
- Part weight / size
- Machine moulding casting up to 30 kg · Hand moulding
- Lot size
- Single parts, small series, medium and large series, spare parts supply
- Materials
- GJL, GJV, GJS, special materials
- 1 x hot-blast cupola furnace (max. 30 t/h)
- 1 x 5-t line-frequency induction crucible furnace
- 3 x 8-t medium-frequency induction crucible furnaces
- 3 x 60-t holding furnaces
- 5 x vertical moulding lines
- Automated magnesium wire treatment with digital batch control system
- Siemens NX CAD/CAM/CAE
- Magmasoft simulation
Components
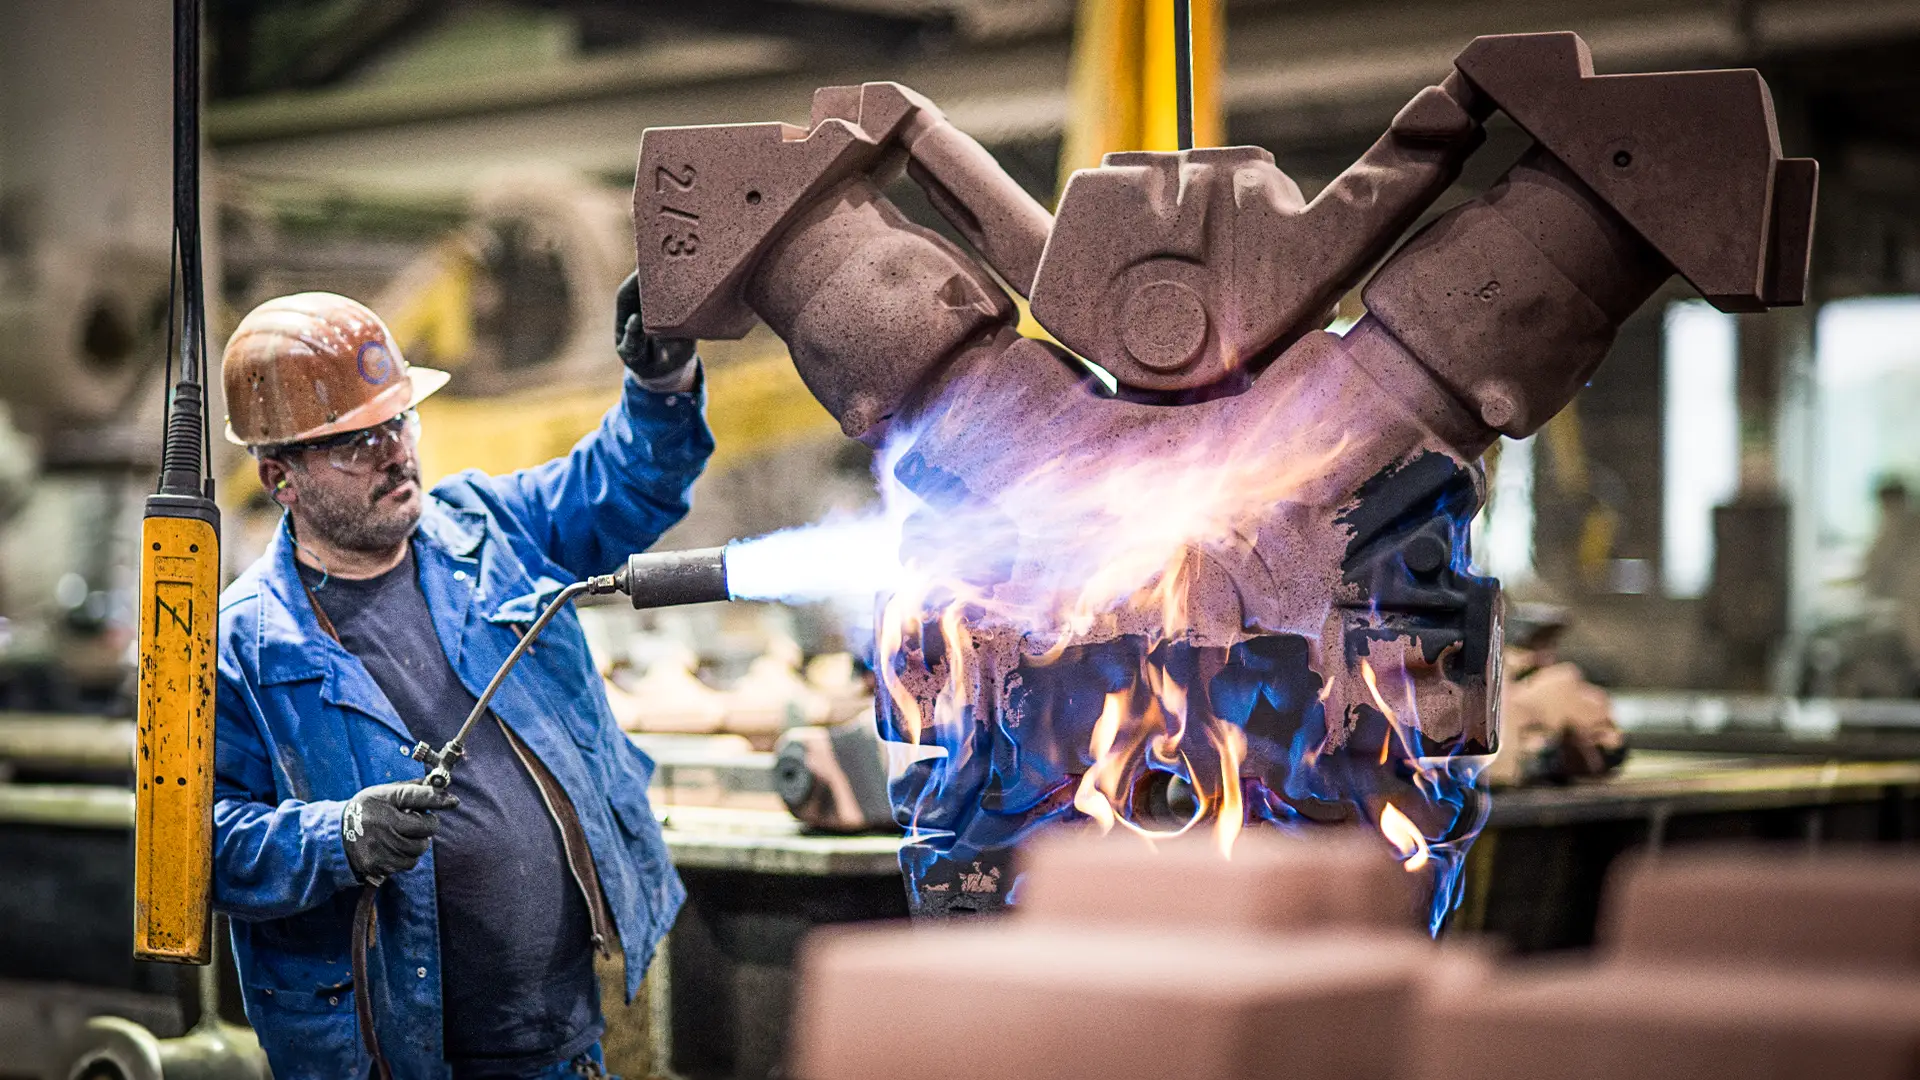
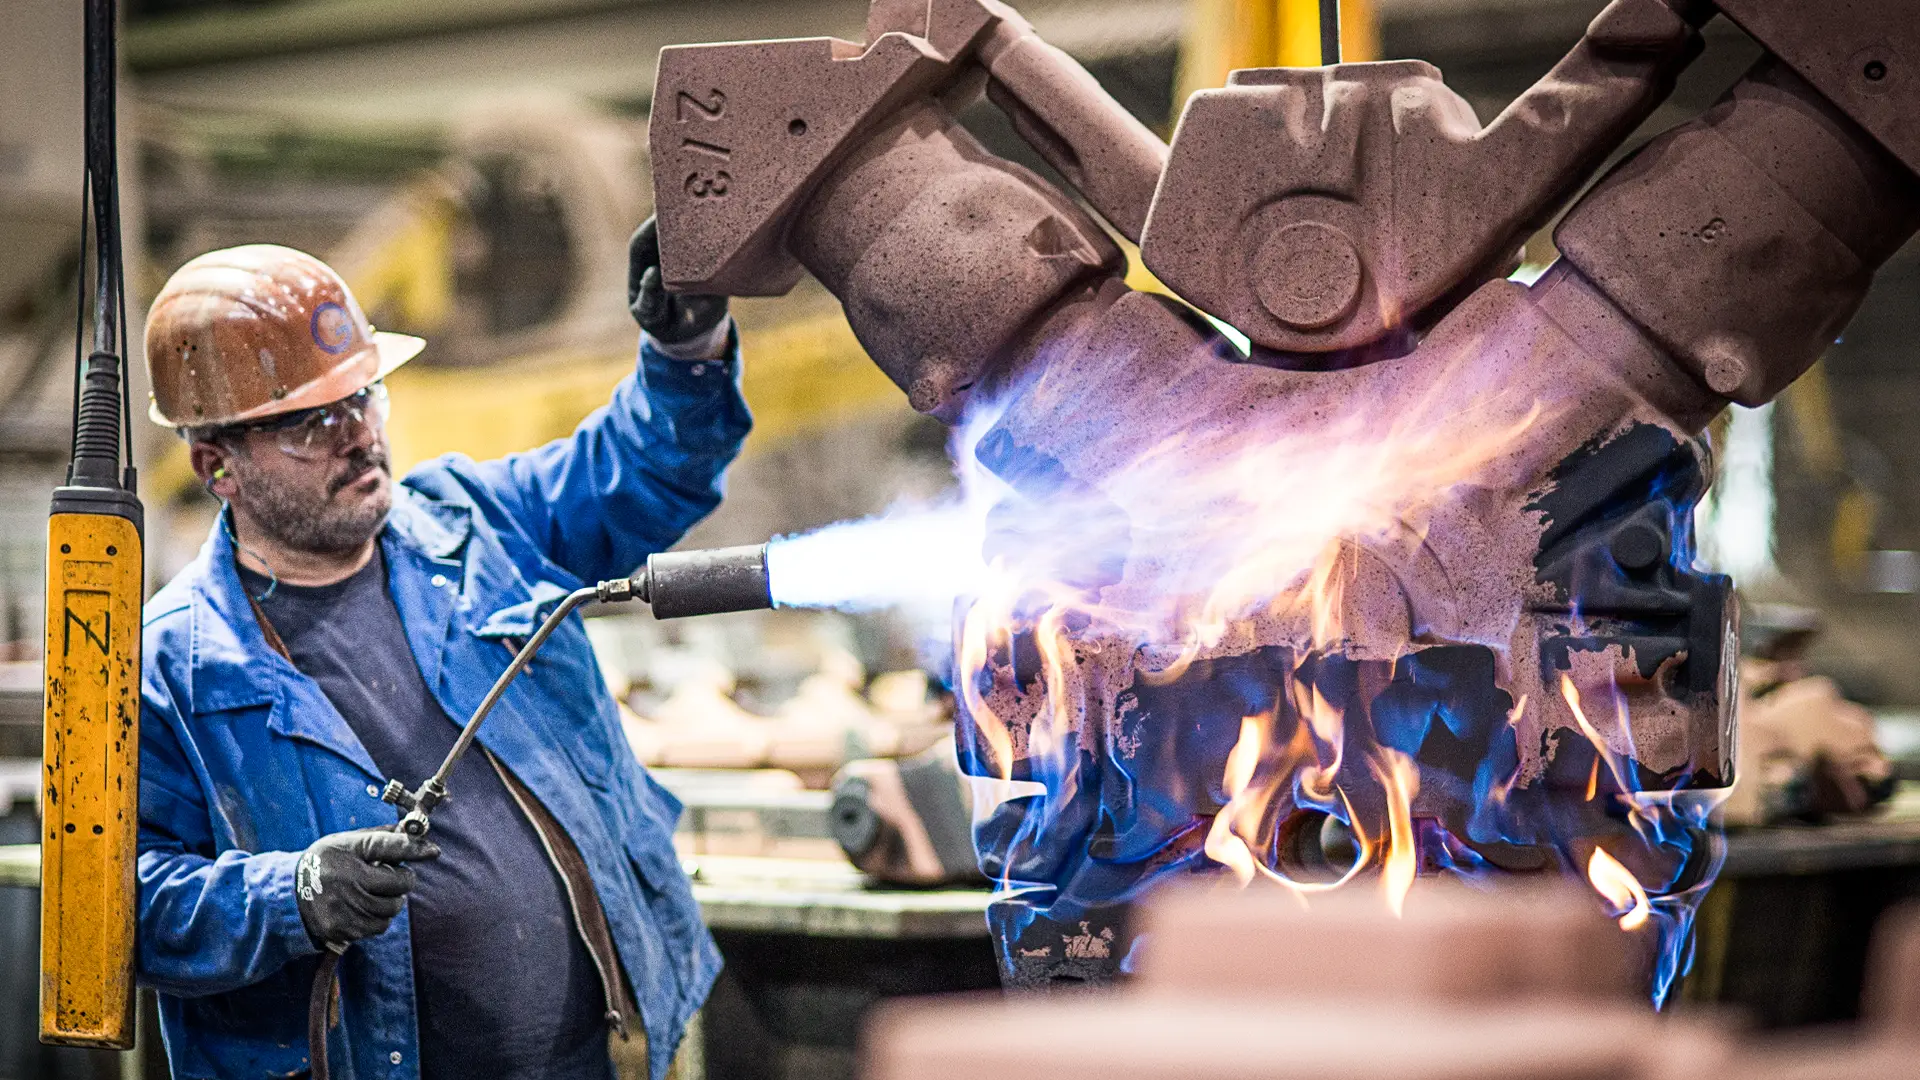
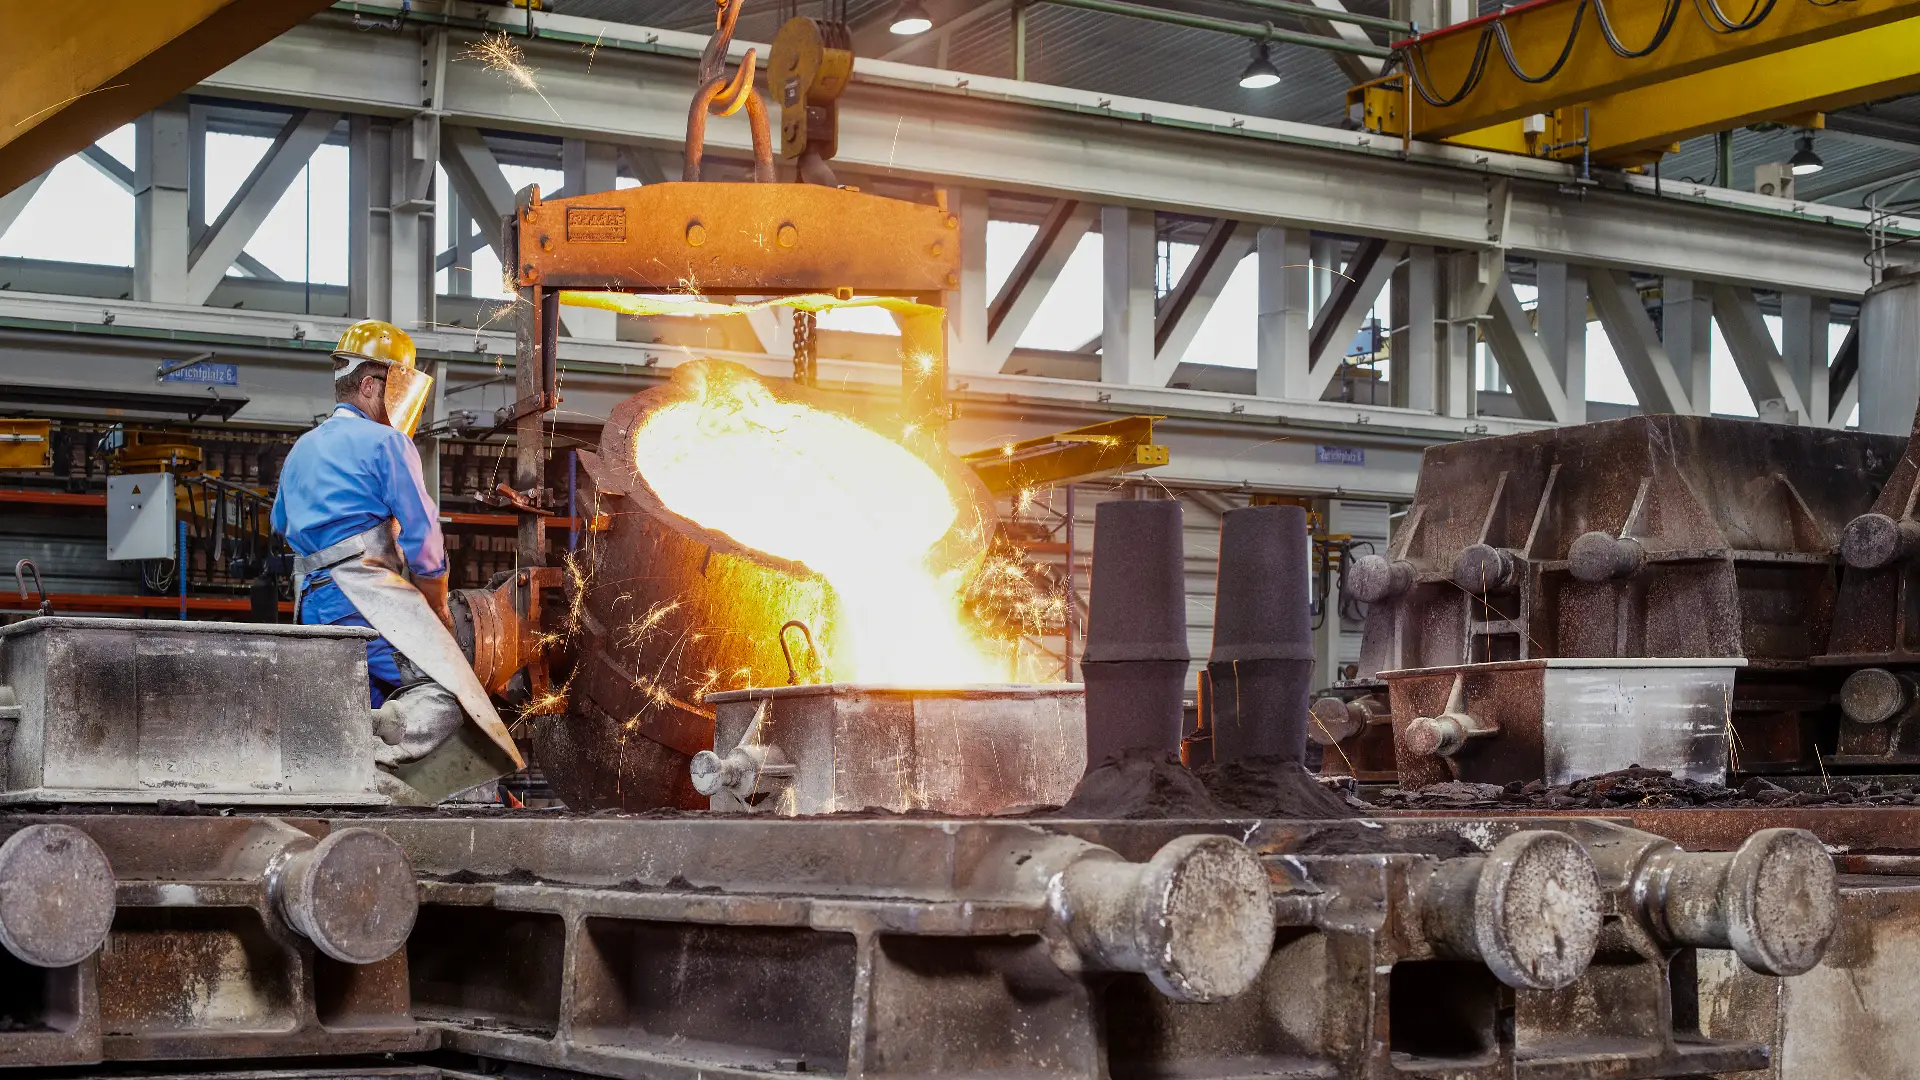
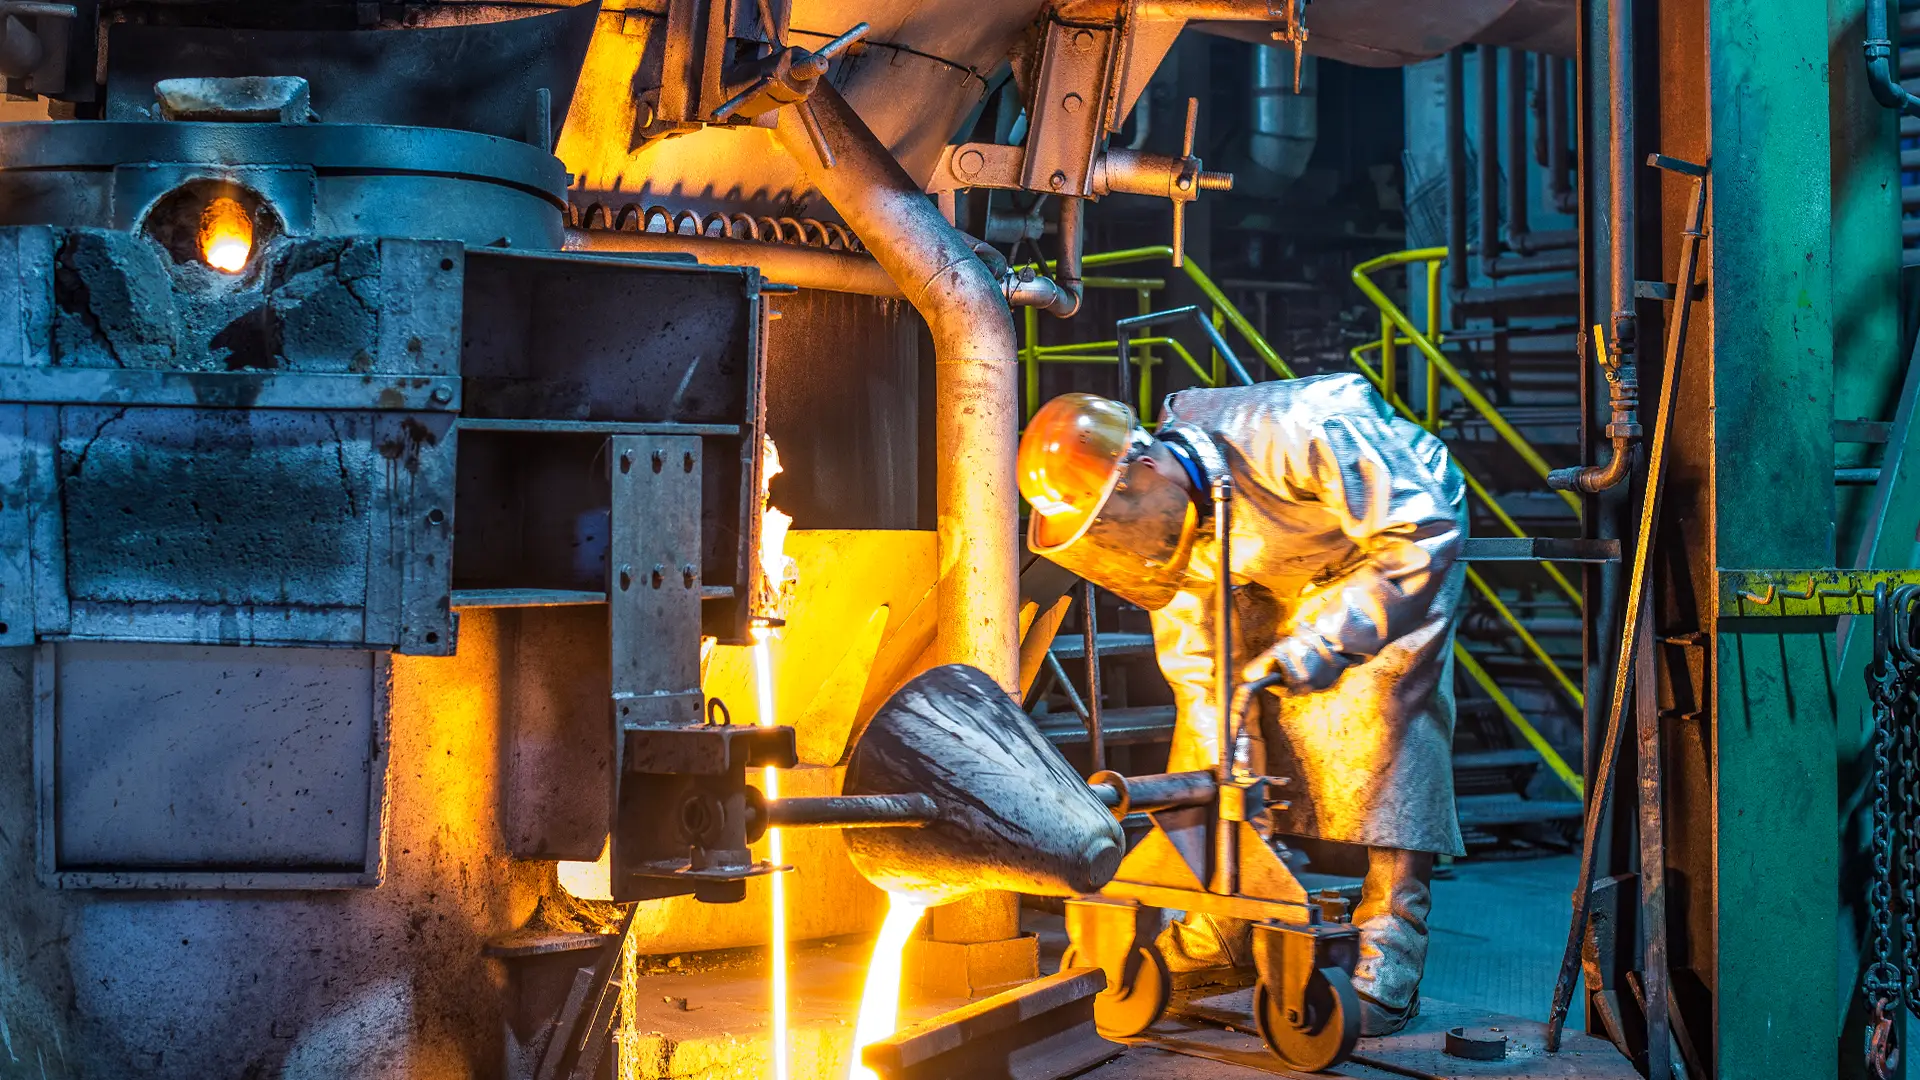
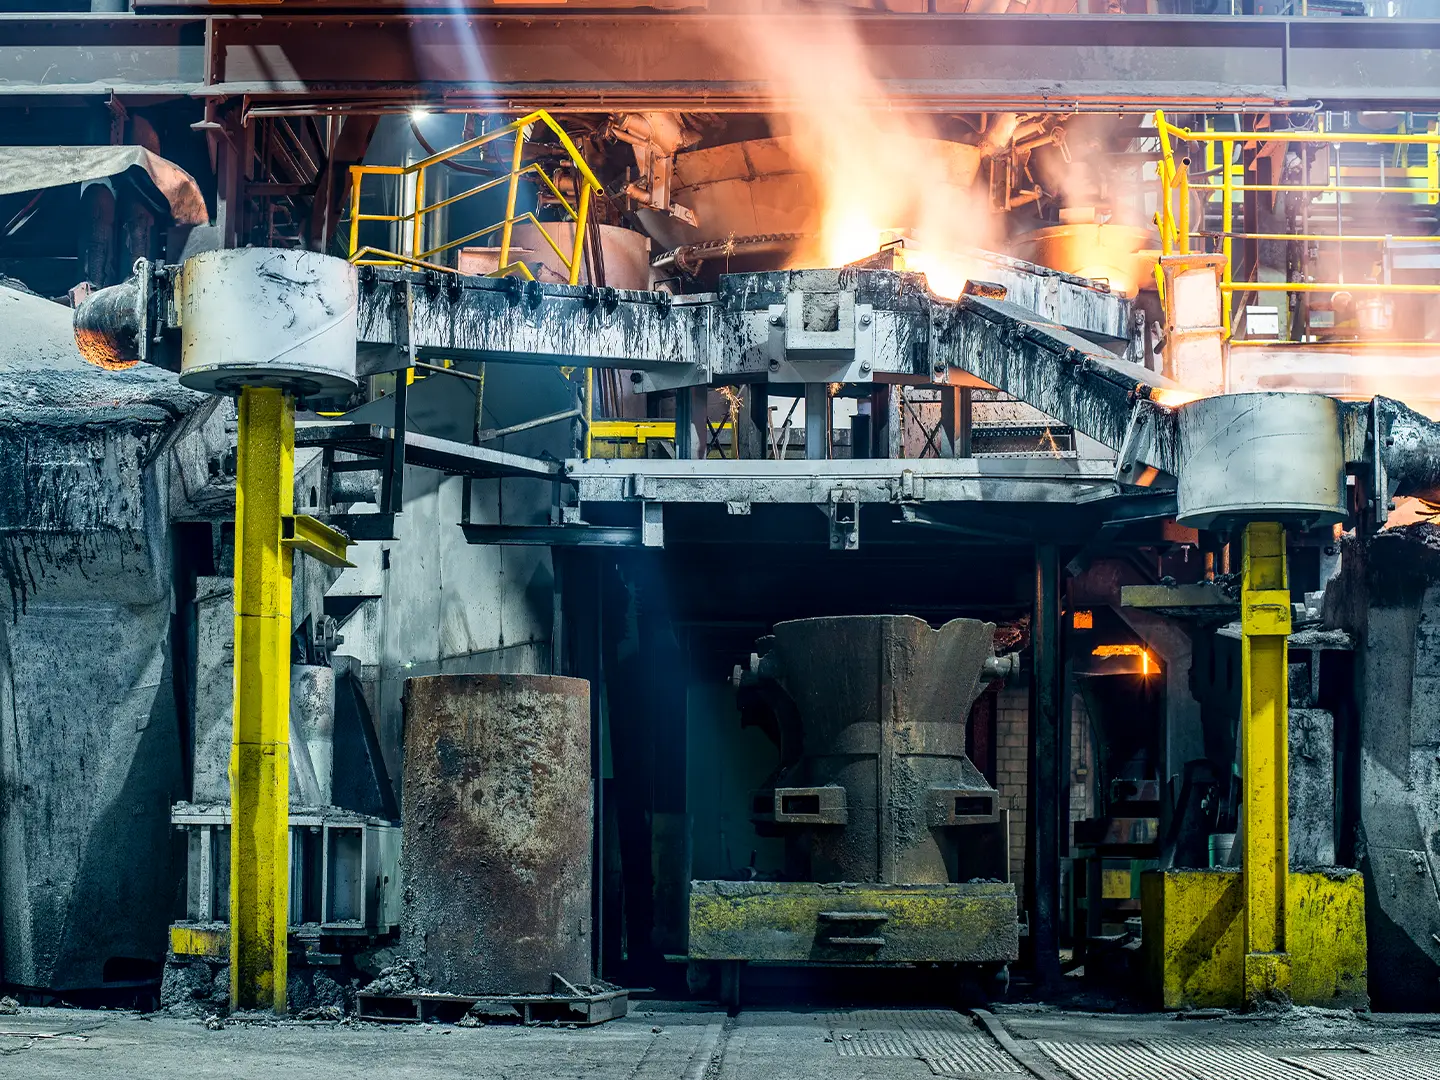
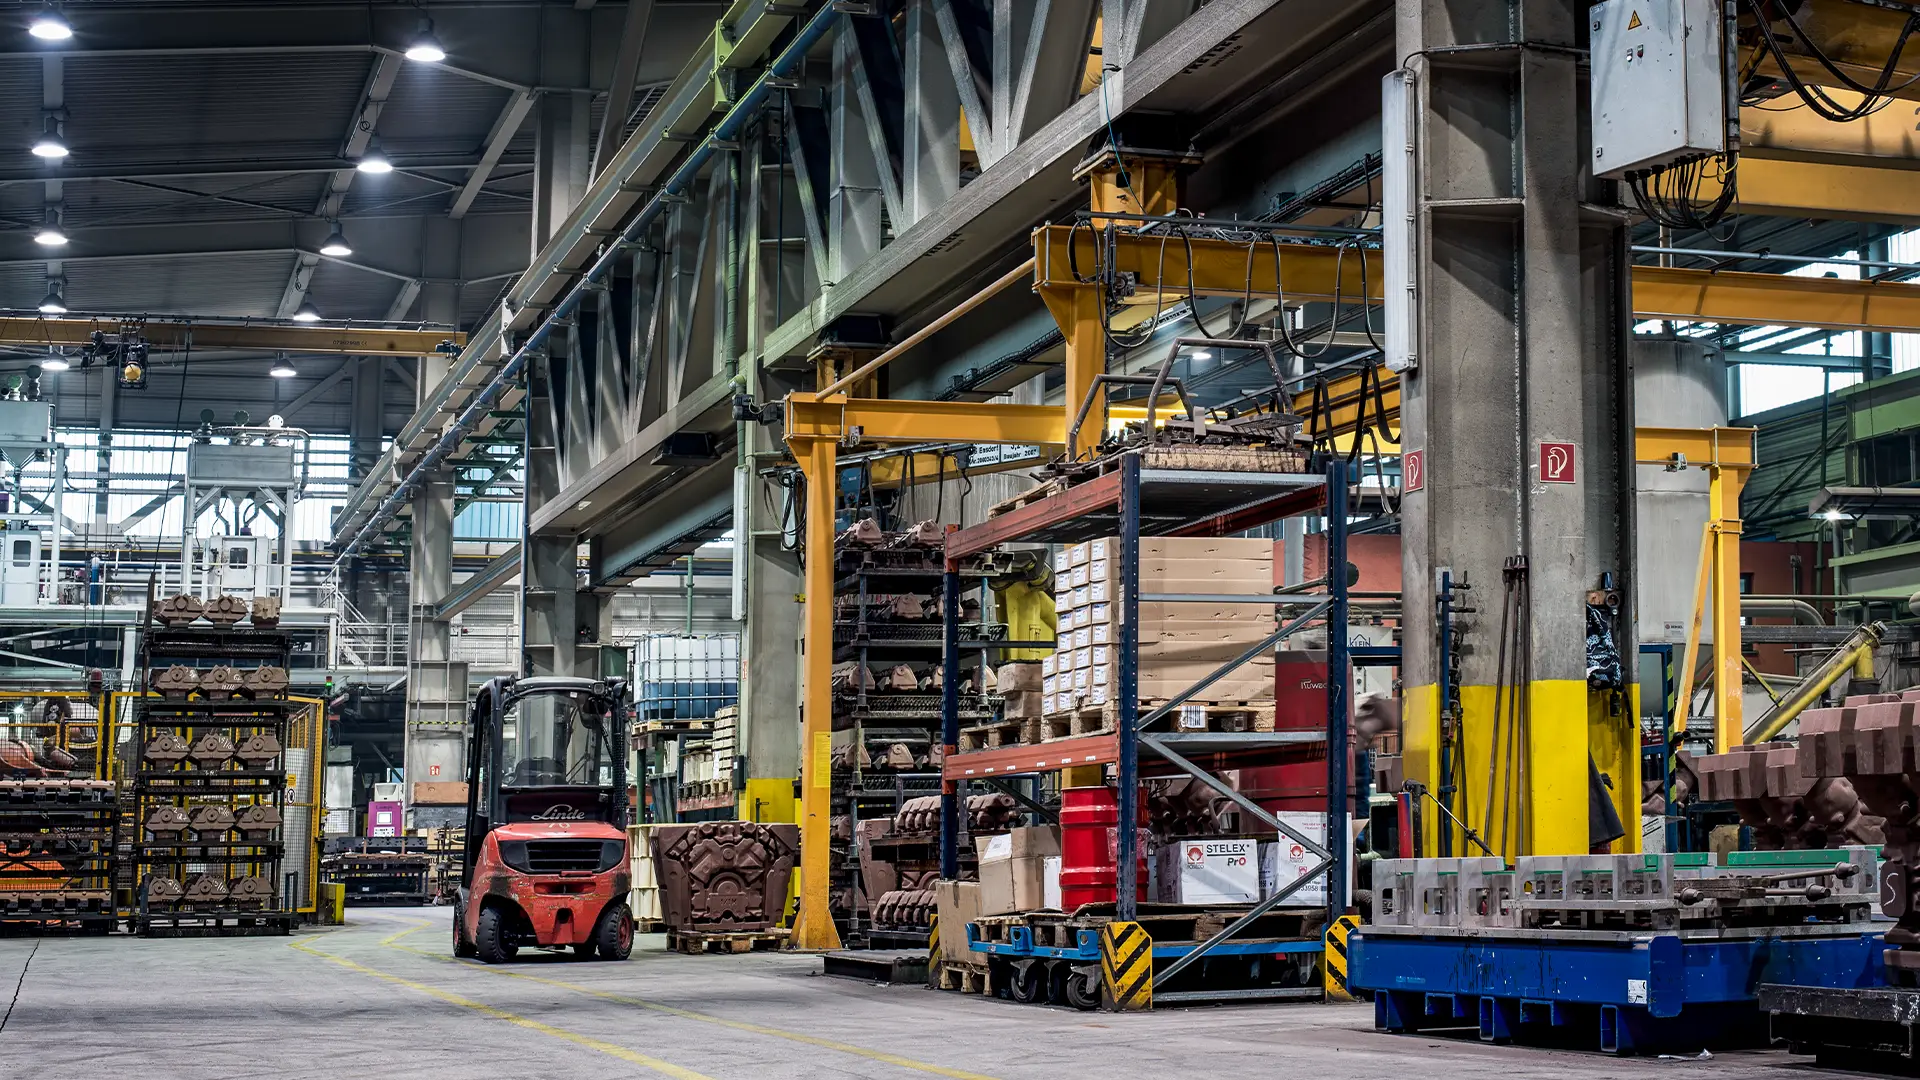
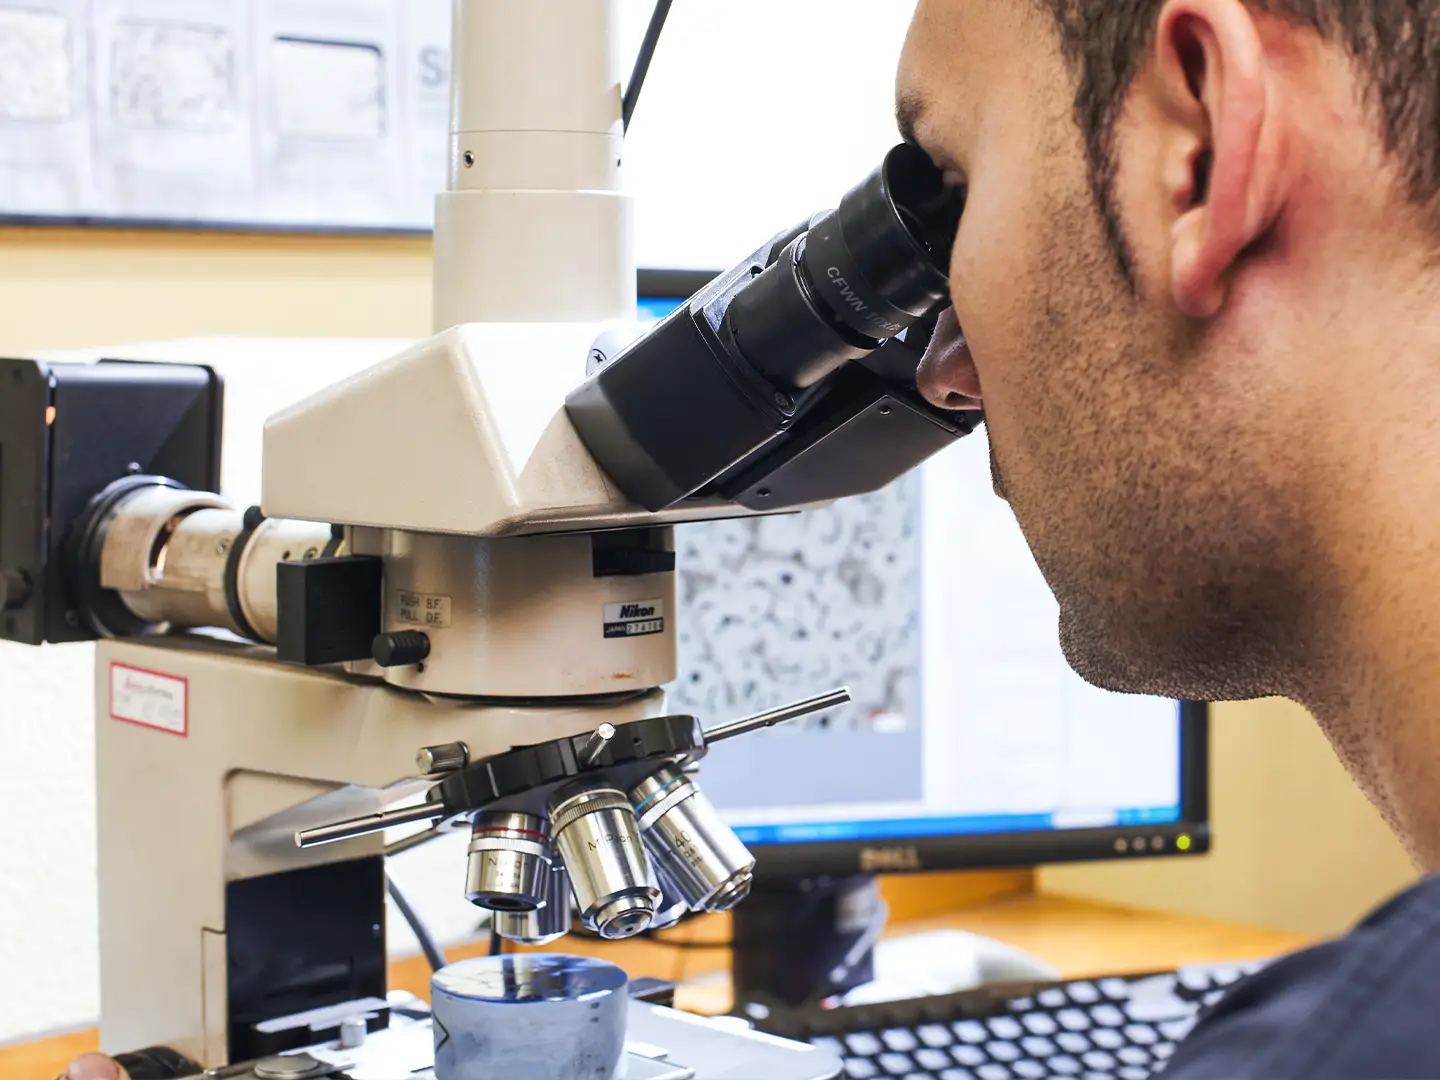
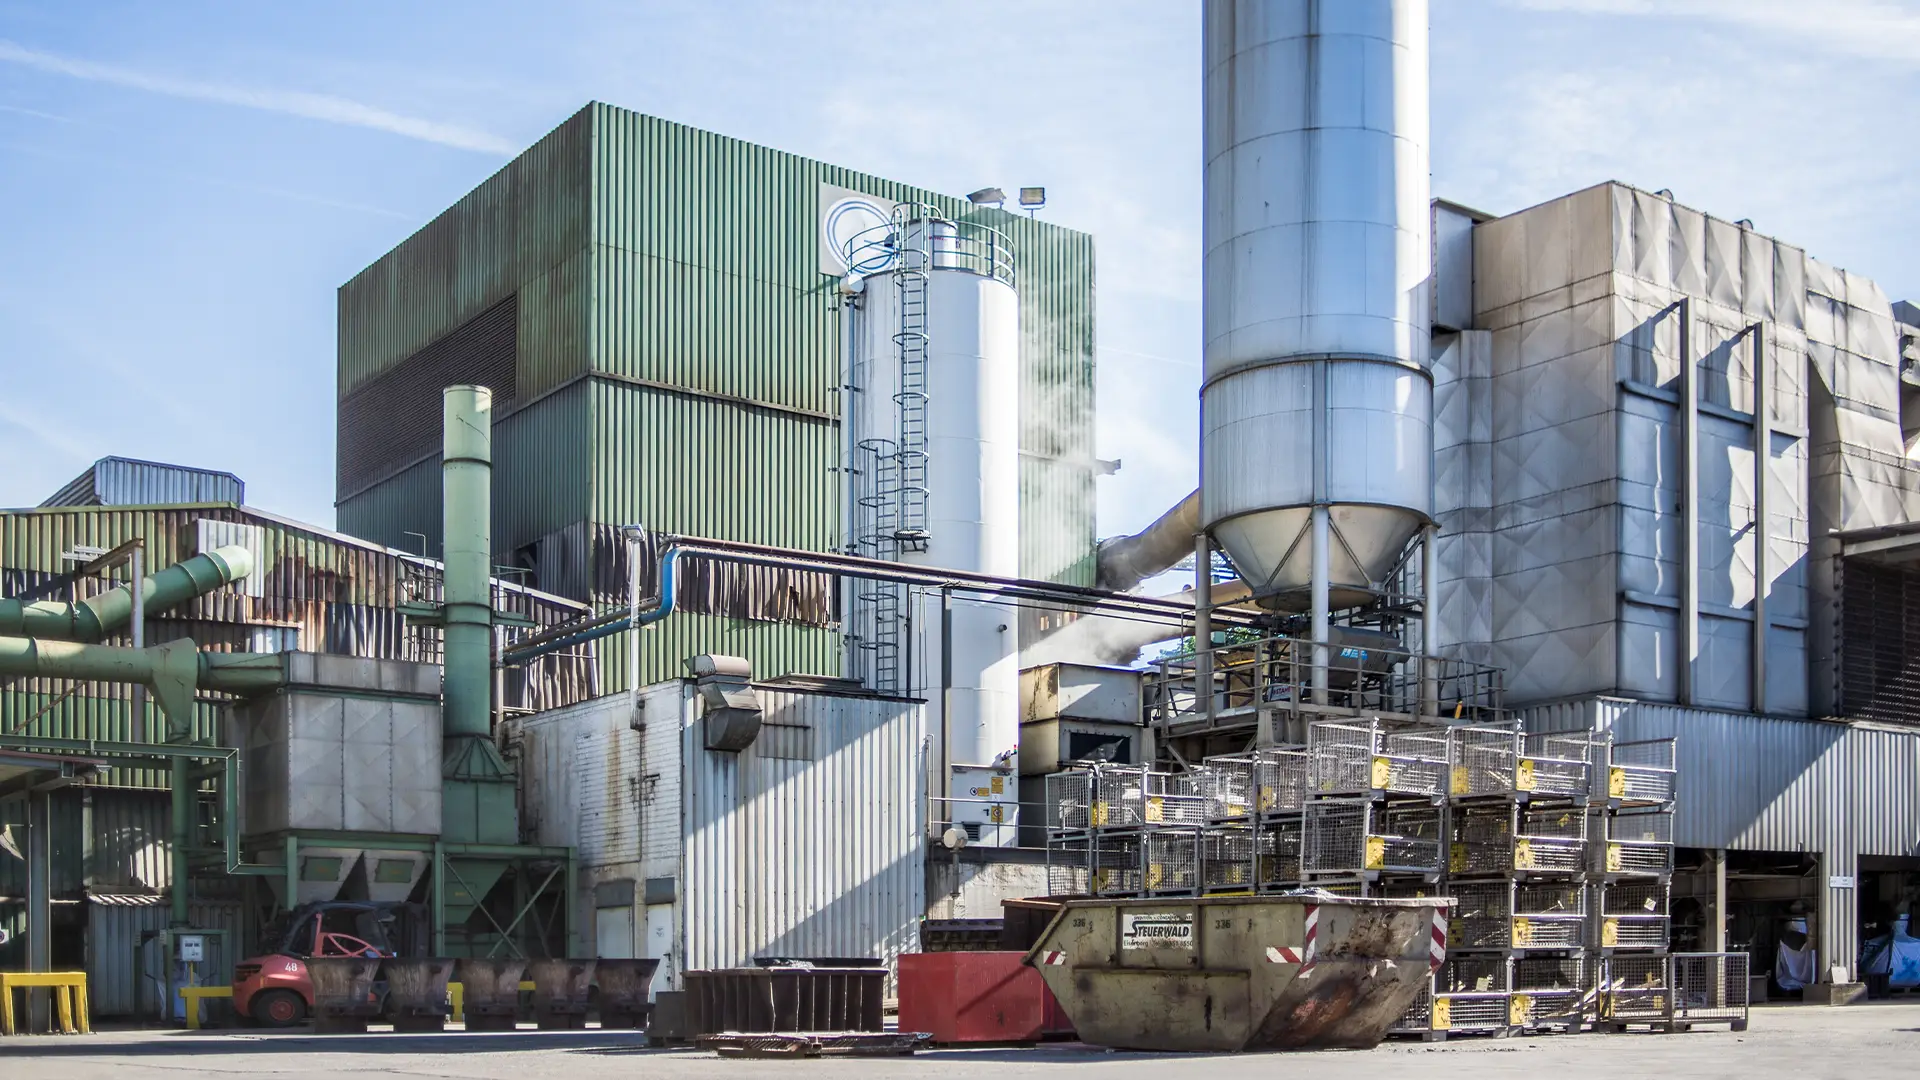
Inside the production
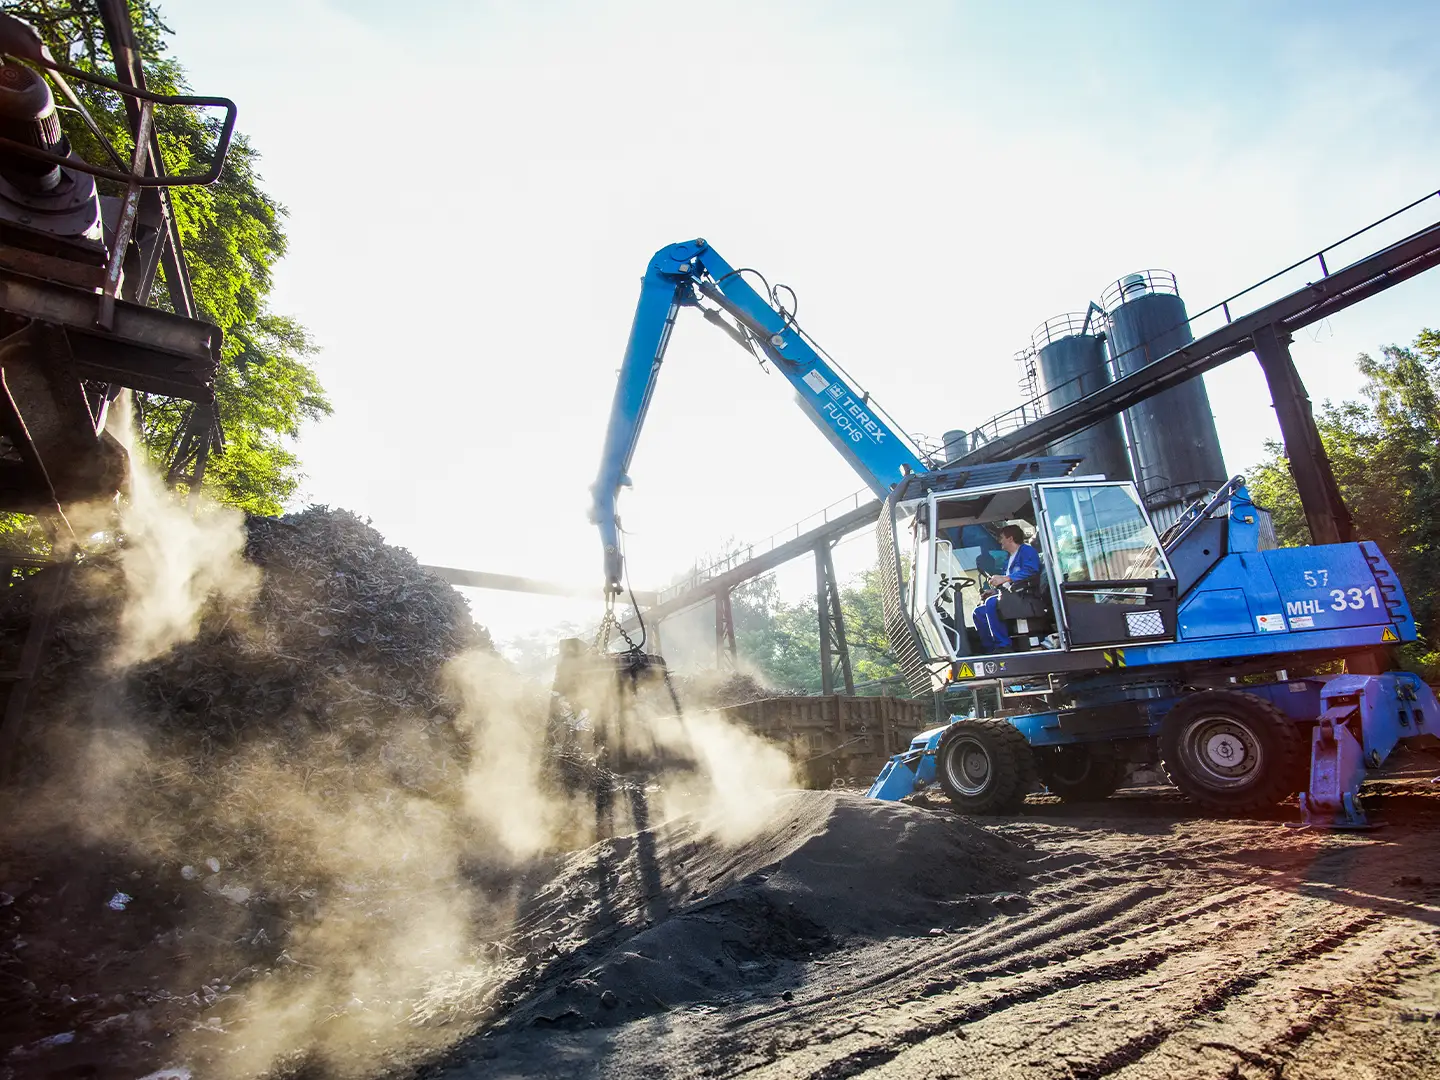
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Hand moulding castingCasting | – | – | up to 5 t part weight | Single parts & small series | EN-GJL-150 to EN-GJL-350, GJV-300 to GJV-450, EN-GJS-400-15-LT to EN-GJS-700-2, EN-GJS-500-15 to EN-GJS-600-10 |
| Machine moulding casting (vertical moulding lines)Casting | – | – | up to 30 kg | medium and large series as well as | EN-GJL-150 to EN-GJL-350, GJV-300 to GJV-450, EN-GJS-400-15-LT to EN-GJS-700-2, EN-GJS-500-15 to EN-GJS-600-10 |
| Machining (cutting)Machining | – | – | – | – | Cast iron (GJL, GJS, GJV) |
| Surface finishing / painting / coatingSurface | – | – | – | – | Cast iron (GJL, GJS, GJV) |
| Assembly / pre-assembly (ready-to-install product solutions)Assembly | – | – | – | – | Cast iron (GJL, GJS, GJV) |
| Recycling (steel scrap, casting scrap, recycled material)Casting | – | – | – | – | Pig iron, Steel scrap, Casting scrap, Recycled material |
| Design & simulation (Siemens NX CAD/CAM/CAE, Magmasoft)Engineering | – | – | – | – | – |
| 3D printing / rapid prototypingAdditive | – | – | – | – | – |
| Quality assurance and metrology (100% inline metrology, CNC tactile metrology, optical)Testing | – | – | – | – | – |
| Casting for passenger/commercial/agricultural vehicles (up to 40 kg, ready-to-install machined andCasting | – | – | up to 40 kg | – | Cast iron |
| Casting for mechanical engineering and decentralised power supply (up to 15 t, ready-to-installCasting | – | – | up to 15 t | – | Cast iron |
8 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| Hot-blast cupola furnace | – | 1 | max. 30 t/h | – | Eisenberg (Palatinate) |
| Line-frequency induction crucible furnace | 5 t | 1 | 5 t | – | Eisenberg (Palatinate) |
| Medium-frequency induction crucible furnace | 8 t | 3 | 8 t | – | Eisenberg (Palatinate) |
| Holding furnace | 60 t | 3 | 60 t | – | Eisenberg (Palatinate) |
| Vertical moulding line (machine moulding casting) | – | 5 | Part weights up to 30 kg | – | Eisenberg (Palatinate) |
| Automated magnesium wire treatment system (wire feeding) | – | 1 | – | – | Eisenberg (Palatinate) |
| Siemens NX CAD/CAM/CAE system | Siemens NX | – | – | – | – |
| Magmasoft simulation system | MAGMA Magmasoft | – | – | – | – |
Additional services
Reference customers
Quality
DiHAG Gienanth strives for zero-defect production and relies on 100% inline metrology, CNC-controlled tactile metrology, optical measuring methods and robot-assisted quality assurance for large castings. The composition of the input material is continuously analysed.
| Evidence | Eisenberg (Palatinate) |
|---|---|
| Certified standards in all processes | |
| 100% inspection of the finest tolerances | |
| Optical measuring methods / sampling | |
| CNC tactile metrology | |
| Robot-assisted QA for large castings |
History
- 1735
Founding of the hammer mill in Eisenberg/Palatinate (today's headquarters); expansion into an ironworks of the industrialist family von Gienanth
- ab 1900
Production of high-quality cast iron components for the automotive industry, including the first engines for Bugatti racing cars
- 1935
First cylinder crankcases for large engines in Eisenberg
- 1964
Start of automated production on vertically parted moulding lines – one of the very first companies to do so