Zinc and aluminium die-cast parts with in-house toolmaking, CNC machining and assembly manufacturing for the automotive industry and other sectors.
Eisenmann Druckguss GmbH
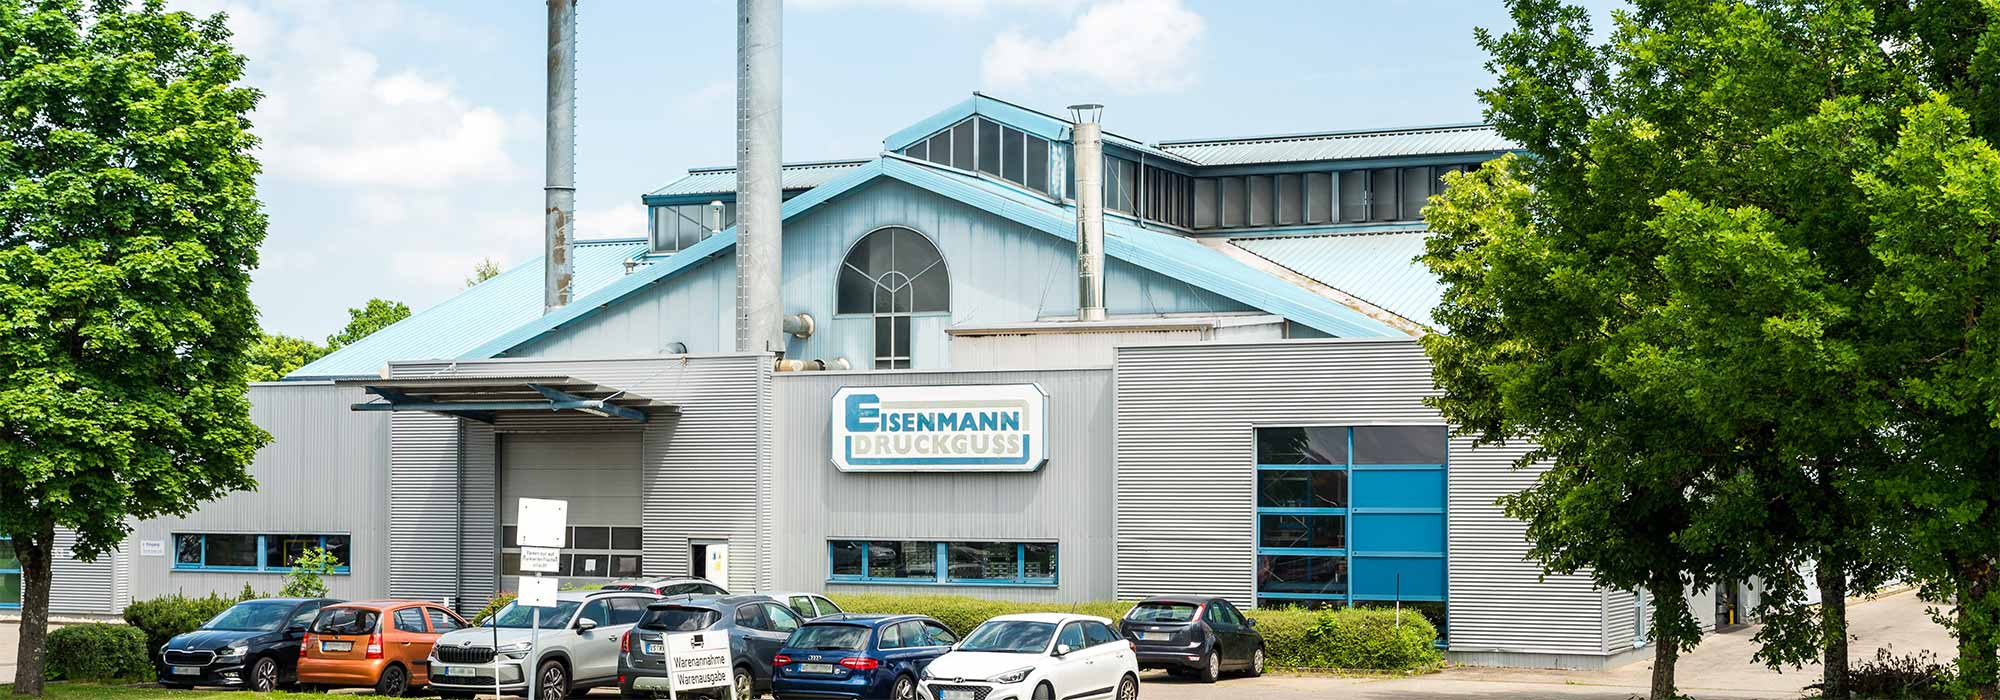
Villingen-Schwenningen (Plant I, II, III)New on Amplifa
About EISENMANN Druckguss
Eisenmann Druckguss GmbH has been manufacturing highly precise components from zinc and aluminium using the die casting process since 1933. The product portfolio comprises zinc die-cast parts from 1 g to 3,500 g on 17 fully automated casting cells (20 t to 200 t clamping force) as well as aluminium die-cast parts from 16 g to 6,000 g on ten cold chamber casting cells with 350 t to 1,050 t clamping force. With its own "cast-to-size" technology (net-shape casting), mechanical post-machining can be dispensed with in many cases. The range of services also includes in-house mould and toolmaking, 4- and 5-axis CNC machining on twelve machining centres, most of them twin-spindle, surface finishing, component and assembly manufacturing with up to 30 individual parts including X-ray and leak testing, as well as development with CAE and Moldflow 3D simulation. Customers come, among others, from the automotive, drive and precision engineering, mechanical engineering, electrical, medical technology and aerospace sectors. Around 170 employees produce more than 80 million parts annually at three plants in Villingen-Schwenningen.
- Site
- Villingen-Schwenningen
- Processes
- Zinc die casting, Aluminium die casting (cold chamber), Net-shape casting / cast-to-size, CNC machining (4- and 5-axis, material removal), 5-axis milling, Surface finishing (zinc nickel, KTL, thick-layer passivation, blue passivation,, Chromating, Powder coating
- Materials
- Zinc alloy ZL0410 / ZL5, Zinc alloy ZL0430 / ZL2, Aluminium alloy 226 D, Aluminium alloy 230 D, Aluminium alloy 231 D, Aluminium alloy 239 D, Aluminium alloy EN AC-43500, Aluminium alloy 226 D (EN AC-Al Si9Cu3(Fe))
- Certificates
- ISO 9001:2015, IATF 16949:2016, DIN EN ISO 14001, DIN EN ISO 50001, ISO 9001, IATF 16949, ISO 14001, ISO 50001
- Founded
- 1933
- Employees
- 170
- Industries
- Automotive, Drive and precision engineering, Fittings and hardware, Mechanical engineering, Building services/Sanitary, Electrical/Electronics
- 01
Development / Prototypes (CAE, Moldflow 3D, 3D printing)
- 02
Mould and toolmaking
- 03
Zinc/aluminium die casting
- 04
CNC machining (4-/5-axis)
- 05
Surface finishing
- 06
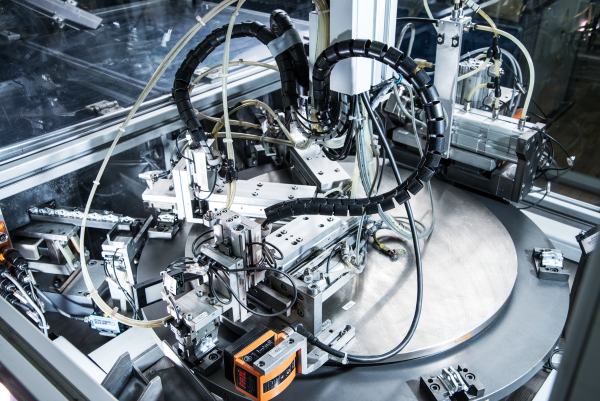
Component/assembly manufacturing including testing
- 07
Project management and delivery
Materials and Processes
Zinc alloy ZL0410 / ZL5
Zinc die casting for parts from 1 g to 3,500 g with high dimensional accuracy and tool life.
Zinc alloy ZL0430 / ZL2
Zinc alloy for precision parts with short casting cycles and high strength.
Aluminium alloy 226 D (EN AC-Al Si9Cu3(Fe))
Aluminium alloy for cold chamber die-cast parts from 16 g to 6,000 g.
Aluminium alloy 230 D (EN AC-Al Si12(Fe))
Aluminium alloy with good castability for complex geometries.
Aluminium alloy 231 D (EN AC-Al Si12Cu1(Fe))
Aluminium alloy for robust die-cast parts.
Aluminium alloy 239 D (EN AC-Al Si10Mg(Fe))
Aluminium alloy with high strength and corrosion resistance.
Aluminium alloy EN AC-Al Si10MnMg(Fe)
Aluminium alloy for high-strength, thin-walled structural parts.
Net-shape casting technology
Casting process for maximum casting accuracy that often makes mechanical post-machining unnecessary.
High-Speed Cutting (toolmaking)
Technology for roughing and finishing the finest contours in toolmaking.
4-/5-axis CNC machining
Machining in the thousandths-of-a-millimetre range on predominantly twin-spindle machining centres.
Surface finishing
Processes such as zinc nickel, KTL, chrome plating, gold plating and powder coating for corrosion protection up to 720 h salt spray test.
Rapid Prototyping
Plastic laser sintered parts and STL parts for prototypes and samples.
Locations
Plant I – Villingen-Schwenningen
DEZinc die casting and administration
- Part weight / size
- 1 g – 3,500 g
- Lot size
- Series production
- Materials
- ZnAl4Cu1, ZnAl4Cu3
- 17 fully automated die casting cells (20 t – 200 t clamping force)
- Transfer and special-purpose machines
Plant II – Villingen-Schwenningen
DEAluminium die casting
- Part weight / size
- 16 g – 6,000 g
- Lot size
- Series production
- Materials
- EN AC-46000, EN AC-44300, EN AC-47000, EN AC-43400, EN AC-43500
- 10 fully automated cold chamber casting cells (350 t – 1,050 t clamping force)
Plant III – Villingen-Schwenningen
DECNC technology
- Lot size
- Series production
- Materials
- Zinc and aluminium die-cast parts
- 12 4-/5-axis machining centres (predominantly twin-spindle)
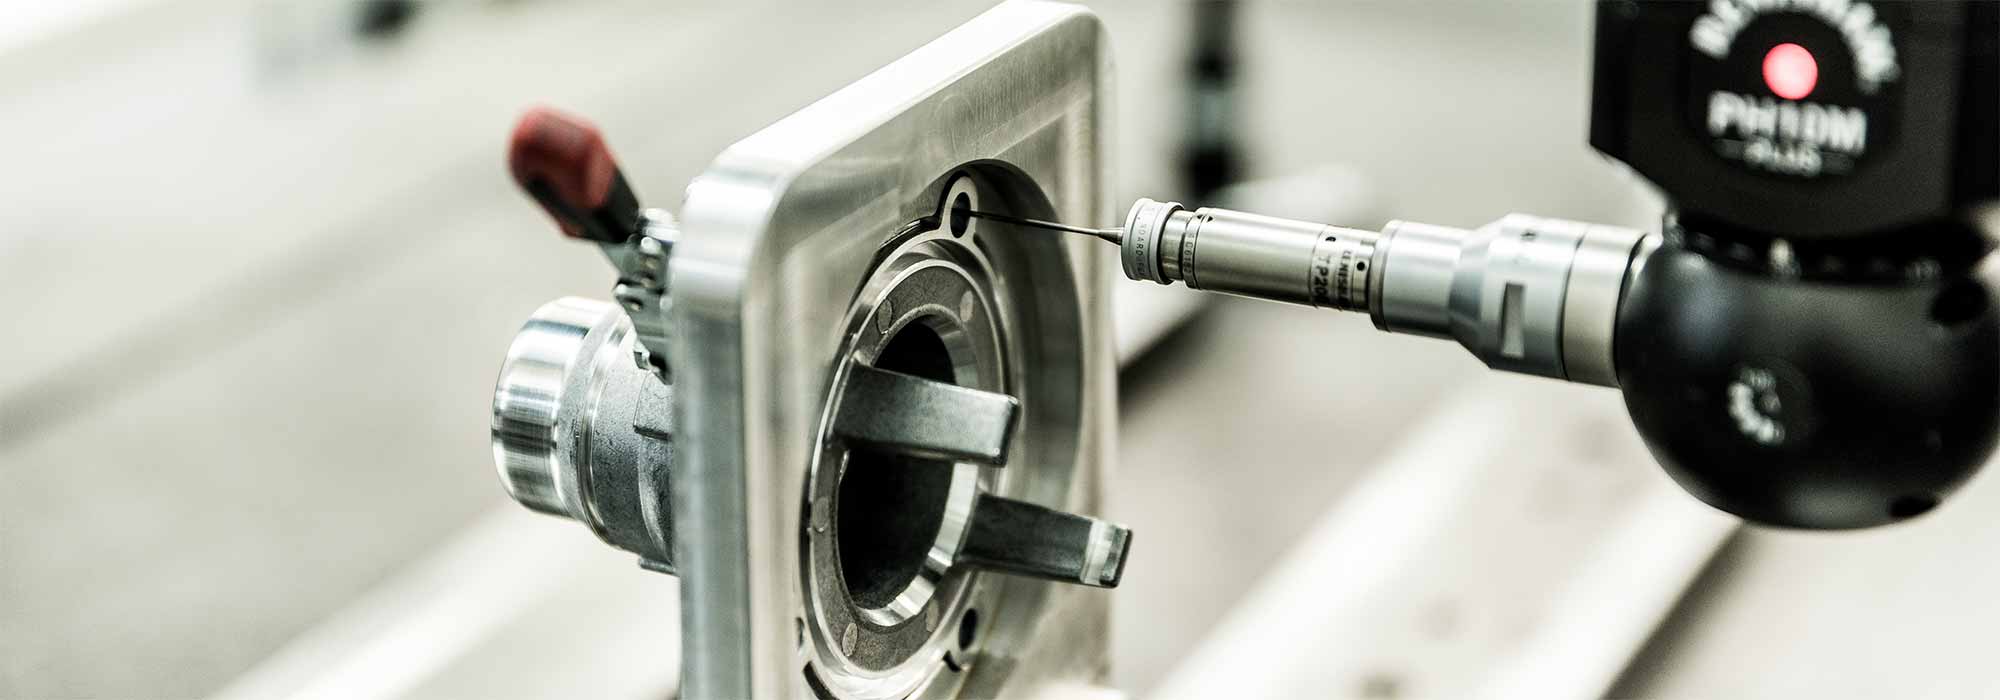
- 3D measuring machines
Components
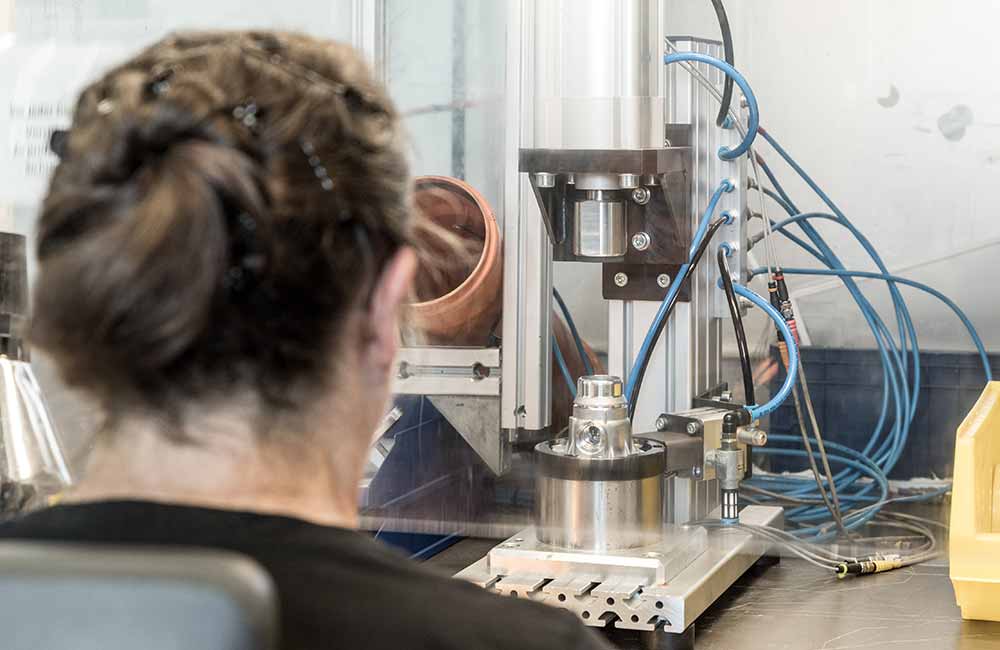
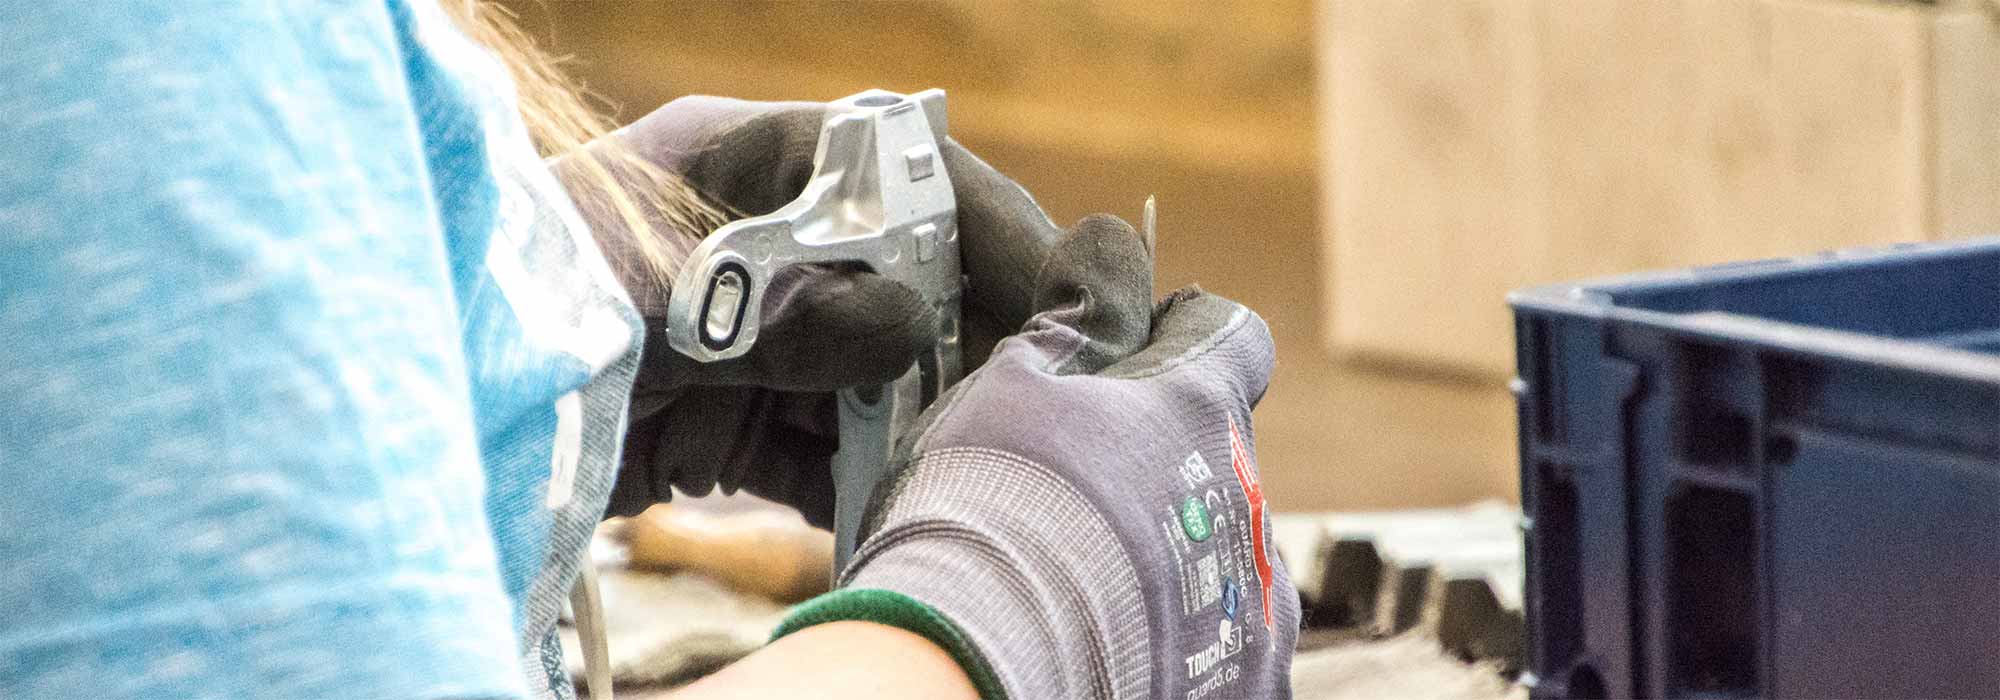
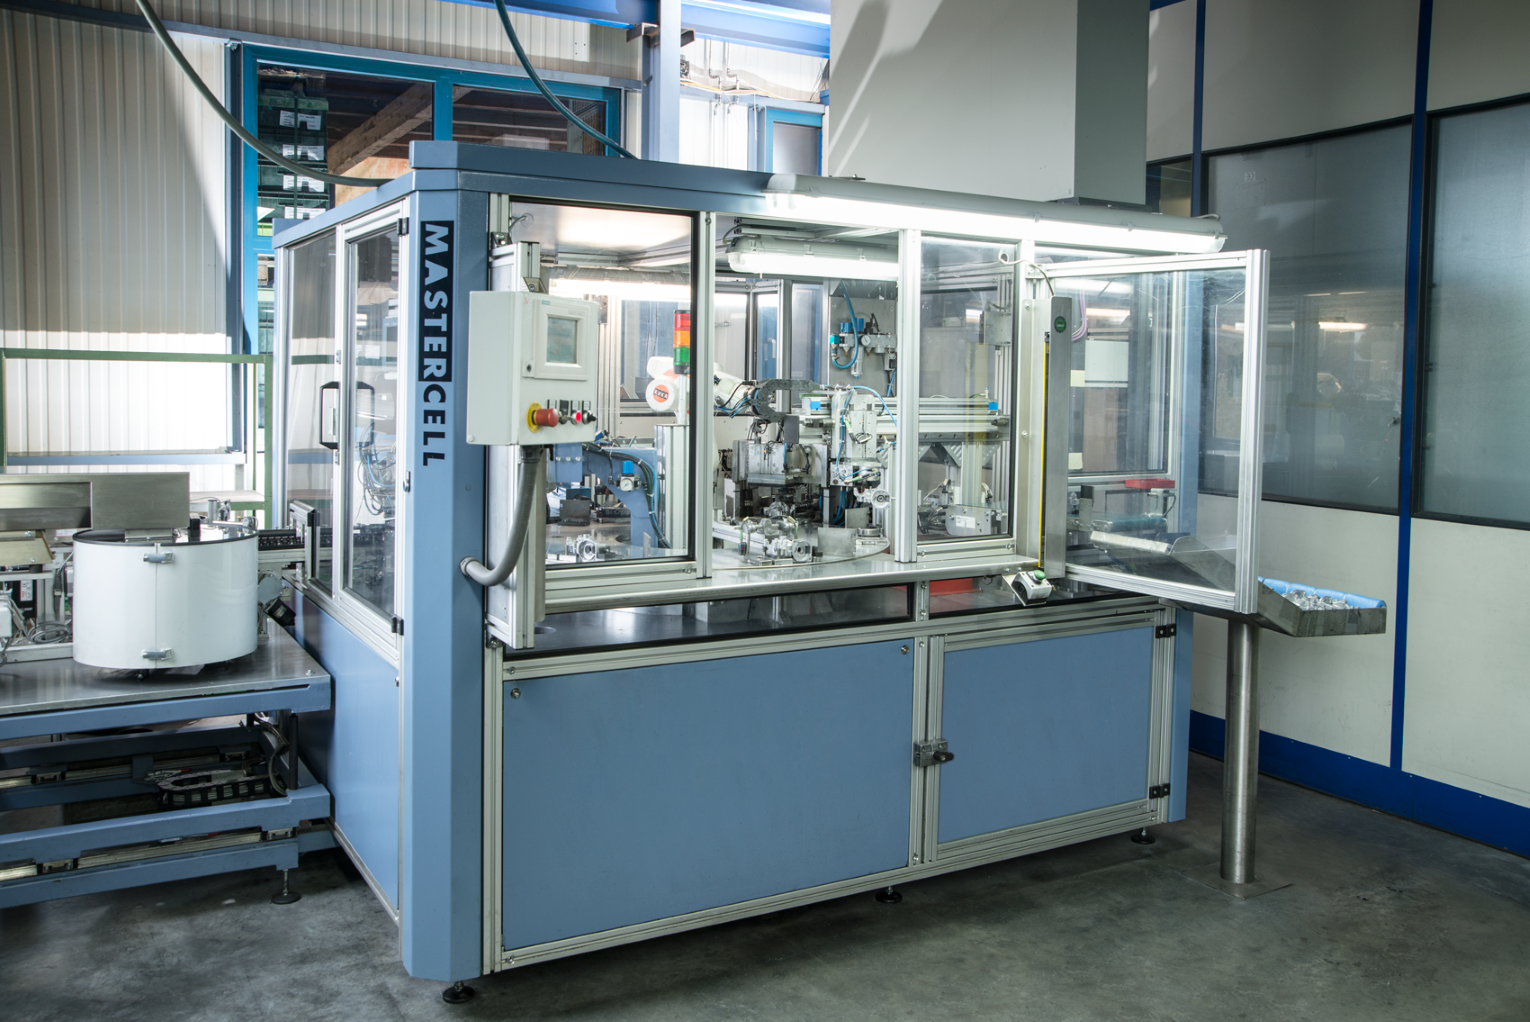
Inside the production
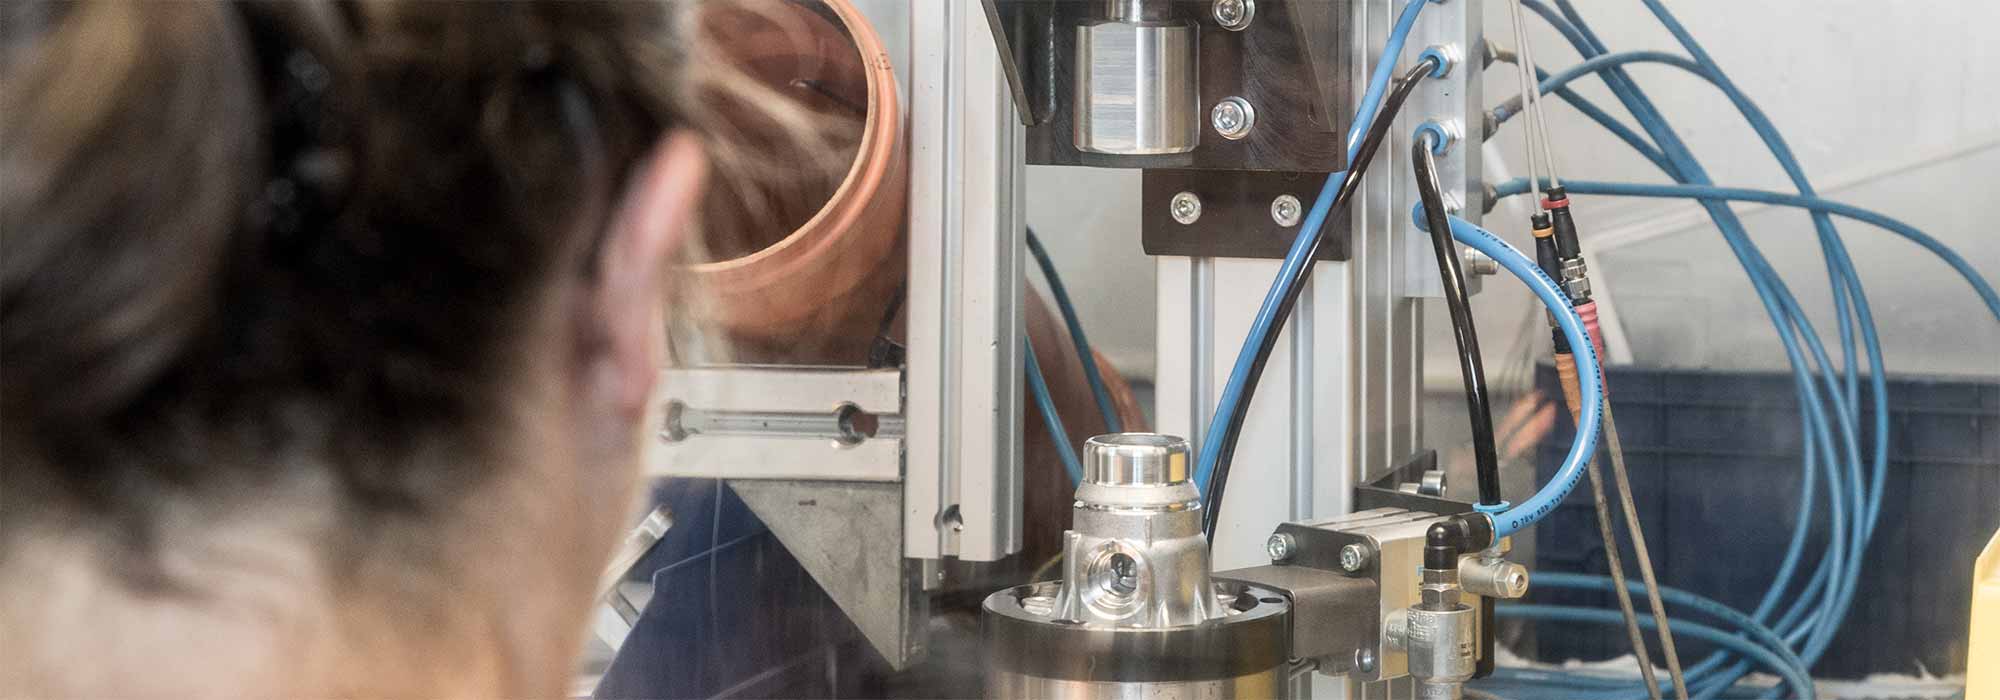

Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Zinc die castingCasting | – | – | 1g – 3,500g | – | ZnAl4Cu1, ZnAl4Cu3 |
| Aluminium die casting (cold chamber)Casting | – | – | 16g – 6,000g | – | EN AC-Al Si9Cu3(Fe), EN AC-Al Si12(Fe), EN AC-Al Si12Cu1(Fe), EN AC-Al Si10Mg(Fe), EN AC-Al Si10MnMg(Fe) |
| Net-shape casting / cast-to-sizeCasting | – | – | – | – | Aluminium |
| CNC machining (4- and 5-axis, material removal)Machining | Thousandths-of-a-millimetre range | – | – | – | Zinc die-cast parts, Aluminium die-cast parts |
| 5-axis millingMachining | – | – | – | – | – |
| Surface finishing (zinc nickel, KTL, thick-layer passivation, blue passivation,Surface | – | – | – | – | Aluminium die-cast parts, Zinc die-cast parts |
| ChromatingSurface | – | – | – | – | Zinc |
| Powder coatingSurface | – | – | – | – | Zinc, Aluminium |
| Assembly manufacturing / assembly (incl. X-ray and leak testing, joining and bonding technology)Assembly | – | – | – | – | – |
| Mould and toolmaking (design, simulation, gate calculation, mould manufacturing, sampling,Engineering | – | – | – | – | – |
| Development / Prototypes (CAE, Moldflow 3D simulation, STL parts, 3D printing, sandEngineering | – | – | – | – | – |
| 3D printing / Rapid Prototyping (plastic laser sintered parts)Additive | – | – | – | – | Plastic |
| Testing (3D measuring machines, X-ray inspection, leak testing)Testing | – | – | – | – | – |
5 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| Cold chamber die casting machine (fully automated casting cell) | – | 10 | Clamping force 350t to 1,050t | – | Plant II Villingen-Schwenningen |
| Die casting machine (fully automated casting cell) | – | 17 | Clamping force 20t to 200t | – | Plant I Villingen-Schwenningen |
| 4-/5-axis machining centre (predominantly twin-spindle) | – | 12 | – | – | Plant III Villingen-Schwenningen |
| 3D measuring machine | – | – | – | – | Villingen-Schwenningen |
| Transfer and special-purpose machines | – | – | – | – | Villingen-Schwenningen |
Additional services
Reference customers
Quality
The quality management system is based on ISO 9001:2015 and IATF 16949 and is documented in a QM manual. Testing is carried out, among other things, with 3D measuring machines, X-ray inspection and leak testing.
| Evidence | Villingen-Schwenningen |
|---|---|
| ISO 9001 | |
| IATF 16949 | |
| ISO 14001 | |
| ISO 50001 |
History
- 1933
Founded by Fritz Eisenmann in a cellar vault with a specially modified casting machine that was already capable of producing with hundredths-of-a-millimetre accuracy.