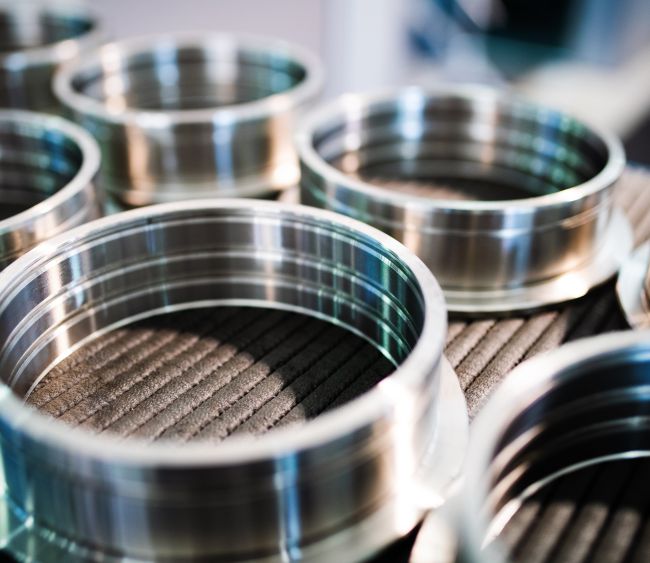
Contract manufacturing of machine components and assemblies in steel, stainless steel and aluminium – from cutting to assembly.
Ferrotechnik Maschinenbau GmbH
8401 Kalsdorf bei Graz, Austria · 40313 Sveti Martin na Muri (Vrhovljan), CroatiaNew on Amplifa
Contract manufacturing with deep vertical integration
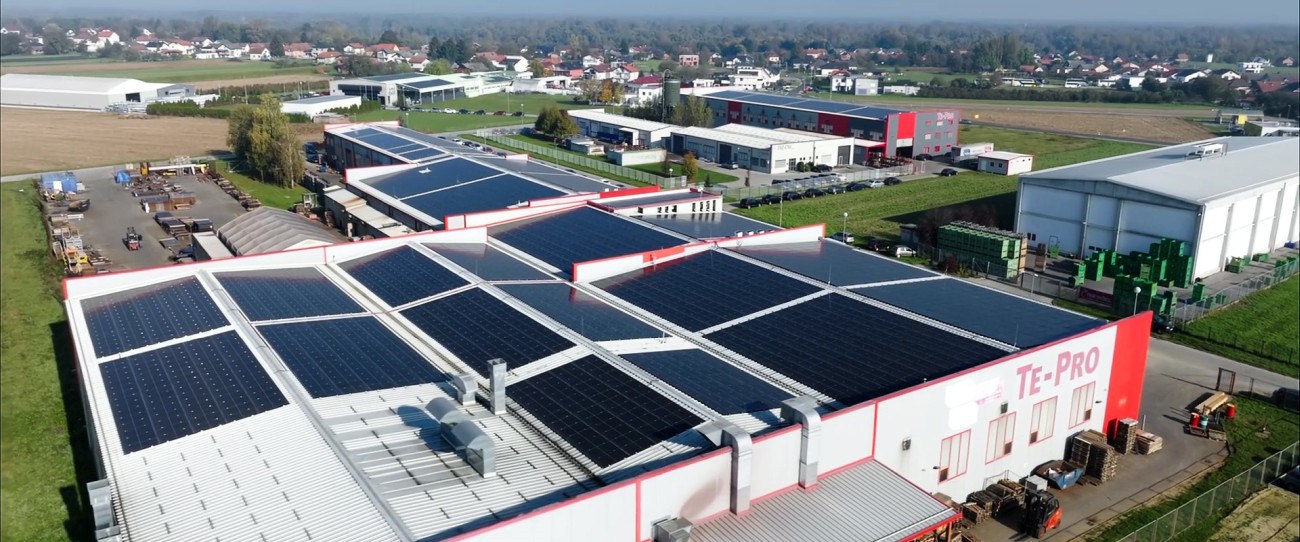
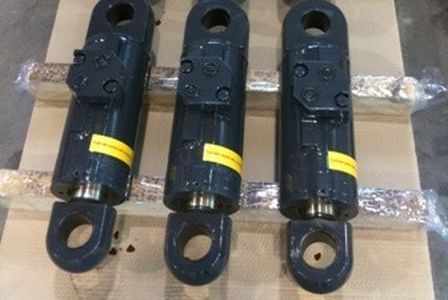
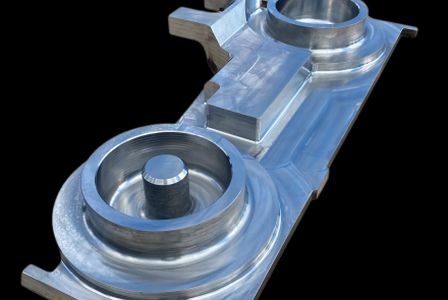
Ferrotechnik Maschinenbau GmbH is a contract manufacturing company based in Styria, headquartered in Kalsdorf near Graz, with a second production site in Croatia (Te-Pro d.o.o., Sveti Martin na Muri). The company manufactures machine components up to complete assemblies in carbon steel, stainless steel and aluminium. Its value chain includes cutting, CNC milling and turning (travel up to 6 m, workpiece weight up to 10 t), bending with CNC press brakes (650 t press force, 4 m bending length), welding with three welding robots, bonding, grinding/polishing, hardening, sandblasting and surface coating in two paint and drying booths, as well as complete assembly. A key focus is the manufacture and testing of hydraulic cylinders on the in-house hydraulic and valve adjustment test bench. Main customer industries are rail transport, power generation and mining machinery; over 600,000 parts and around 4,000 different products are delivered annually.
- Site
- Kalsdorf bei Graz
- Processes
- Turning, Milling, Forming (bending with CNC-controlled press brakes), Welding, MAG welding with flux-cored wire (135), TIG welding (141), Bonding (2K adhesives, 1K moisture-curing, solvent- or water-based systems), Painting / surface coating (including sandblasting and heat treatment)
- Materials
- Carbon steel, Stainless steel, Aluminium, Sheet steel (also several centimetres thick), Structural steel and aluminium materials to EN 1090-2, material groups 1.2, 1.4, 2.1, 2.2, 3.1, MAG welding with flux-cored wire, TIG welding, Bonding
- Certificates
- DIN EN ISO 9001:2015, EN 15085-2 CL1 (welding of rail vehicles), EN 15085-2 CL4, EN ISO 3834-2:2021, EN 1090-2 EXC3, EN 17460 A3 (bonding of rail vehicles), DIN EN ISO 14001:2015, DIN 2303 Q2 BK1 (defence technology), ISO 9001, ISO 14001, EN 15085-2 CL1, EN ISO 3834-2, EN 17460 A3 (bonding), DIN 2303 Q2 BK1
- Founded
- 1936 (as
- Employees
- 250
- Industries
- Rail transport, Power generation, Mining machinery, Special machinery, Defence technology, Construction machinery/attachments
Materials and processes
Carbon steel
Main material for welded assemblies, sheet metal processing and heat-treated components.
Stainless steel
Machining and welding of corrosion-resistant components.
Aluminium
Lightweight components with CNC machining and welding.
MAG welding with flux-cored wire
Certified to EN 1090-2 for structural steel and aluminium materials of material groups 1.2, 1.4, 2.1, 2.2, 3.1 according to CEN ISO/TR 15608.
TIG welding
Precision fusion welding according to EN ISO 3834-2.
Bonding
Adhesive bonds according to EN 17460 (safety class A3) for rail vehicles, including 2K and moisture-reactive 1K adhesives.
Heat treatment / hardening
In-house hardening of carbon steel components.
Production sites
Kalsdorf bei Graz
ATHeadquarters and production
- Part weight / size
- up to 10 t, travel up to 6 m
- Lot size
- Single parts to series production
- Materials
- Carbon steel, stainless steel, aluminium
- More than 50 CNC turning and milling machines
- 3 welding robots
- CNC press brake (650 t, 4 m bending length)
- 2 paint and drying booths
- Hydraulic and valve adjustment test bench
- Laser tracker
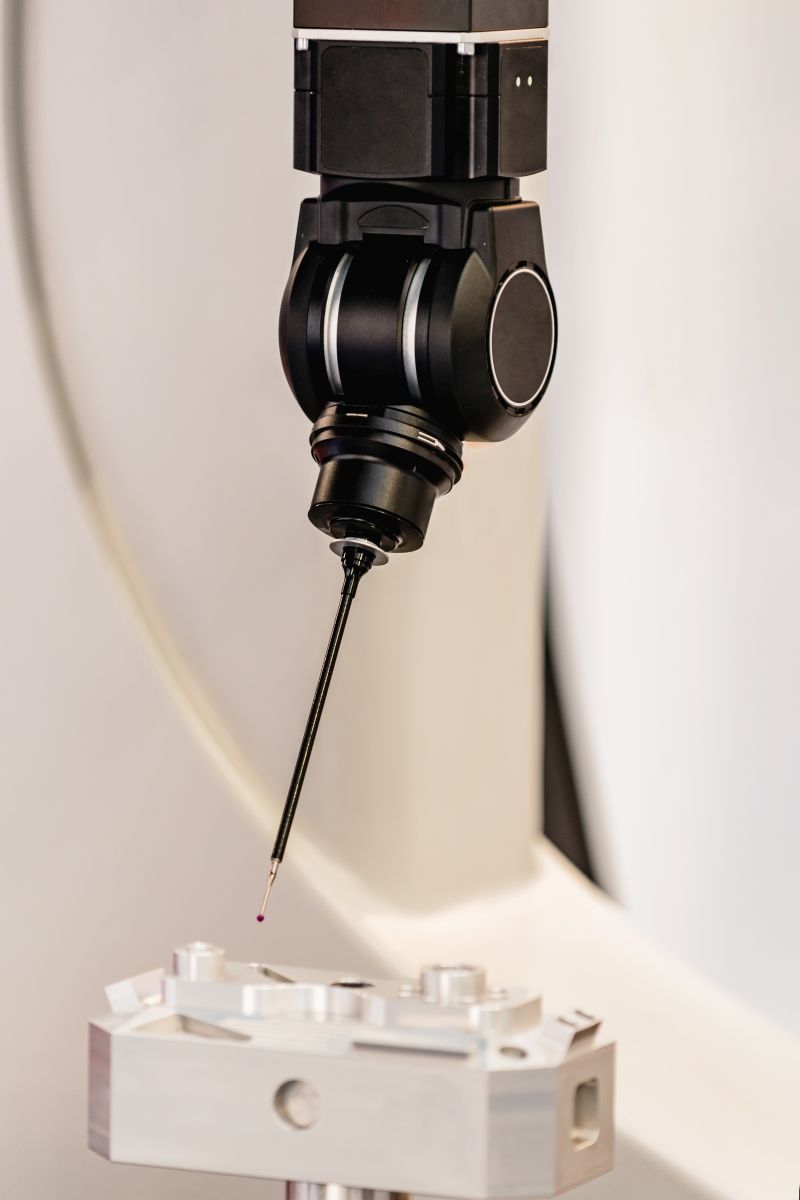
- 3D coordinate measuring machine
Sveti Martin na Muri (Te-Pro d.o.o.)
HRProduction site (subsidiary since 2005)
- Materials
- Structural steel and aluminium materials (MG 1.2, 1.4, 2.1, 2.2, 3.1)
- MAG and TIG welding system (certified to EN 1090-2 EXC3)
Components and products
Inside the production
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| TurningMachining | – | Travel up to 6 metres | up to 10 tonnes | – | Carbon steel, Stainless steel, Aluminium |
| MillingMachining | – | Travel up to 6 metres | up to 10 tonnes | – | Carbon steel, Stainless steel, Aluminium |
| Forming (bending with CNC-controlled press brakes)Forming | – | Bending length up to 4 metres | – | – | Sheet steel (also several centimetres thick) |
| WeldingJoining | – | – | – | – | Carbon steel, Stainless steel, Aluminium |
| MAG welding with flux-cored wire (135)Joining | – | – | – | – | Material groups 1.2, 1.4, 2.1, 2.2, 3.1 according to CEN |
| TIG welding (141)Joining | – | – | – | – | Material groups 1.2, 1.4, 2.1, 2.2, 3.1 according to CEN |
| Bonding (2K adhesives, 1K moisture-curing, solvent- or water-based systems)Joining | – | – | – | – | Load transfer by means of high-modulus adhesives |
| Painting / surface coating (including sandblasting and heat treatment)Surface | – | – | – | – | – |
| HardeningHeat treatment | – | – | – | – | Carbon steel |
| Grinding/polishingSurface | – | – | – | – | – |
| Cutting (sheet metal processing)Forming | – | – | – | – | Steel |
| Manufacture of hydraulic cylinders (including testing on the hydraulic and valve adjustment testAssembly | – | – | – | – | – |
| Complete assembly / pre-assembly of complete systemsAssembly | – | – | – | – | – |
| Quality inspection / metrology (laser tracker, 3D coordinate measuring machines)Inspection | smallest tolerances | – | – | – | – |
7 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| CNC-controlled machines (turning and milling machines) | – | over 50 | Travel up to 6 metres | – | Kalsdorf, Austria / Croatia |
| CNC-controlled press brake | – | – | Bending length up to 4 metres, press force 650 tonnes | – | – |
| Welding robots | – | 3 | – | – | – |
| Paint and drying booth | – | 2 | – | – | Kalsdorf |
| Laser tracker | – | – | – | – | – |
| 3D coordinate measuring machine | – | – | – | – | – |
| Hydraulic and valve adjustment test bench | – | – | – | – | – |
Additional services
Reference customers
Certifications and metrology
Quality assurance is carried out using laser trackers and 3D coordinate measuring machines that precisely capture the smallest tolerances. The company is certified, among others, to DIN EN ISO 9001:2015, EN 15085-2 CL1 and EN ISO 3834-2:2021.
| Evidence | Kalsdorf bei Graz | Sveti Martin na Muri (Te-Pro) |
|---|---|---|
| ISO 9001 | ||
| ISO 14001 | ||
| EN 15085-2 CL1 | ||
| EN ISO 3834-2 | ||
| EN 1090-2 EXC3 | ||
| EN 17460 A3 (bonding) | ||
| DIN 2303 Q2 BK1 |
History
- 1936
Founded as Karl Broda KG in Vienna and Graz: forging and steel hardening shop, regeneration, repair and new manufacture of track and undercarriage parts.
- 1977
The Graz plant becomes independent under Ing. Gottfried Michael Vieltorf as “Ferrotechnik mech. Werkstätte und Härterei GmbH”; design and manufacture of attachments for construction machines as well as contract manufacturing.
- 1998
Certification to DIN ISO 9001.
- 2005
Foundation of the subsidiary Te-Pro d.o.o. in Croatia as a second production site.
- 2011
Construction of a new company headquarters in Kalsdorf near Graz with 2,500 m² of production and storage space.
- 2012
Certification to EN 15085-2 CL1 (welding of rail vehicles and rail vehicle parts).
- 2013
Foundation of the subsidiary Ferromod GmbH for the development and manufacture of concrete block moulds for the building materials industry.
- 2023
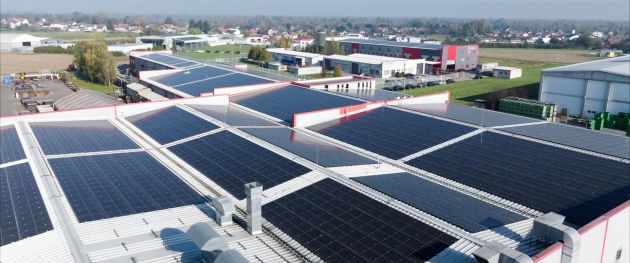
Commissioning of a photovoltaic system (7,000 m², 720 kW, approx. 500 t CO₂ savings per year); transfer of 49% of the company shares to Ing. Thomas Vieltorf.