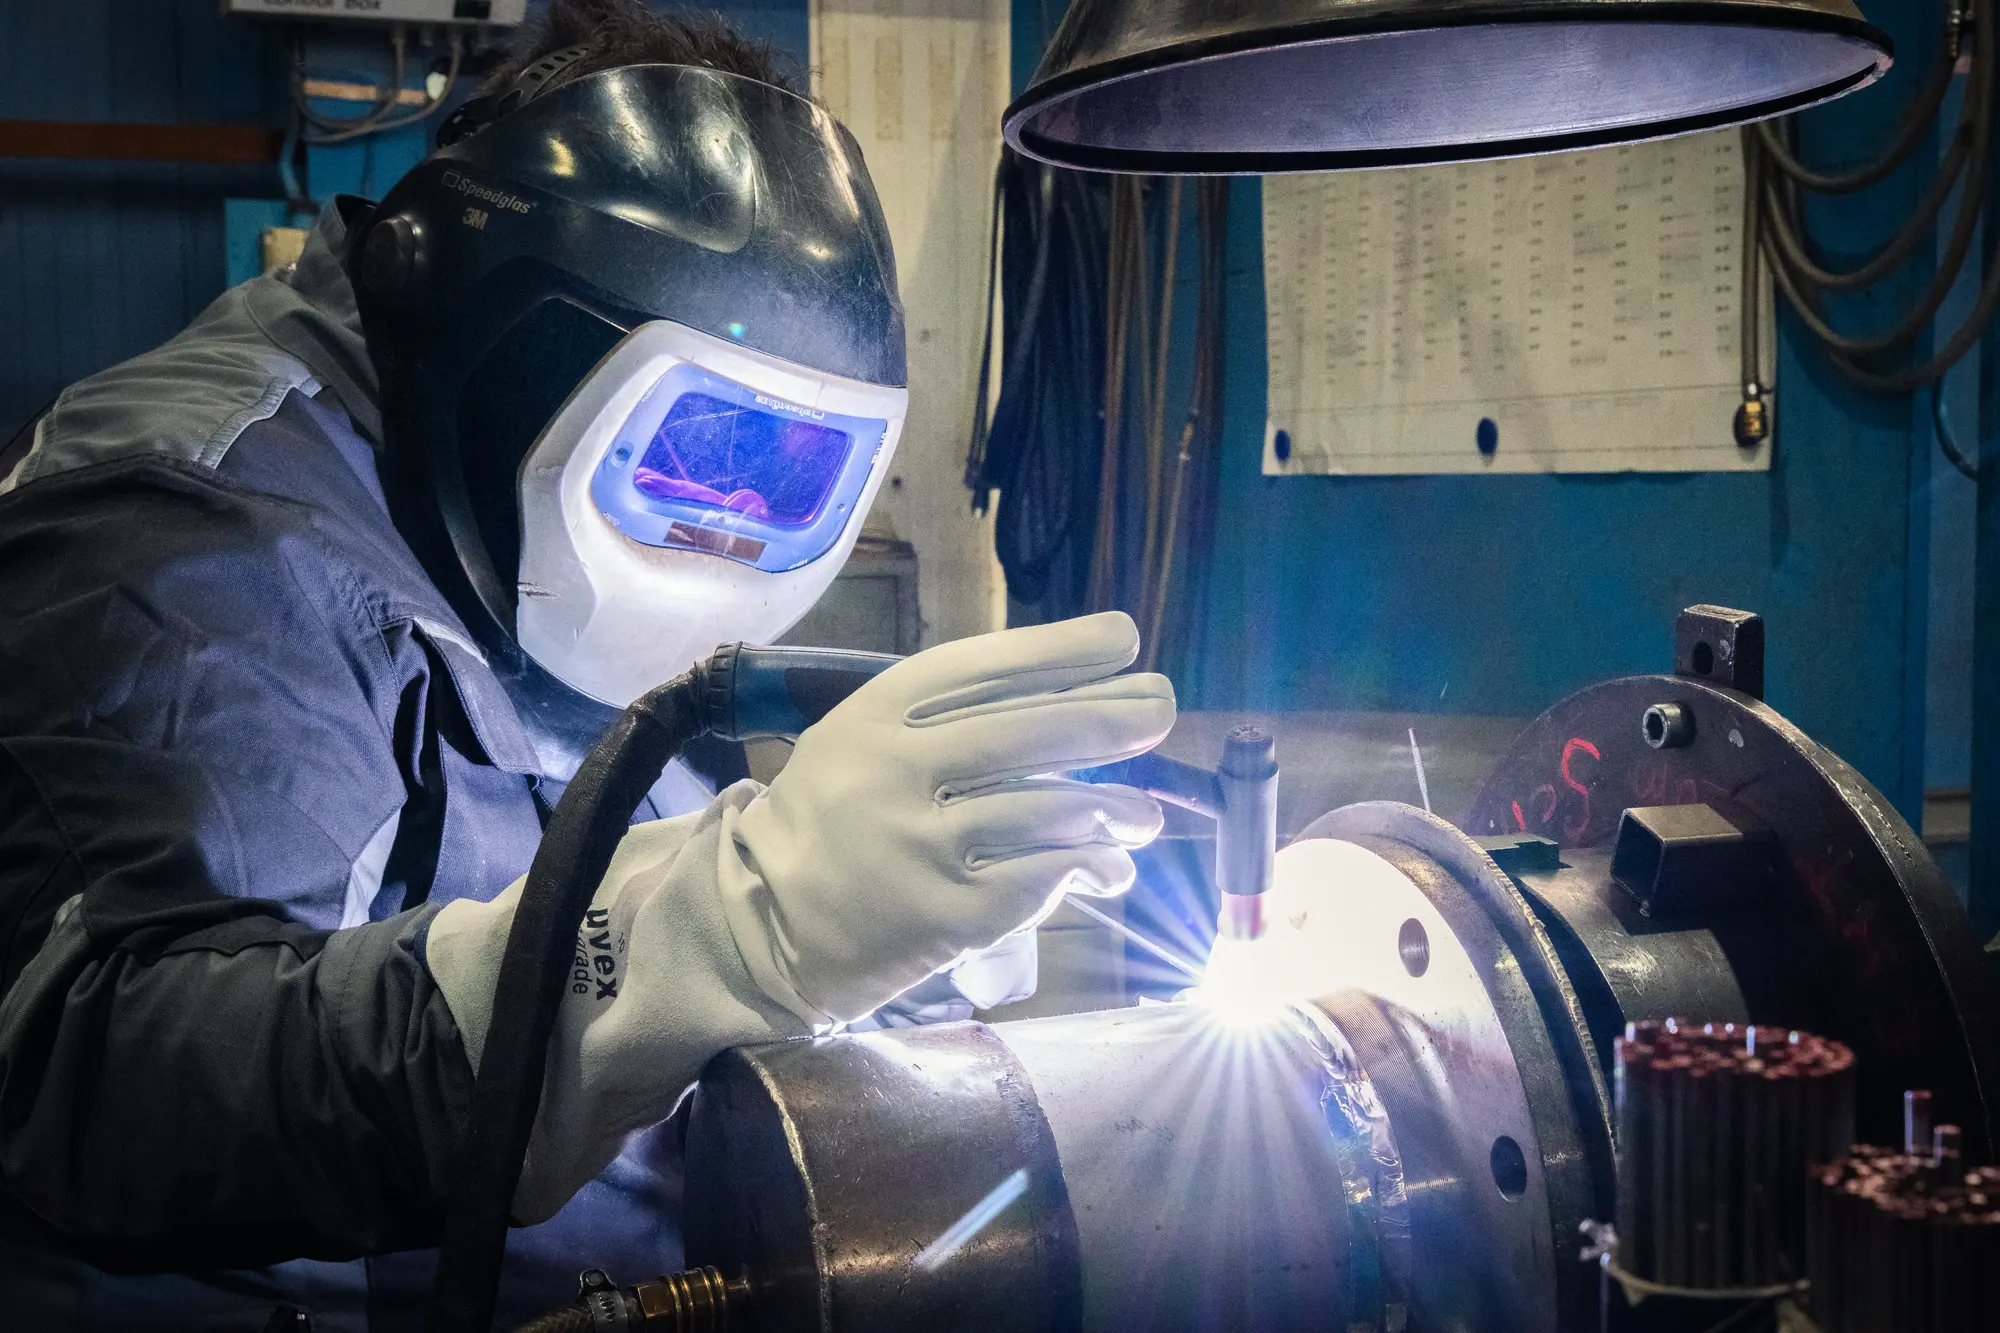
Vessels, apparatus and tubular heat exchangers in stainless steel and carbon steel – up to 3,000 mm diameter and 16 t component weight.
Friedrich Gruber GmbH Behälter- und Apparatebau
64846 Groß-Zimmern (headquarters, production and administration)New on Amplifa
Vessel and apparatus construction since 1964
Friedrich Gruber GmbH Behälter- und Apparatebau has been manufacturing custom apparatus, pressure and process vessels as well as straight-tube and U-tube heat exchangers since 1964 at its Groß-Zimmern site in the Rhine-Main region. Production is carried out to drawings, specifications and operating data in stainless steel and carbon steel; further materials such as duplex steel 1.4462 and nickel alloys (e.g. Hastelloy B-2, Hastelloy C-276, Alloy 59) are covered by procedure qualifications. Components are manufactured with diameters up to 3,000 mm, unit weights up to 16 tonnes and wall thicknesses up to 20 mm, usually as one-offs and small series. The service portfolio includes design and strength calculations according to the AD code, CAD drawing creation (AutoCAD 2D, Solidworks 3D), qualified TIG and MIG/MAG welding production, as well as testing and documentation. A particular focus is the 1:1 replacement of existing straight-tube and U-tube heat exchangers based on drawings, nameplates, operating data or the old unit – without conversion of the overall system. Customers include industries such as plant engineering, chemical process engineering and industrial process technology.
- Site
- Groß-Zimmern
- Processes
- Apparatus construction (custom apparatus for thermal and process engineering tasks), Vessel construction (pressure and process vessels), Straight-tube heat exchangers, U-tube heat exchangers, 1:1 replacement / reconstruction of existing heat exchangers, TIG welding, MIG/MAG welding, Design and strength calculation according to AD code
- Materials
- Stainless steel, Carbon steel, Duplex steel, Hastelloy B-2, Hastelloy C-276, Alloy 59, Duplex steel 1.4462, Nickel steels (Hastelloy B-2, Hastelloy C-276, Alloy 59)
- Certificates
- AD 2000-HP0 (manufacturer qualification welding shop), Module A2 under Directive PED 2014/68/EU (internal production control with, Specialist company qualification under §62 Water Resources Act, Quality assurance framework agreement with InfraServ Höchst GmbH & Co. KG, Module A2 under PED 2014/68/EU (internal production control with monitoring of, Manufacture according to DIN EN 13445
- Founded
- 1964
- Employees
- 15
- Industries
- Plant engineering, Process engineering, Industrial process technology
- 01
Design and strength calculation according to AD code
- 02
CAD drawing creation (AutoCAD 2D, Solidworks 3D)
- 03
Material processing (e.g. plasma cutting)
- 04
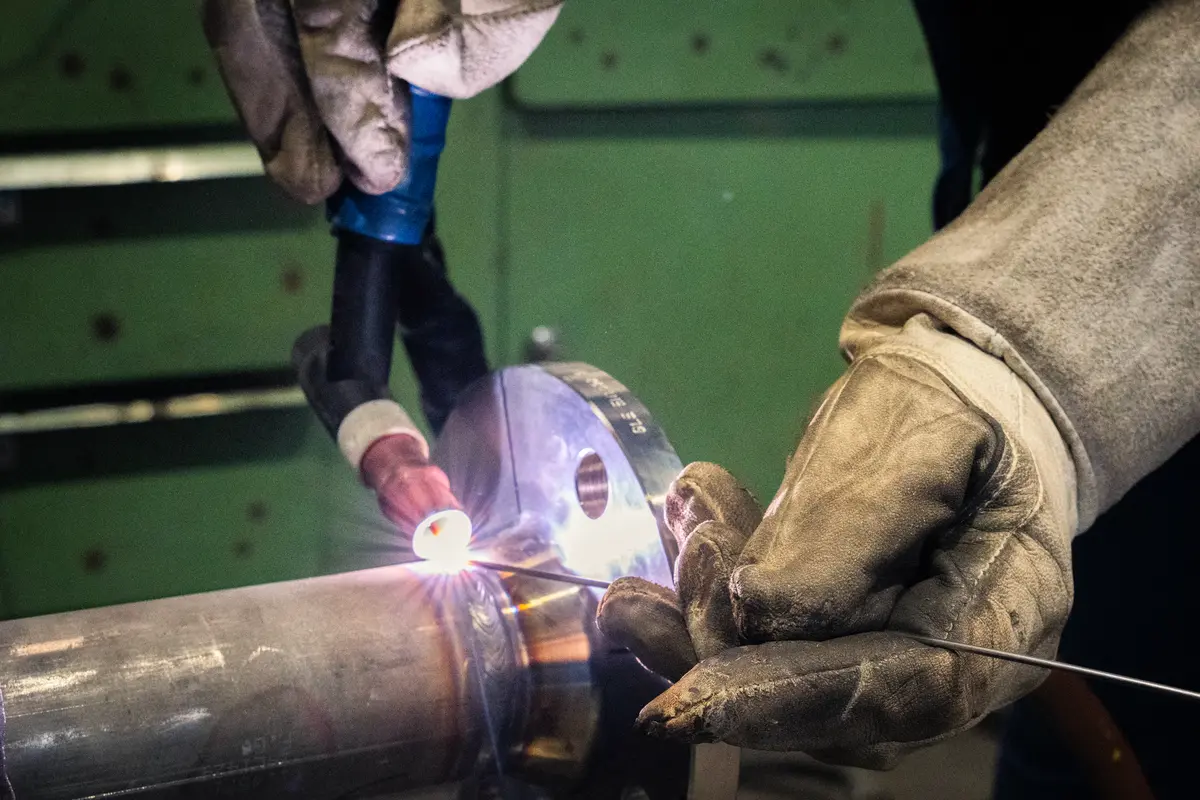
TIG and MIG/MAG welding production
- 05
Testing (X-ray, XRF, ultrasonic, wall/coating thickness measurement,
- 06
Material certificates and documentation
- 07
Manufacture of associated piping, supports, scaffolding and platforms
Materials and manufacturing processes
Stainless steel
Base material for vessels, apparatus and heat exchangers with procedure qualification according to AD 2000-HP series.
Carbon steel
Used for pressure and process vessels as well as apparatus with procedure qualification according to AD 2000-HP series.
Duplex steel 1.4462
Nickel or highly alloyed material with available procedure qualification for corrosion-exposed applications.
Nickel steels (Hastelloy B-2, Hastelloy C-276, Alloy 59)
Highly corrosion-resistant materials with available procedure qualifications for aggressive media in process engineering.
TIG welding
Qualified welding process for stainless steel and nickel alloy components.
MIG/MAG welding
Qualified welding process, among others, for carbon steel constructions.
Strength calculation according to AD code
Design of vessels and apparatus according to the AD code and associated regulations.
CAD drawing creation (AutoCAD 2D, Solidworks 3D)
Creation of production drawings to customer specification on modern CAD systems.
Production site
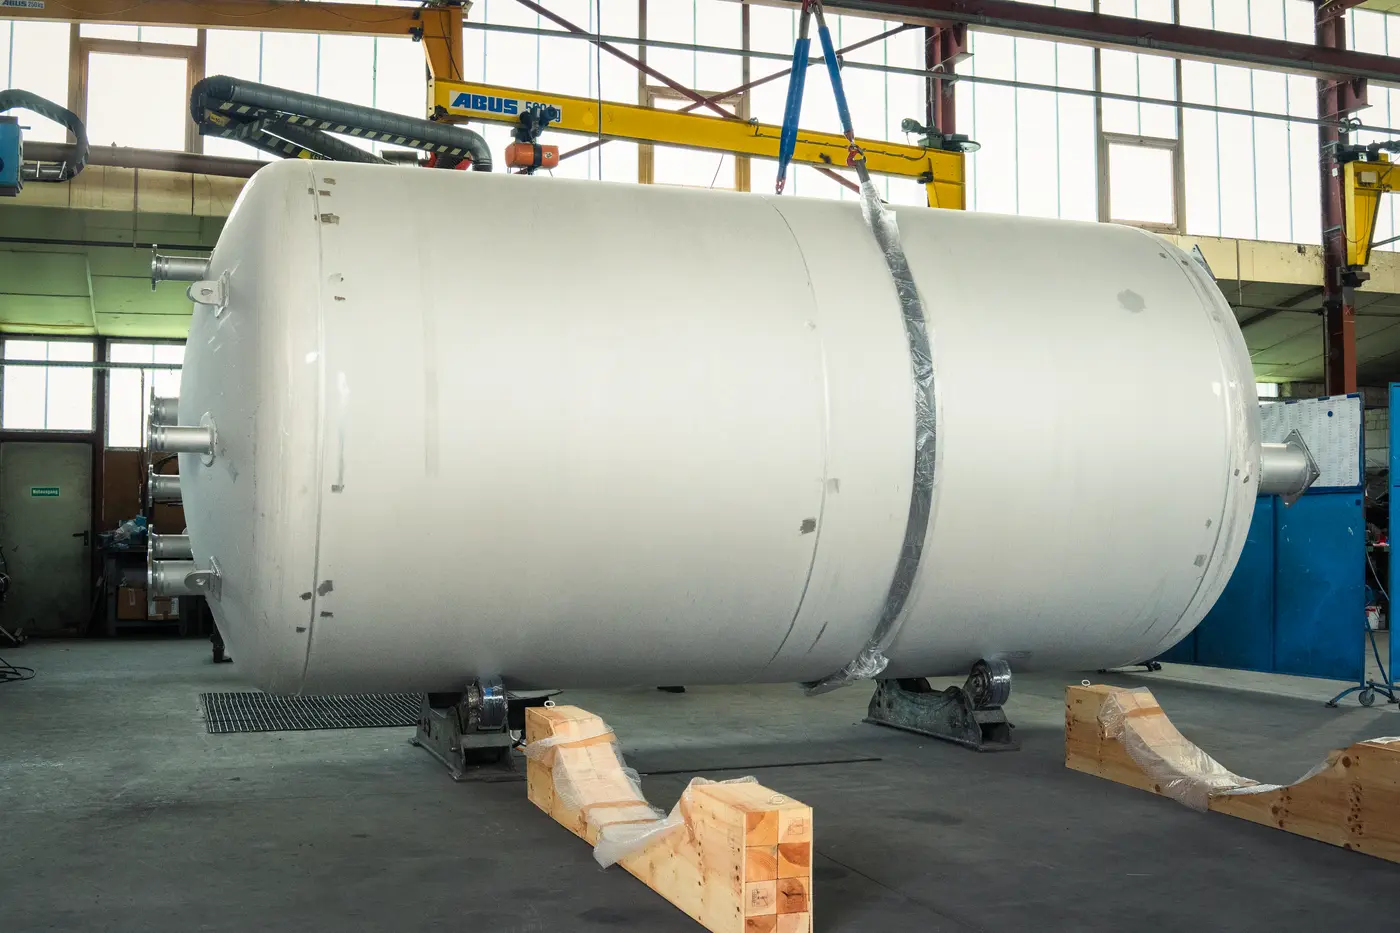
Groß-Zimmern
DEProduction and administration (headquarters)
- Part weight / size
- Components up to 3,000 mm diameter, up to 16 t, wall
- Lot size
- One-offs to small series
- Materials
- Stainless steel, carbon steel, duplex steel 1.4462, nickel steels (Hastelloy B-2, C-276, Alloy 59)
- CAD system AutoCAD 2D
- CAD system Solidworks 3D
- X-ray fluorescence spectrometer (XRF)
Manufactured components
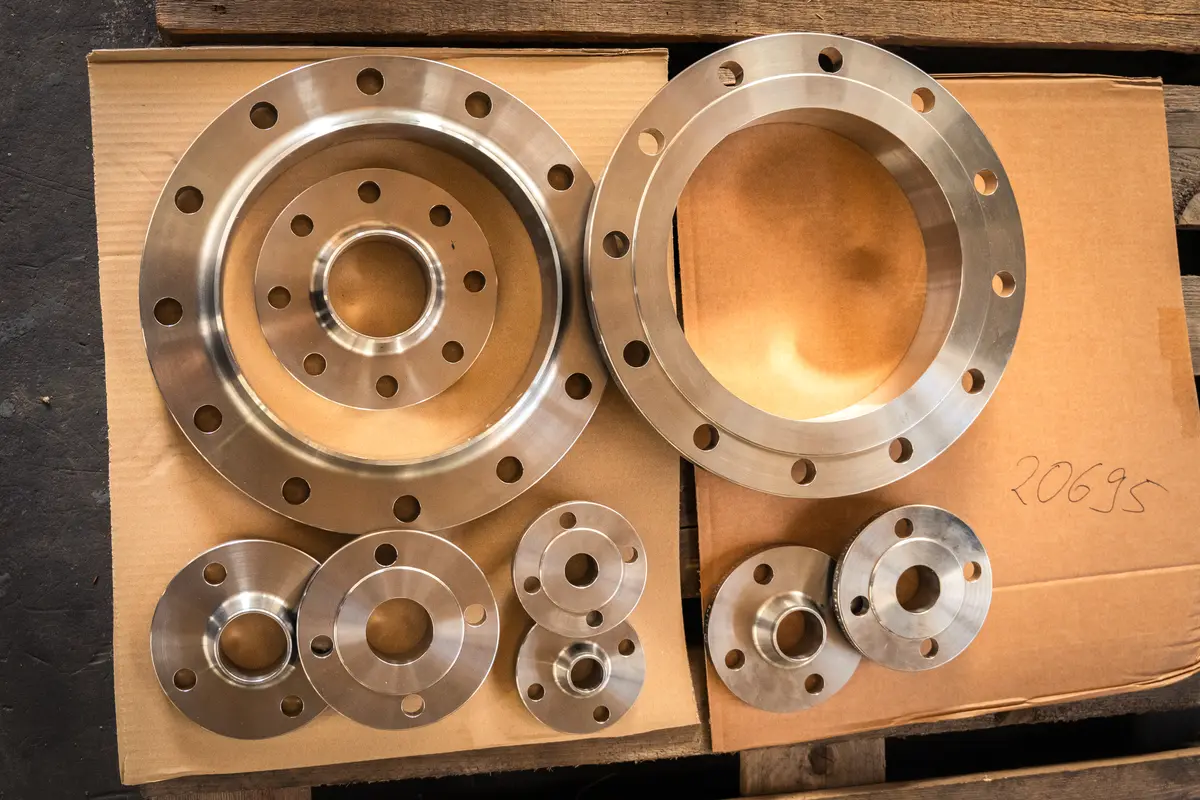
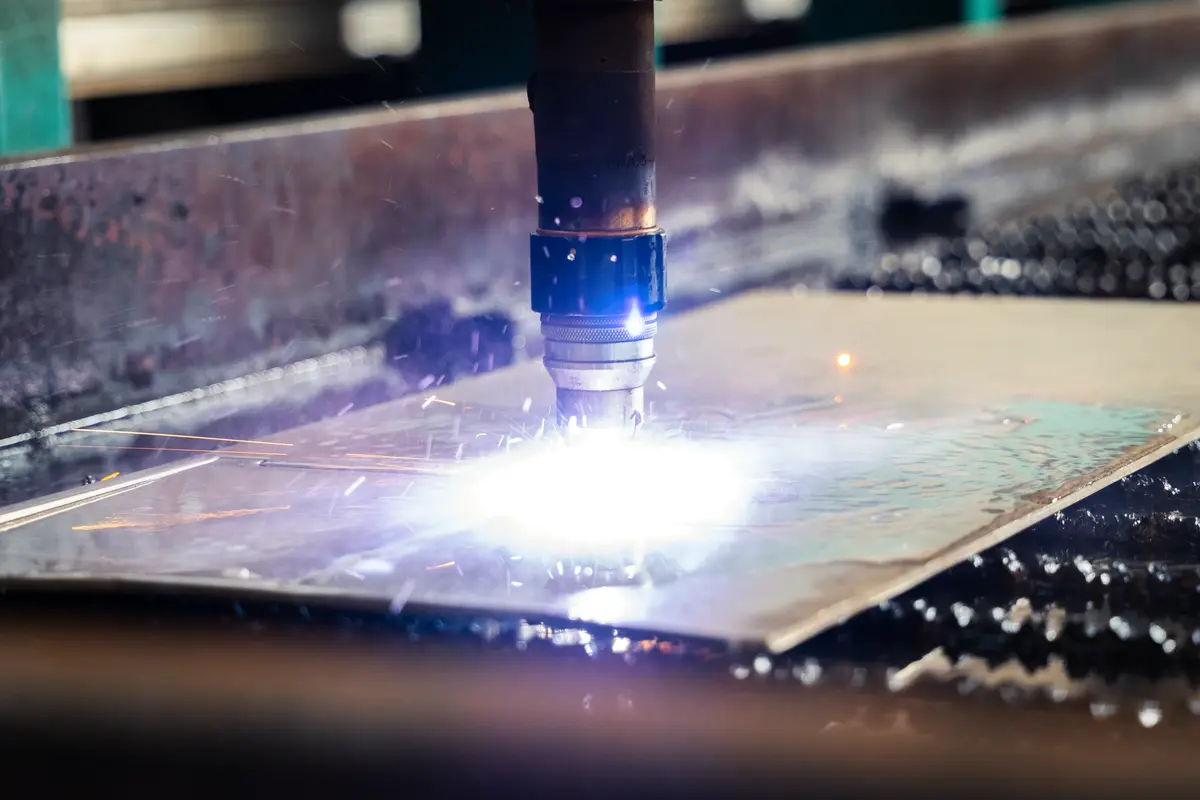
Inside the production
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Apparatus construction (custom apparatus for thermal and process engineering tasks)Joining | – | 3,000 mm diameter | 16 t | – | Stainless steel, Carbon steel |
| Vessel construction (pressure and process vessels)Joining | – | 3,000 mm diameter | 16 t | – | Stainless steel, Carbon steel |
| Straight-tube heat exchangersJoining | – | 3,000 mm diameter | 16 t | – | Stainless steel, Carbon steel |
| U-tube heat exchangersJoining | – | 3,000 mm diameter | 16 t | – | Stainless steel, Carbon steel |
| 1:1 replacement / reconstruction of existing heat exchangersEngineering | – | – | – | – | Stainless steel, Carbon steel |
| TIG weldingJoining | – | – | – | – | Stainless steel, Carbon steel |
| MIG/MAG weldingJoining | – | – | – | – | Stainless steel, Carbon steel |
| Design and strength calculation according to AD codeEngineering | – | – | – | – | – |
| Drawing creation (AutoCAD 2D, Solidworks 3D)Engineering | – | – | – | – | – |
| X-ray (weld seam testing)Testing | – | – | – | – | – |
| X-ray fluorescence spectrometer (XRF) material mix-up testingTesting | – | – | – | – | – |
| Ultrasonic testing (transmission)Testing | – | – | – | – | – |
| Wall and coating thickness measurementTesting | – | – | – | – | – |
| Surface roughness measurementTesting | – | – | – | – | – |
| Manufacture of piping, supports, scaffolding and platformsAssembly | – | – | – | – | Stainless steel, Carbon steel |
3 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| CAD system AutoCAD 2D | – | – | – | – | Groß-Zimmern |
| CAD system Solidworks 3D | – | – | – | – | Groß-Zimmern |
| X-ray fluorescence spectrometer (XRF) | – | – | – | – | Groß-Zimmern |
Additional services
Reference customers
Qualifications and testing
As an approved welding shop under AD 2000-HP0 with internal production control and monitored conformity assessment (Module A2 under PED 2014/68/EU), Gruber manufactures in accordance with AD 2000 and DIN EN 13445. Modern testing methods such as X-ray, ultrasonic (transmission), XRF for material mix-up testing as well as wall, coating thickness and roughness measurement ensure documented quality with material certificates and traceability.
| Evidence | Groß-Zimmern |
|---|---|
| AD 2000-HP0 (manufacturer qualification welding shop) | |
| Module A2 under PED 2014/68/EU (internal production control with monitoring of | |
| Specialist company qualification under §62 Water Resources Act | |
| Quality assurance framework agreement with InfraServ Höchst GmbH & Co. KG | |
| Manufacture according to DIN EN 13445 |
Company history
- 1964
Company founded; more than 50 years of experience in vessel and apparatus construction
- 1992
Registration of Friedrich Gruber GmbH Behälter- und Apparatebau, Darmstadt Local Court (HRB 32402)
- 2006
Registration of share capital of 300,000 DEM; Klaus Gruber registered as managing director
- 2026
Manuel Pfarr and Guido Barth registered as managing directors (according to Northdata)