Red brass castings raw and machined, copper and alloy strips as well as fittings for drinking water installation.
Gebr. Kemper GmbH + Co. KG
Olpe · Keltern · DülmenNew on Amplifa
About us
Gebr. Kemper GmbH + Co. KG is a family company founded in 1864, with its headquarters and central production site in Olpe in the Sauerland region. The company is divided into three business divisions: The Casting Technology division produces red brass castings raw and machined using the sand casting process (casting weights from 80 grams to 25 kilograms) on a fully automatic, clay-bonded green sand moulding line, including CAD design, casting simulation and CNC machining. The Rolled Products division manufactures strips made of copper and copper alloys – from strip casting through rolling, annealing and surface finishing to slitting – for the automotive and electrical industries. The Building Services division produces fittings and systems for drinking water hygiene, complemented by the Dendrit STUDIO planning software. Materials include red brass, lead-free red brass and brass alloys, bronzes and high-performance alloys (KHP®). Customers come from building services, the foundry industry, and the automotive and electrical industries. The subsidiaries Profiltech (Keltern) and Dendrit (Dülmen) expand the portfolio with profiled strips and building services software.
- Site
- Olpe – Biggesee
- Processes
- Red brass casting (sand casting, clay-bonded green sand moulding line), CAD design, design and engineering of castings, casting simulation, Machining of castings (raw and machined, CNC-controlled rotary transfer machine), Leak testing and washing (automated washing and leak testing systems), Strip casting and continuous casting for rolled products, Cold/hot rolling of metal strips (pass schedule, strip thickness reduction), Annealing (bell furnaces and continuous strip annealing lines), Surface finishing of strips (brushing, passivation, oiling, metallic coating)
- Materials
- Lead-free red brass (Rg+), Lead-free brass, Brass, Red brass (Rg5), Red brass multi-component bronze, Copper Cu-ETP, Copper Cu-PHC, Copper Cu-HCP
- Certificates
- ISO 9001:2015, ISO 9001:2015 (Rolled Products), ISO 14001:2015, ISO 50001:2018, ISO 45001:2018, ISO/IEC 27001, AEO (Customs Office Dortmund), CrefoZert creditworthiness certificate, IQNet (ISO 9001:2015), ISO 9001, ISO 14001, ISO 50001, ISO 45001, AEO
- Founded
- 1864
- Industries
- Building Services / Drinking Water Installation, Foundry / Casting Technology, Automotive industry, Electrical and electronics industry
- 01
Foundry (sand casting / continuous casting)
- 02
Rolling
- 03
Annealing
- 04
CNC machining
- 05
Surface finishing
- 06
Leak testing
- 07
Assembly
Materials and Processes
Lead-free red brass (Rg+)
REACH- and RoHS-compliant material for fittings and castings in contact with drinking water.
Red brass (Rg5)
Previously used, proven red brass for fittings manufacture.
Lead-free brass (CuZn42)
Lead-free brass material for building services components in contact with drinking water.
Brass CW617N
Standard brass for building fittings.
Red brass multi-component bronze
Sand casting alloy for demanding, long-lasting castings.
Copper Cu-ETP
Pure copper material with high electrical conductivity for strips.
Bronze CuSn6
Bronze strip with high strength for current-carrying spring elements.
Bronze HP
Bronze with improved bending properties in strip thicknesses up to 0.4 mm.
KHP®102 (CuNiSi)
High-performance alloy for miniaturisation in the connector and electronics sector.
KHP®181 (CuCrZr)
Precipitation-hardenable copper alloy for contact elements in high-current applications.
Locations
Olpe
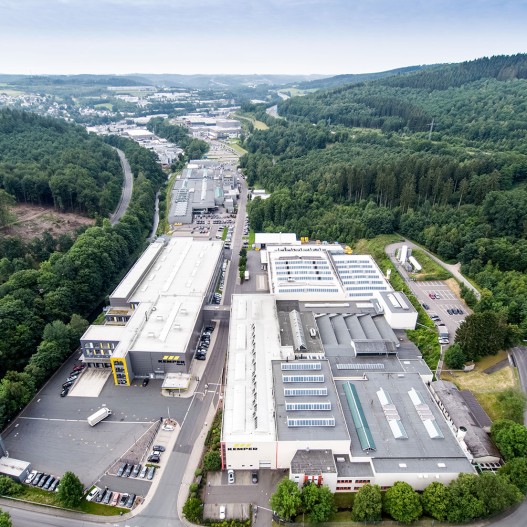
DEHeadquarters and production site (Plant 1 Casting Technology, Plants 2+3 Rolled Products, Plant 4 Building Services)
- Part weight / size
- 80 g – 25 kg casting weight
- Lot size
- Small, medium and large series
- Materials
- Red brass, brass, copper alloys, stainless steel
- Clay-bonded green sand moulding line (fully automatic)
- Melting furnaces for copper-tin alloys
- CNC-controlled rotary transfer machine
- Robot-assisted loading and unloading with camera recognition
- Automated washing and leak testing systems
- Rolling mills with state-of-the-art measurement and control technology
- Bell annealing furnaces and continuous strip annealing lines
- Slitting lines
Keltern
DEProfiltech Stufenbandprofile GmbH – profiled strips
- Materials
- Copper alloys
Dülmen
DEDendrit Haustechnik-Software GmbH
Components
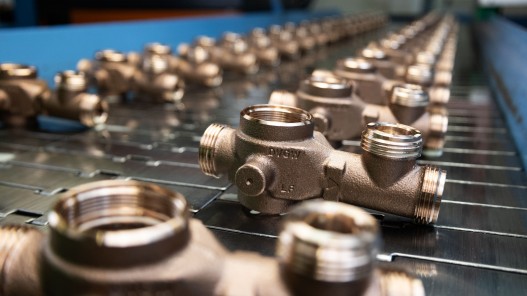
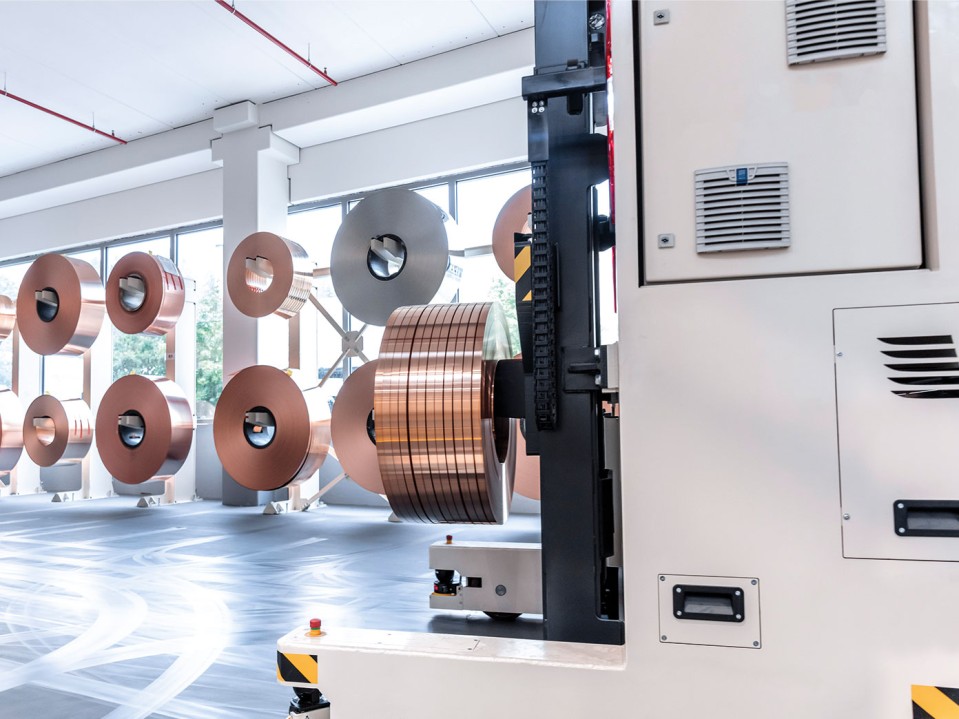
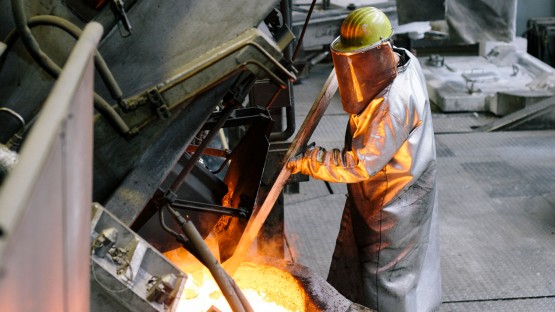
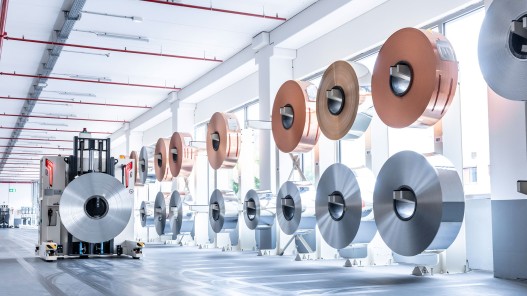
Inside the production
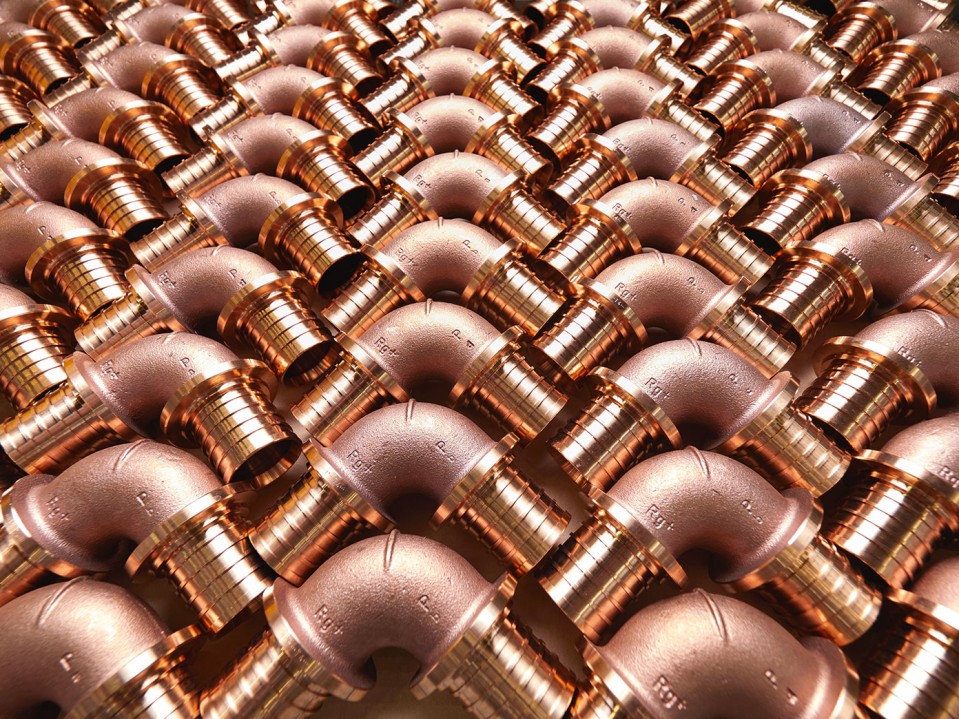
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Red brass casting (sand casting, clay-bonded green sand moulding line)Casting | – | 80 grams to 25 kilograms | 80 g – 25 kg | Small series – Large series | Lead-free red brass (Rg+), CuSn7Zn4Pb7-C, CuSn7Zn2Pb3-C, CuSn5Zn5Pb5-C, CuSn3Zn8Pb5-C, Copper-tin alloys |
| CAD design, design and engineering of castings, casting simulationEngineering | – | – | – | – | Copper alloys |
| Machining of castings (raw and machined, CNC-controlled rotary transfer machine)Machining | – | – | 80 g – 25 kg | – | Red brass, Copper alloys, Stainless steel |
| Leak testing and washing (automated washing and leak testing systems)Testing | – | – | – | Large series – Large series | Red brass |
| Strip casting and continuous casting for rolled productsCasting | – | – | – | – | Copper, Copper alloys, Bronzes, Copper-nickel-silicon |
| Cold/hot rolling of metal strips (pass schedule, strip thickness reduction)Forming | Strip thickness tolerances tighter than international | – | – | – | Copper, CuSn bronzes, Copper alloys |
| Annealing (bell furnaces and continuous strip annealing lines)Heat treatment | – | – | – | – | Copper, Copper alloys |
| Surface finishing of strips (brushing, passivation, oiling, metallic coating)Surface | – | – | – | – | Copper, Copper alloys |
| Slitting and recoiling of metal strips, stretch-bend levellingForming | – | – | – | – | Copper, Copper alloys |
| Manufacture of stepped strip profilesForming | – | – | – | – | Copper, Copper alloys |
| Manufacture of fittings and systems for drinking water installationAssembly | – | – | – | – | Red brass Rg+ (CC470K), Brass CW510L-DW, Brass CW617N |
10 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| Clay-bonded green sand moulding line (fully automatic, with continuous sand preparation) | – | – | – | – | Plant 1, Olpe |
| Melting furnaces for copper-tin alloys | – | – | – | – | Plant 1, Olpe |
| CNC-controlled rotary transfer machine | – | – | – | – | Plant 1, Olpe |
| Robot-assisted loading and unloading with camera recognition | – | – | – | – | Plant 1, Olpe |
| Automated washing and leak testing systems | – | – | – | – | Plant 1, Olpe |
| Bell annealing furnaces | – | – | – | – | Rolled Products, Olpe |
| Continuous strip annealing lines | – | – | – | – | Rolled Products, Olpe |
| Slitting lines | – | – | – | – | Rolled Products, Olpe |
| Rolling mills (with state-of-the-art measurement and control technology) | – | – | – | – | Plant II + III, Olpe |
| Finishing rolling stand | – | – | – | 1982 | Olpe |
Additional services
Reference customers
Quality
Automated washing and leak testing systems ensure the quality of castings; production is carried out with continuous process documentation and computer-aided casting simulation. Quality assurance is certified to ISO 9001, ISO 14001, ISO 50001 and ISO 45001.
| Evidence | Olpe |
|---|---|
| ISO 9001 | |
| ISO 14001 | |
| ISO 50001 | |
| ISO 45001 | |
| ISO/IEC 27001 | |
| AEO |
History
- 1864
Founding of the hinge factory “Gebr. Kemper” in Olpe by Johann-Anton and Eberhard Eduard Kemper
- 1893
Purchase of a copper hammer mill in Saßmicke
- 1899
Purchase of the first areas of the later company premises (former Rüblinghauser Hütte); switch to copper processing
- 1921
Conversion of the drive system from water wheels to water turbines, electrification
- 1928
Construction of a copper smelter with refining operation
- 1953
Commissioning of an aluminium foundry
- 1962
Establishment of continuous casting production for rolled products
- 1974
Relocation to a new industrial and commercial area in the Bigge valley; founding of the subsidiary Kemper Metallurgie Maschinenbau
- 1982
Entry into electrical engineering (rolled products) through acquisition of the first finishing rolling stand
- 1993–2012
Founding of sales companies in Switzerland, Shanghai, Great Britain and the USA
- 2010
Acquisition of Dendrit Haustechnik-Software GmbH, Dülmen
- 2012
Acquisition of Profiltech Stufenbandprofile GmbH, Keltern
- 2014–2020
Construction of office building, shipping/picking, production areas and high-bay warehouse