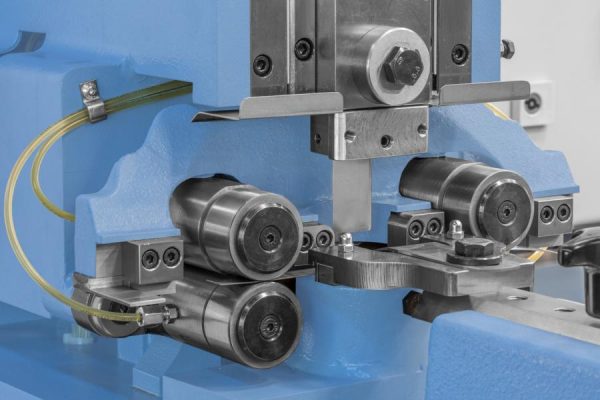
Special machine building for the saw industry: tooth-setting, swaging and grinding machines, reels, retrofitting and service in Remscheid.
HAAS Maschinenbau GmbH
Remscheid (Glockenstahlstrasse 3)New on Amplifa
About HAAS Maschinenbau
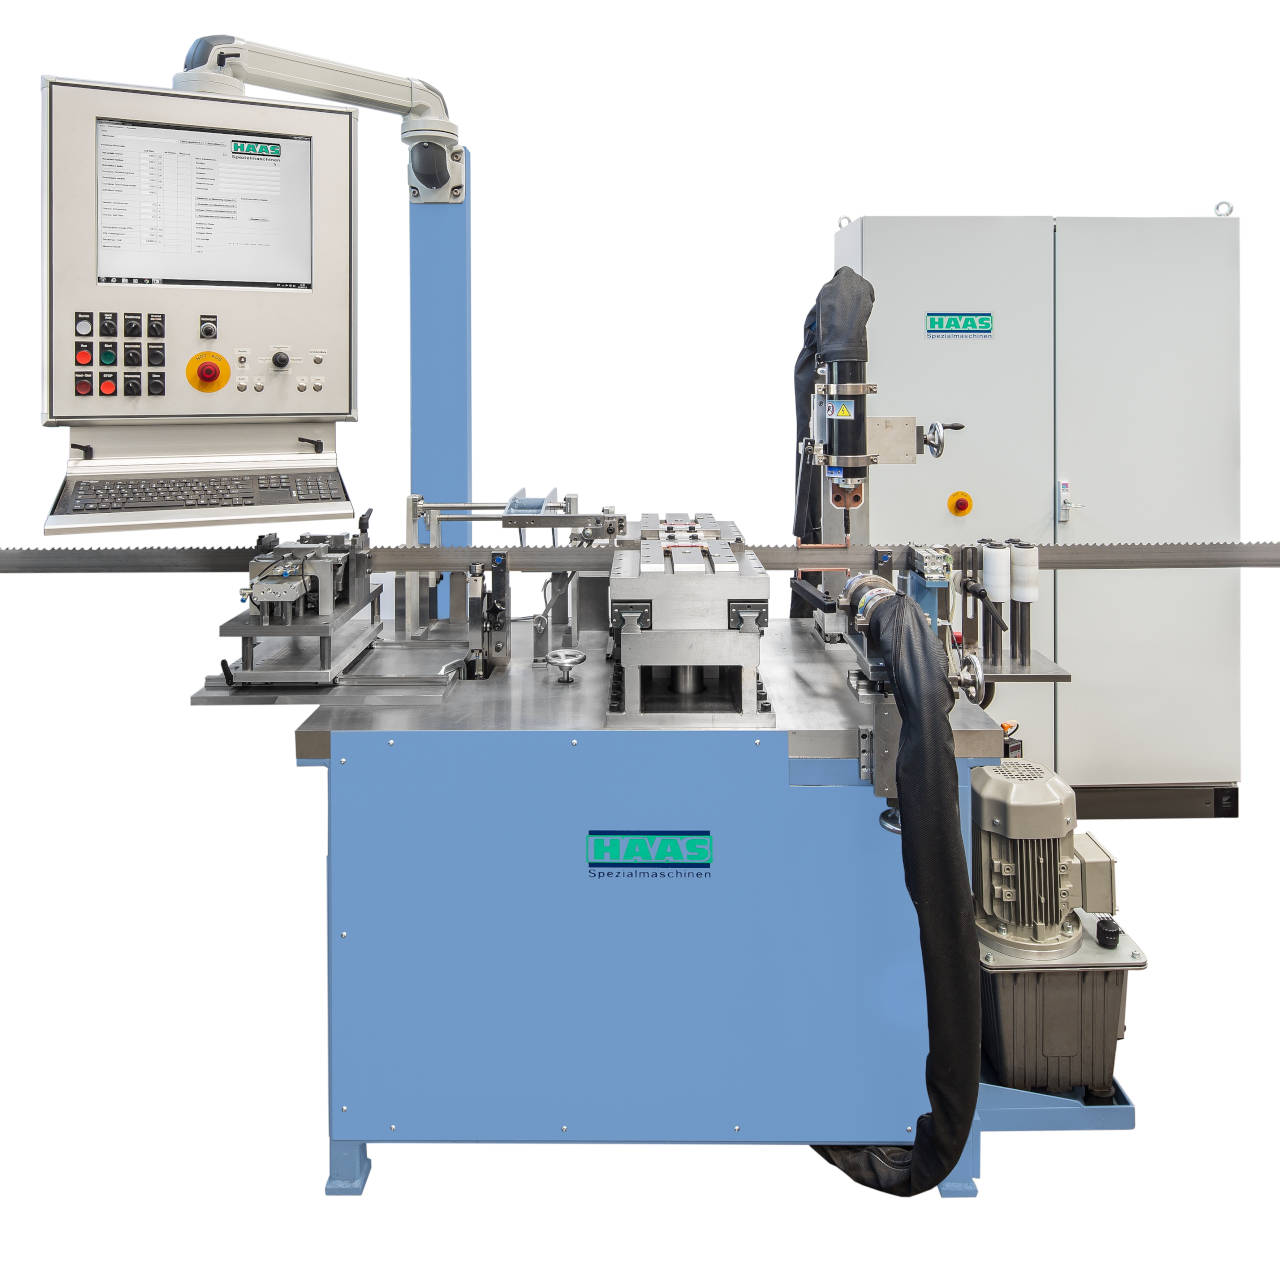
HAAS Maschinenbau GmbH is a family-run special machine builder headquartered in the Hasten district of Remscheid. Since 1983 the company has developed and manufactured tooth-setting machines, swaging machines, grinding machines, roller feeds and reel systems for the international saw, bandsaw and knife industry. The machines are produced with a high level of in-house manufacturing; base structures consist of welded steel constructions, while cast parts and hydraulic components are sourced from German specialist firms. In addition to building new machines for prototypes and small series, HAAS offers retrofitting, repair and maintenance, build-up welding, flame spraying, hard chrome plating as well as spare part and wear part manufacturing. 1,700 m² of shop floor space house lathes, boring mills, sawing and grinding machines, welding systems and a ten-ton crane. Customers include Röntgen Metallsägen, Pisana, Lumbeck & Wolter, Benteler Distribution, Wilpu and Arntz.
- Site
- Remscheid
- Processes
- Special machine building (tooth-setting, swaging, grinding machines, reels), Tooth-setting (stamping) of bandsaws and handsaws, Swaging of saw bands (bi-metal and carbide-tipped bandsaws), Swaging of jigsaws and reciprocal saws, Retrofitting / modernization / general overhaul of machines (re-broaching of guideways,, Repair and restoration of individual machines, production lines, manufacturing and, Bonding techniques (single-sided wet bonding, double-sided contact bonding), Flame spraying (thermal coating process, wire/powder materials)
- Materials
- Steel (welded steel construction, saw steel, strip material), Cast parts, Bi-metal, Carbide, Ceramic materials, Wire, strip and sheet material, Metallic materials (flame spraying), Steel (welded steel construction)
- Certificates
- Project management and quality management
- Founded
- 1983
- Employees
- 10
- Industries
- Bandsaw manufacturers, Saw industry, Knife industry, Printing industry, Metal processing
- 01
Design and development
- 02
Machining (turning, milling, grinding, broaching)
- 03
Welded constructions
- 04
Build-up welding and coating technology (flame spraying, hard chrome plating)
- 05
Assembly of special machines
- 06
Commissioning, service and retrofitting at the customer's site
Materials & Processes
Steel (welded steel construction)
Machine base structures and saw steel strip material for tooth-setting and swaging.
Cast parts
Sourced from German specialist companies for tooth-setting machine components.
Bi-metal
Hardened bi-metal bandsaws have been swaged to production standard since 2013.
Carbide (HM)
Carbide-tipped bandsaws are swaged with tolerances of ±0.02 mm.
Metallic and ceramic materials
Build-up materials for flame spraying for wear and corrosion protection.
Locations
Remscheid
DEProduction and administration
- Lot size
- Prototypes to small series
- Materials
- Steel, cast parts, bi-metal, carbide
- Tooth-setting machine H-ZE1 (in-house build)
- NC tooth-setting machine PZH / PZH 2 / PZH 3
- Swaging machines PS-H 67 H / PS-H 100 H
- Single-part swaging machine with servo gantry handling
- Uncoiling and recoiling reels (H-250, VA-300, H-1000, V-150/300/500)
- Roller feed
- Lathes
- Boring mills
- Sawing and grinding machines
- Welding systems
- Fixtures for flame spraying
- Ten-ton crane
Products & Components
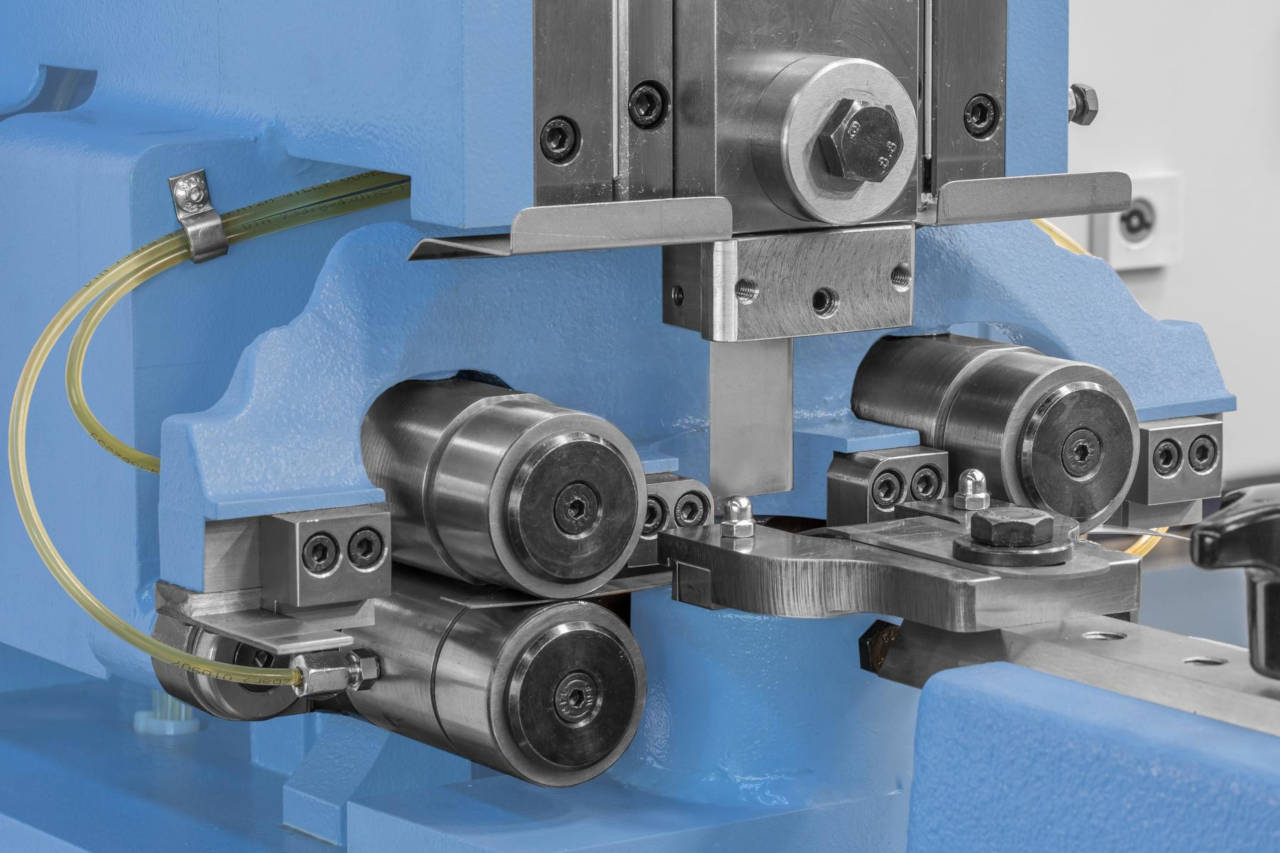
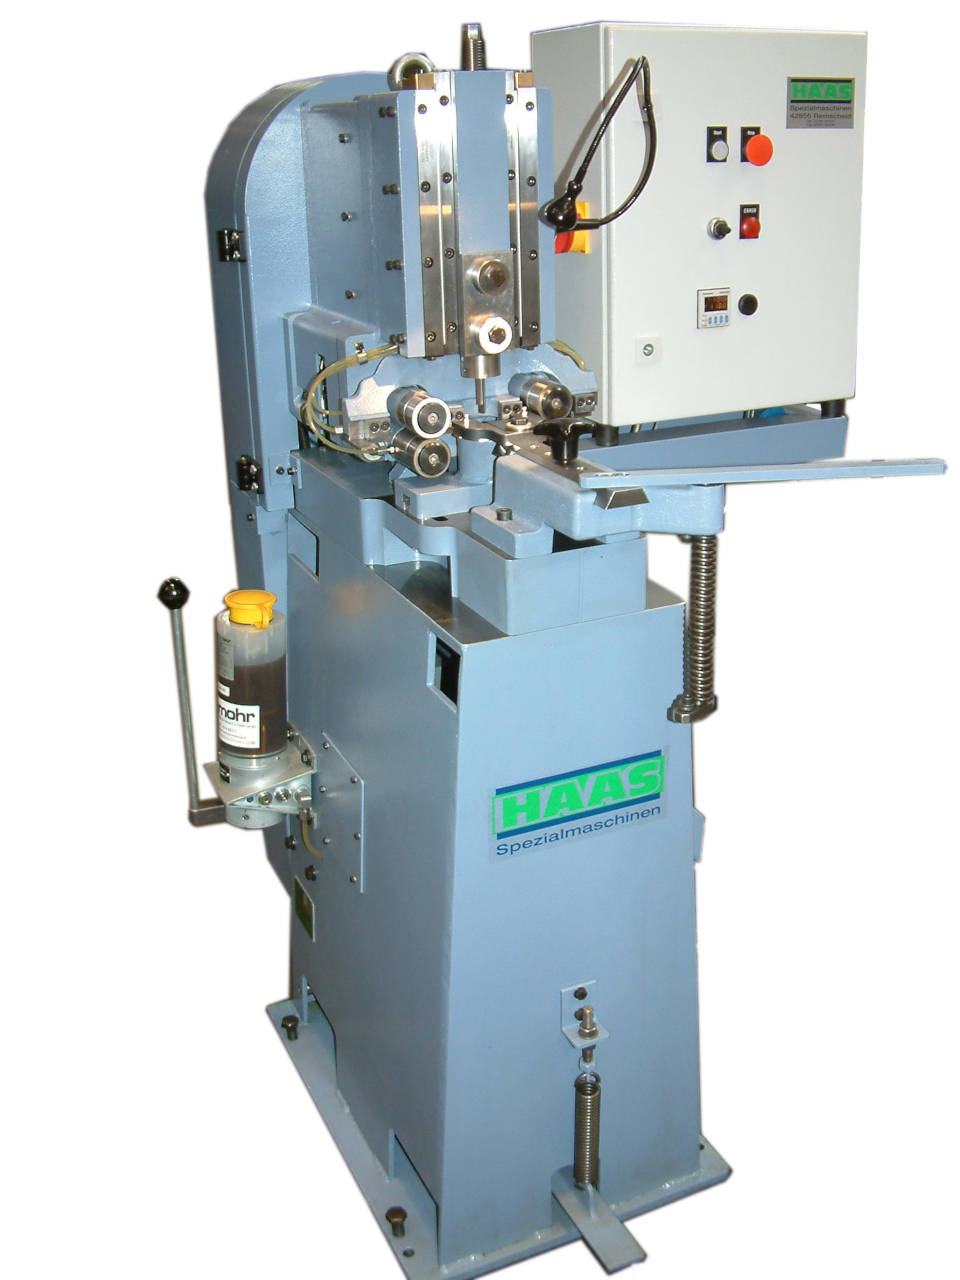
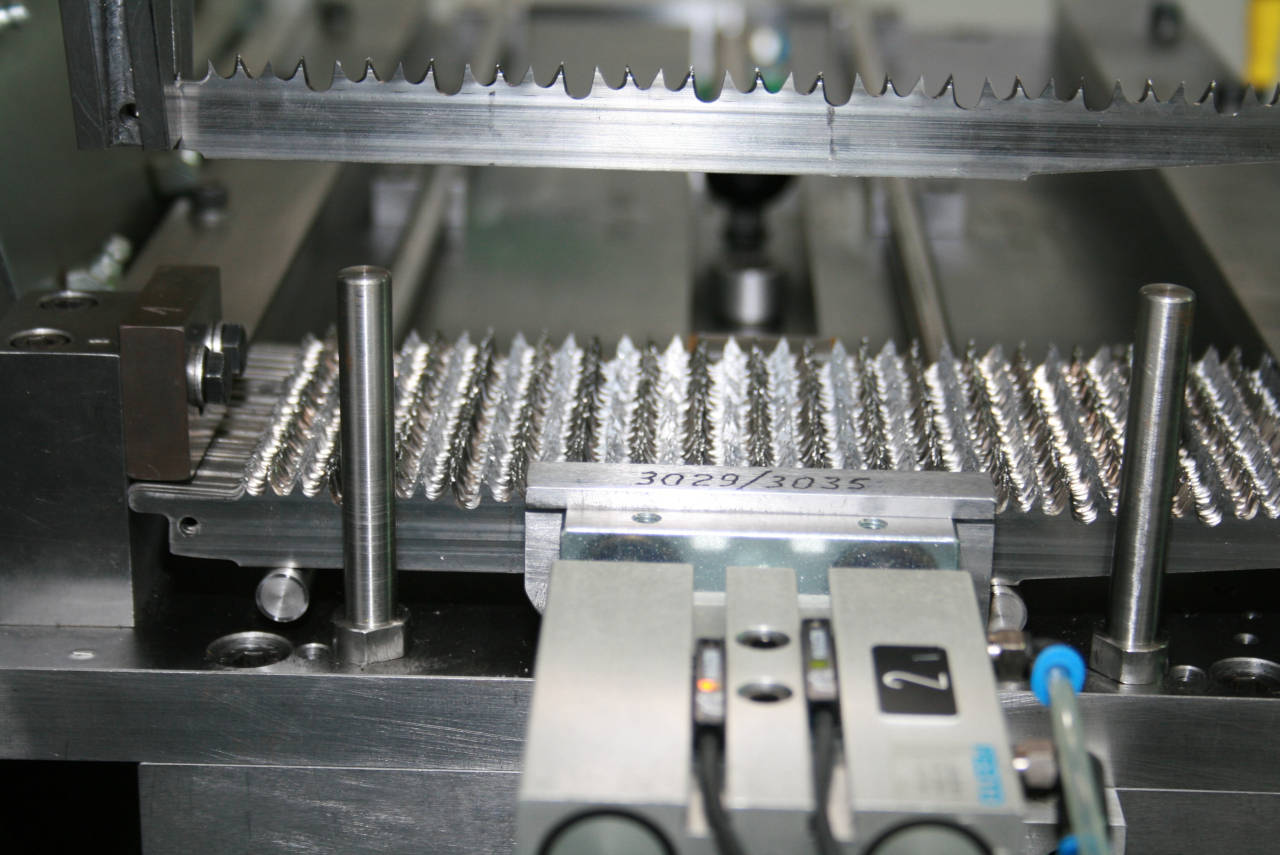
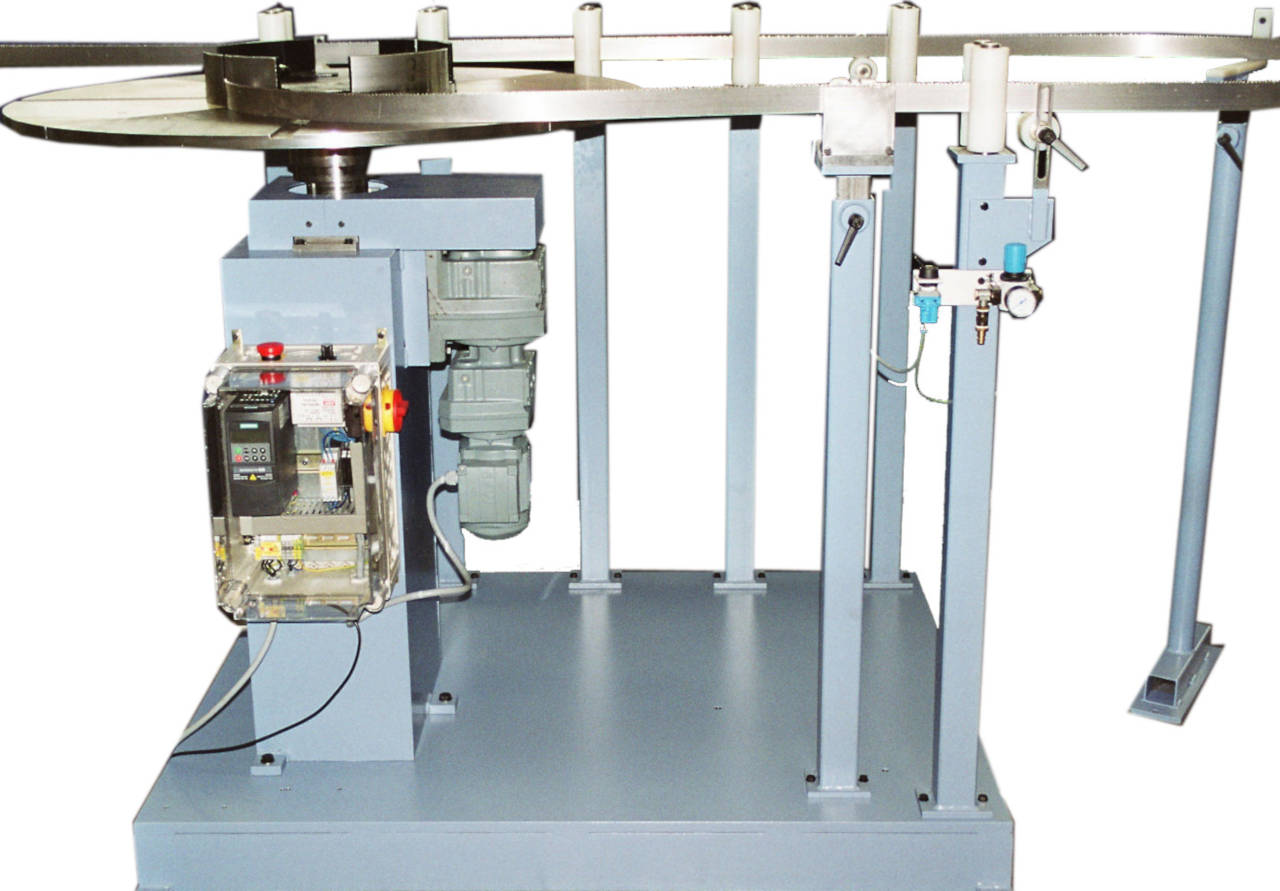
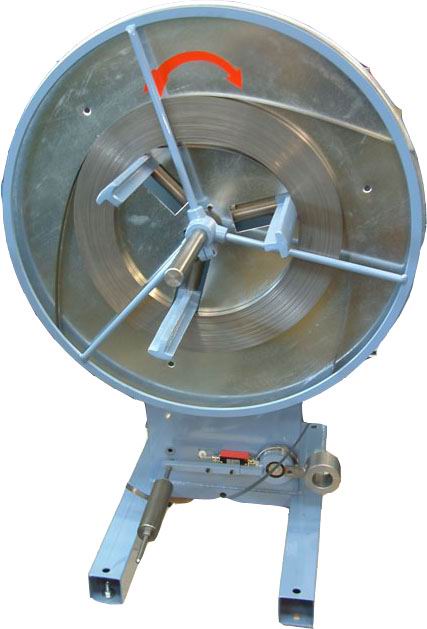
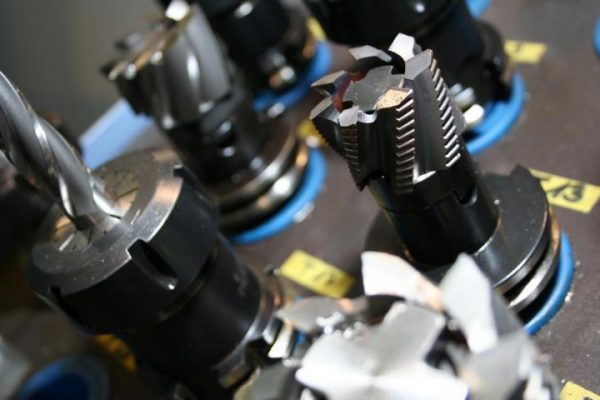
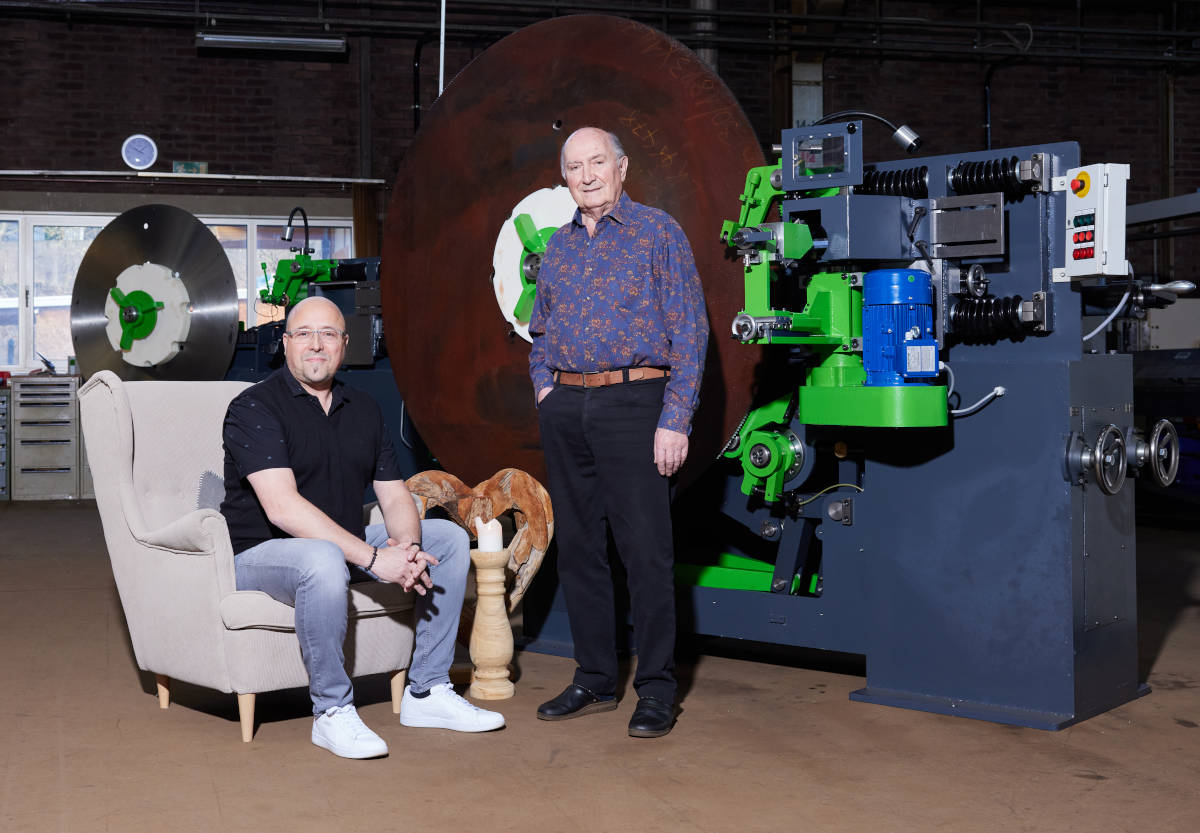
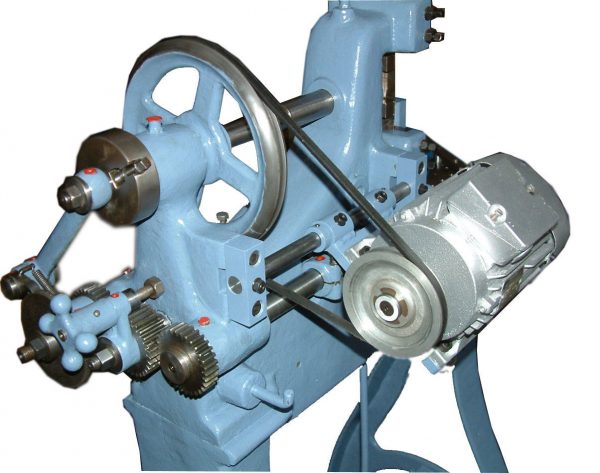
Inside the production
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Special machine building (tooth-setting, swaging, grinding machines, reels)Engineering | – | – | – | Prototypes/single parts – Small series | Steel (welded steel construction), Cast parts |
| Tooth-setting (stamping) of bandsaws and handsawsForming | Tooth pitch increments 0.1 mm; tolerance per stroke <0.01 mm | Band width 5–200 mm × Band thickness max. 1.5 mm | – | – | Saw steel |
| Swaging of saw bands (bi-metal and carbide-tipped bandsaws)Forming | +/- 0.02 mm | 150 mm (group swaging) × Band width 20–105 mm × Band thickness up to 2 mm | – | – | Bi-metal, Carbide, Steel |
| Swaging of jigsaws and reciprocal sawsForming | +/- 0.02 mm | 150 mm | – | – | Steel |
| Retrofitting / modernization / general overhaul of machines (re-broaching of guideways,Engineering | – | – | – | – | – |
| Repair and restoration of individual machines, production lines, manufacturing andAssembly | – | – | – | – | – |
| Bonding techniques (single-sided wet bonding, double-sided contact bonding)Joining | – | – | – | – | – |
| Flame spraying (thermal coating process, wire/powder materials)Surface | – | – | – | – | metallic materials, ceramic materials |
| Hard chrome plating (build-up technique for highly stressed parts)Surface | – | – | – | – | Metal |
| Metal build-up by powder jet processSurface | – | – | – | – | Metal |
| CoatingsSurface | – | – | – | – | – |
| Welding processes (build-up welding)Joining | – | – | – | – | Metal |
| EDM (electrical discharge machining)Machining | – | – | – | – | Metal |
| TurningMachining | – | – | – | – | – |
| MillingMachining | – | – | – | – | – |
| GrindingMachining | – | – | – | – | – |
| BroachingMachining | – | – | – | – | – |
| Rolling of tension zones in saw blades (rolling rollers, rolling track adjustment)Forming | – | – | – | – | Saw blade steel |
| Spare part and wear part manufacturing in-houseMachining | – | – | – | – | – |
18 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| Uncoiling reel (horizontal) | HAAS H-250 | – | Coil weight max. 250 kg; band width up to 80 mm; outer diameter up to 1200 mm; band speed | – | Remscheid |
| Uncoiling reel (vertical) | HAAS VA-300 | – | Coil weight max. 300 kg; band width up to 240 mm; outer diameter up to 800–1200 mm; | – | Remscheid |
| Recoiling reel (horizontal, driven) | HAAS H-1000 | – | Coil weight max. 500 kg; band width up to 120 mm; outer diameter up to 1200 mm; band speed | – | Remscheid |
| Recoiling/uncoiling reel (vertical) | HAAS V-150 / V-300 / V-500 | – | Coil weight 150–300–500 kg, max. 800 kg; band width up to 150–300 mm; outer diameter up to 870–1000 | – | Remscheid |
| Tooth-setting machine | HAAS H-ZE1 | – | Blade width 6–200 mm; blade thickness max. approx. 1.5 mm; tooth pitch approx. <1–20 mm; pressing | – | Remscheid |
| High-performance NC tooth-setting machine | HAAS PZH | – | Band width 5–60 mm; band thickness max. 1.0 mm; stroke rate 100–1000/min (Siemens FU); feed 1–99.9 | – | Remscheid |
| NC tooth-setting machine | HAAS PZH 2 / PZH 3 | – | Pressing force 15 t (PZH 2) / 25 t (PZH 3) | – | Remscheid |
| Automatic swaging machine for saw bands | HAAS PS-H 67 H / PS-H 100 H | – | Band width 20–105 mm; band thickness up to 2 mm; tolerance ±0.02 mm; machining length up to 150 mm | – | Remscheid |
| Single-part swaging machine (jigsaw/reciprocal saws, fully automatic, servo gantry handling) | HAAS | – | Tolerance ±0.02 mm; machining length up to 150 mm | – | Remscheid |
| Roller feed | HAAS | – | W x H x D 220 x 750 x 400 mm incl. drive; carbide-coated knurling wheel; hardened and | – | Remscheid |
| Tooth-setting machine (retrofit) | Gustav Paffenhoff ZE / ZG / ZH | – | – | 2006 | Remscheid |
| Lathes | – | – | – | – | Remscheid |
| Boring mills | – | – | – | – | Remscheid |
| Sawing and grinding machines (machine park) | – | – | – | – | Remscheid |
| Welding systems (various welding processes) | – | – | – | – | Remscheid |
| Fixtures for metal spraying | – | – | – | – | Remscheid |
| Ten-ton crane | – | 1 | – | – | Remscheid |
| Three-ton scale | – | 1 | – | – | Remscheid |
Additional services
Reference customers
Quality
Manufacturing is carried out with a high proportion of in-house production; tolerances of ±0.02 mm when swaging and less than 0.01 mm per stroke on the PZH tooth-setting machine are maintained. An integrated quality control system monitors symmetry and swage width.
| Evidence | Remscheid |
|---|---|
| Project management and quality management |
History
- 1979
Hans R. Haas starts out self-employed in a garage on Ackerstrasse with repairs and small machines for the saw industry.
- 1983
Foundation of HAAS Maschinenbau GmbH by Hans R. Haas; design work at Petter Otto Vogel.
- 1985
Relocation to larger premises on Büchelstrasse.
- 2004
Move to 1,700 m² of shop floor space on Glockenstahlstrasse.
- 2006
Retrofit of a Paffenhoff tooth-setting machine type ZE.
- 2007
Oliver R. Haas becomes managing director on 1 July; Hans R. Haas becomes authorized signatory.
- 2013
Production readiness of the process for swaging bi-metal and carbide-tipped bandsaws.
- 2015
Establishment of the retrofitting business as a partner for machine modernization.