Manufacturing of metal parts, individual components and complex assemblies through laser cutting, machining, welding, surface technology and assembly
Härtwig Maschinenbau GmbH & Co. KG
CunewaldeNew on Amplifa
About Härtwig Maschinenbau
Härtwig Maschinenbau GmbH & Co. KG in Cunewalde is a medium-sized contract manufacturer for metal and sheet metal processing. Around 60 employees manufacture custom individual parts as well as complex assemblies for machinery; approximately 1,000 different individual parts pass through production each day. The value chain ranges from design and consulting through laser cutting, saw cutting, oxy-fuel flame cutting, folding, punching, CNC turning and milling, welding and tube bending to deburring, blasting, painting, powder coating and assembly of mechanical assemblies including electrical, pneumatic and hydraulic drives. The materials processed are mainly steels (e.g. S235, S355, C45, 16MnCr5), stainless steels (1.4301, 1.4404), aluminium (EN AW-6060), copper (Cu-ETP) and plastics (PA6). Customers include renowned transport system suppliers to the automotive industry, mechanical engineering companies as well as SMEs from Upper Lusatia; turned parts also go to medical and electrical engineering. The company works on networked industrial production and participates in research projects such as iBoxII (TU Chemnitz) and AdapStiff (Fraunhofer IWU). Orders come from the region, from all over Germany and from a number of other countries.
- Site
- Cunewalde
- Processes
- Laser cutting (fibre laser), Saw cutting (CNC sawing machines), Oxy-fuel flame cutting, CNC folding (laser-controlled angle sensing, mark-free bending), Punching (CNC punching), CNC turning (turning machines with driven tools, bar magazine), CNC milling (machining centres), Welding (MIG, MAG, TIG, spot welding; MAG welding robot cell)
- Materials
- S235JRG2, S235JR+C, S235JRC+C, S235JRGC+C, S355J2G3 / S355J2G3C+C, S355J2+C, S355JRG2, S355JRG2C+C
- Certificates
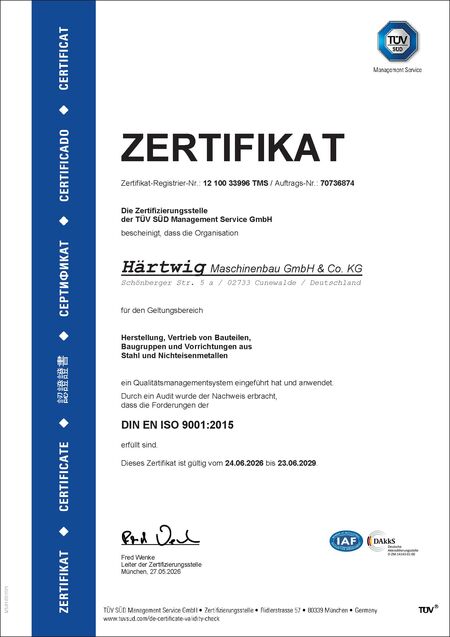
- DIN EN ISO 9001:2015, EN 1090-2:2018+A1:2024
- Founded
- 2006 (mer
- Employees
- around 60
- Industries
- Mechanical engineering, Automotive industry (transport systems), Plant engineering, Medical technology, Electrical engineering, Automotive industry (transport systems/transport system suppliers)
- 01
Design & consulting (.dxf, .dwg, .ai, CAD)
- 02
Laser cutting / saw cutting / flame cutting
- 03
Folding & punching
- 04
CNC turning & CNC milling
- 05
Welding
- 06
Tube bending
- 07
Deburring & marking
- 08
Blasting / painting / powder coating
- 09
Assembly
- 10
Quality assurance
Materials & Processes
S235JRG2 / S235JR
Structural steel for laser cutting, punching and saw cutting in general mechanical engineering applications.
S355J2G3 / S355JRG2
Higher-strength structural steel for load-bearing assemblies and structural steelwork according to EN 1090-2.
C45 / C45E
Heat-treatable steel for machined turned parts and components with higher strength requirements.
16MnCr5
Case-hardening steel for case-hardened components such as shafts and gears.
11SMn30 / 11SMnPb30
Free-cutting steel for production-ready turned parts.
1.4301 (X5CrNi18-10)
Stainless steel for corrosion-resistant components and in-house products such as planters.
1.4404
Chromium-nickel-molybdenum stainless steel for applications with higher corrosion stress.
EN AW-6060 (AlMgSi0.5)
Aluminium alloy for lightweight, machinable components.
Cu-ETP (CW004A)
Electrolytic copper for electrically conductive components.
PA6
Plastic for machinable technical parts.
Locations
Cunewalde
DEHeadquarters and production
- Part weight / size
- Welded assemblies up to 2,000 kg
- Lot size
- Individual parts, small, medium and large series
- Materials
- Steel, stainless steel, aluminium, copper, plastic
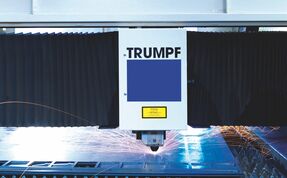
- Fibre laser cutting system (4,000 x 2,000 mm, up to 25 mm, up to 140 m/min)
- CNC sawing machine (Ø up to 400 mm, profiles up to 500 x 300 mm)
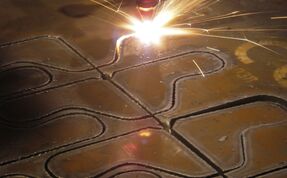
- CNC flame cutting machine (6,000 x 2,000 mm, up to 360 mm)
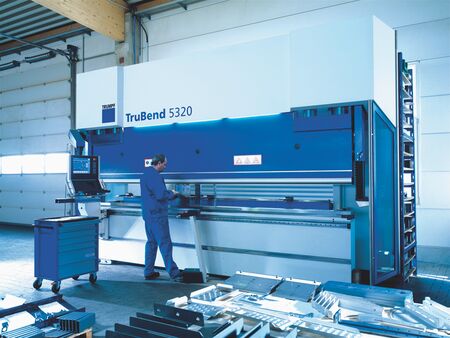
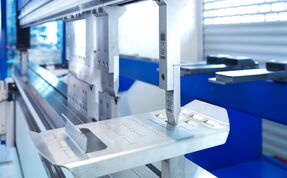
- CNC press brake with laser-controlled angle sensing (4,400 mm, 320 t)
- CNC punching machine with tool changer
- CNC turning machine with driven tools (length up to 1,000 mm, Ø up to 500 mm)
- CNC machining centre (2,100 x 860 x 910 mm)
- MAG welding robot cell (1,200 x 1,000 mm)
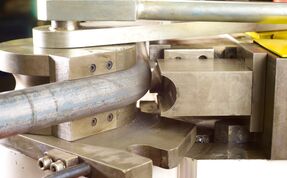
- Mandrel bending machine (tube Ø up to 60 mm)
- Through-feed blasting system (1,500 x 500 mm)
- Deburring machine (sheets up to 100 mm, width 1,500 mm)
Components
Inside the production
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Laser cutting (fibre laser)Machining | – | 4,000 mm × 2,000 mm | – | – | Steel, Metals |
| Saw cutting (CNC sawing machines)Machining | tightest tolerances | 500 mm × 300 mm | – | – | Steel (various steel grades) |
| Oxy-fuel flame cuttingMachining | – | 6,000 mm × 2,000 mm | – | – | Steel |
| CNC folding (laser-controlled angle sensing, mark-free bending)Forming | – | 4,400 mm | – | – | – |
| Punching (CNC punching)Forming | – | – | – | – | Sheet metal |
| CNC turning (turning machines with driven tools, bar magazine)Machining | – | 1,000 mm × 500 mm (diameter; bar material | – | Small, medium and large series | Metals |
| CNC milling (machining centres)Machining | – | 2,100 mm × 860 mm × 910 mm | – | – | Metals, Plastic, Wood |
| Welding (MIG, MAG, TIG, spot welding; MAG welding robot cell)Joining | – | 1,200 mm × 1,000 mm | 2,000 kg | – | Metals |
| Tube bending (mandrel bending process, cold forming)Forming | – | 60 mm (tube diameter) | – | – | Tubes |
| Deburring (brushing, filing, countersinking, grinding, milling, vibratory finishing, thermal,Surface | – | 1,500 mm (deburring machine, sheets up | – | – | Metals |
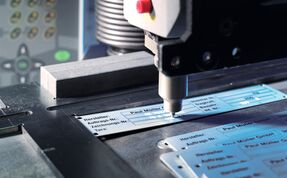
| Marking (needle embosser, colour printing, labelling)Surface | – | – | – | – | – |
| Blasting (through-feed blasting system, manual blasting with glass beads, corundum)Surface | – | 1,500 mm × 500 mm | – | – | Metals |
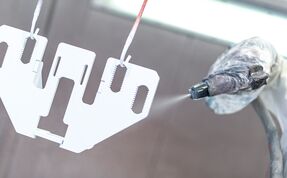
| Wet painting (one-/two-component) and powder coatingSurface | – | 6,000 mm | – | – | Metals |
| Assembly of mechanical assemblies incl. electrical, pneumatic and hydraulic drivesAssembly | – | – | – | – | – |
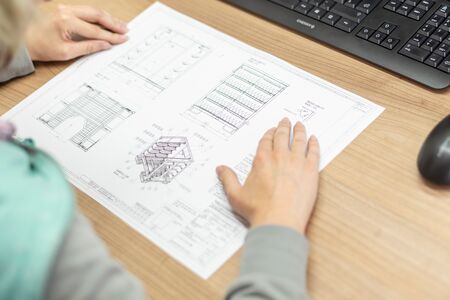
| Design (3D design workstations, .dxf, .dwg, .ai, CAD)Engineering | – | – | – | – | – |
| Quality assurance / dye penetrant testing of weld seams according to DIN EN ISO 3452-1Testing | – | – | – | – | – |
11 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| Fibre laser cutting system | – | – | 4,000 x 2,000 mm (oversize formats), sheets up to 25 mm thickness, up to 140 m/min | – | Cunewalde |
| CNC sawing machine | – | – | Diameter up to 400 mm, profile size up to 500 x 300 mm | – | Cunewalde |
| CNC flame cutting machine | – | – | Max. sheet size 6,000 x 2,000 mm, thickness up to 360 mm | – | Cunewalde |
| CNC press brake (laser-controlled angle sensing) | – | – | Max. folding length 4,400 mm, press force up to 320 t | – | Cunewalde |
| CNC punching machine (punching machines with tool changer) | – | – | – | – | Cunewalde |
| CNC turning machine with driven tools | – | – | Length up to 1,000 mm, diameter up to 500 mm; bar magazine up to 70 mm diameter | – | Cunewalde |
| CNC machining centre (milling) | – | – | Max. machining dimension 2,100 x 860 x 910 mm | – | Cunewalde |
| MAG welding robot cell | – | – | 1,200 x 1,000 mm | – | Cunewalde |
| Mandrel bending machine | – | – | Tube diameter up to 60 mm | – | Cunewalde |
| Through-feed blasting system | – | – | Max. component size 1,500 x 500 mm | – | Cunewalde |
| Deburring machine | – | – | Sheet thickness up to 100 mm, max. width 1,500 mm | – | Cunewalde |
Additional services
Reference customers
Quality
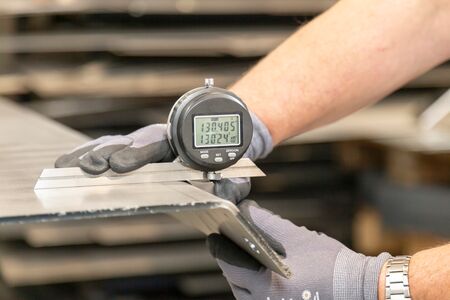
All manufacturing steps are monitored by means of precise machine technology; inspection and measuring equipment of the latest generation is used. Weld seams are inspected where required by means of dye penetrant testing according to DIN EN ISO 3452-1; the quality management system is certified according to DIN EN ISO 9001:2015.
| Evidence | Cunewalde |
|---|---|
| DIN EN ISO 9001:2015 | |
| EN 1090-2:2018+A1:2024 |
History
- 1992
Foundation of the company Gerätebau Eberhard Härtwig in Cunewalde by Eberhard Härtwig.
- 1998
Foundation of the company Metall- und Blechbearbeitung Andreas Härtwig by Andreas Härtwig.
- 2006
Merger of the two companies to form Härtwig Maschinenbau GmbH & Co. KG.
- 2010
Participation in the iBoxII research project (modular container system with RFID technology, TU Chemnitz, funded by the Free State of Saxony/EFRE).
- 2015
Support for the restoration of the church bells of the Cunewalde church.
- 2019
Start of participation in the Zwanzig20-smart³ joint project AdapStiff (lead management Fraunhofer IWU) on integration into forming tools.