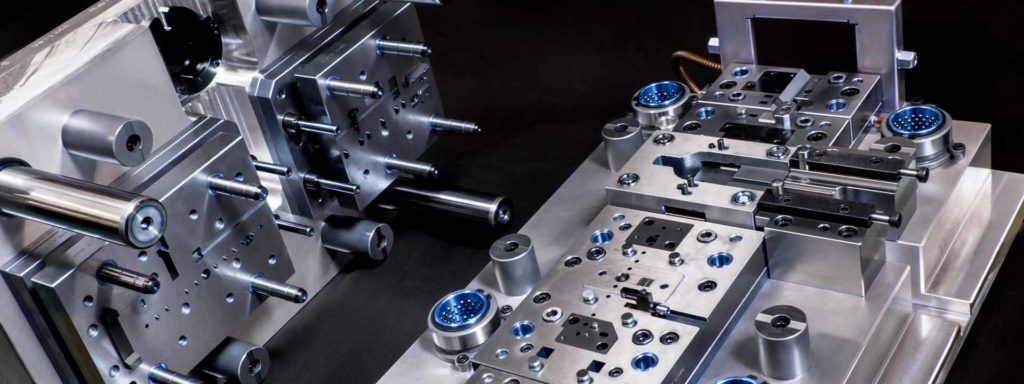
Halter AG manufactures stamping and bending tools, stamped parts, laser cuts and EDM work from one-off parts to large series.
Halter AG Werkzeugbau
HombrechtikonNew on Amplifa
About Halter AG Werkzeugbau
Halter AG Werkzeugbau is an owner-managed Swiss family business in Hombrechtikon in the canton of Zurich. Since 1948, the company has been developing and manufacturing stamping and bending tools – from simple cut-off and compound tools to progressive compound dies with tool lengths of up to approx. 900 mm – and operates its own stamping shop with press forces of 150 to 1,200 kN for sheet thicknesses of 0.2 to 4 mm. The service portfolio also includes laser cutting with a 1.5 kW fiber laser (working area 1,300 x 800 mm) and precision foils from 0.1 mm for compensation and regrinding shims, laser marking, mechanical CNC machining as well as die-sinking and wire EDM. Materials processed include steel, stainless steel, aluminium, copper, brass, precious metals, spring steels and spring bronzes as well as selected plastics; a focus is on machining copper and brass for electrical engineering. In addition, the company offers reworking, cleaning, assembly, jig and fixture building, design, tool maintenance and delivery concepts such as Kanban. Customers come from precision instruments, weighing systems, the electrical industry, metrology, locking systems and aviation.
- Site
- Hombrechtikon
- Processes
- Toolmaking of stamping and bending tools (progressive compound, compound dies, bending tools,, Building of fixtures (assembly, press, inspection and measuring fixtures), Stamping/laser and stamped parts (cutting, bending, embossing, thread forming), Sheet thickness stamping 0.2–4 mm, Stamping shop press force 150–1,200 kN, Die-sinking EDM (EDM), Wire EDM (EDM), Mechanical machining (CNC manufacturing)
- Materials
- Steel, Stainless steel, Aluminium, Copper, Brass, Precious metals, Spring steels and spring bronzes, Plastics (selected)
- Certificates
- ISO 9001, ISO 14001, EcoVadis Gold
- Founded
- 1948
- Industries
- Precision instruments, Weighing systems, Electrical industry, Electrical engineering, Metrology, Microscopy/precision optics
- 01
Design and Engineering
- 02
Toolmaking (stamping and bending tools, progressive compound dies)
- 03
Stamping, laser cutting, CNC machining, EDM
- 04
Reworking, cleaning, finishing via partners
- 05
Assembly, press-fitting, riveting
- 06
Quality inspection and documentation
- 07
Packaging and delivery concepts (Kanban, consignment warehouse)
Materials and Processes
Steel
Toolmaking and stamped parts, up to approx. 8 mm thickness in laser cutting.
Stainless steel
For precision and stamped parts as well as laser cuts up to approx. 3 mm.
Aluminium
Material for tools, fixtures and thin-walled sheet parts.
Copper
Focus for applications in electrical engineering, including milling of copper busbars.
Brass
Key material of the stamping shop, especially for electrical engineering.
Spring steels and spring bronzes
For spring precision components and laser cuts.
Precious metals
Precious metals are processed for specialised stamping applications.
Plastics (selected)
Plastic parts are also stamped for selected applications.
Precision foil 1.4310
From 0.1 mm for compensation and regrinding shims ex stock.
1.4034
Foil and sheet in several thicknesses for compensation and grinding shims.
Ck75
Hardened spring steel for compensation shims up to 3.0 mm.
Sites
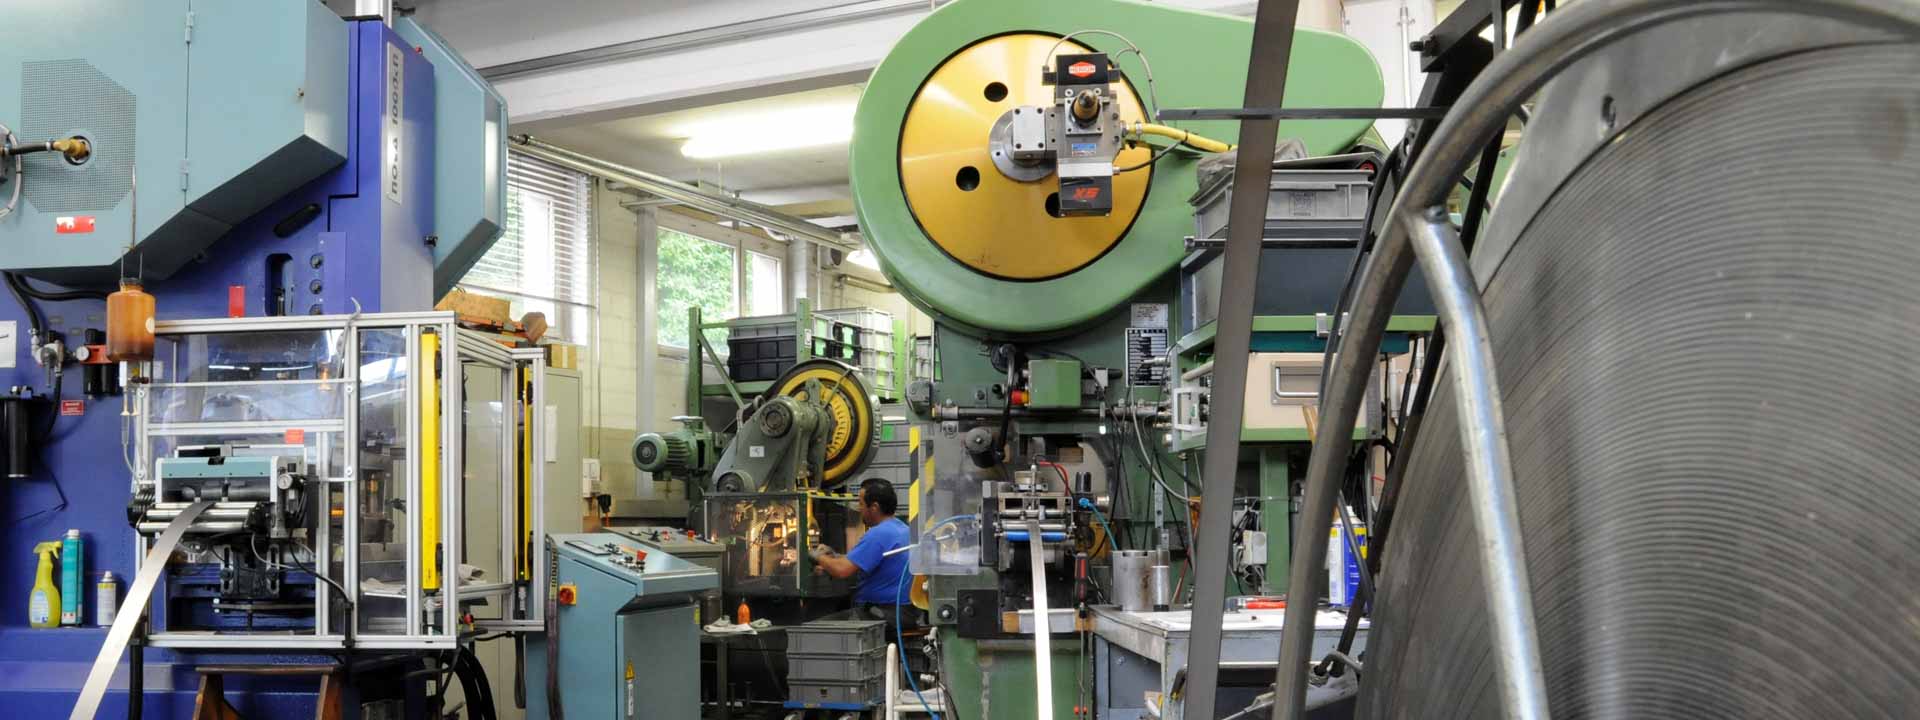
Hombrechtikon
CHHeadquarters, toolmaking, stamping shop, manufacturing
- Lot size
- 10 to 10,000,000+ parts
- Materials
- Copper, brass, steel, stainless steel, spring steels, spring bronzes, aluminium, precious metals, plastic
- Stamping presses
- C-frame presses 150–1,200 kN
- Fiber laser cutting machine 1.5 kW (1,300 x 800 mm)
- Fiber laser marking machine 50 W (150 x 150 mm)
- Die-sinking EDM machine
- Wire EDM machine
- CNC machining machines
- HEMO vacuum cleaning system (solvent/ultrasonic)
Components and Manufacturing Services
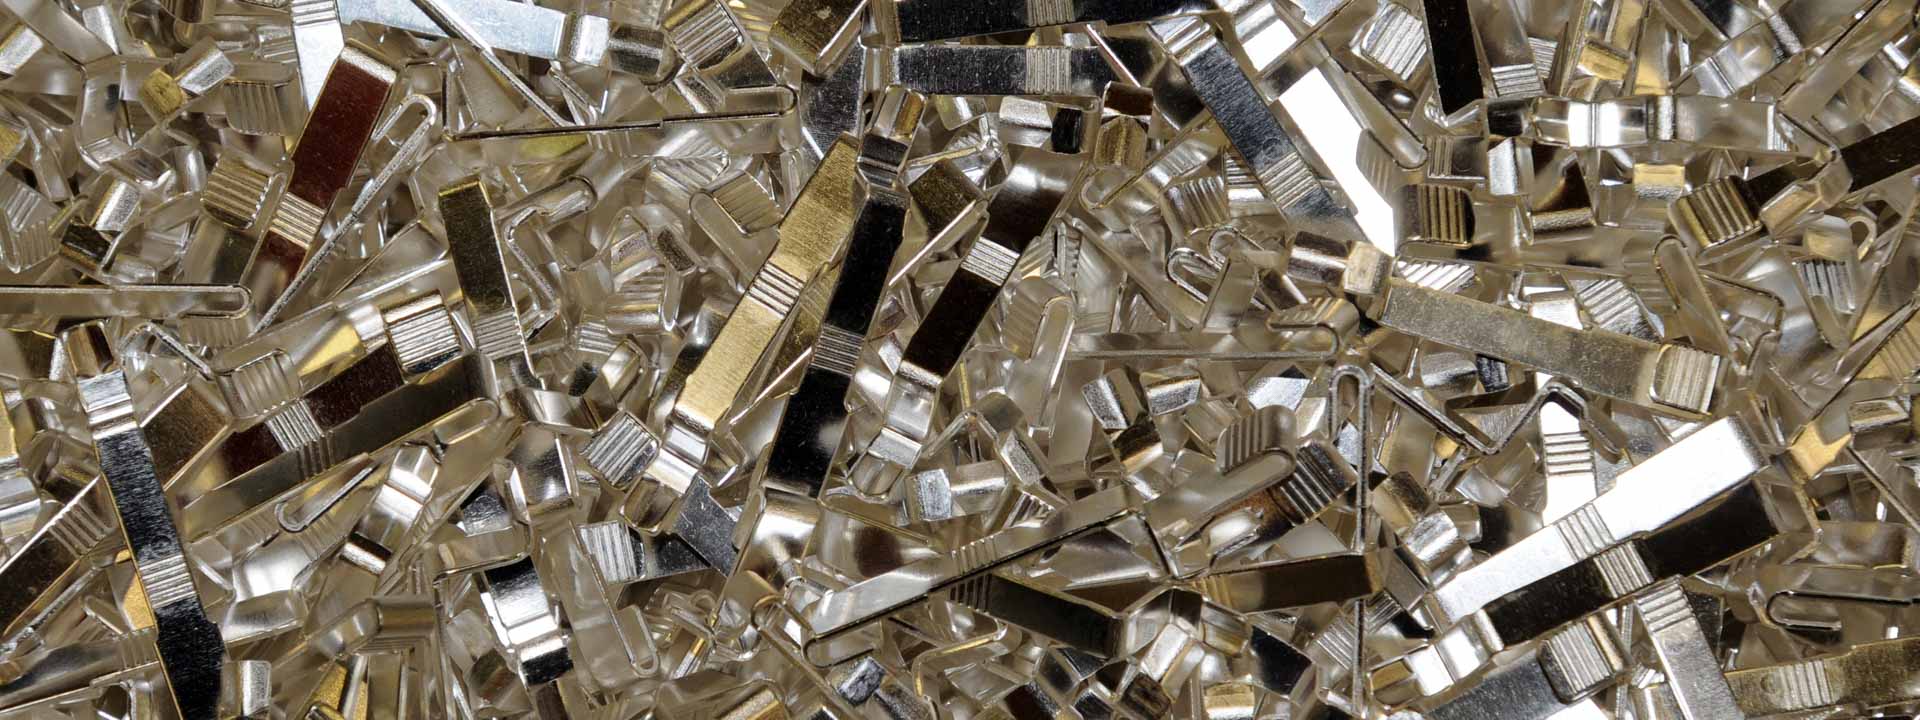
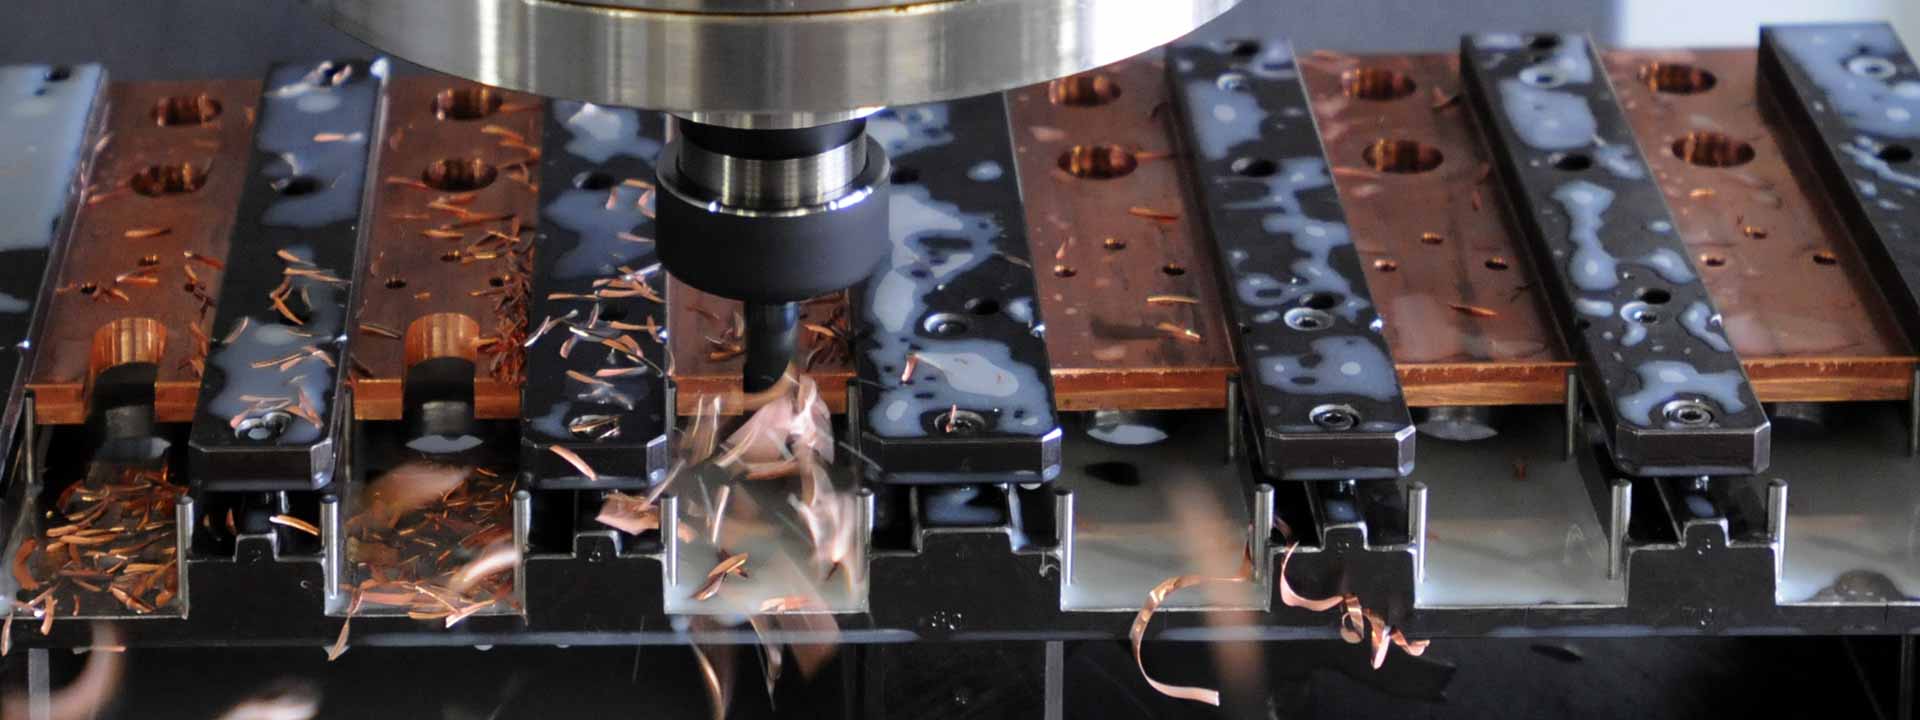
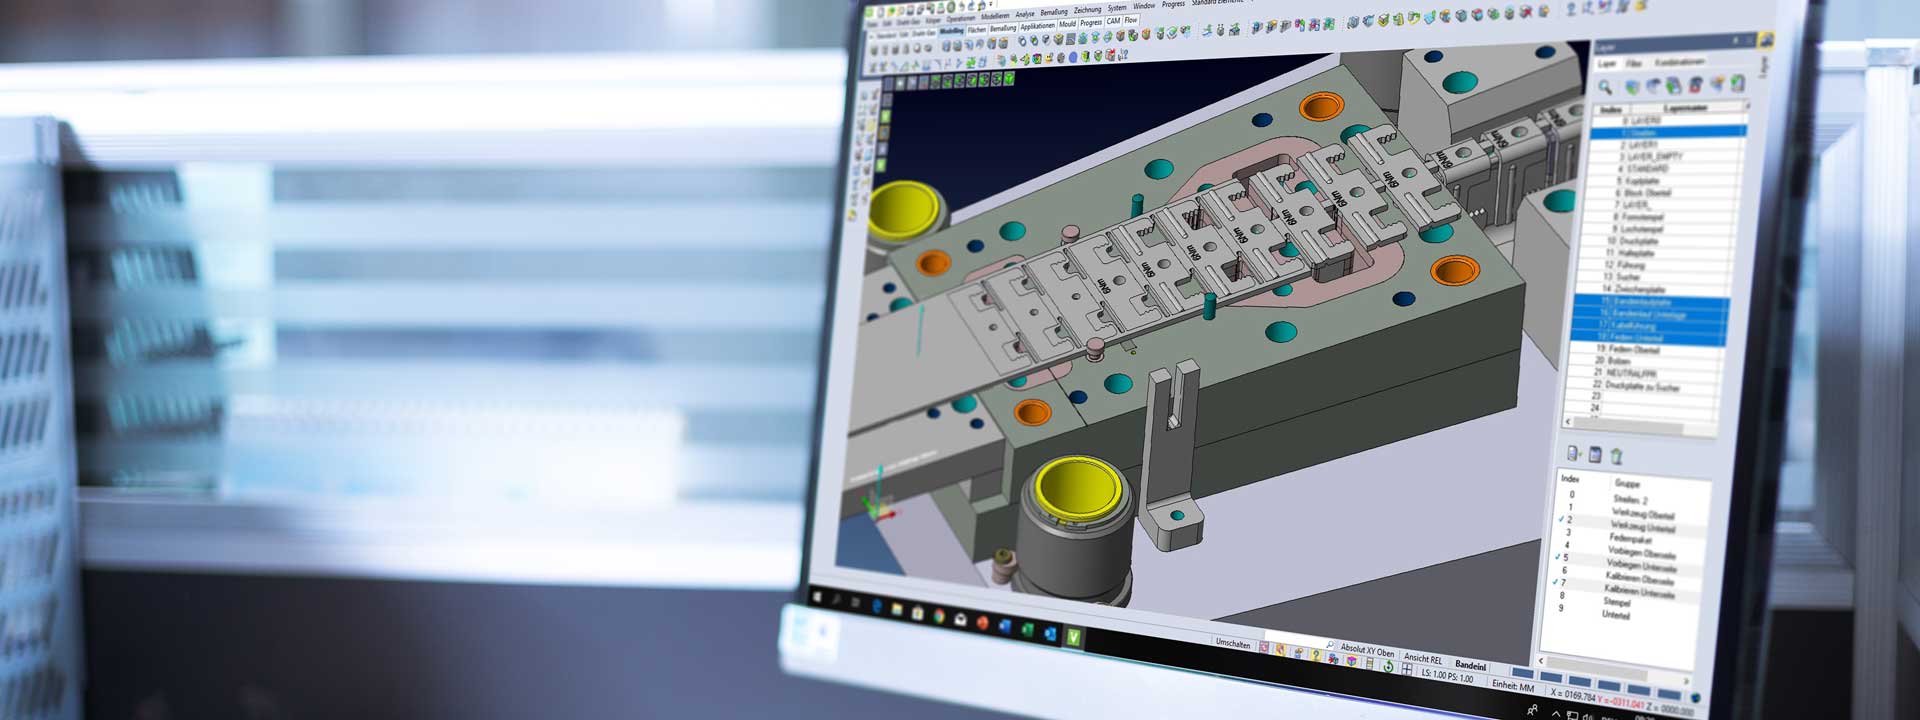
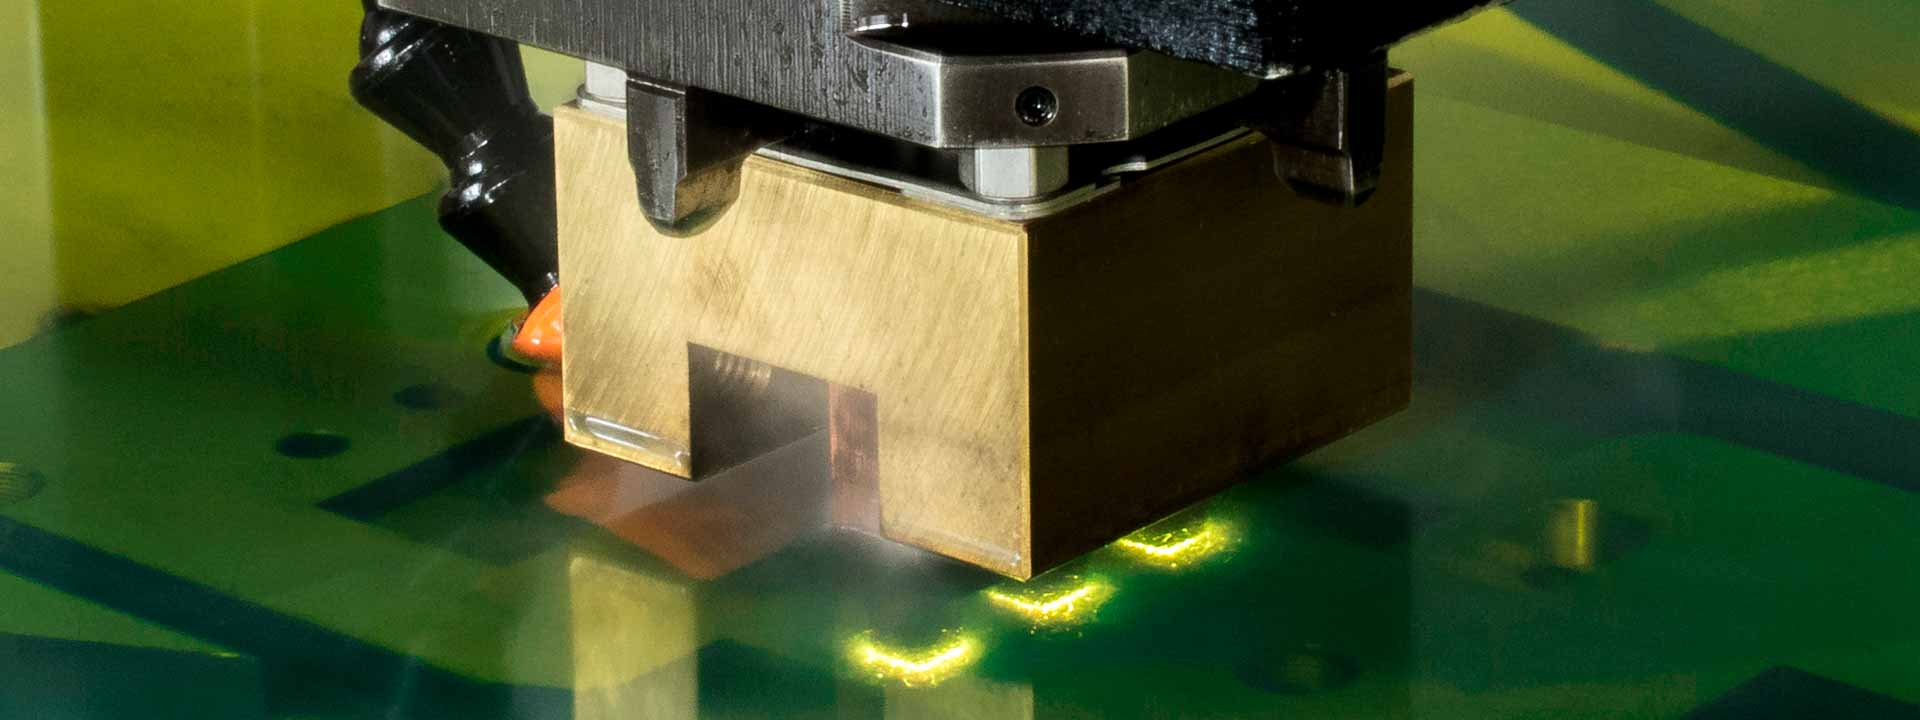
Inside the production
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Toolmaking of stamping and bending tools (progressive compound, compound dies, bending tools,Toolmaking/Clamping | – | approx. 900 mm tool length | – | – | Steel, Stainless steel, Aluminium, Copper, Brass, Precious metals, Spring steels, Spring bronzes, Plastic |
| Building of fixtures (assembly, press, inspection and measuring fixtures)Engineering | – | – | – | – | Steel, Aluminium |
| Stamping/laser and stamped parts (cutting, bending, embossing, thread forming)Forming | – | Strip width up to 250 mm | – | 10 – 10,000,000+ | Copper, Brass, Steel, Stainless steel, Spring steels, Spring bronzes, Aluminium, Precious metals, Plastic |
| Sheet thickness stamping 0.2–4 mmForming | – | – | – | – | Metal |
| Stamping shop press force 150–1,200 kNForming | – | – | – | – | Metal |
| Die-sinking EDM (EDM)Machining | – | – | – | – | Metal |
| Wire EDM (EDM)Machining | – | – | – | – | Metal |
| Mechanical machining (CNC manufacturing)Machining | – | – | – | – | Metal |
| Laser cutting (fiber laser 1.5 kW)Cutting | approx. ±0.05 mm | 1300 mm × 800 mm | – | – | Steel, Stainless steel, Spring steel, Copper, Brass, Aluminium |
| Laser cutting steel up to approx. 8 mm, stainless steel/spring steel up to approx. 3 mmCutting | – | – | – | – | Steel, Stainless steel, Spring steel |
| Laser marking/laser engraving (50 W fiber laser)Surface | – | max. 300 mm × 150 mm × 150 mm | – | – | Metals, anodised aluminium, INOX |
| Compensation and regrinding shims (precision foils from 0.1 mm)Cutting | – | – | – | – | 1.4310, 1.4034, Ck75 |
| Reworking: vibratory grinding/trowalisingSurface | – | – | – | – | Metal |
| Manual deburring and grindingSurface | – | – | – | – | Metal |
| Aqueous parts cleaningSurface | – | – | – | – | Metal |
| Vacuum cleaning with solvent and ultrasonics (HEMO)Surface | – | – | – | – | Metal |
| Thread cutting and thread forming M1.5–M20Machining | – | – | – | – | Metal |
| Drilling, reaming, countersinkingMachining | – | – | – | – | Metal |
| Assembly, press-fitting, rivetingAssembly | – | – | – | – | Metal |
| Surface treatment via partners: galvanising, nickel plating, tin plating, silver plating, goldSurface | – | – | – | – | Metal |
| Welding work (via partners)Joining | – | – | – | – | Metal |
| Design and engineering (from idea to documentation)Engineering | – | – | – | – | – |
| Tool take-over, servicing and maintenance of stamping, bending and progressive compound toolsEngineering | – | – | – | – | Metal |
| Acceptance and series inspection reports (EMPB, PPAP, inspection records, EN 10204 3.1)Testing | – | – | – | – | – |
8 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| Fiber laser cutting machine (1.5 kW) | – | – | 1300 x 800 mm | – | Hombrechtikon |
| Fiber laser marking machine (50 W) | – | – | 150 x 150 mm | – | Hombrechtikon |
| Stamping presses | – | – | – | – | Hombrechtikon |
| C-frame presses (C-frame presses, 150–1,200 kN) | – | – | – | – | Hombrechtikon |
| HEMO vacuum cleaning system (solvent/ultrasonic) | HEMO | – | – | – | Hombrechtikon |
| Die-sinking EDM machine | – | – | – | – | Hombrechtikon |
| Wire EDM machine | – | – | – | – | Hombrechtikon |
| CNC machining machines (mechanical machining) | – | – | – | – | Hombrechtikon |
Additional services
Reference customers
Quality and Sustainability
Quality begins throughout the entire manufacturing process: stamping processes are monitored with systems for monitoring feed, part ejection, double-sheet and strip-end detection as well as stamping force; components are inspected with optical and tactile measuring instruments. Inspection documentation includes EMPB, PPAP, series inspection reports and EN 10204 3.1 material certificates.
| Evidence | Hombrechtikon |
|---|---|
| ISO 9001 | |
| ISO 14001 | |
| EcoVadis Gold |
Company History
- 1948
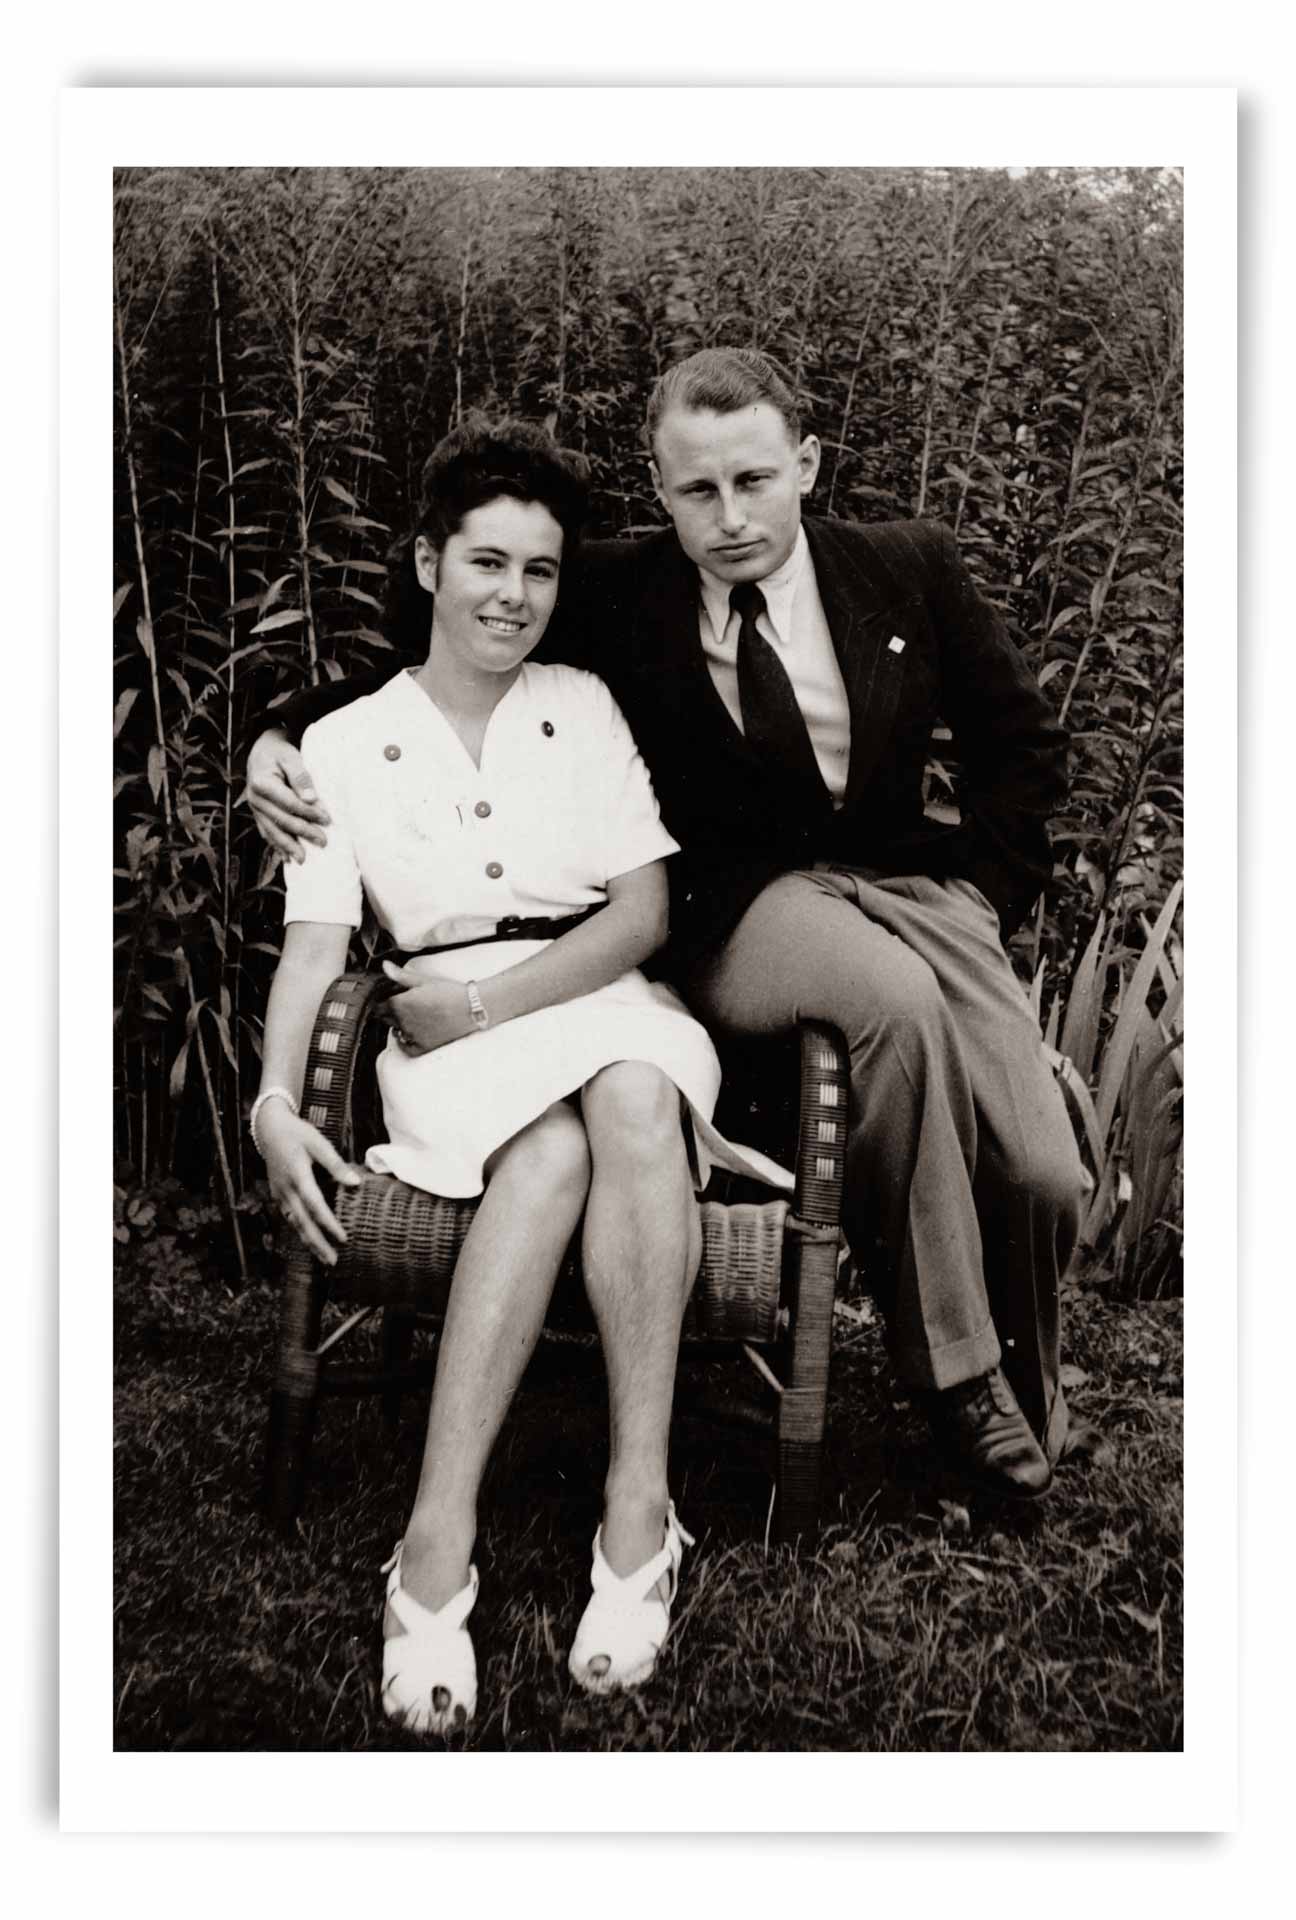
Founded as 'A. Halter Werkzeugbau' by Armin Halter in Feldbach, canton of Zurich
- 1951
Move to a new factory building at Oetwilerstrasse 53 in Hombrechtikon
- 1980
Move to a new building at Oetwilerstrasse 57
- 1982
Change of legal form to a stock corporation (Aktiengesellschaft) under today's name 'Halter AG Werkzeugbau'
- 1995
Erich Halter takes over the majority shares and the management
- 1999
Stefan Halter, third generation, joins the family business
- 2012
Stefan Halter takes over the majority shares and the management