Precision cutting tools made of carbide and ultra-hard materials: grooving, broaching, milling, drilling and turning.
Hartmetall-Werkzeugfabrik Paul Horn GmbH
Tübingen (headquarters) · Tübingen, Dußlinger Weg (Horn Hartstoffe GmbH)New on Amplifa
About HORN
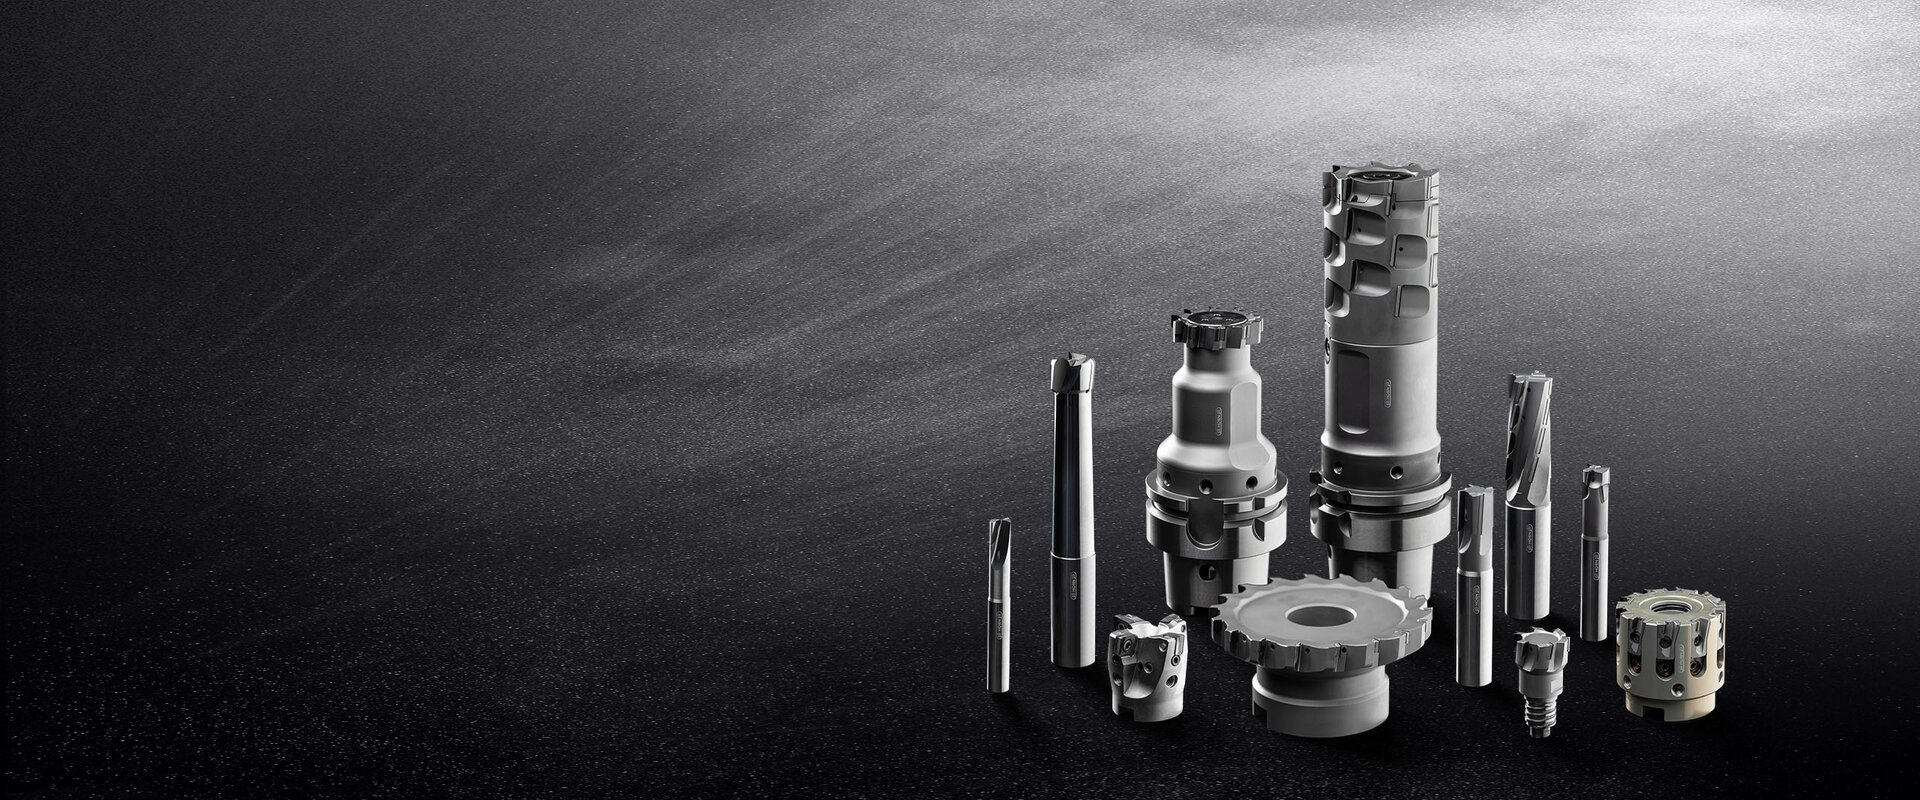
Hartmetall-Werkzeugfabrik Paul Horn GmbH is a manufacturer of precision cutting tools headquartered in Tübingen. The company produces tools for grooving and groove forming (speed forming), broaching, slot broaching, milling, drilling, turning, gear skiving and hobbing, as well as tools made of ultra-hard materials such as PCD, CVD diamond, MCD and CBN. The value chain comprises four pillars: in-house research and development, in-house coating technology (Coating Center), in-house carbide production (blanks, semi-finished products and wear parts) and in-house manufacturing technologies. With the Greenline system, HORN delivers custom tool inserts within five working days. More than 25,000 standard tools and over 150,000 sold custom solutions serve, among others, the automotive industry, aerospace, medical technology, tool and mold making, chemicals, hydraulics and the jewelry industry. The company supplies customers in 70 countries on all continents and, with around 950 employees at the Tübingen site, is its largest industrial employer.
- Site
- Tübingen
- Processes
- Broaching (groove forming, speed forming), Slot broaching from inner diameter 9 mm, Carbide milling cutters (DP/DS systems for material groups), PCD milling for aluminum machining, Carbide drills (D1122), Broaching of splines/grooves (technical request broaching: groove lengths, bore diameter, shank, Gear skiving / gear milling / gear hobbing, Hard turning/hard milling with CBN tooling
- Materials
- PCD (polycrystalline diamond), CVD thick-film diamond (99.9% diamond), Single-crystal diamond, cubic boron nitride, Carbide, Aluminum alloys (PCD machining), Steel (solid carbide drills DS systems: unalloyed/high-strength/heat-treated/rust-resistant/titanium, Cast materials (D1122 drilling system)
- Certificates
- DIN EN ISO 9001, VDA 6.4, DIN EN ISO 14001:2015, DIN EN ISO 50001:2018, ISO 45001, DIN EN ISO 14001, ISO 50001
- Founded
- 1969
- Employees
- 1500
- Industries
- Automotive, Aerospace, Medical technology, Tool and mold making, Chemicals, General mechanical engineering
- 01
Research & Development
- 02
In-house carbide production (blanks, semi-finished products, wear parts)
- 03
Tool manufacturing
- 04
Coating in the in-house Coating Center
- 05
Testing & Demonstration Center
- 06
Sales & technical support (cutting data calculator, HORN Academy)
Materials & Cutting Materials
Carbide
Base material for precision cutting tools; in-house production of carbide semi-finished products and wear parts.
Polycrystalline Diamond (PCD)
For machining of aluminum alloys, carbide green compacts and composite materials.
CVD thick-film diamond (99.9% diamond)
Cutting material chemically produced from the gas phase; shows its strengths in machining sintered carbide.
Single-Crystal Diamond
For high-gloss polished surfaces with roughness in the nanometer range.
Cubic Boron Nitride
As the second-hardest material, mainly for machining hardened materials in hard turning and hard milling.
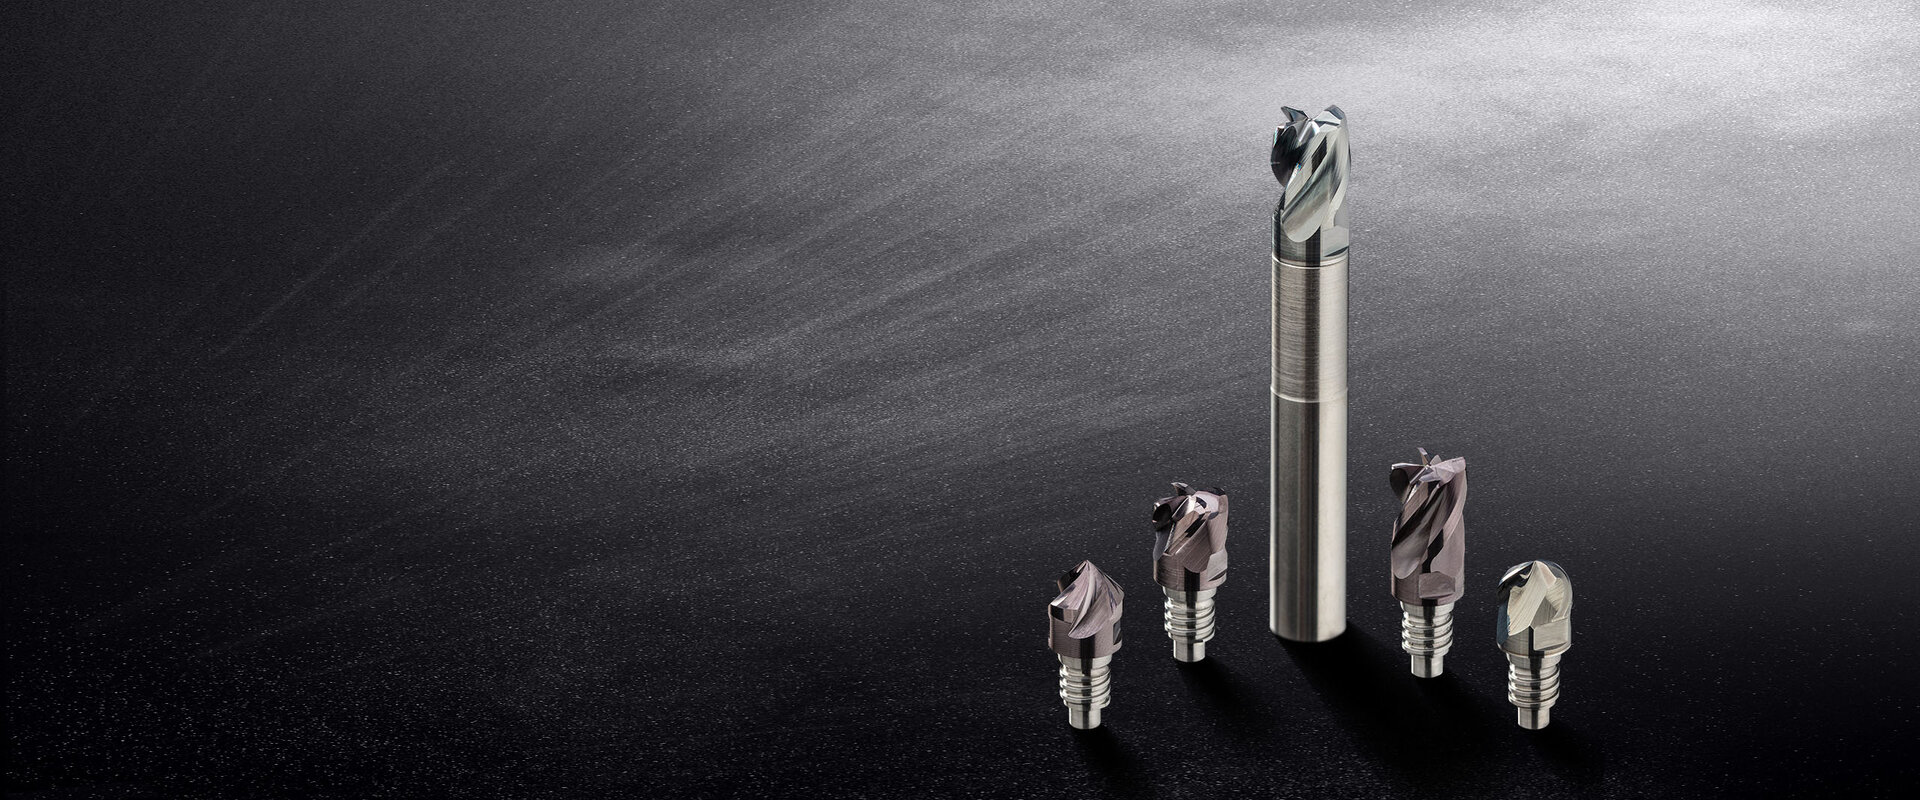
Solid carbide milling cutters (DP/DS systems)
Milling cutter programs for unalloyed, high-strength, heat-treated and rust-resistant steels, titanium, cobalt-chromium and aluminum.
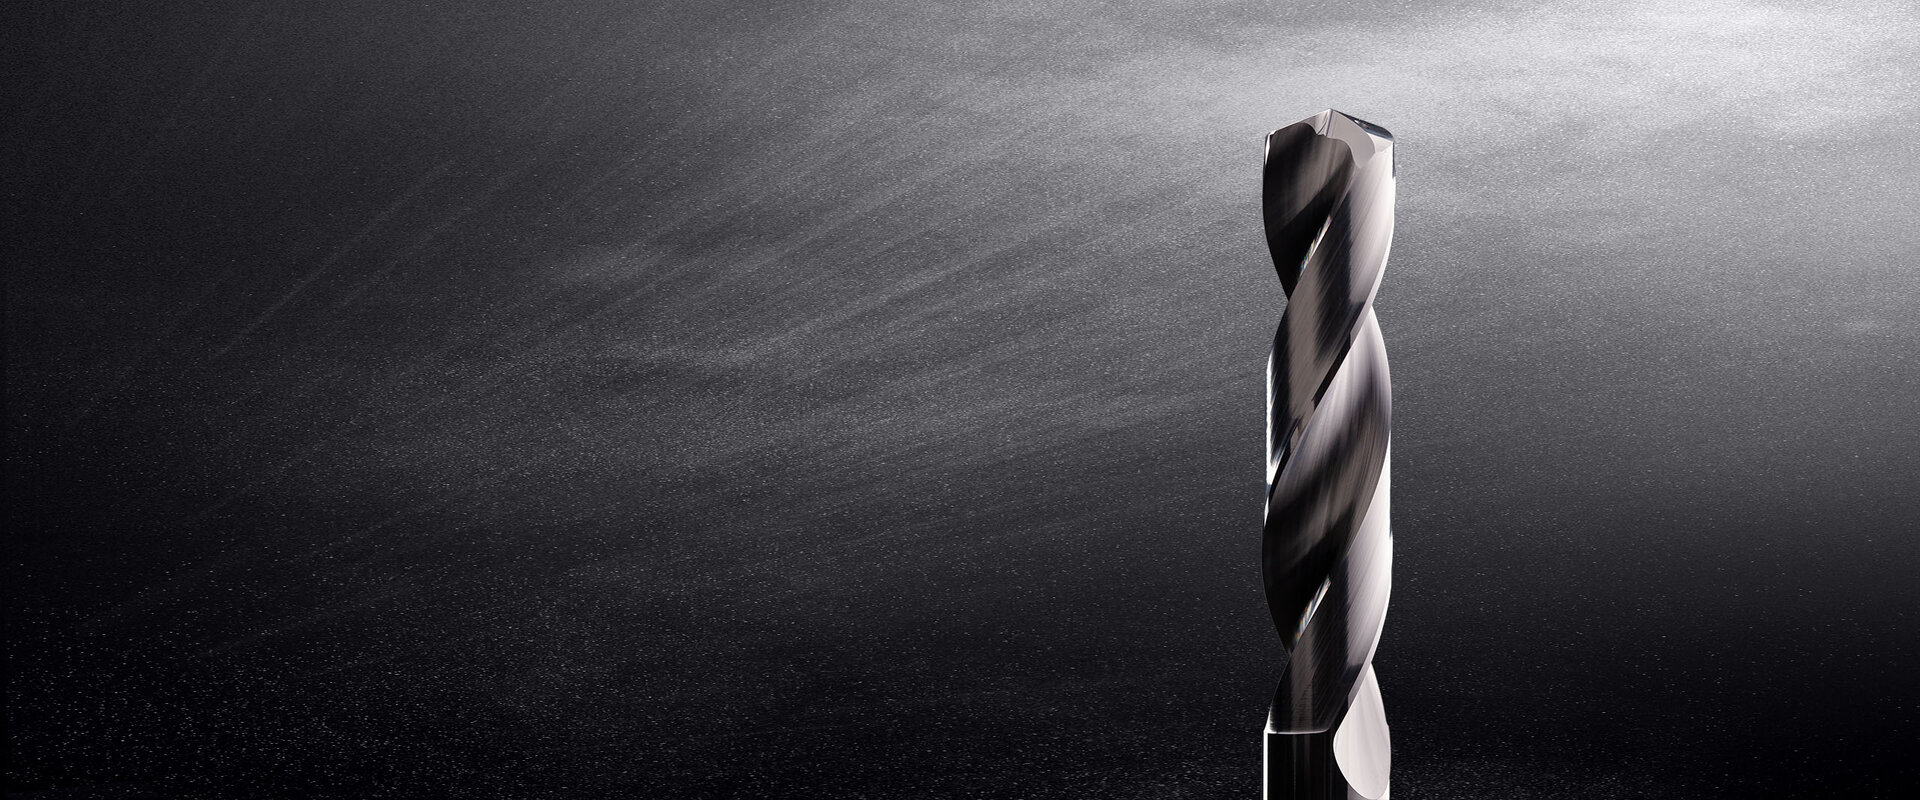
Solid carbide drill (System D1122)
For productive and economical drilling in steel and cast materials.
Sites
Tübingen (Horn-Straße 1)
DEHeadquarters, production, administration, Demonstration Center, Coating Center
- Materials
- Carbide, PCD, CVD-D, MCD, CBN
- Turn-mill center
- Lathe
- Milling machines (2)
- Sliding-headstock lathe
- Coating center
Tübingen (Dußlinger Weg)
DEProduction site of Horn Hartstoffe GmbH: carbide pressing processes, semi-finished products and wear parts
- Materials
- Carbide
- Pressing processes for carbide production
Tool Systems & Components
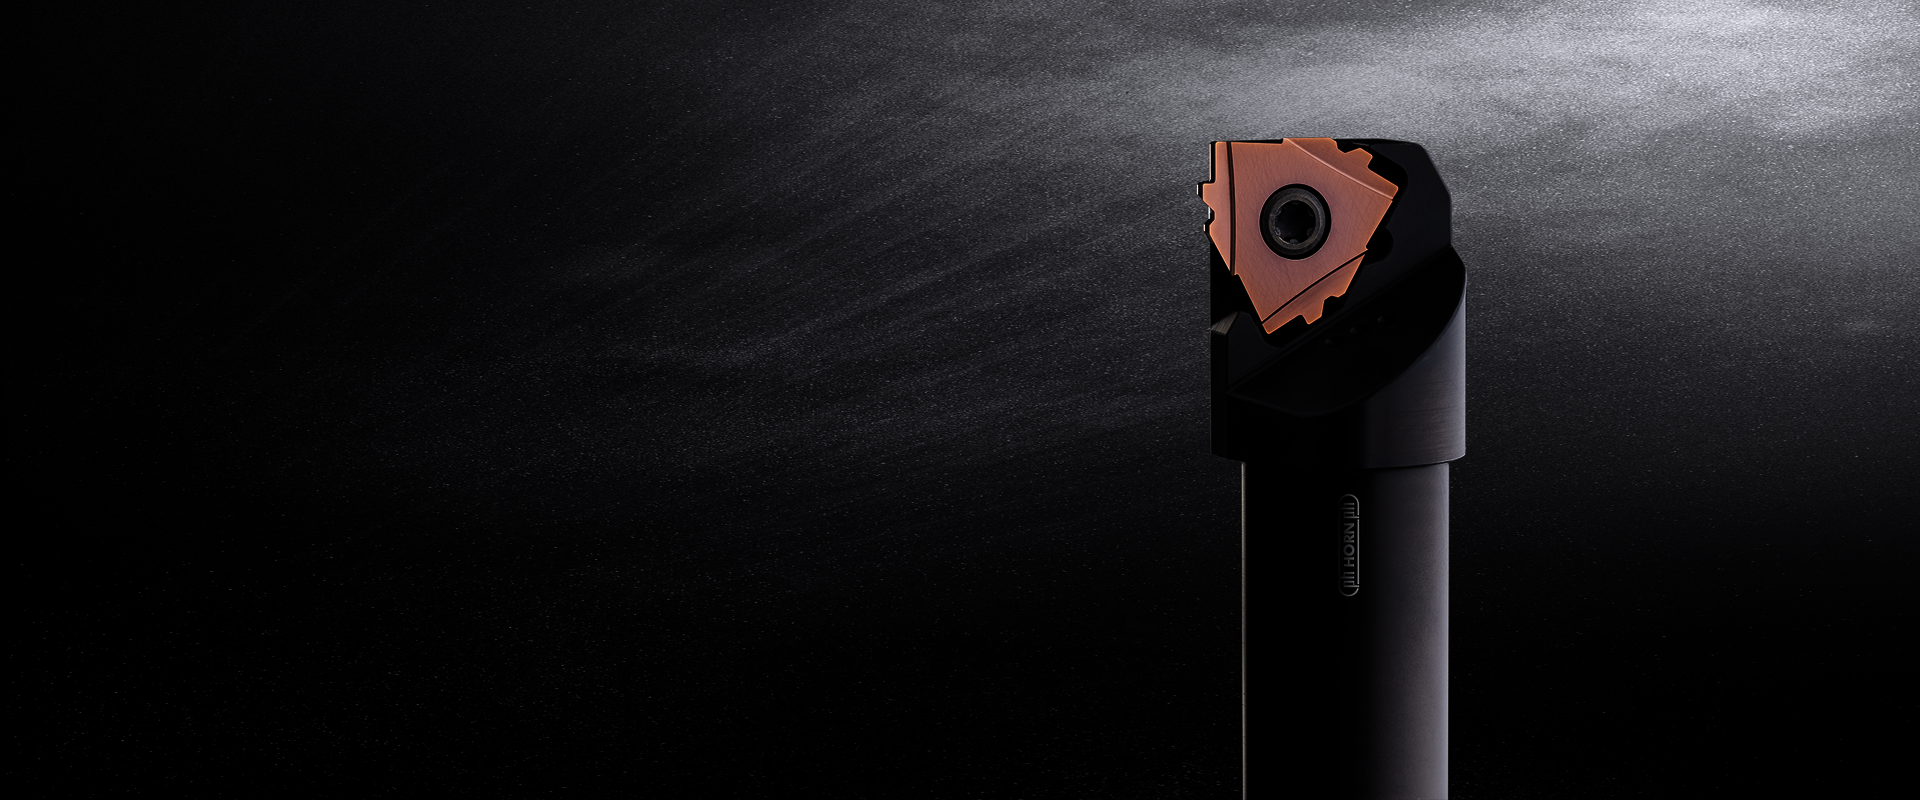
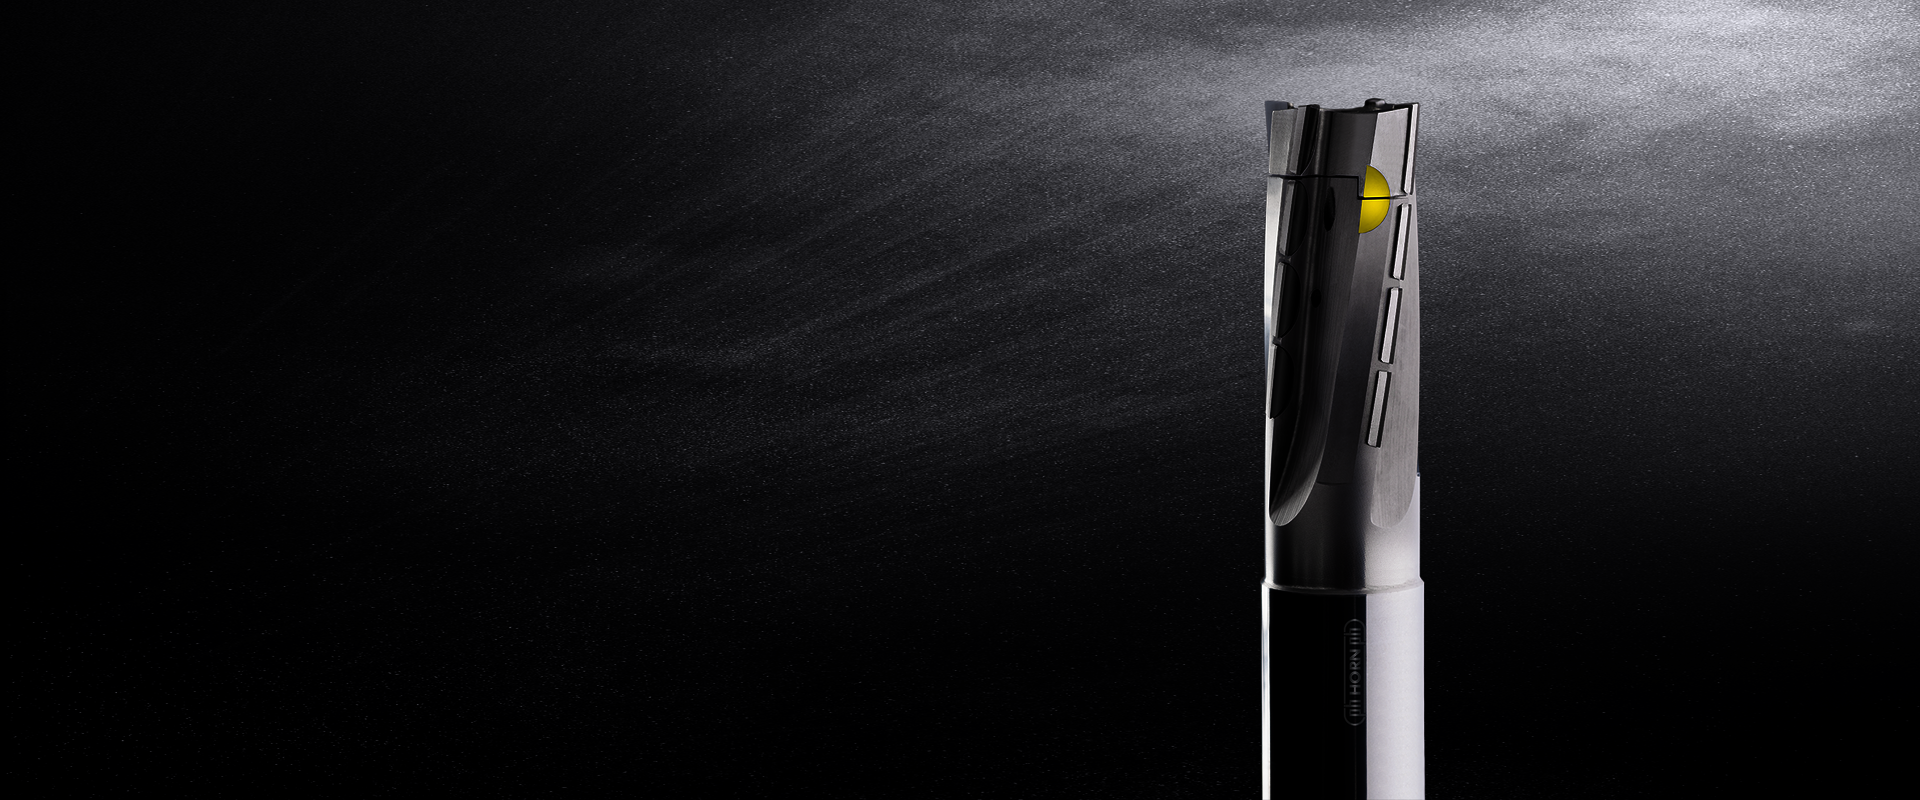
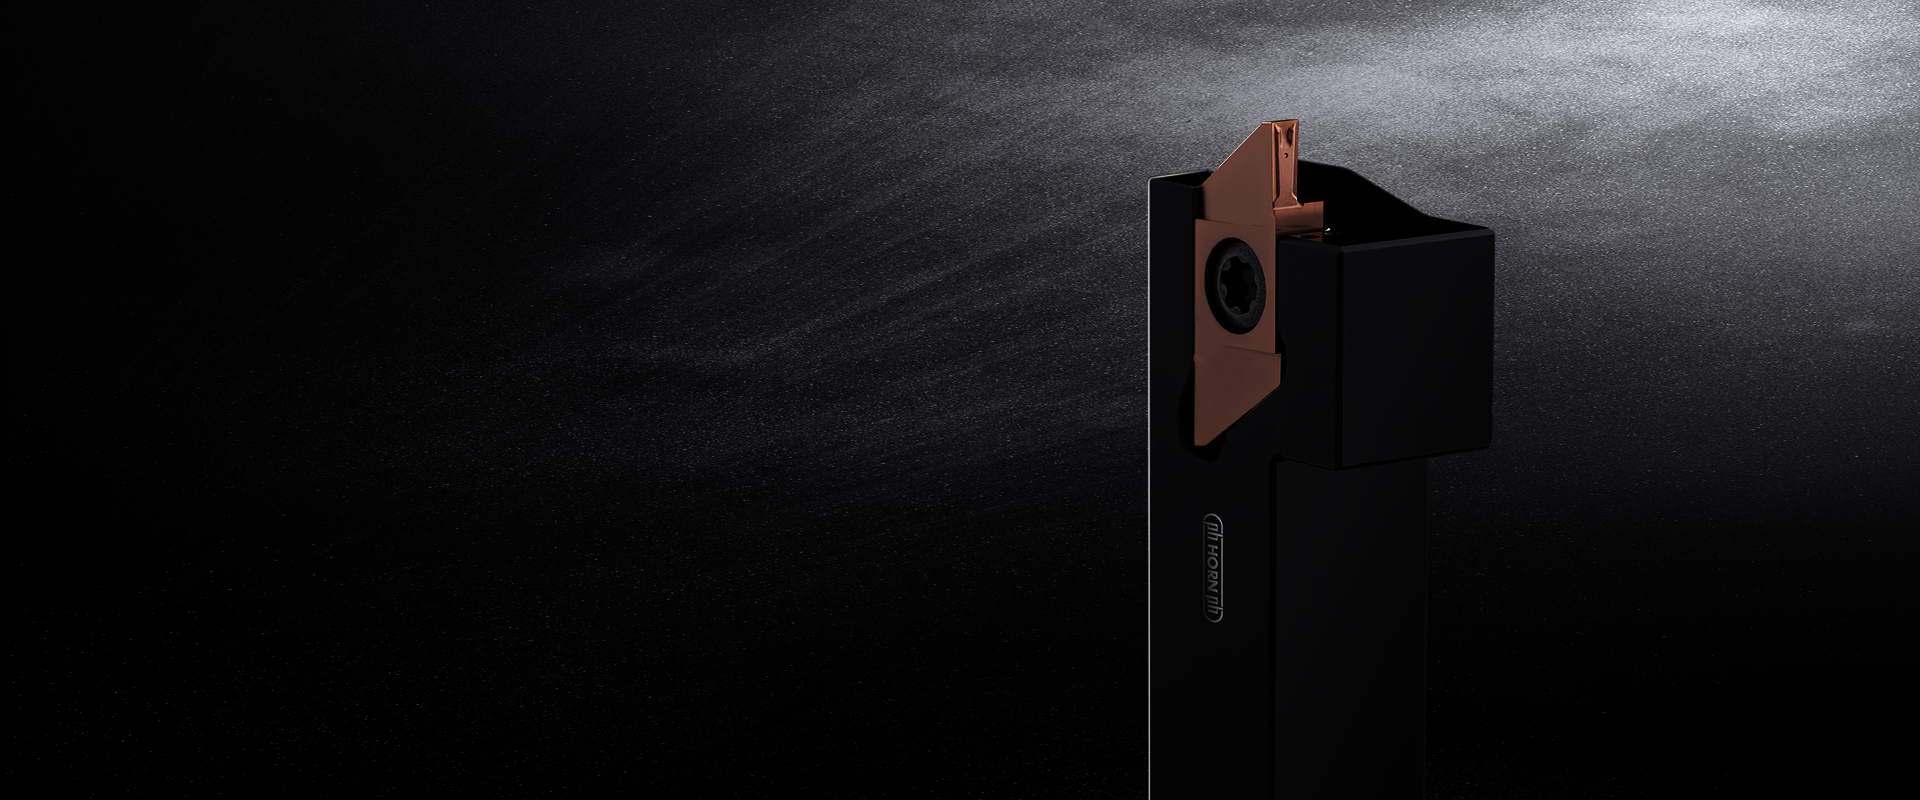
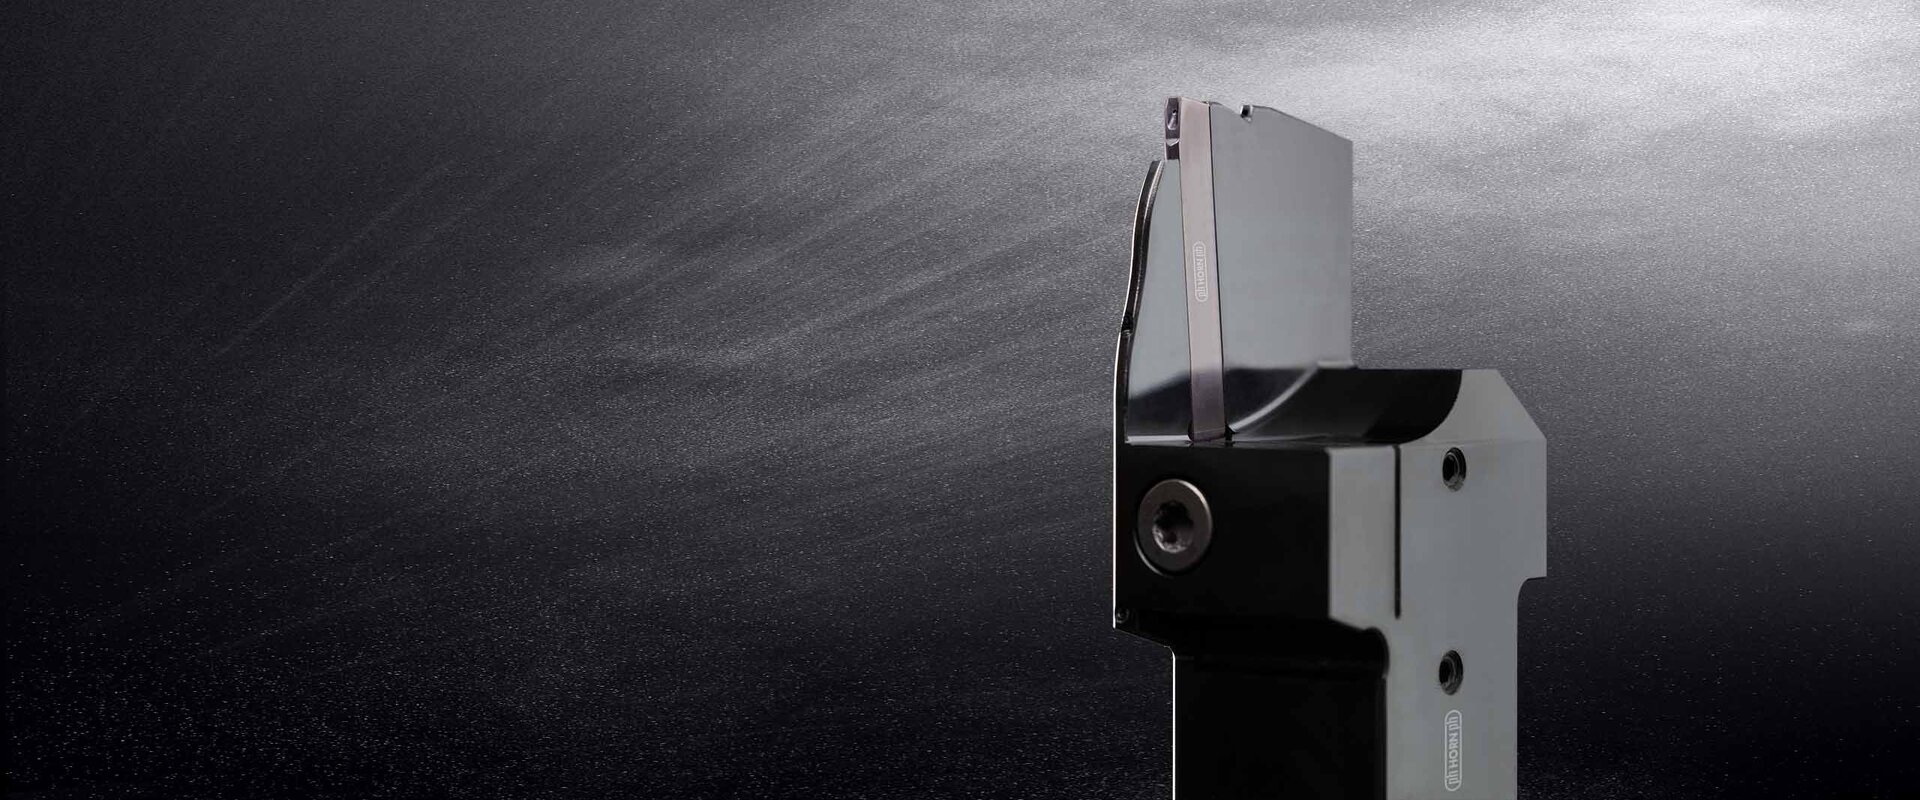
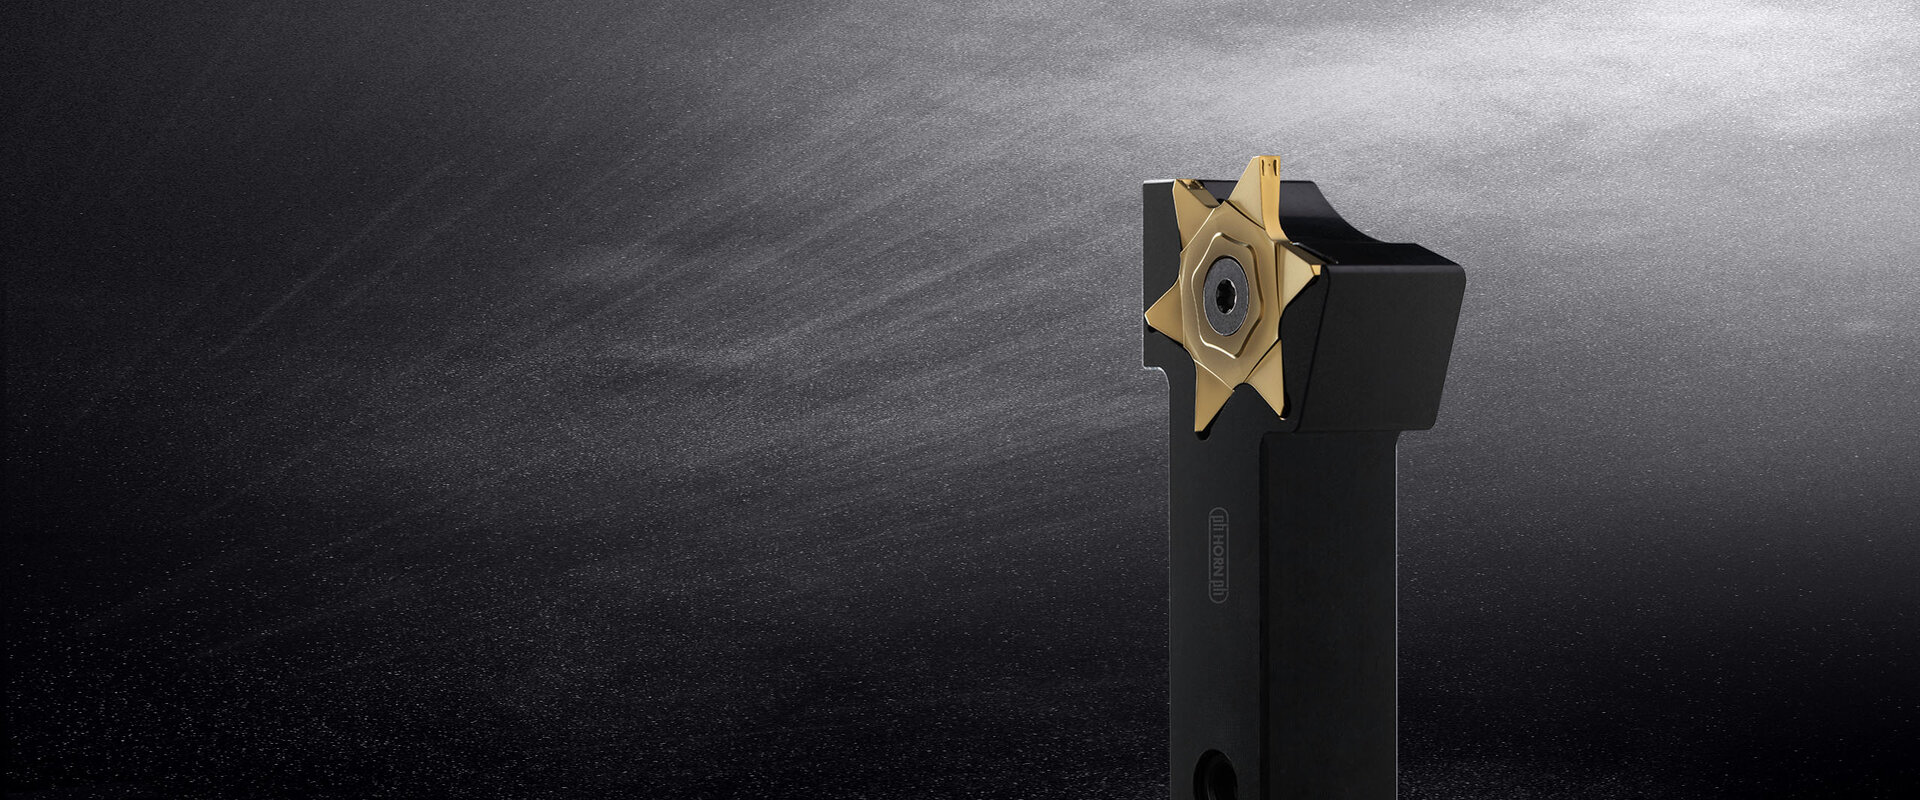
Inside the production
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Broaching (groove forming, speed forming)Cutting | – | – | – | – | – |
| Slot broaching from inner diameter 9 mmCutting | – | – | – | – | Steel, Cast |
| Carbide milling cutters (DP/DS systems for material groups)Cutting | – | – | – | – | Steel, Aluminum, Stainless steel, Titanium, Cobalt-chromium steels |
| PCD milling for aluminum machiningCutting | – | – | – | – | Aluminum |
| Carbide drills (D1122)Cutting | – | – | – | – | Steel, Cast |
| Broaching of splines/grooves (technical request broaching: groove lengths, bore diameter, shankCutting | – | – | – | – | – |
| Gear skiving / gear milling / gear hobbingCutting | – | – | – | – | hardened/not hardened (form field) |
| Hard turning/hard milling with CBN toolingCutting | – | – | – | – | hardened materials, Steel |
| PCD tools for non-ferrous metals, carbide green compacts, composite materialsCutting | – | – | – | – | Aluminum alloys, Carbide (green compacts), Composite materials |
| CVD-D tools for carbide machiningCutting | – | – | – | – | Carbide |
| MCD high-gloss turning/milling, roughness in the nanometer rangeCutting | Roughness in the nanometer range | – | – | – | Non-ferrous metals |
| Custom tool manufacturing (Greenline: tool inserts within 5, toolholders within 10 working days)Engineering | – | – | – | – | – |
| Blank/carbide production (in-house carbide manufacturing, pressing processes, carbide semi-finishedEngineering | – | – | – | – | Carbide |
| Tool coating (in-house coating center)Surface | – | – | – | – | – |
| Additive manufacturing (technical instructions)Additive | – | – | – | – | – |
| Drilling / turning / milling / broaching / grooving / gear hobbing (cutting data calculator)Cutting | – | – | – | – | – |
| Fine boring/reaming with exchangeable-head systems (URMA, changeover in seconds to micron level)Cutting | – | – | – | – | – |
4 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| Turn-mill center | – | – | – | – | Demonstration Center Tübingen (>500 m²) |
| Lathe | – | 1 | – | – | Demonstration Center Tübingen |
| Milling machines | – | 2 | – | – | Demonstration Center Tübingen |
| Sliding-headstock lathe | – | 1 | – | – | Demonstration Center Tübingen |
Additional services
Quality & Certification
The integrated management system covers quality, environment, energy and occupational safety and is based on DIN EN ISO 9001, VDA 6.4, DIN EN ISO 14001, ISO 50001 and ISO 45001. In the Demonstration Center (>500 m²), cutting data, prototype tests and series parameters are determined on real customer parts.
| Evidence | Tübingen |
|---|---|
| DIN EN ISO 9001 | |
| VDA 6.4 | |
| DIN EN ISO 14001 | |
| ISO 50001 | |
| ISO 45001 |
Company History
- 1969
Founded as Paul Horn Einstechtechnik by Paul Horn in Waiblingen; initially sites in Gomaringen and Nehren.
- 1981
Relocation of production and administration to Tübingen; renamed Hartmetall-Werkzeugfabrik Paul Horn GmbH.
- 1991
Lothar Horn joins the company, construction of the main plant, founding of Horn Hartstoffe GmbH.
- 1995
Lothar Horn becomes managing director.
- 1999
New building in Tübingen with approx. 9000 m² including coating center; between 1993 and 2001 founding of foreign subsidiaries in France, England, the USA and Hungary.
- 2008
Additional production hall with 5,500 m² of extra production space.
- 2011
New building for Horn Hartstoffe GmbH with approx. 5,000 m²; all forming processes now in-house.
- 2013
Production of carbide semi-finished products and wear parts also for third parties.
- 2016
Commissioning of a 15,000 m² production building (Tübingen's largest industrial building) and a 3,500 m² administration wing.
- 2018
Markus Horn becomes managing director in March; Matthias Rommel takes over responsibility for technology and production in November.
- 2023
Lothar Horn dies on February 5; management consisting of Markus Horn and Matthias Rommel.
- 2025
Relocation of HORN (Shanghai) Trading Co. Ltd. on December 9.