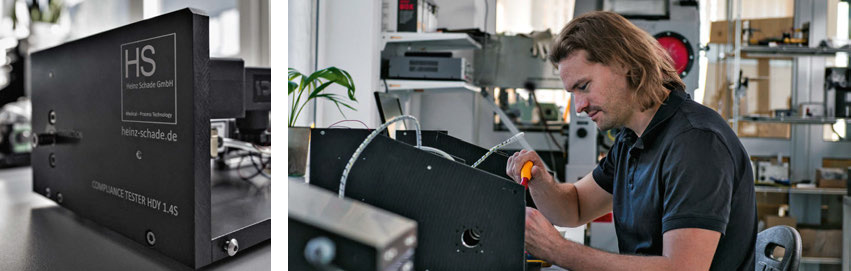
Development, manufacture and service of machines for stent, balloon and catheter production
Heinz Schade GmbH
Reutlingen-Mittelstadt (DE)New on Amplifa
About Heinz Schade GmbH
Heinz Schade GmbH is a family-run process and machine engineering company founded in 1999 and headquartered in Reutlingen-Mittelstadt near Stuttgart. The company develops, designs and manufactures machines for the production of stents, balloon catheters and catheters, including tube cutting machines (manual and software-controlled), tube drilling machines, tube stretching and drawing machines, balloon forming machines, crimping and rotary swaging machines, infrared welding machines as well as wet process systems for cleaning and electropolishing, especially of NiTinol stents. In addition, the company offers testing equipment such as radial force testers and pressure and leak test devices, its own software (SoftCut, Univers V2), machine rental, contract production under cleanroom conditions, remote maintenance and after-delivery service. All machines are developed and assembled at the site near Stuttgart and sold worldwide.
- Site
- Reutlingen-Mittelstadt
- Processes
- Cleaning (removal of laser slag and final cleaning before packaging, combining spray and, Electro Polishing (electropolishing of NiTinol stents to increase surface quality), Tube cutting (manual and automated, cutting lengths approx. 0.5 mm to 80 m in, Tube drilling (automatic tube drilling machine, length repeatability approx. 0.1 mm, angle <1°), Tube stretching (tube stretching machine CAL2, heats the tube from inside and outside for, Balloon forming (BF 208-300: single-piece production and continuous process for longer tubes, e.g., Crimping (programmable crimping machine for securely crimping stents onto balloon catheters), Rotary swaging (rotary swaging machine ROMA 3 for fine tubes)
- Materials
- NiTinol, PA, PE, PU, PUR, PTFE, EPDM, Silicones
- Certificates
- 100 % quality control (company statement), Batch traceability via software
- Founded
- 1999
- Industries
- Medical technology, Stent, balloon and catheter production
- 01
Development and design
- 02
Assembly of machines at the Reutlingen site
- 03
Software (SoftCut, Univers V2)
- 04
100 % quality control
- 05
Delivery, remote maintenance and service
- 06
Optional contract production under cleanroom conditions
Materials and Processes
Polyamide (PA)
Common tube material for the cutting, drilling and stretching machines.
Polyethylene (PE)
Standard material for machining and cutting tubes to length.
Polyurethane (PU)
Soft tube material that can be machined in a dimensionally stable way with the machines.
Polyurethane elastomer (PUR)
Used for cutting, drilling and stretching of medical technology tubes.
PTFE
Low-friction tube material for catheter applications, machinable on the machines.
EPDM
Elastomeric tube material, also suitable for the gripper principle of the Cut MT GZ.
Silicones
Soft tubes with low inherent stability for precise processing.
PET
Material for machine-based stretching of tubes with the CAL2.
NiTinol
Stent material that is electropolished for higher surface quality.
Stainless steel
Used for housing top surfaces and spools, and as material for metal tubes and steel-reinforced hoses.
Locations
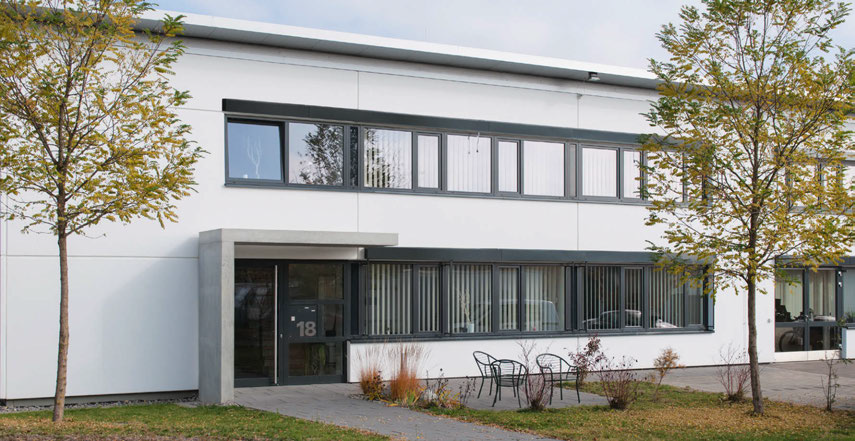
Reutlingen-Mittelstadt
DEHeadquarters, development and production
- Materials
- Plastics (PA, PE, PU, PUR, PTFE, EPDM, silicones), NiTinol, stainless steel
- Electropolishing system Avantgarde
- Stent polishing/etching system HS-Wet
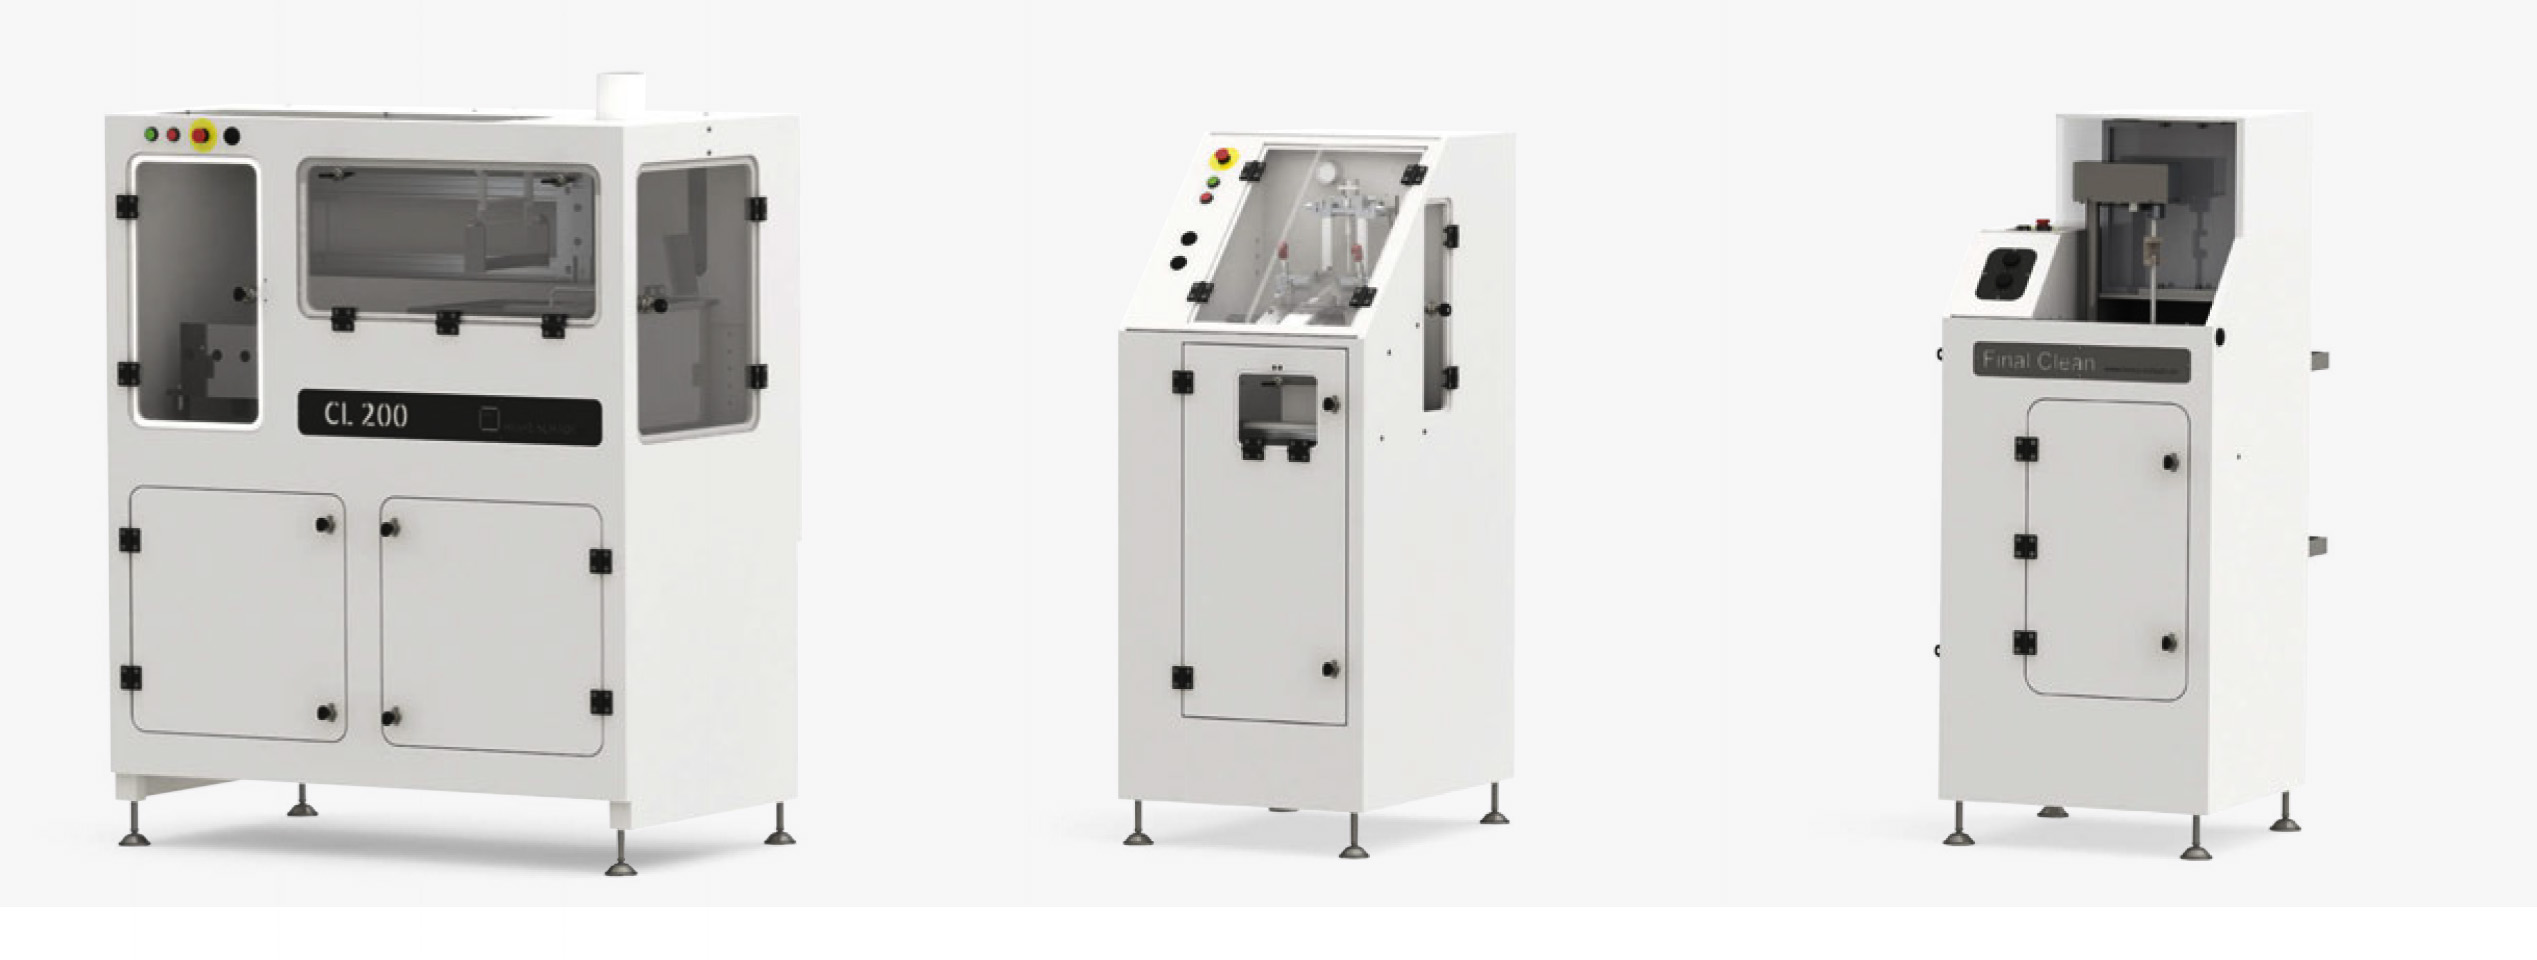
- Wet-chemical cleaning system CL 200
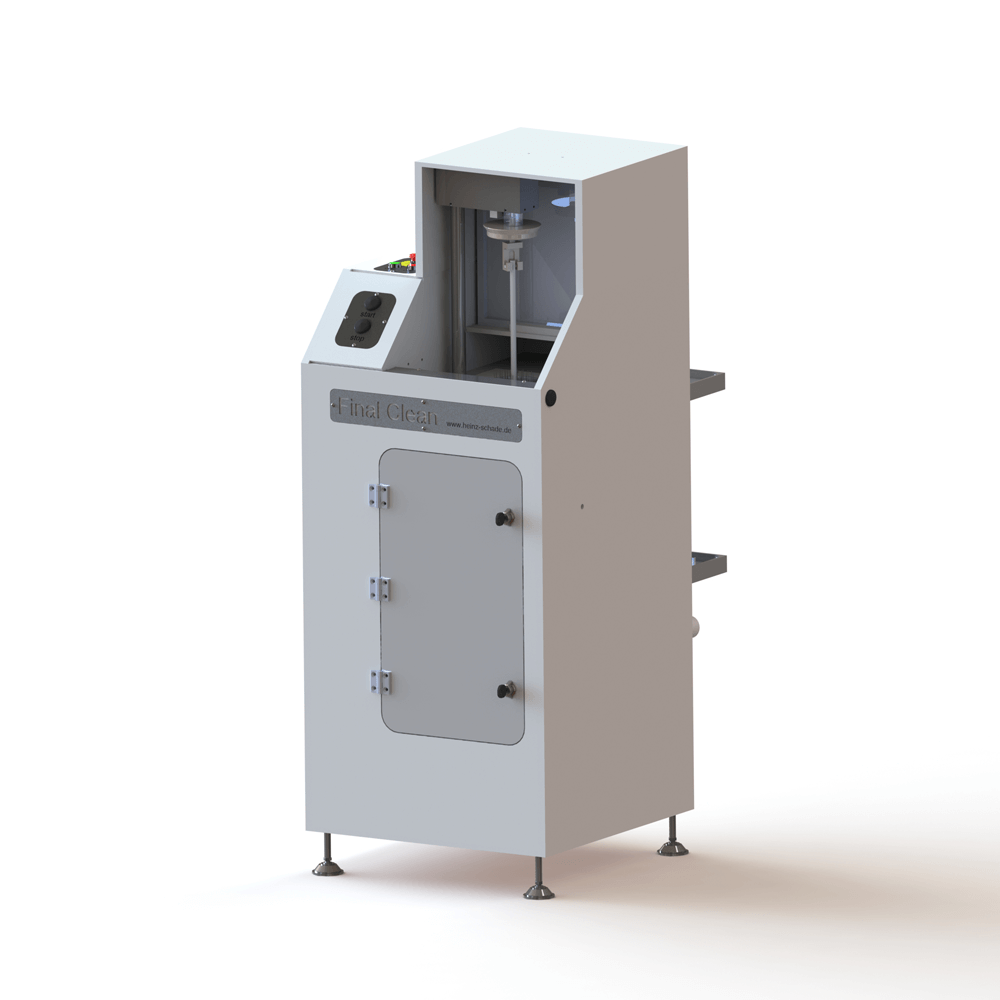
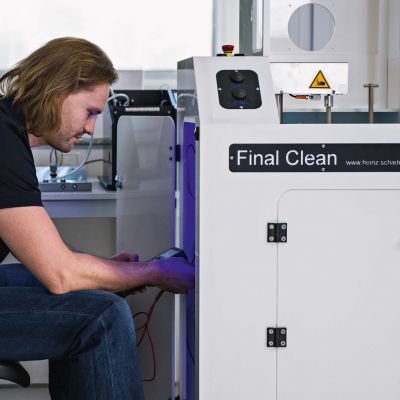
- Cleaning system Final Clean
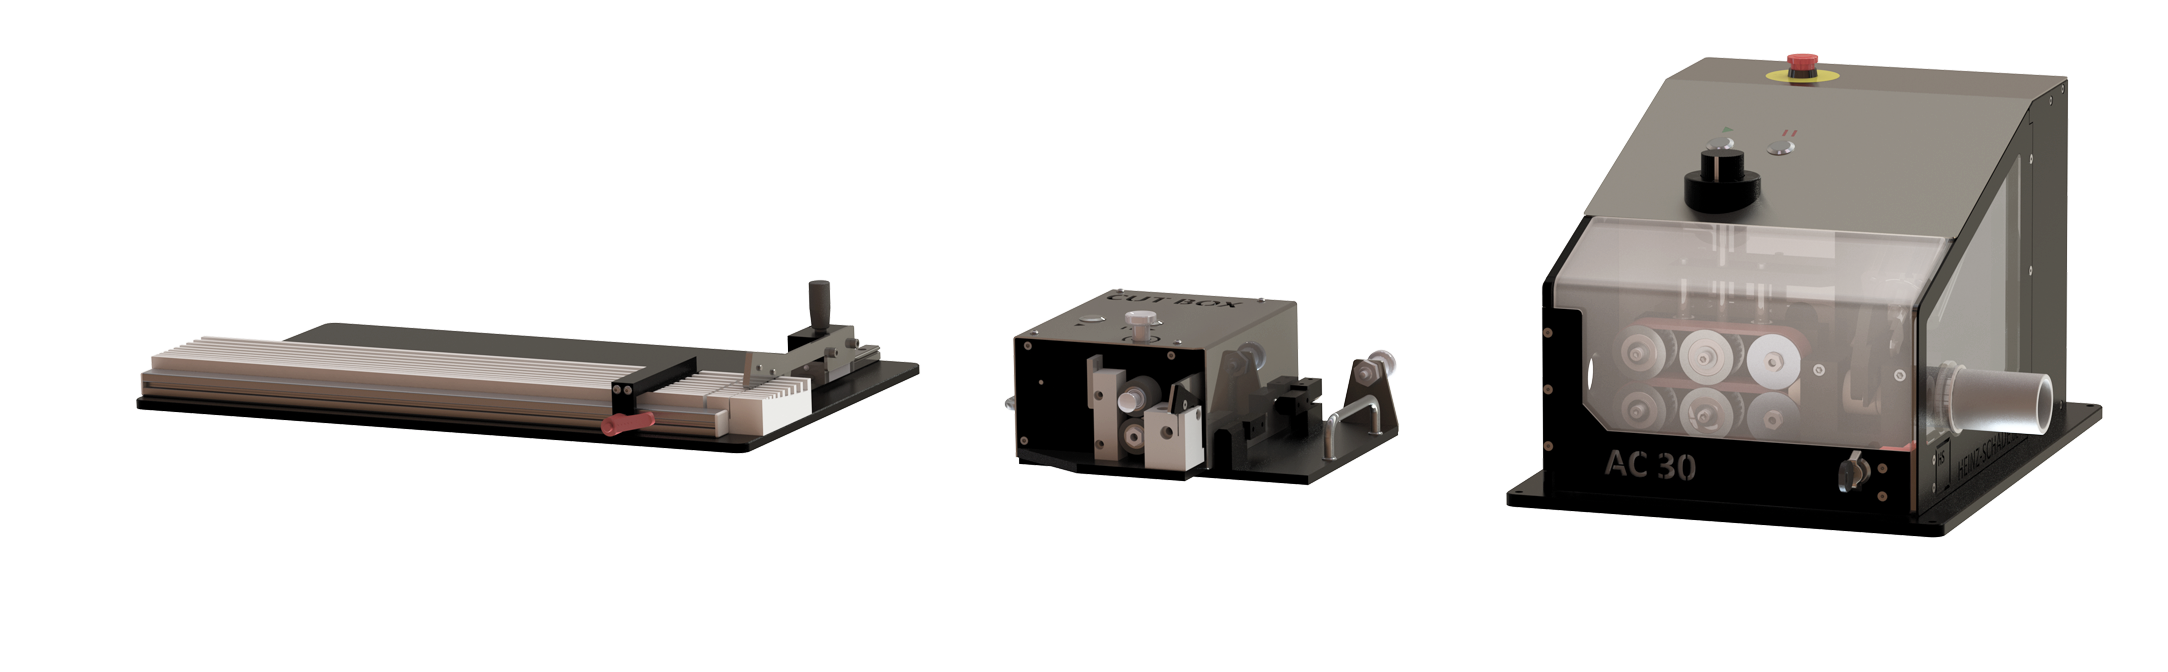
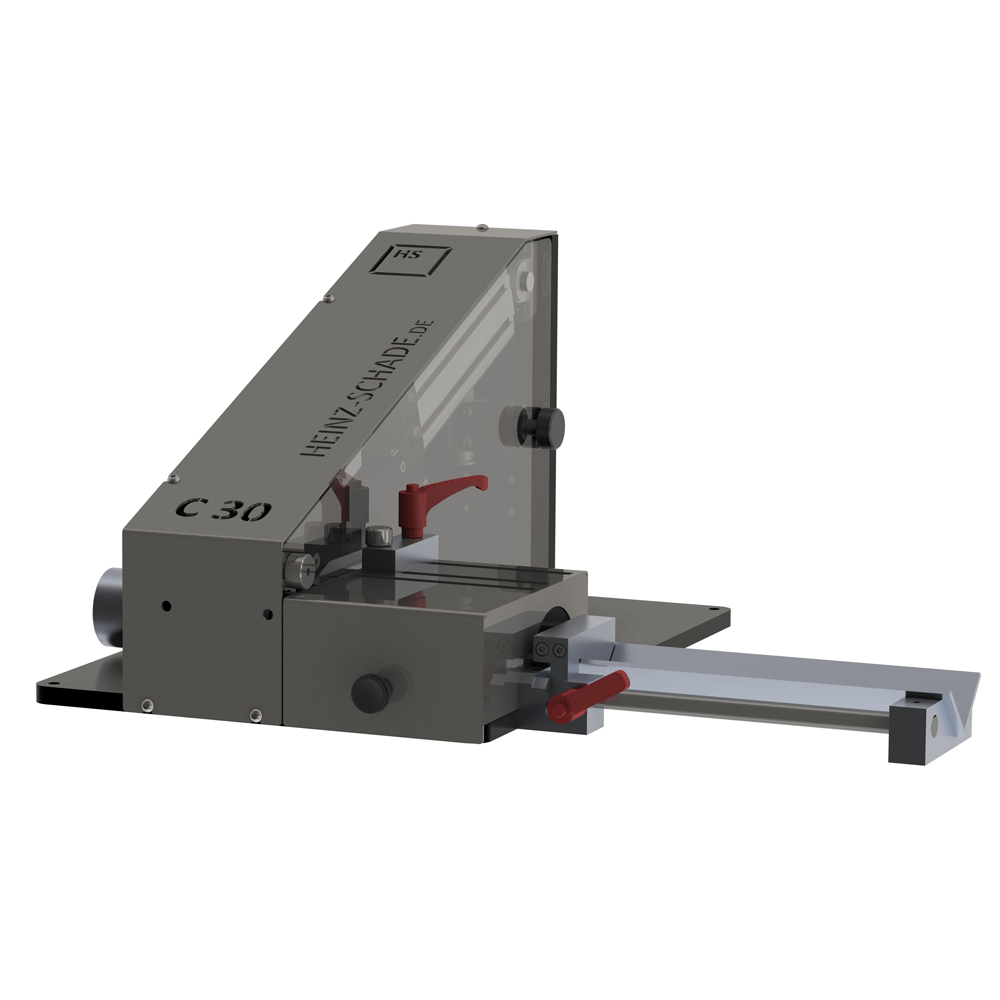
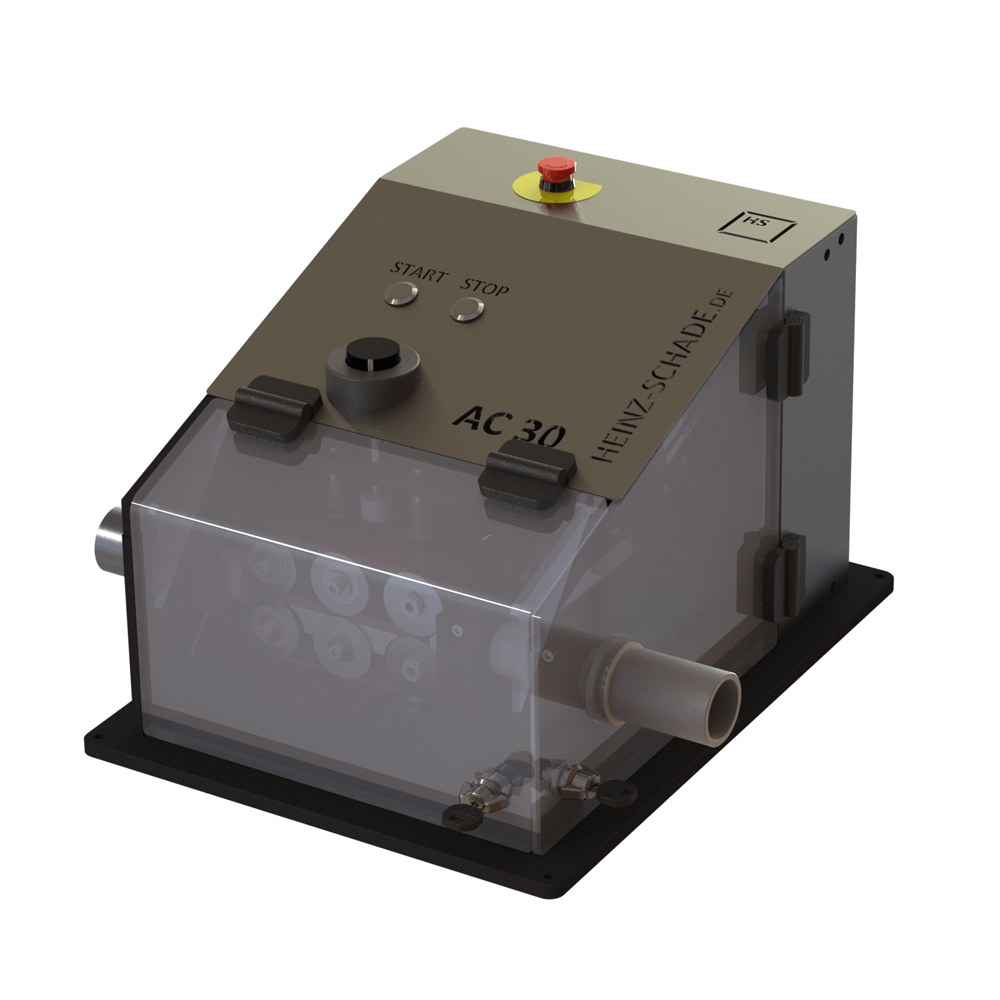
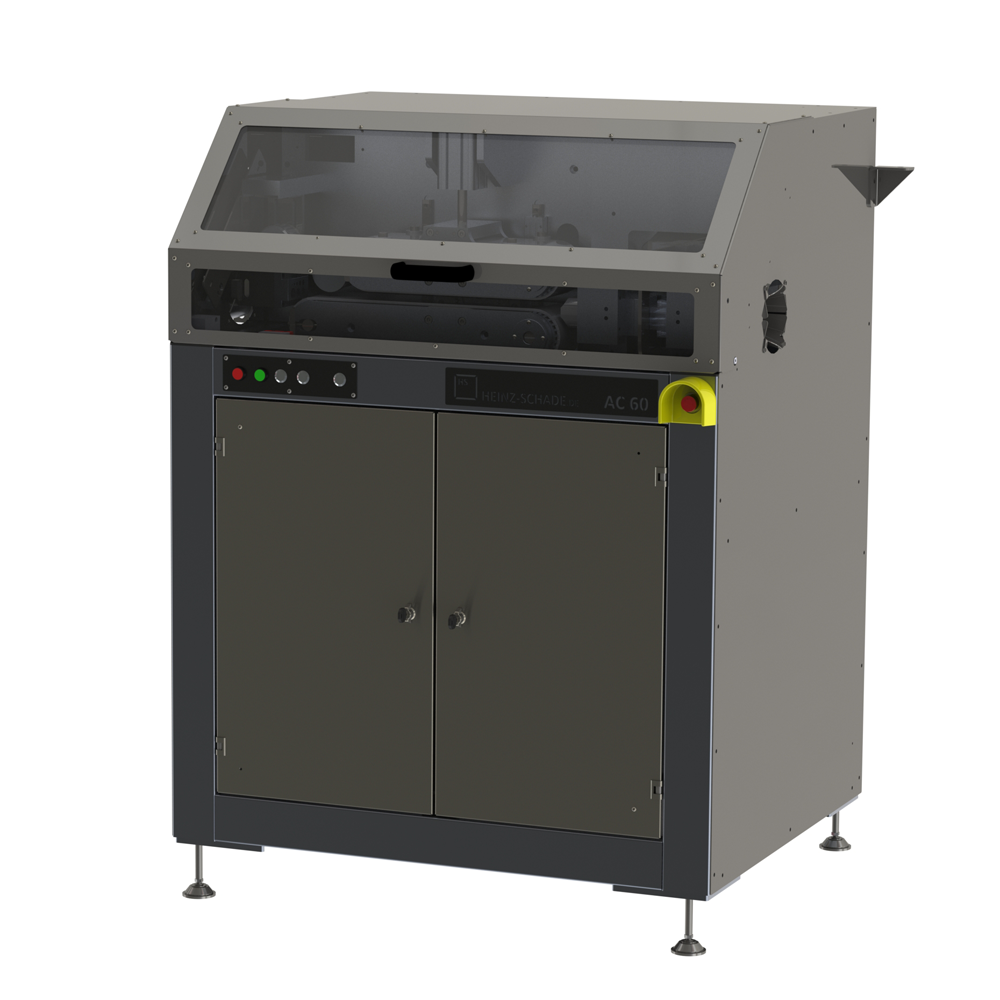
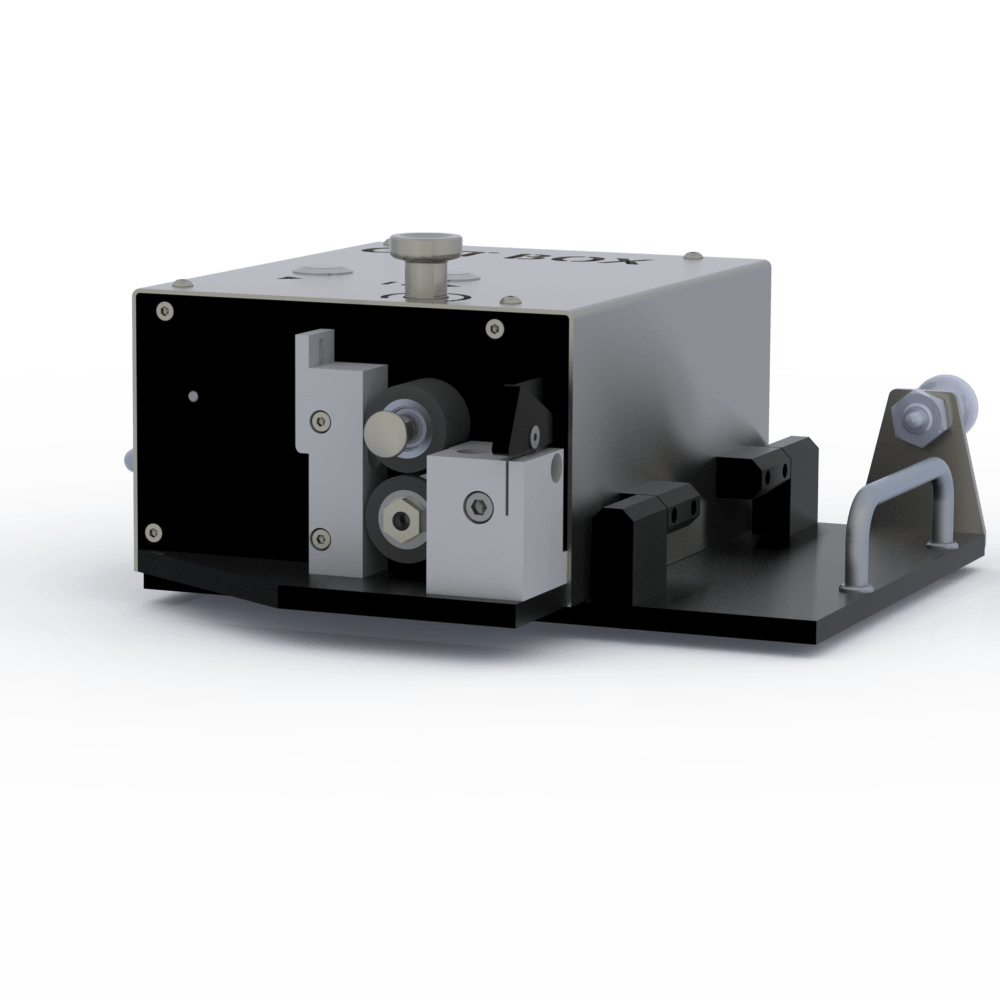
- Tube cutting machines C 30/C 100/C 200, Cut Box, AC 30/60/100
- Tube drilling machine Kiwi
- Tube stretching machine CAL2
- Tube drawing machine Gemini
- Balloon forming machines BF 208-300/BF 209
- Crimping machine Crimpmaster 3
- Rotary swaging machine Roma 3
- Welding machine IR4
- Radial force tester RF 200
- Pressure and leak test device Druleck 2
- Tensile and friction tester DLF 380
Machines and Components
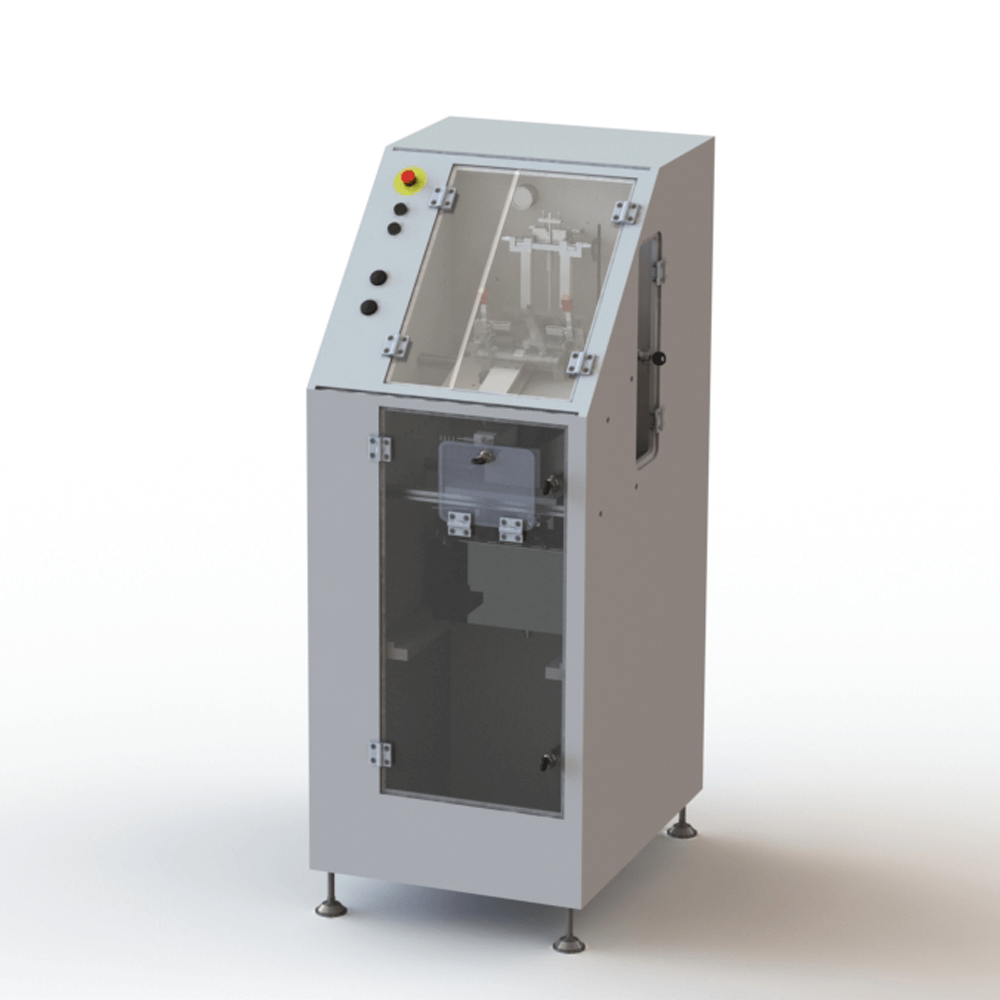
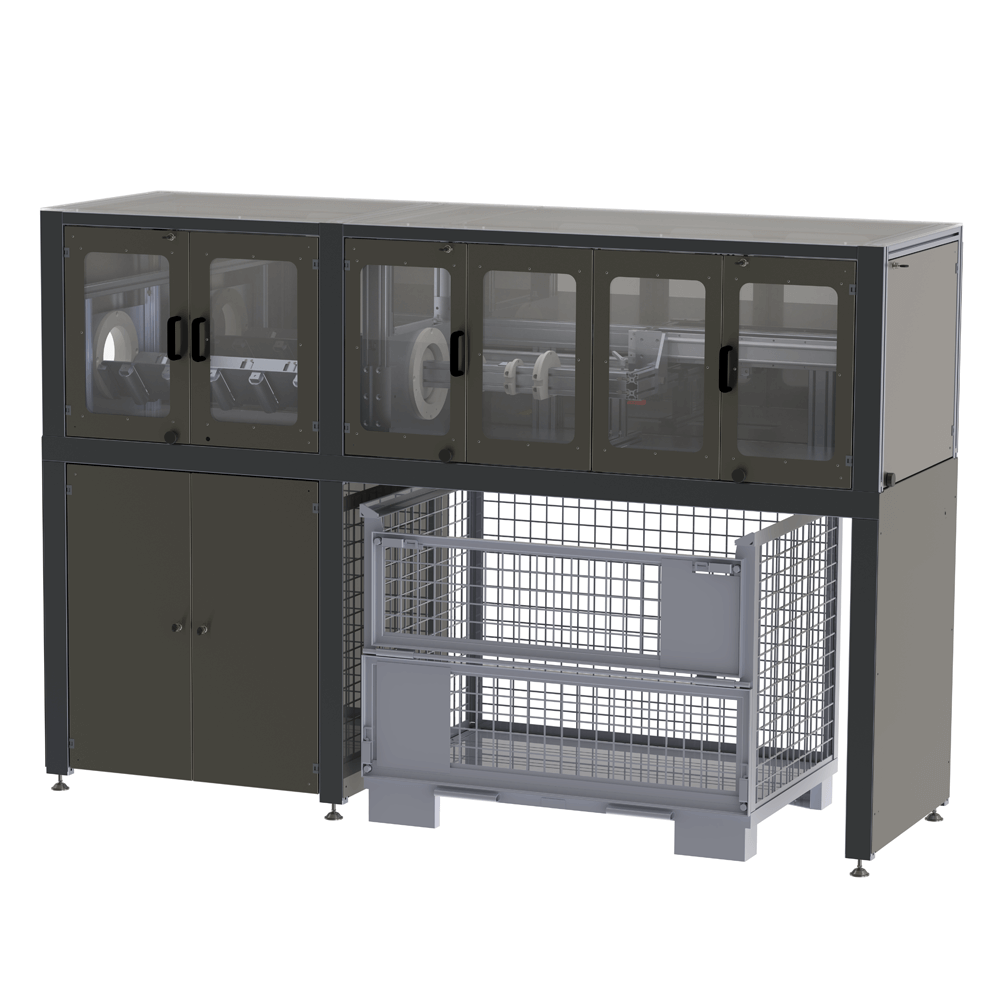
Inside the production
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Cleaning (removal of laser slag and final cleaning before packaging, combining spray andSurface | – | – | – | – | – |
| Electro Polishing (electropolishing of NiTinol stents to increase surface quality)Surface | – | – | – | – | NiTinol, various materials |
| Tube cutting (manual and automated, cutting lengths approx. 0.5 mm to 80 m inMachining | – | up to 80 m (tube length, automated); | – | – | PA, PE, PU, PUR, PTFE, EPDM, silicones, steel-reinforced hoses, metal tubes |
| Tube drilling (automatic tube drilling machine, length repeatability approx. 0.1 mm, angle <1°)Machining | length approx. 0.1 mm, angle <1° | – | – | – | PA, PE, PU, PUR, PTFE, EPDM, silicones |
| Tube stretching (tube stretching machine CAL2, heats the tube from inside and outside forForming | – | travel length 500 mm | – | – | PA, PUR, PTFE, PET |
| Balloon forming (BF 208-300: single-piece production and continuous process for longer tubes, e.g.Plastics | – | – | – | – | pretreated tubes |
| Crimping (programmable crimping machine for securely crimping stents onto balloon catheters)Assembly | – | – | – | – | stents, balloon catheters |
| Rotary swaging (rotary swaging machine ROMA 3 for fine tubes)Forming | – | – | – | – | – |
| Infrared welding of plastic tubes (IR4; also welding of hypotube and sideport)Joining | – | – | – | – | plastic tubes, hypotube, sideport |
| Pressure and leak testing (100 % inline inspection of balloons and catheters)Testing | – | – | – | – | balloons, catheters |
| Radial force measurement (fast and simple measurement of radial force)Testing | – | – | – | – | – |
| Tensile and friction force testing (inline production tester and development)Testing | – | – | – | – | – |
| Process and machine engineering for stent, balloon and catheter production (development, design andEngineering | – | – | – | – | – |
| Contract manufacturing of products under cleanroom conditionsAssembly | – | – | – | – | – |
| Annealing process / high-vacuum annealing processHeat treatment | – | – | – | – | – |
35 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| Electropolishing system | Heinz Schade Avantgarde | – | – | – | Reutlingen, Germany |
| Electropolishing system (stent polishing/etching system) | Heinz Schade HS-Wet | – | – | – | – |
| Wet-chemical cleaning system | Heinz Schade CL 200 | – | – | – | – |
| Cleaning system | Heinz Schade Final Clean | – | – | – | – |
| Manual cutting device (several tubes simultaneously) | Heinz Schade Cut MT | – | 1-30 mm | – | – |
| Manual tube cutting machine | Heinz Schade C 30 | – | Tube diameter 1-30 mm; stop up to 2 m | – | – |
| Manual cutting machine | Heinz Schade C 100 | – | 5-100 mm (side) / approx. 1-100 mm (details) | – | – |
| Manual tube cutting machine | Heinz Schade C 200 | – | 10-200 mm; length 1400 mm, optional mandrel up to 650 mm | – | – |
| Software-controlled cutting machine | Heinz Schade Cut Box | – | 0.3-10 mm; length approx. 0.5 mm to approx. 80 m in 0.01 mm steps | – | – |
| Automatic tube cutting machine | Heinz Schade AC 30 | – | 1-30 mm; length approx. 0.5-80 mm/80 m in 0.01 mm steps; feed 0-34 m/sec; 330x450x320 mm, 22 kg | – | – |
| Automatic tube cutting machine | Heinz Schade AC 60 | – | 1-60 mm; feed 0-60 m/sec; 961x800x1450 mm, 250 kg | – | – |
| Automatic tube cutting machine | Heinz Schade AC 100 | – | 1-100 mm; feed 0-60 m/sec; 961x800x1450 mm, 300 kg | – | – |
| Software-controlled cutting machine (gripper principle) | Heinz Schade Cut MT GZ 8 | – | 1-8 mm; length approx. 25-500 mm in 0.01 mm steps | – | – |
| Software-controlled cutting machine (gripper principle) | Heinz Schade Cut MT GZ 26 | – | 1-26 mm; length approx. 25-500 mm | – | – |
| Tube saw (for steel-reinforced hoses, metal tubes, rotating circular blade) | Heinz Schade CS 50 | – | 1-50 mm; stop 1 m | – | – |
| Unwinder | Heinz Schade Unwinder/Reel | – | – | – | – |
| Automatic unwinder | Heinz Schade Winder 230 / Automatic Unwinder | – | – | – | – |
| Rewinder | Heinz Schade AHA 500 | – | – | – | – |
| Stainless steel spool | Heinz Schade VA Spool | – | – | – | – |
| External tube feeder | Heinz Schade BV30 | – | – | – | – |
| Balloon forming machine | Heinz Schade BF 208-300 | – | – | – | – |
| Balloon forming machine | Heinz Schade BF 209 | – | – | – | – |
| Crimping machine | Heinz Schade Crimpmaster 3 | – | – | – | – |
| Pressure and leak test device | Heinz Schade Druleck 2 | – | – | – | – |
| Welding machine (infrared heating, plastic tubes, hypotube, sideport) | Heinz Schade IR4 | – | – | – | – |
| Tube drilling machine | Heinz Schade Kiwi | – | Drill bits 0.1-3 mm; 200x350x220 mm, 7.5 kg | – | – |
| Tube drilling machine with linear and rotary axis | Heinz Schade Kiwi and KX-100 | – | 260x350x400 mm, 11 kg | – | – |
| Gantry drilling machine (several tubes, multiple drill heads possible) | Heinz Schade 3AX 1S | – | 1210x700x1000 mm, 50 kg | – | – |
| Tube stretching machine | Heinz Schade CAL2 | – | Tube diameter 0.5-8 mm; travel length 500 mm; 800x200x300 mm, 19 kg | – | – |
| Tube drawing machine | Heinz Schade Gemini | – | two axes | – | – |
| Radial force tester | Heinz Schade RF 200 | – | – | – | – |
| Rotary swaging machine | Heinz Schade Roma 3 | – | – | – | – |
| Tensile and friction tester | Heinz Schade DLF 380 | – | – | – | – |
| Stent testing accessory (manual inspection under the microscope) | Heinz Schade Stent Roller | – | – | – | – |
| High-vacuum annealing system | Heinz Schade | – | – | – | – |
Additional services
Quality
According to the company, it places emphasis on 100 % quality control of all products. The process data of the machines are documented with software support and enable complete batch traceability.
| Evidence | Reutlingen-Mittelstadt |
|---|---|
| 100 % quality control (company statement) | |
| Batch traceability via software |
History
- 1999
Foundation of the family company in Reutlingen near Stuttgart