Spheroidal graphite and grey iron castings from 1 to 1000 kg as well as special weaving machines and packaging systems from Emsdetten.
Jürgens Holding GmbH
Emsdetten (Lönsstraße 15)New on Amplifa
About Jürgens
Jürgens Holding GmbH in Emsdetten bundles three business fields: Jürgens Gießerei GmbH & Co. KG (foundry), Jürgens Maschinenbau GmbH & Co. KG (mechanical engineering) and Packaging and Automation Technology. The foundry produces castings in ferritic spheroidal graphite iron to DIN EN 1563 and grey iron to DIN EN 1561 with unit weights of 1 to 1000 kg – from design engineering through prototyping and simulation, core shooting in the cold-box process, fully automatic flask lowering moulding using the SEIATSU process, to machining, finishing (chromating, Tennifer) and assembly. In the melting operation, three ABB medium-frequency crucible furnaces (4 t each) produce around 5 t of liquid iron per hour, corresponding to approx. 80 t of spheroidal graphite iron per day; the Mg treatment is carried out by the wire injection process. The mechanical engineering division, one of the world's active manufacturers of special weaving machines, builds shuttle, gripper and projectile weaving machines (JP-2000/JP-4000/JP-5000) for paper machine clothing, as well as fully automatic roll handling and packaging systems for the gypsum, film and nonwovens industries. Customers of the castings and systems come from, among others, the paper, gypsum, film and nonwovens industries as well as general mechanical engineering; the foundry's sales territory is Germany and Europe, while the machines are delivered worldwide.
- Site
- Emsdetten
- Processes
- Spheroidal graphite iron (cast iron with spheroidal graphite), Grey iron, Core shooting, cold-box process, Core making by the Resol-CO2 process (hand core-making station, prototypes), Melt treatment / wire injection process (Mg cored wire), Small flask line production (SEIATSU air-flow squeeze moulding process, 120 moulds/h), Large flask line production (SEIATSU air-flow squeeze moulding process, 30 flask halves/h), Machining / finishing of castings
- Materials
- Spheroidal graphite iron (cast iron with spheroidal graphite, ferritic as-cast), Grey iron, Pig iron grades, Steel scrap, Deep-drawing sheet packages, Spheroidal graphite iron (DIN EN 1563), Grey iron (DIN EN 1561), SEIATSU air-flow squeeze moulding process
- Certificates
- DIN EN ISO 9001, ISO 9001
- Founded
- 1921
- Industries
- Paper industry (paper machine clothing, technical textiles), Gypsum industry, Film and nonwovens industry (nonwovens), Hazardous and industrial goods (packaging), Textile machinery building
- 01
Engineering (2D/3D: AutoCAD, GENIUS, Pro/ENGINEER, Creo 4.0)
- 02
Prototyping, simulation, trial castings
- 03
Core shooting, cold-box or Resol-CO2 (hand core-making station)
- 04
Moulding shop (SEIATSU, small and large flask moulding lines)
- 05
Melting operation (ABB medium-frequency crucible furnaces, wire injection)
- 06
Casting and post-treatment
- 07
Machining and finishing (chromating, Tennifer)
- 08
Assembly
- 09
Casting logistics (GLO) with storage and just-in-time provision
Materials and Processes
Spheroidal graphite iron (DIN EN 1563)
Ferritic cast iron with spheroidal graphite in the as-cast condition without annealing, with high load capacity and tensile strength.
Grey iron (DIN EN 1561)
Characterised by low heat generation and good damping properties.
SEIATSU air-flow squeeze moulding process
Air-flow compaction with a hydraulic multi-piston press for dimensionally accurate castings with a clean surface.
Cold-box core shooting process
Highly mechanised core production with shooting volumes of 2.5–30 l and core box heights up to 620 mm.
Wire injection process (Mg cored wire)
Magnesium treatment of the base melt to ensure the required cast iron quality.
Chromating
Finishing process for machined casting surfaces.
Tennifer
Finishing process for the surface treatment of castings.
Site
Emsdetten
DEHeadquarters, foundry, mechanical engineering (weaving machines and packaging technology)
- Part weight / size
- Castings 1–1000 kg; weaving machines up to 80 t
- Lot size
- Raw castings 1–1000 kg unit weight; 10–15 weaving machines/year
- Materials
- Spheroidal graphite iron (EN-GJS), grey iron (EN-GJL)
- 3 ABB medium-frequency crucible furnaces of 4 t each
- 4 core shooting machines (cold-box, 2.5–30 l)
- Fully automatic flask lowering moulding machine, small flask line (620x620x220/220+50 mm, up to 120 moulds/h)
- Fully automatic flask lowering moulding machine, large flask line (1500x1200x400/400+50 mm, up to 30 flask halves/h)
- Casting machines/pouring locomotives
- Charge mixer
- Optical vacuum emission spectrometer
- GLO storage system (approx. 4000 m², approx. 3000 storage slots) with fully automatic packaging system
- Projectile weaving machines JP-2000/JP-4000/JP-5000 (6–10 m weaving width)
- Band gripper weaving machines
- Shuttle looms up to 33.15 m weaving width
- Warp knitting tricot machines (Karl Mayer) up to 400 m/min
Components and Products
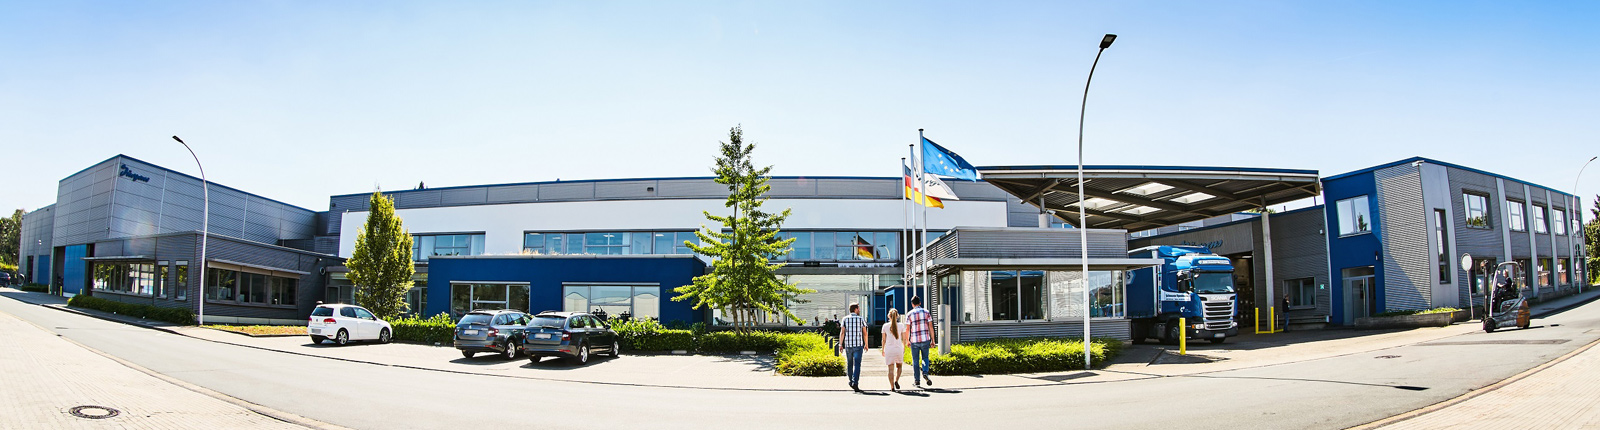
Inside the production
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Spheroidal graphite iron (cast iron with spheroidal graphite)Casting | – | – | 1 kg – 1000 kg | – | Spheroidal graphite iron (EN-GJS, ferritic as-cast) |
| Grey ironCasting | – | – | 1 kg – 1000 kg | – | Grey iron (EN-GJL) to DIN EN 1561 |
| Core shooting, cold-box processCasting | – | 620 mm | – | – | – |
| Core making by the Resol-CO2 process (hand core-making station, prototypes)Casting | – | – | – | – | – |
| Melt treatment / wire injection process (Mg cored wire)Casting | – | – | – | – | Spheroidal graphite iron |
| Small flask line production (SEIATSU air-flow squeeze moulding process, 120 moulds/h)Casting | – | 620 mm × 620 mm × 220/220+50 mm | approx. 120 kg | – | Spheroidal graphite iron, Grey iron |
| Large flask line production (SEIATSU air-flow squeeze moulding process, 30 flask halves/h)Casting | – | 1500 mm × 1200 mm × 400/450 mm | 80 kg – 1000 kg | – | Spheroidal graphite iron, Grey iron |
| Machining / finishing of castingsMachining | – | – | – | – | Spheroidal graphite iron, Grey iron |
| Finishing: chromatingSurface | – | – | – | – | – |
| Finishing: TenniferSurface | – | – | – | – | – |
| Testing: hardness, visual and ultrasonic testing, magnetic particle crack/dye penetrant testingTesting | – | – | – | – | – |
| Design/engineering of castings (2D/3D: AutoCAD, GENIUS, Pro/ENGINEER, Creo 4.0)Engineering | – | – | – | – | – |
| Assembly / ready-to-install casting-based componentsAssembly | – | – | – | – | Spheroidal graphite iron, Grey iron |
| Casting logistics (GLO): corrosion-protected storage, just-in-time, fully automaticAssembly | – | – | – | – | – |
| Manufacture of special weaving machines (forming fabric, papermaker felt, dryer screen weavingAssembly | – | 8–30 m weaving width | 80 t | 10–15 machines/year | – |
| Packaging systems and systems (roll handling, gypsum, hazardous and industrial goods)Assembly | – | – | – | – | – |
12 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| Core shooting machine (cold-box) | – | several | Shooting volume 2.5–20 l (brochure: 2.5–30 l), core box height up to 620 mm | – | Emsdetten |
| ABB medium-frequency crucible furnace | ABB | 3 | 4 t capacity, approx. 5 t liquid iron/h, 80 t spheroidal graphite iron/day | – | Emsdetten |
| Fully automatic flask lowering moulding machine (small flask line with pattern turntable) | – | 1 | Flask size 620x620x220/220+50 mm, up to 120 moulds/h | – | Emsdetten |
| Fully automatic flask lowering moulding machine (large flask line with pattern roller conveyor) | – | 1 | Flask size 1500x1200x400/400+50 mm, up to 30 flask halves/h | – | Emsdetten |
| Casting machine/pouring locomotive | – | – | – | – | Emsdetten |
| Optical vacuum emission spectrometer | – | – | – | – | Emsdetten |
| GLO storage system with BSS and integrated packaging system | – | 1 | approx. 4000 m², approx. 3000 storage slots, approx. 9 m height | – | Emsdetten |
| Band gripper weaving machine | Jürgens | – | – | seit 2000 | Emsdetten |
| Projectile weaving machine JP-2000 / JP-4000 / JP-5000 | Jürgens JP-2000 / JP-4000 / JP-5000 | – | Weaving widths 6–10 m; JP-4000: 6 m at 210–230 picks/min; JP-5000: 10 m at 130 picks/min | – | Emsdetten |
| Shuttle loom | Jürgens | – | Weaving width up to 33.15 m (world record 2005) | – | Emsdetten |
| Warp knitting tricot machine (tandem, Karl Mayer) | Karl Mayer | – | up to 400 m/min warping speed | – | Emsdetten |
| Charge mixer | – | – | – | – | Emsdetten |
Additional services
Reference customers
Quality
An optical vacuum emission spectrometer tests melt samples, supplemented by hardness, visual and ultrasonic testing, magnetic particle crack/dye penetrant testing, 3-D coordinate measurement as well as tensile and notched bar impact bending tests. Inspection certificates to DIN EN 10204 are issued by recognised experts; test results are recorded and evaluated via a central PPS system.
| Evidence | Emsdetten |
|---|---|
| ISO 9001 |
History
- 1921
Albert Bernhard Jürgens founds the company in Emsdetten as a trading business for wooden shoes; later manufacture of lathes, milling and copying machines.
- 1947
Foundation stone laid at the present site at Lönsstraße 15; production of wooden shoe machines and mechanical looms (among others for jute, sisal and coconut fabrics).
- 1954
Albert Hubert Jürgens joins; development and start of production of ferritic spheroidal graphite iron in the as-cast condition without annealing as the first foundry in the Federal Republic.
- 1989
Albert Andreas Jürgens (3rd generation) joins the company.
- 1995
Introduction of the JP-2000 projectile weaving machine for paper machine clothing – worldwide the fastest broad weaving machine for forming fabrics.
- 2000
Delivery of the first Jürgens band gripper weaving machine.
- 2002
Albert Andreas Jürgens becomes sole shareholder and managing director.
- 2003
Modernisation of the first HP200 competitor weaving machine to band gripper and new control system.
- 2004
Entry into packaging and automation technology for the gypsum, film and nonwovens industries.
- 2005
World record: widest shuttle loom in the world at 33.15 m (Guinness Book of World Records); founding of the holding company.
- 2006
Cooperation with Karl Mayer: worldwide agency and sales rights for warp knitting tricot machines for the paper machine clothing market.
- 2007
Introduction of the JP-5000 projectile weaving machine (10 m, 130 picks/min).
- 2008
Delivery of the world's first tandem warp knitting tricot machine (250 m/min) and the first Accutense yarn brakes (up to 400 m/min) via Karl Mayer.
- 2011
Commissioning of the JP-4000 projectile weaving machine (6 m, 210–230 picks/min).
- 2013
First stretching frame with infrared fabric heating for the PMC market, directly downstream of the weaving machine.
- 2014
Delivery of packaging system no. 100; end customer Saint-Gobain Brazil.
- 2015
Introduction of the e-drive concept for band gripper weaving machines; delivery of the world's largest handling and packaging system for nonwoven rolls to the USA.