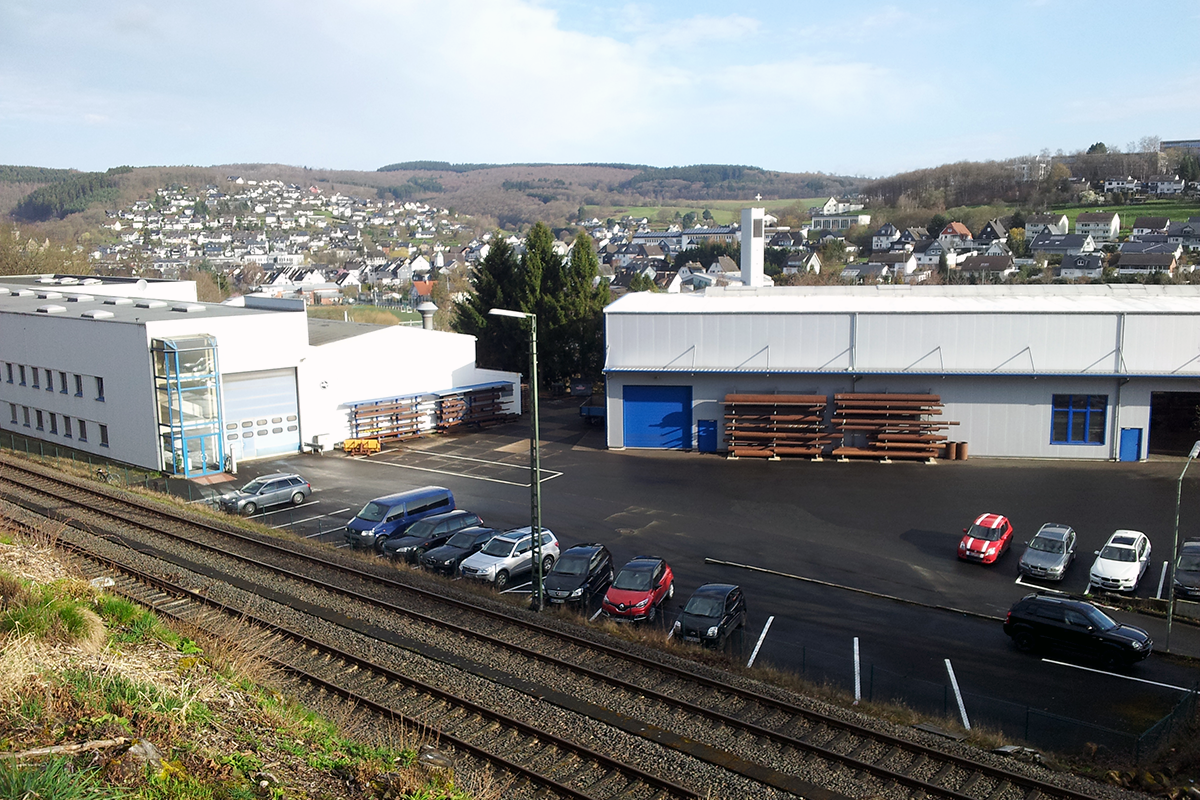
Manufacture of piping, vessels and apparatus from steel and stainless steel in Neunkirchen-Zeppenfeld
Karl Adolf Welsch Apparatebau GmbH
57290 Neunkirchen (Zeppenfeld)New on Amplifa
Metal processing from the Siegerland, now in its third generation
Karl Adolf Welsch Apparatebau GmbH is an owner-managed company in its third generation, based in Neunkirchen-Zeppenfeld in the Siegerland region. The company manufactures complete piping systems, flange connections, segment bends, branch fittings (laterals), Y-pieces and reducers, as well as vessels such as pressure vessels, agitator vessels, dispatch vessels, storage vessels and storage silos. In apparatus engineering, the company produces combustion chambers, wet deslaggers, static mixers, heat exchanger housings and conveying equipment. The range of in-house production includes 3D pipe laser cutting, plasma cutting, mechanical machining, bending of cylindrical and conical components, and partially automated welding on submerged-arc (SAW) and MAG welding systems. In addition, the company offers sandblasting and painting as well as wear protection through lining with basalt or aluminium oxide ceramics and manufacture from wear-resistant materials. Materials processed include structural steels, pressure vessel steels, fine-grained structural steels, creep-resistant steels, stainless steels, duplex steels and heat-resistant materials. Customers come from the chemical, paper, energy, wastewater and waste industries as well as from mining. Production is carried out in accordance with codes such as EN 13445, EN 13480 and AD 2000.
- Site
- Neunkirchen
- Processes
- Piping construction (complete piping systems, flange connections, segment bends, Y-pieces, reducers,, Vessel construction (pressure vessels, agitator vessels, storage vessels, storage silos), Apparatus engineering (static mixers, flare pipes, combustion chambers, wet deslaggers, slag drop, 3D pipe laser cutting (pipes and profiles), Plasma cutting, Developed patterns, Welding (manual and automatic welding, MAG/SAW, partially automated), Sandblasting (in own sandblasting booth, DIN EN ISO 12944-5 Part 4)
- Materials
- Structural steels (e.g. S235, S355), Pressure vessel steels (e.g. P265GH, P355GH), Fine-grained structural steels (e.g. P275, P355, P460 as NH, NL1 or NL2), Creep-resistant steels (e.g. 16Mo3, 19Mn5), Stainless steels (e.g. 1.4301, 1.4306, 1.4541, 1.4571, 1.4401, 1.4404, 1.4539), Duplex steels (e.g. 1.4462), Heat-resistant materials (e.g. 1.4713, 1.4724, 1.4762, 1.4828, 1.4841, 1.4878), KAW 100 (wear-protection plate, e.g. chute bend 8+5 mm)
- Certificates
- EN ISO 3834-2, AD 2000 data sheet HP 0 / HP 100R; EN 13445-4,-5; EN 13480-4,-5 (Directive, Module A2 per Directive 2014/68/EU, Welding coordination person per EN ISO 14731 (Achim Hirsch, Level B), VT Level 2 per DIN EN ISO 9712 (Achim Hirsch), PT Level 2 per DIN EN ISO 9712 (Achim Hirsch), UKCA approval, AD 2000 HP 0 / HP 100R, Directive 2014/68/EU (Module A2), Welding coordination EN ISO 14731, VT Level 2 per ISO 9712, PT Level 2 per ISO 9712, ISO 9001
- Founded
- 1961
- Industries
- Chemical industry, Paper industry, Energy sector, Wastewater industry, Mining, Waste incineration/waste processing
- 01
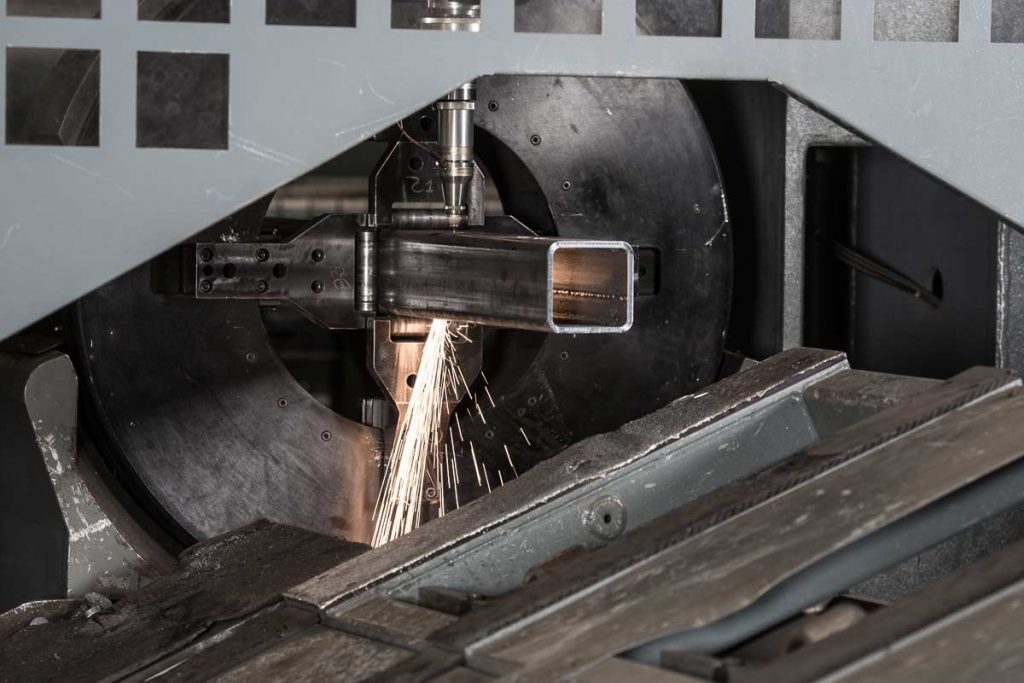
3D pipe laser cutting
- 02
Plasma cutting and developed patterns
- 03
Bending of cylindrical and conical components
- 04
Mechanical machining
- 05
Welding (MAG/SAW, manual and automatic welding)
- 06
Wear-protection lining
- 07
Sandblasting and painting/coating
- 08
Inspection and acceptance with independent experts
Materials and manufacturing processes
Structural steels
Fundamental construction materials for piping, vessel and apparatus engineering.
Pressure vessel steels
Materials for pressure-bearing vessels in accordance with the Pressure Equipment Directive and AD 2000.
Fine-grained structural steels (NH, NL1, NL2)
For highly stressed components with increased requirements on toughness and high-temperature strength.
Creep-resistant steels
Use in temperature-stressed apparatus and pressure vessels.
Stainless steels (e.g. 1.4301, 1.4571, 1.4404)
Corrosion-resistant vessels and piping for chemical and food applications.
Duplex steel
High-strength and corrosion-resistant for aggressive media.
Heat-resistant materials
For combustion chambers and components at high operating temperatures.
Wear-protection plate
Chute bends, e.g. 8+5 mm, for abrasive bulk material conveying.
Basalt ceramic lining
Wear protection for pipe parts in the conveying of abrasive bulk materials.
Aluminium oxide ceramic lining
Increases the service life of components in contact with abrasive media.
Manufacturing site
Neunkirchen (Zeppenfeld)
DEHead office, production
- Part weight / size
- Vessels up to approx. 10 t
- Lot size
- Single parts up to series (contract manufacturing)
- Materials
- Structural steels, pressure vessel steels, stainless steels, duplex, heat-resistant materials
- 3D pipe laser cutting system
- SAW welding system
- MAG welding system
- Welding system for flange pipes
- Bending machines for cylindrical and conical components
- Sandblasting booth (3,650 × 6,550 × 3,250 mm)
- Painting hall
- Crane systems
Components from piping, vessel and apparatus engineering
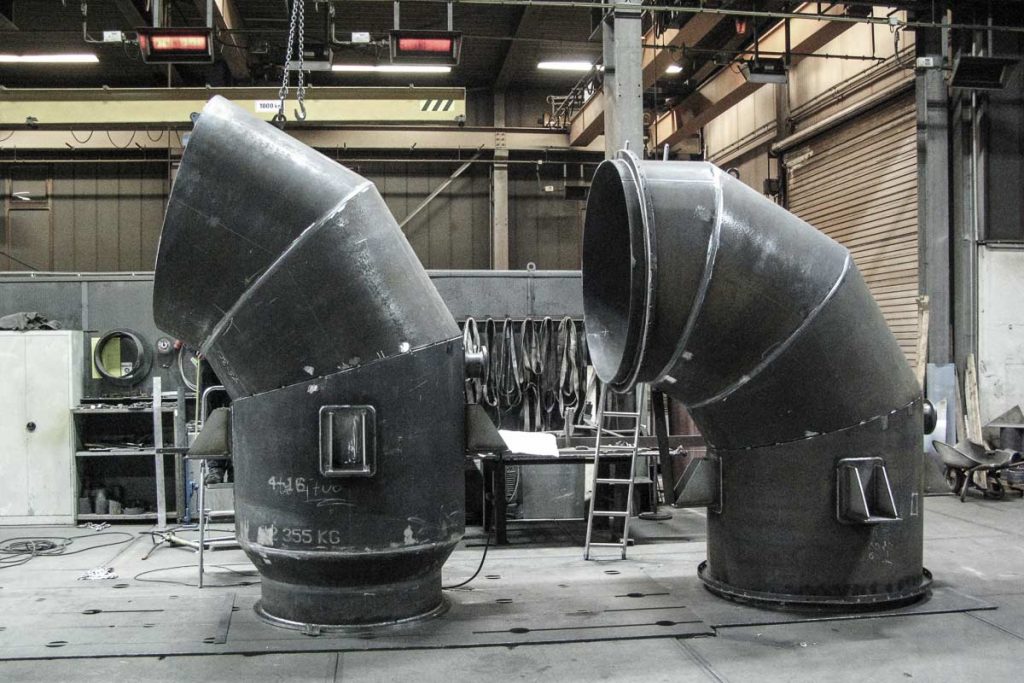
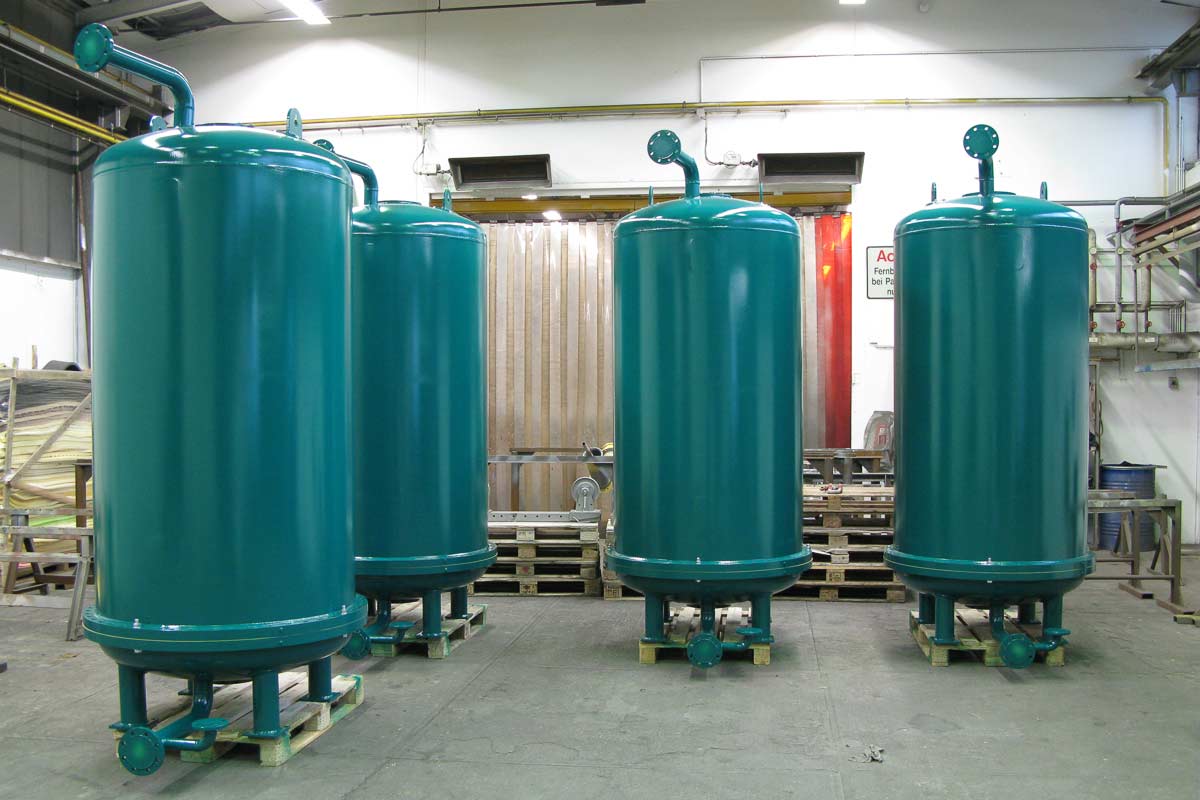
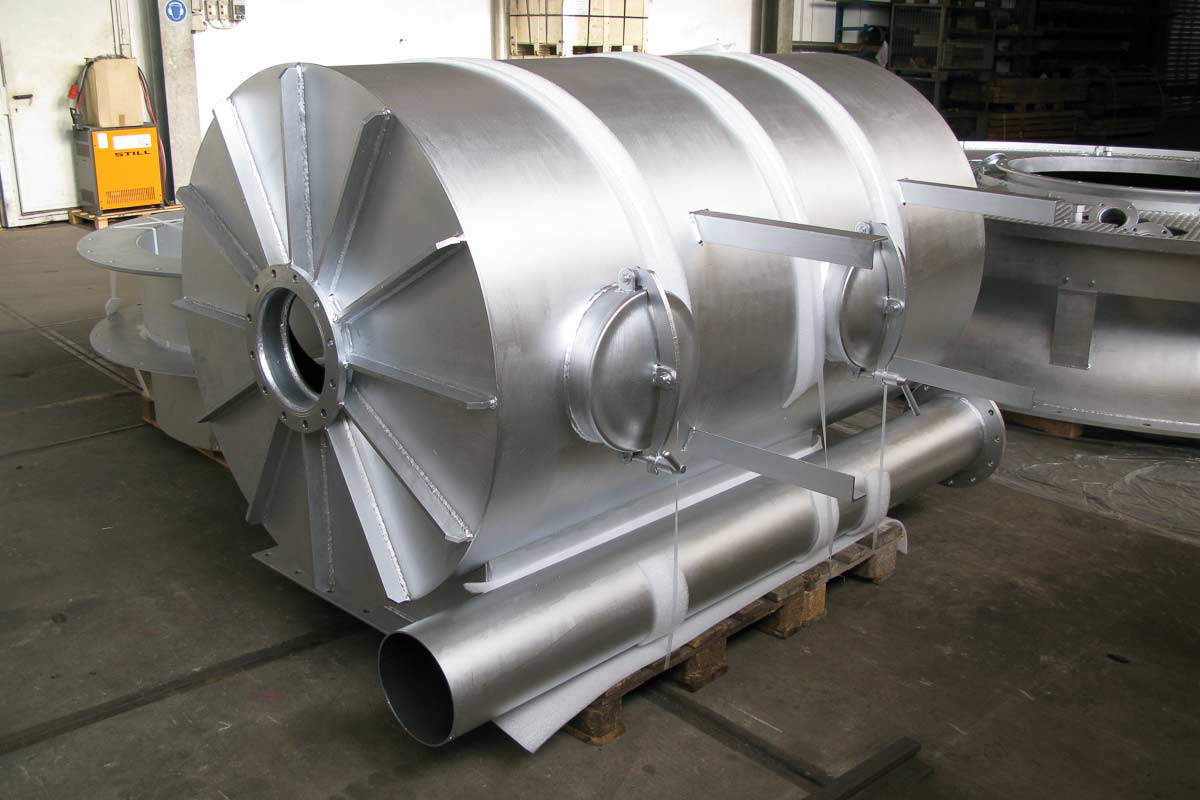
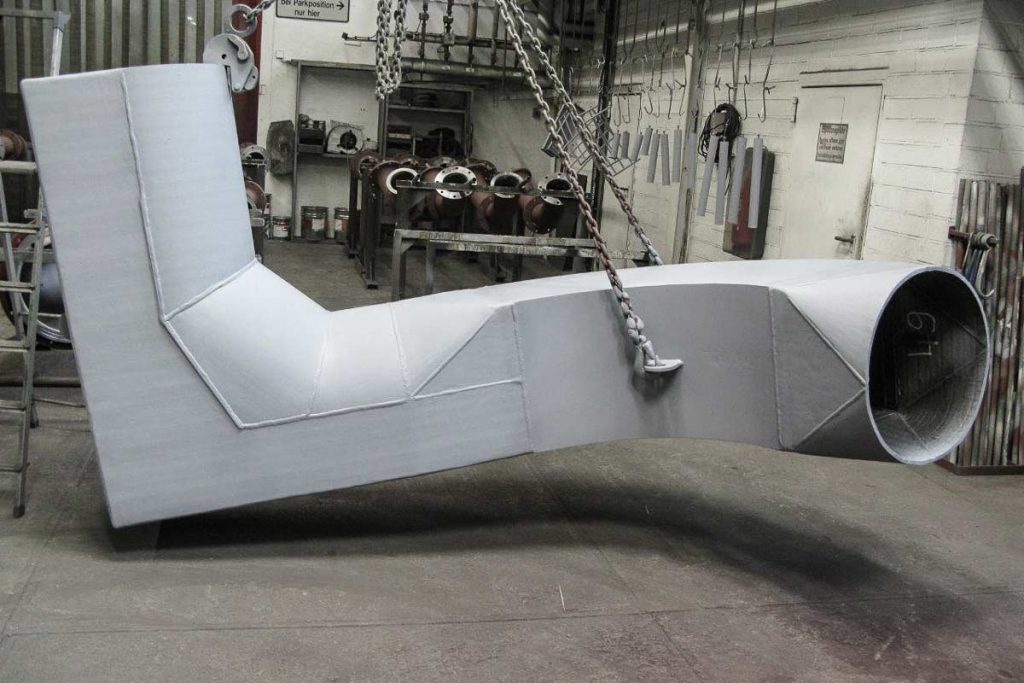
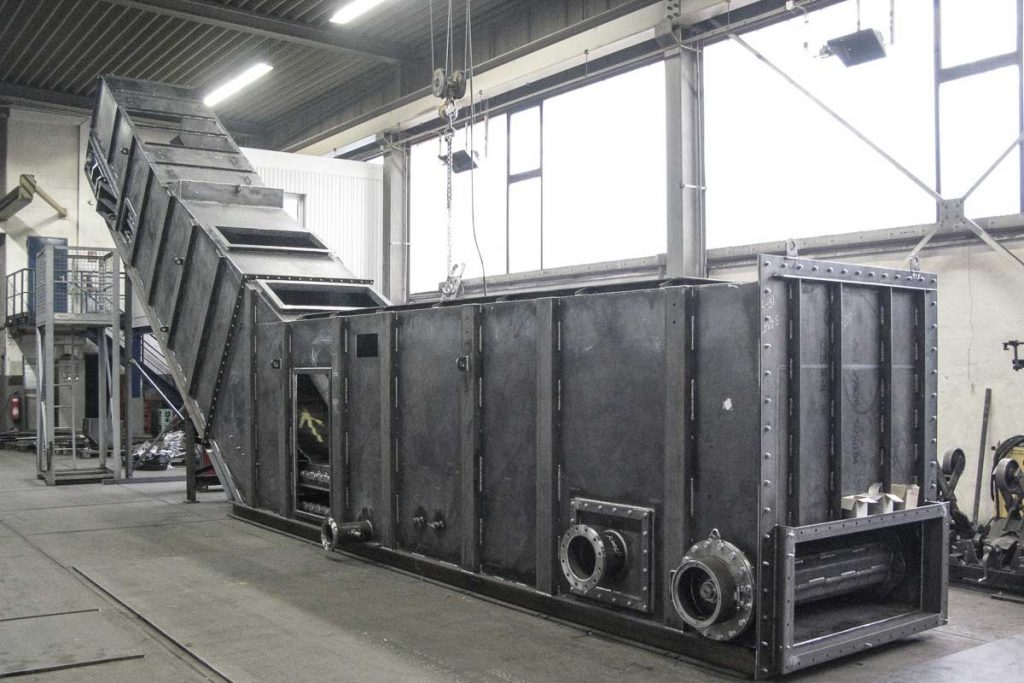
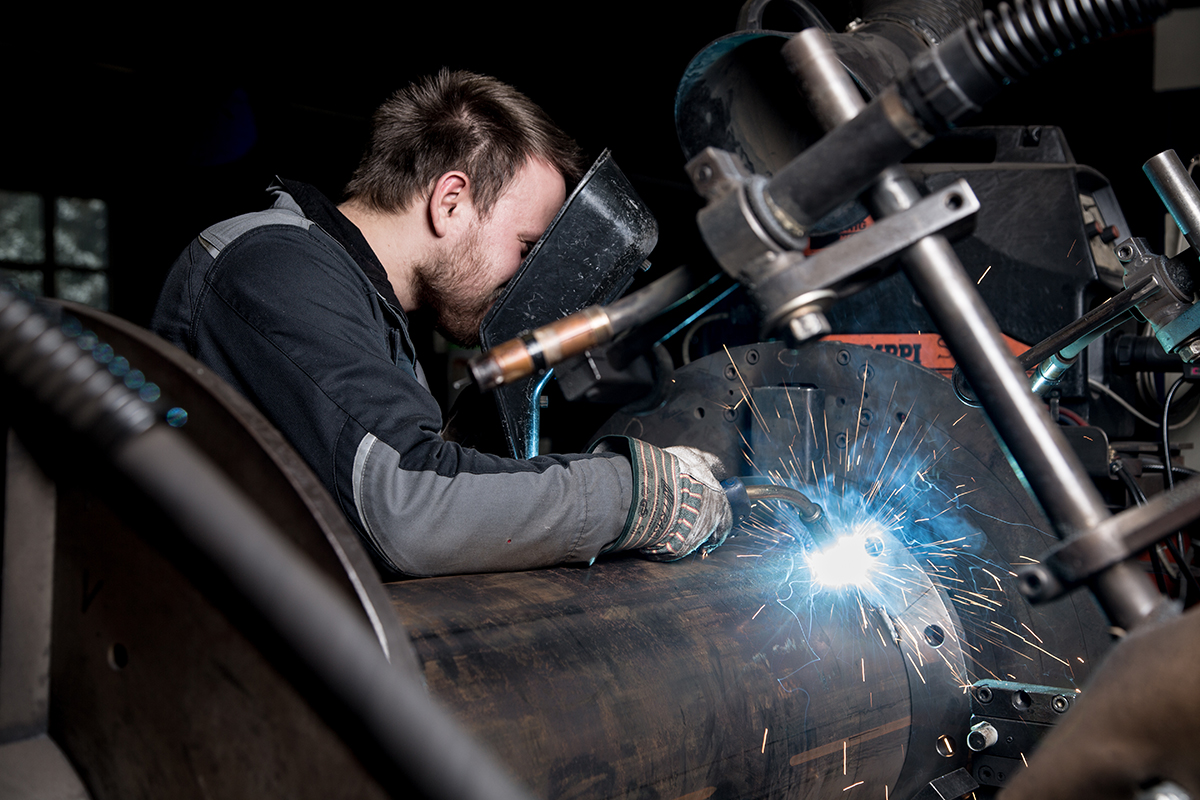
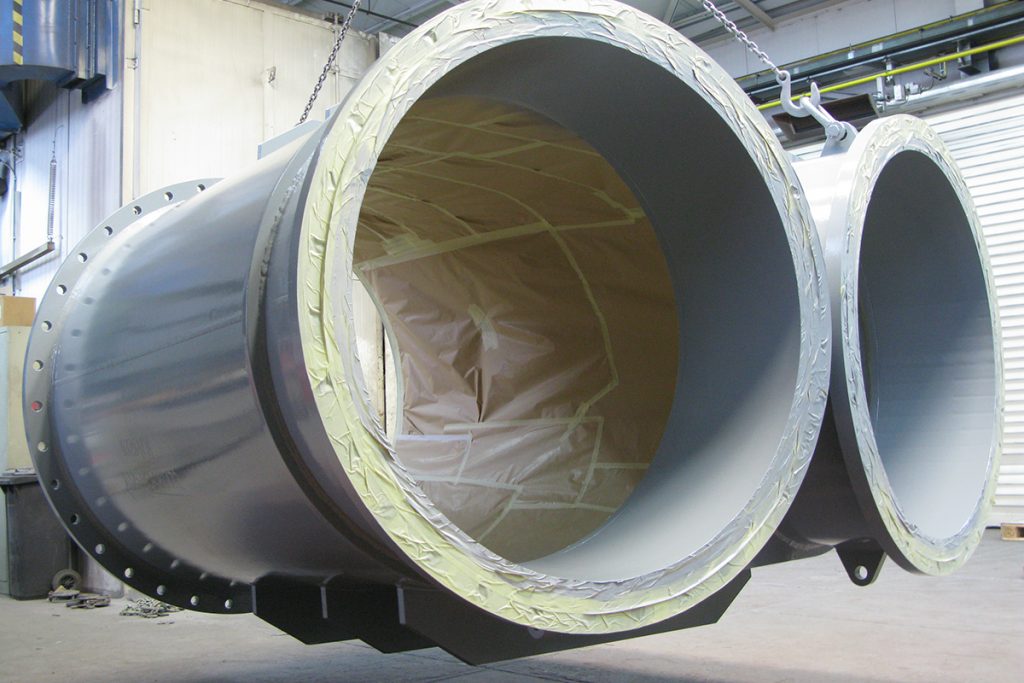
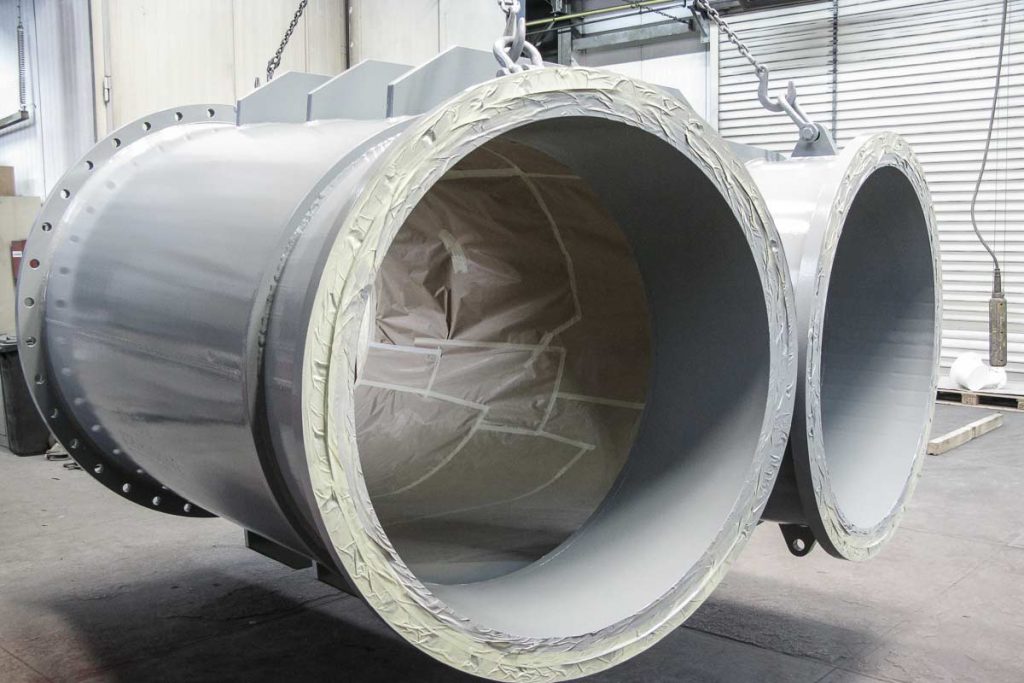
Inside the production
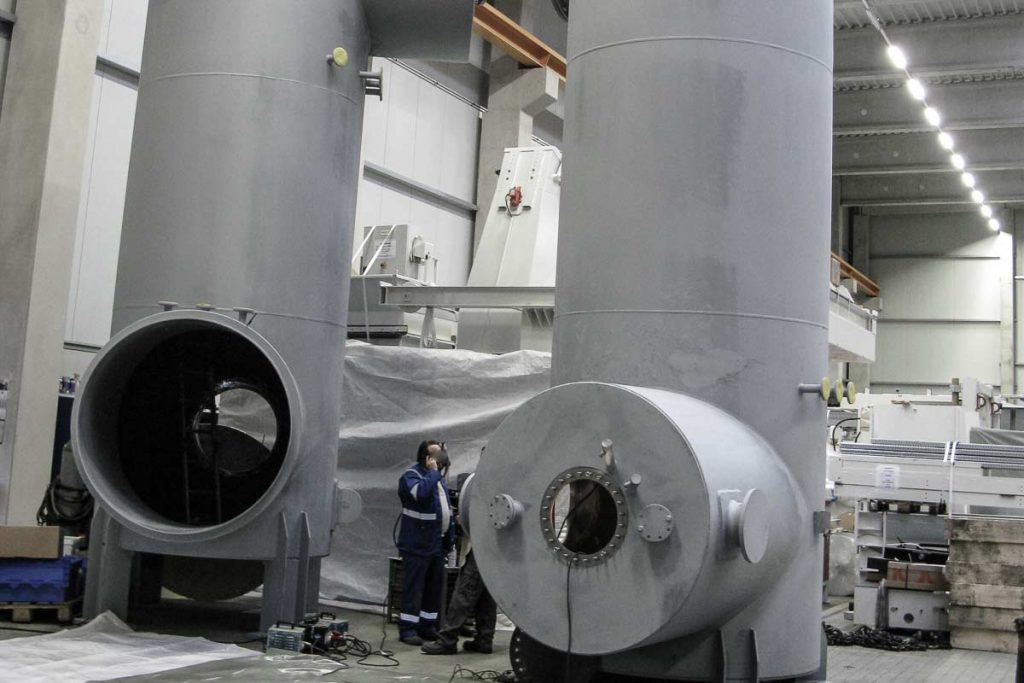
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Piping construction (complete piping systems, flange connections, segment bends, Y-pieces, reducers,Joining | – | – | – | – | Structural steels, Pressure vessel steels, Stainless steels, Heat-resistant steels |
| Vessel construction (pressure vessels, agitator vessels, storage vessels, storage silos)Joining | – | – | approx. 10 tonnes | – | Structural steel, Pressure vessel steels, Stainless steels, Heat-resistant steels |
| Apparatus engineering (static mixers, flare pipes, combustion chambers, wet deslaggers, slag dropJoining | – | 15 m | – | – | Steel, Stainless steel |
| 3D pipe laser cutting (pipes and profiles)Machining | nearly burr-free cut edges | – | – | – | – |
| Plasma cuttingMachining | – | – | – | – | – |
| Developed patternsMachining | – | – | – | – | – |
| Welding (manual and automatic welding, MAG/SAW, partially automated)Joining | – | – | – | – | Material groups 1.1, 1.2, 8 per CEN ISO/TR 15608 |
| Sandblasting (in own sandblasting booth, DIN EN ISO 12944-5 Part 4)Surface treatment | – | 3,650 mm × 3,250 mm | – | – | Metallic materials |
| Painting/coatingSurface treatment | – | – | – | – | – |
| Wear protection (lining with ceramic materials such as basalt or aluminium oxide ceramic;Surface treatment | – | – | – | – | Basalt, Aluminium oxide ceramic, Wear-resistant materials |
| Mechanical machiningMachining | – | – | – | – | – |
| Bending of cylindrical and conical components and apparatus partsForming | – | – | – | – | Steel |
| Contract manufacturing (various work)Joining | – | – | – | – | – |
8 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| 3D pipe laser cutting system | – | – | – | 2008 | Neunkirchen-Zeppenfeld |
| MAG welding system (partially automated welding) | – | – | – | – | Neunkirchen-Zeppenfeld |
| SAW welding system (partially automated welding) | – | – | – | – | Neunkirchen-Zeppenfeld |
| Welding system for flange pipes | – | – | – | – | Neunkirchen-Zeppenfeld |
| Sandblasting booth | – | – | Width 3,650 mm, depth 6,550 mm, height 3,250 mm | – | Neunkirchen-Zeppenfeld |
| Painting hall | – | – | – | – | Neunkirchen-Zeppenfeld |
| Bending machines (for cylindrical and conical components) | – | – | – | – | Neunkirchen-Zeppenfeld |
| Crane systems | – | – | – | – | Neunkirchen-Zeppenfeld |
Additional services
Certified quality
Manufacture in accordance with EN 13445, EN 13480 and AD 2000 with welders exclusively qualified to EN 9606-1 and welding coordination to EN ISO 14731. Acceptances take place in the company's own halls with independent experts from TÜV and Lloyd's Register; ultrasonic and radiographic testing is carried out in-house with external partners.
| Evidence | Neunkirchen (Zeppenfeld) |
|---|---|
| EN ISO 3834-2 | |
| AD 2000 HP 0 / HP 100R | |
| Directive 2014/68/EU (Module A2) | |
| Welding coordination EN ISO 14731 | |
| VT Level 2 per ISO 9712 | |
| PT Level 2 per ISO 9712 | |
| UKCA approval | |
| ISO 9001 |
From the forge to apparatus engineering
- 1961
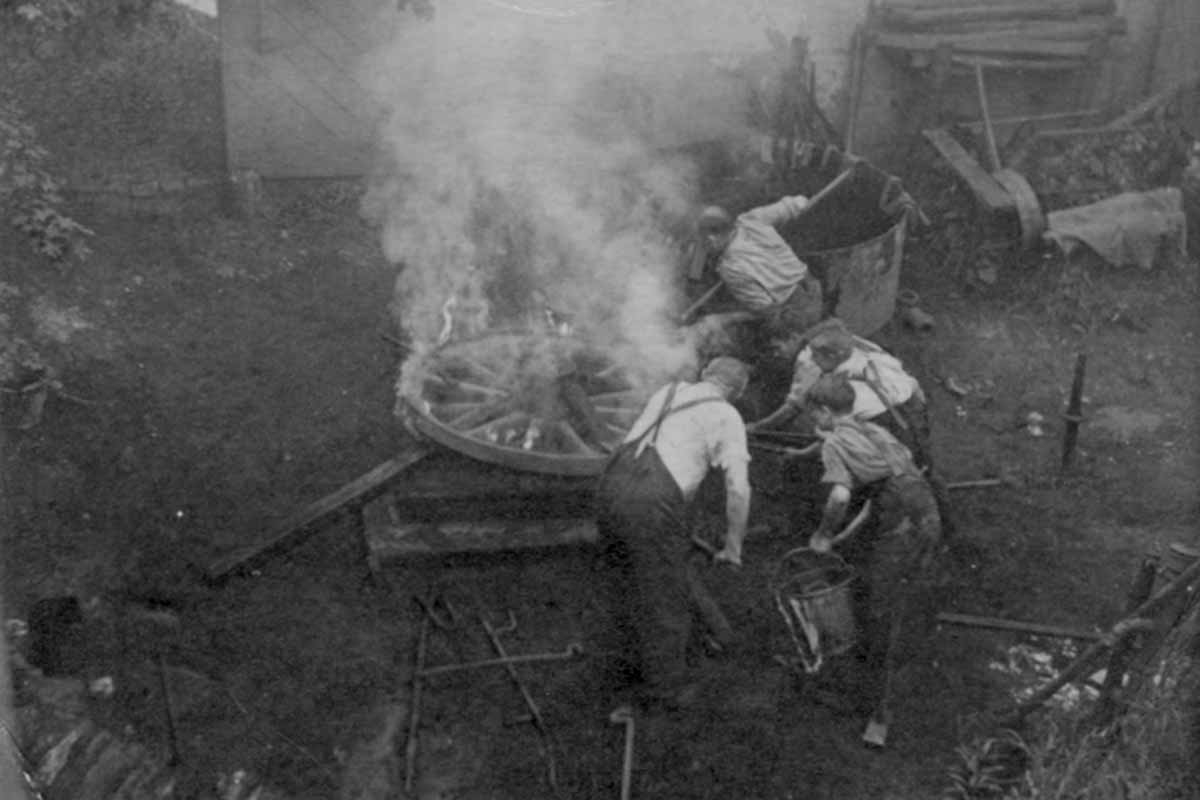
Founded by Karl-Adolf Welsch on the Eiserfelder Tretenbach, based on his grandfather's farriery in Siegen; contract work with forged parts and welding work
- 1968
Relocation to new premises in Herdorf (Rhineland-Palatinate)
- 1973
Expansion of production with an additional hall in Herdorf
- 1987
Second hall extension in Herdorf
- 1996
Conversion into a GmbH and handover to the next generation
- 2004
Relocation to Neunkirchen-Zeppenfeld (North Rhine-Westphalia) with crane systems, painting hall and sandblasting booth
- 2008
Groundbreaking ceremony for new hall; commissioning of the 3D pipe laser cutting system in November