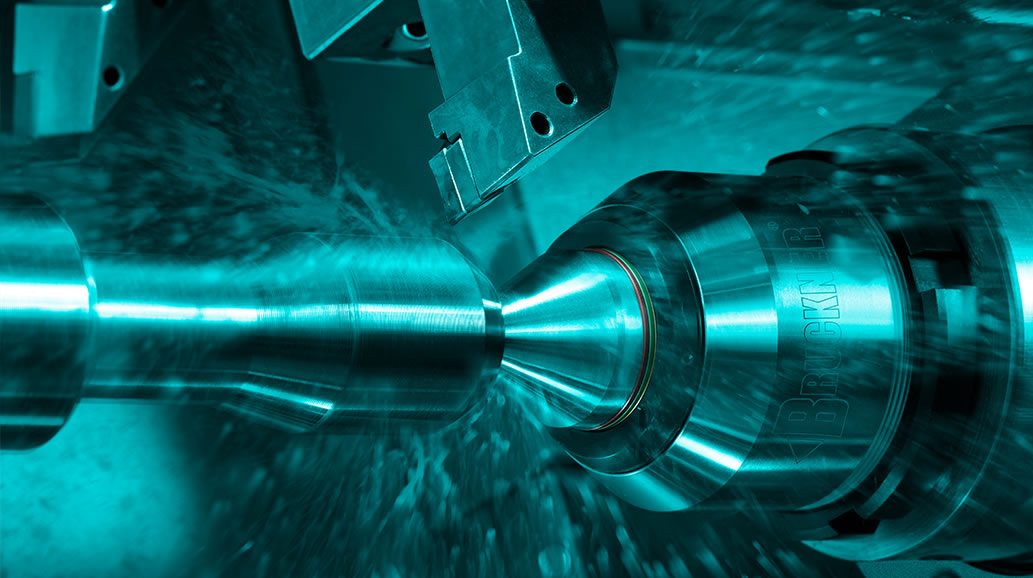
Development and manufacture of lathe centers, high-performance centers, face drivers and tailstock quills for turning and cylindrical grinding
Karl Bruckner GmbH
Weinstadt (Großheppach district)New on Amplifa
About Bruckner
Karl Bruckner GmbH is a medium-sized family business in its fourth generation, based in Weinstadt-Großheppach near Stuttgart. The company specializes in the development and manufacture of fixed and rotating lathe centers, rotating high-performance center points, face drivers (face plates), tailstock quills, taper sleeves and turning grippers. Production takes place in air-conditioned production halls in its own turning operation; materials used are alloyed tool steel, carbide (tungsten carbide) and, for custom designs, polycrystalline diamond (PCD). In addition, the company offers CARBIDOR drive-tip coating based on tungsten carbide as well as regrinding and re-coating services. Customers come from mechanical engineering, automotive, medical, aerospace, energy and environmental technology. Sales are handled worldwide through its own sales organizations and partner companies, including an own sales office in Mexico.
- Site
- Weinstadt
- Processes
- Manufacture of fixed lathe centers made of tool steel (similar to DIN 807 / DIN 806, with and, Manufacture of carbide lathe centers (solid carbide, forms V, GV, Z, GZ, HV, HM Ø 20-45 mm,, Manufacture of rotating high-performance centers (series S/A, NC, LK, LR, LD, C, ZA; shank forms, Manufacture of rotating high-performance center points (ZA series, 60°/75°, with, CARBIDOR® tungsten-carbide-based drive-tip coating for lathe centers and components (hardness, Through hardening and surface hardening of taper heads/shanks, Custom designs of fixed lathe centers with polycrystalline diamond (PCD) insert, Manufacture of mechanical face drivers (face plates), among others with vibration damping
- Materials
- Carbide (tungsten carbide), alloyed tool steel, polycrystalline diamond (PCD), stainless steel, CBN, Diamond (coating), Tungsten carbide (CARBIDOR® coating), CARBIDOR drive-tip coating
- Certificates
- Runout inspection report, Air-conditioned production, Gauge accuracy ≤ AT4 (DIN 228)
- Founded
- 1918
- Industries
- Mechanical engineering, Automotive engineering, Medical technology, Aerospace engineering, Energy technology, Environmental technology
- 01
Development and design
- 02
Turning
- 03
Heat treatment (through and surface hardening)
- 04
Grinding
- 05
CARBIDOR coating
- 06
Inspection (runout deviation with inspection report)
- 07
Worldwide sales
Materials & Processes
Carbide (tungsten carbide)
Used in solid-carbide lathe centers with sa·co safety core for roundness ≤ 0.8 μm.
alloyed tool steel
Base material for lathe centers, center points and housings, through- or surface-hardened.
polycrystalline diamond (PCD)
Material used for custom designs of fixed lathe centers.
CARBIDOR drive-tip coating
Tungsten-carbide-based coating (74-78 HRC, approx. 25 μm) to increase static friction between center and workpiece.
CBN
Coating material for drive-tip coatings on lathe centers.
stainless steel
Coatable material for components such as jaws and collets.
Locations
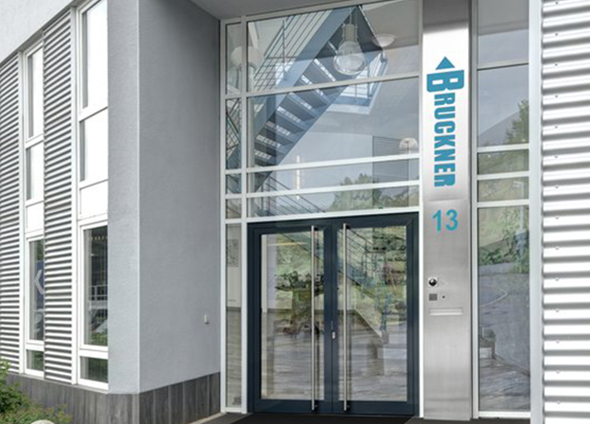
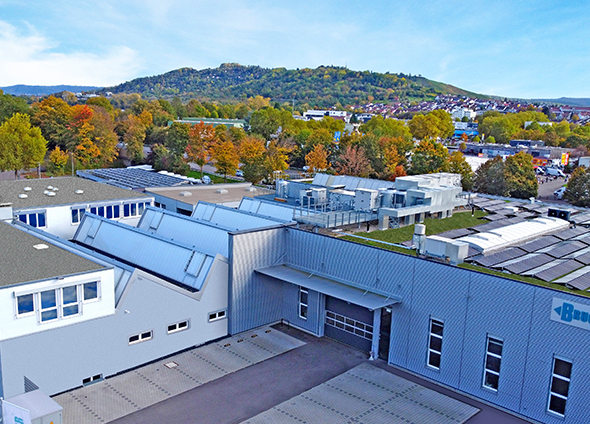
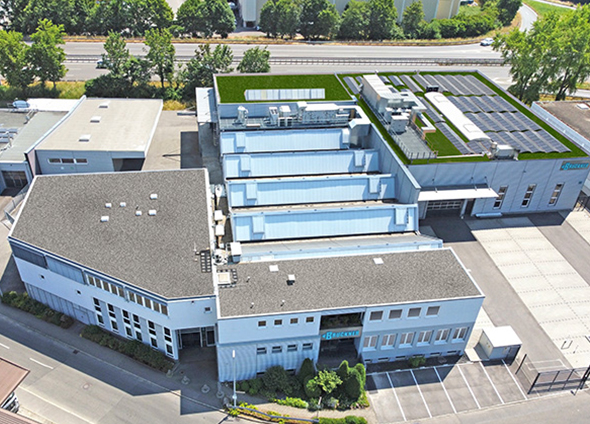
Weinstadt-Großheppach
DEHeadquarters with production and administration
- Materials
- Carbide, tool steel, PCD
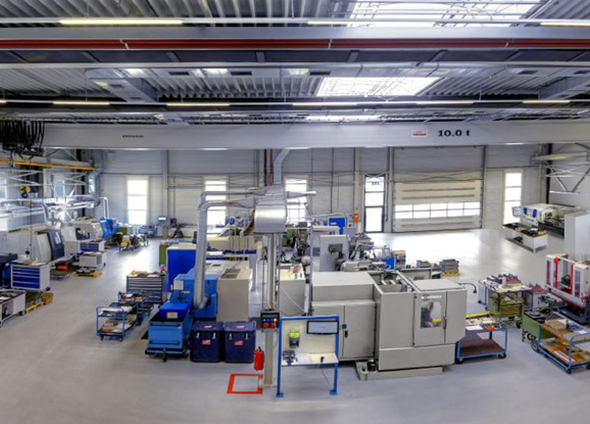
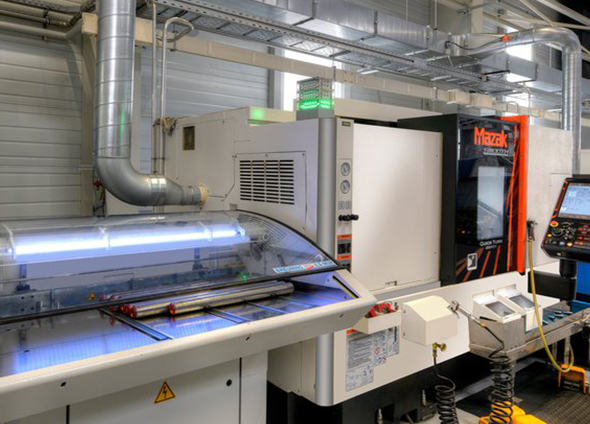
- Lathes (production hall 2020)
- Production machines (capacity expansion 2010)
- Ventilation and air-conditioning systems
- PV system
Components & Products
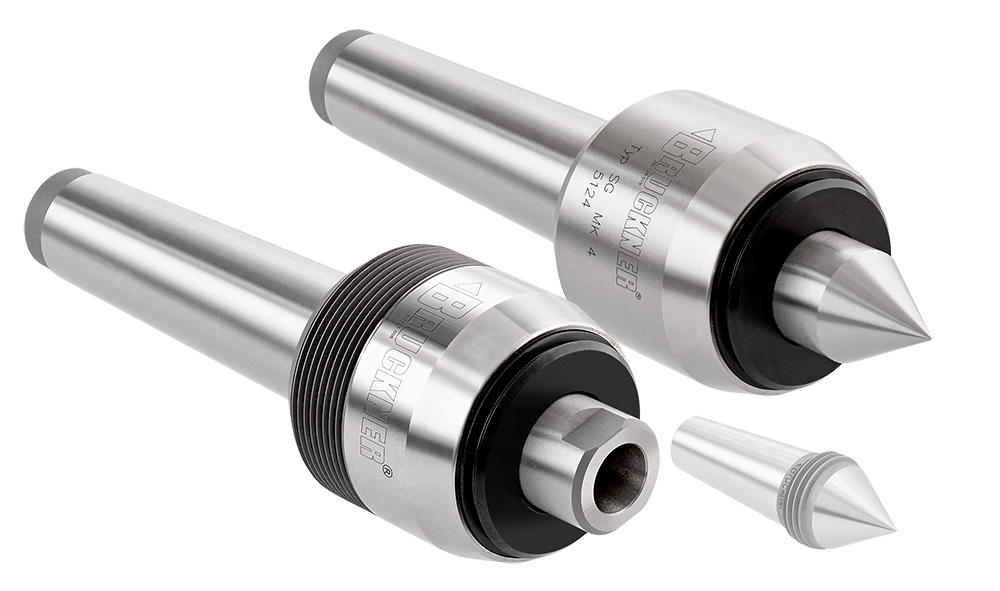
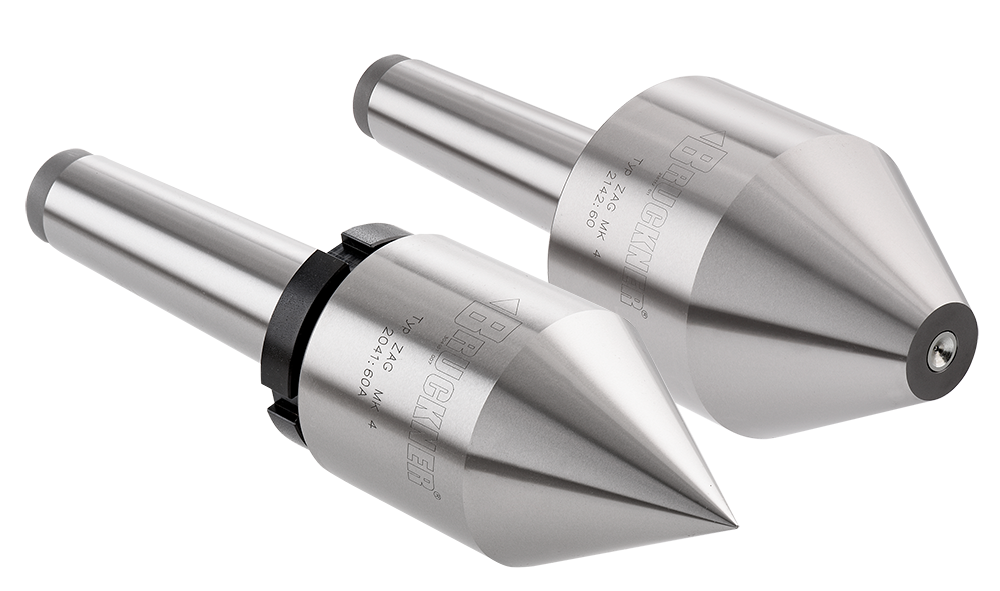
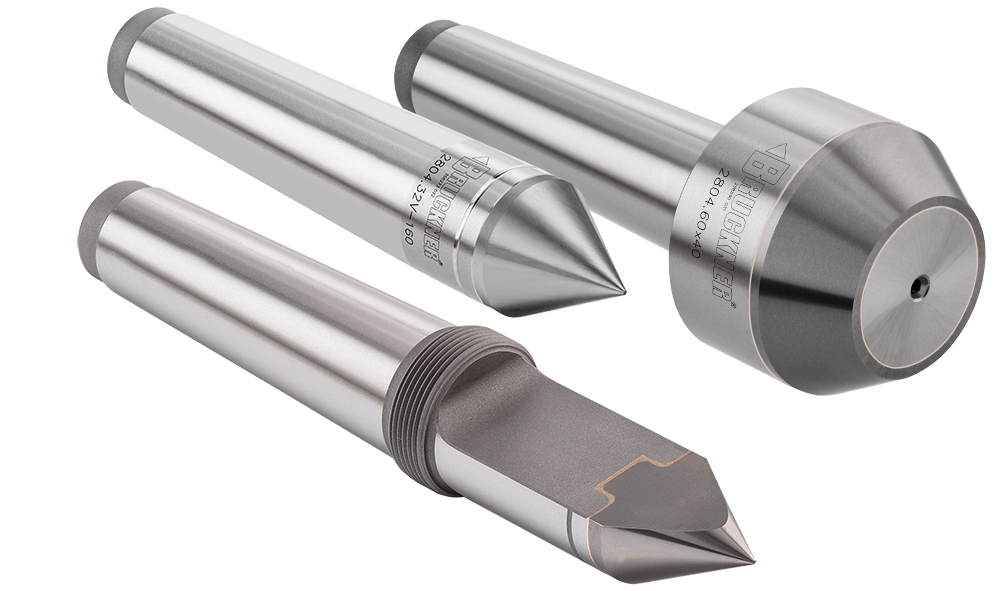
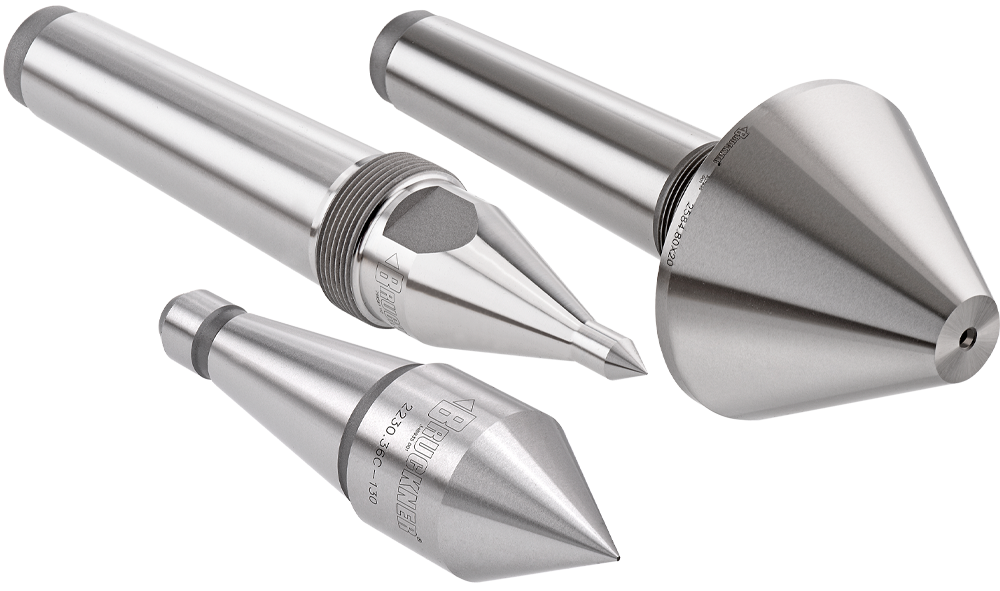
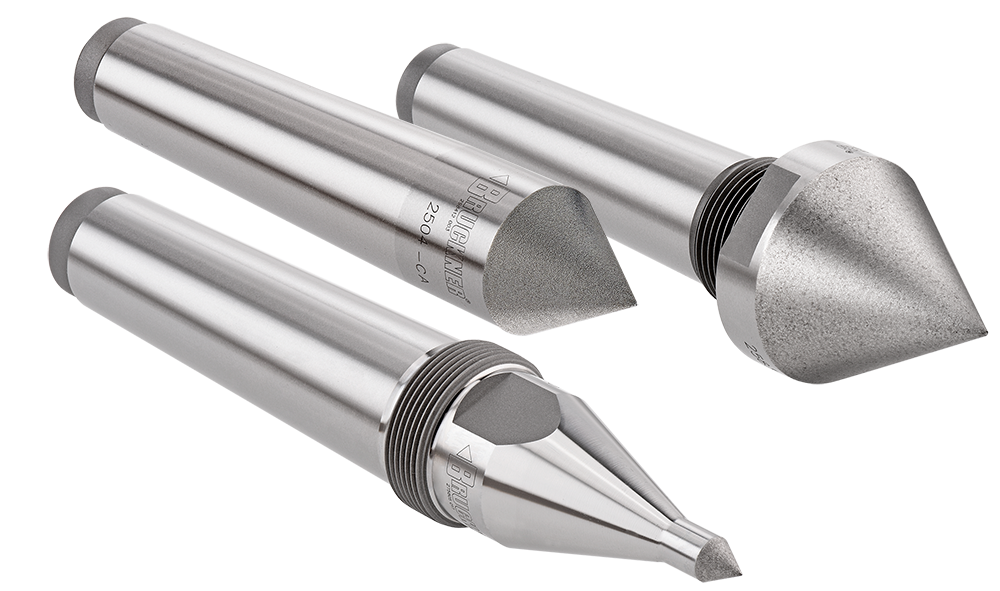
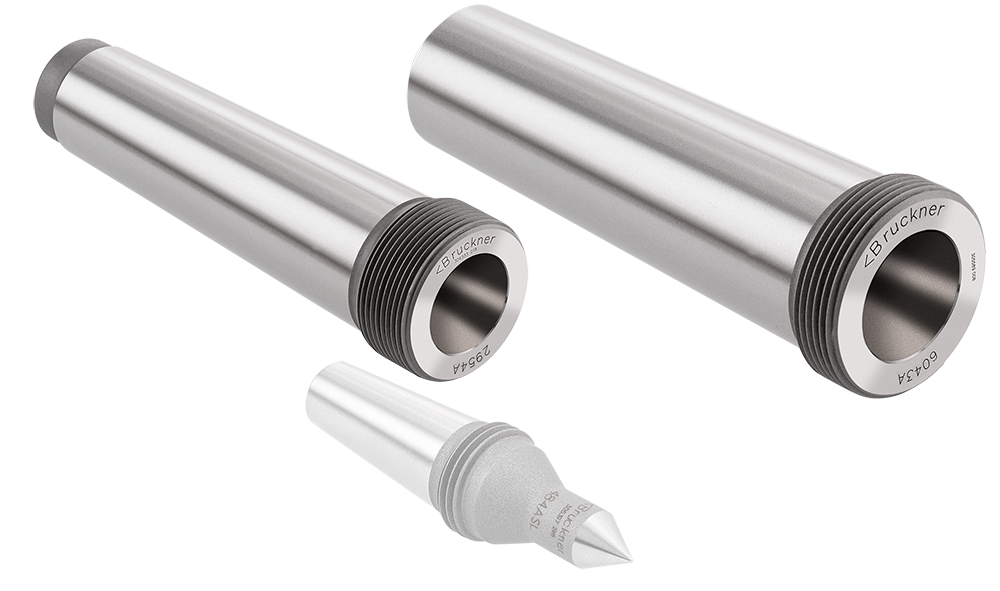
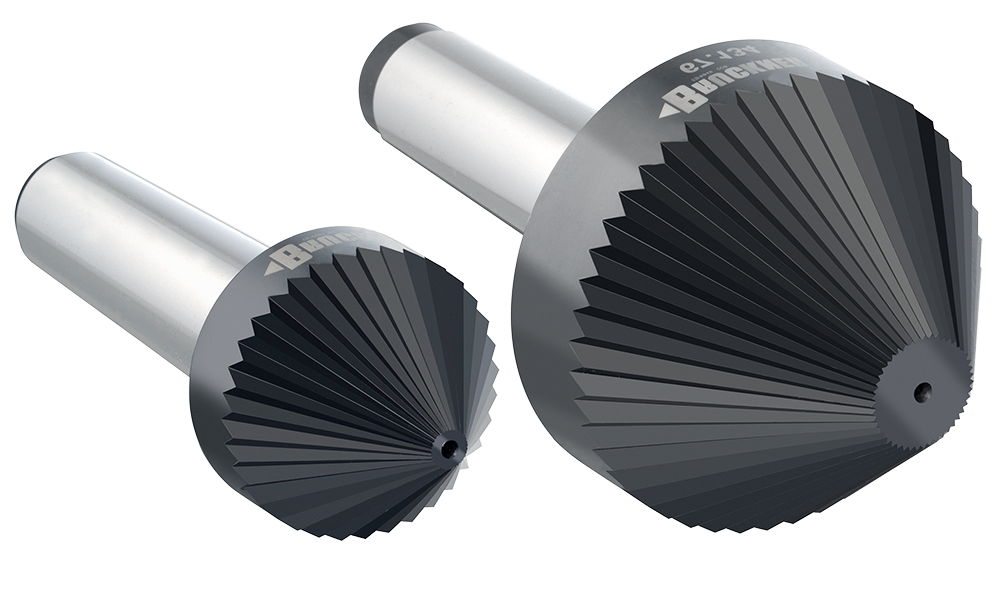
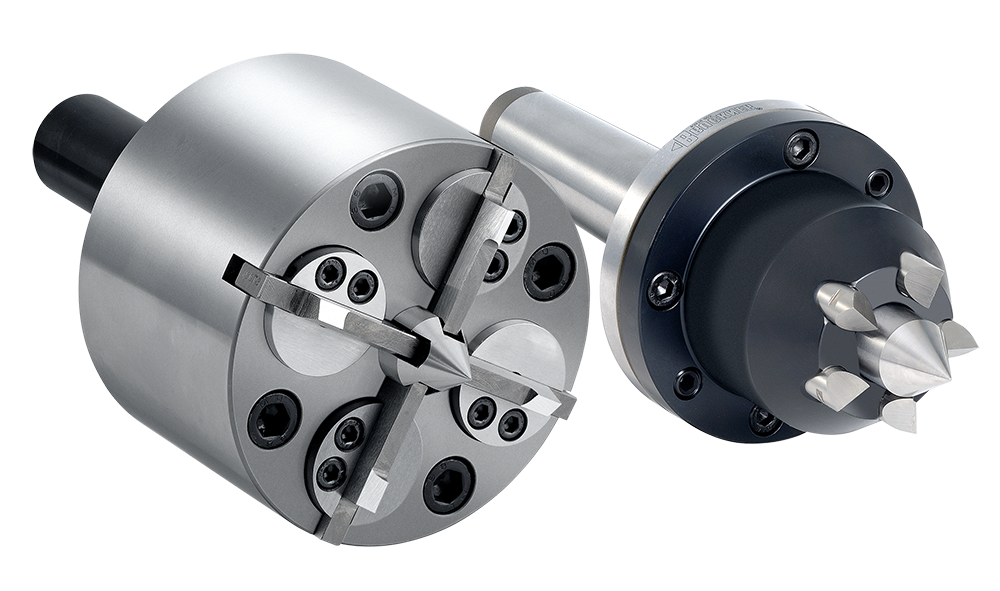
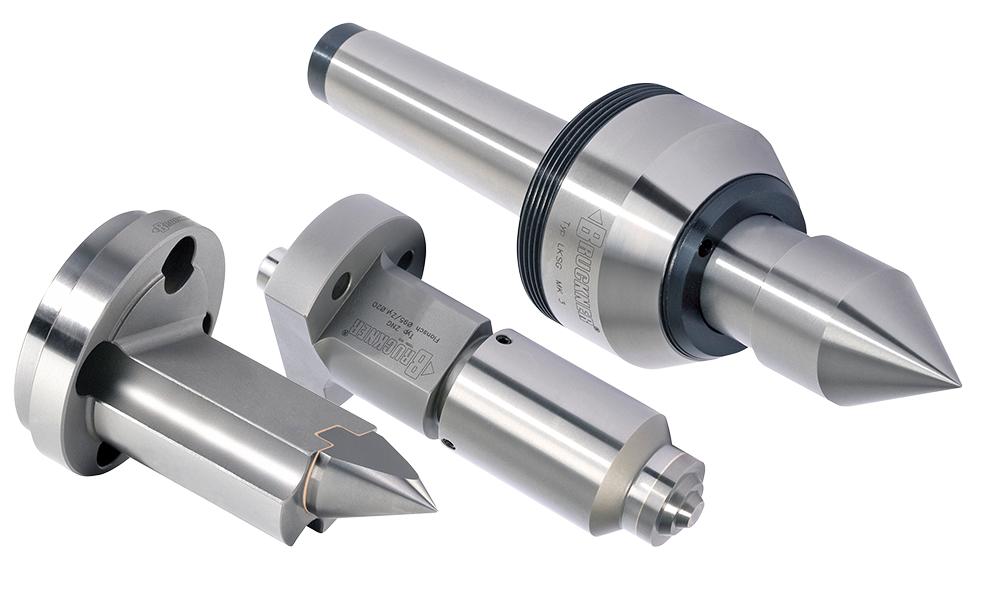
Inside the production
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Manufacture of fixed lathe centers made of tool steel (similar to DIN 807 / DIN 806, with andEngineering | – | – | – | – | alloyed tool steel |
| Manufacture of carbide lathe centers (solid carbide, forms V, GV, Z, GZ, HV, HM Ø 20-45 mm,Engineering | Roundness tolerance at the carbide ≤ 0.8 μm; | – | – | – | Carbide (tungsten carbide), alloyed tool steel (base material) |
| Manufacture of rotating high-performance centers (series S/A, NC, LK, LR, LD, C, ZA; shank formsEngineering | Runout deviation: precise version max. 0.005 mm, | – | – | – | alloyed tool steel, carbide (inserts) |
| Manufacture of rotating high-performance center points (ZA series, 60°/75°, withEngineering | Runout deviation: precise version max. 0.007 mm, | – | – | – | alloyed tool steel |
| CARBIDOR® tungsten-carbide-based drive-tip coating for lathe centers and components (hardnessSurface | Rz: CARBIDOR®-F 15-17 μm, CARBIDOR®-M | – | – | – | tool steel, stainless steel, jaws, collets |
| Through hardening and surface hardening of taper heads/shanksHeat treatment | – | – | – | – | alloyed tool steel |
| Custom designs of fixed lathe centers with polycrystalline diamond (PCD) insertEngineering | – | – | – | – | polycrystalline diamond (PCD), carbide, diamond, CBN |
| Manufacture of mechanical face drivers (face plates), among others with vibration dampingEngineering | – | – | – | – | – |
| Manufacture of tailstock quills with quill support (safety collar) and roller-bearing-mounted quillsEngineering | – | – | – | – | – |
| Manufacture of taper sleeves – spindle sleevesEngineering | – | – | – | – | – |
| Manufacture of turning grippersEngineering | – | – | – | – | – |
| Turning in own production (production hall for turning, 2020)Machining | – | – | – | – | – |
| Regrinding / renewal of CARBIDOR® coatings when wornSurface | – | – | – | – | tool steel |
2 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| Lathes (production hall for turning) | – | – | – | 2020 | Weinstadt-Großheppach |
| Production machines (capacity expansion 2010) | – | – | – | 2010 | Weinstadt-Großheppach |
Additional services
Quality
Production takes place under air-conditioned conditions at a high technical level; runout deviations are documented with an inspection report (high-precision versions max. 0.003 mm). Carbide lathe centers achieve roundness tolerances at the carbide of ≤ 0.8 μm with taper shank tolerance of ≤ AT4 according to DIN 228.
| Evidence | Weinstadt-Großheppach |
|---|---|
| Runout inspection report | |
| Air-conditioned production | |
| Gauge accuracy ≤ AT4 (DIN 228) |
History
- 1918
Foundation of a mechanical workshop in Stuttgart by Karl Friedrich Bruckner; construction of grinding stands and machinists' lathes, start of production of fixed lathe centers.
- 1920
First rotating tailstock center “Centro” as one of the pioneers.
- 1931
Son Karl Georg takes over after the founder's death; development of a standard range of fixed and rotating centers.
- 1940
Lathe centers with carbide inserts added to the sales program.
- 1963
Relocation of the company to Großheppach (25 km from Stuttgart).
- 1969
Expansion with fixed lathe centers and carbide lathe centers works standard.
- 1976
Expansion of the delivery program to include mechanical face drivers.
- 1989
Patented safety core (sa·co) for solid-carbide lathe centers.
- 1994
Takeover of Bokö face plates and rotating centers from competitor Bohner & Köhle GmbH.
- 1996
Patenting of the mechanical face driver with vibration damping and of the tailstock quill support via safety collar.
- 1997
Expansion with spring-loaded centers of the LR and LD series.
- 2007
Rotating centers with VDI, Capto and cylindrical shanks for multi-spindle machines.
- 2008
Establishment of worldwide factory representations; own sales office in Mexico.
- 2010
Expansion with an additional production hall and new machines.
- 2018
First custom designs of fixed lathe centers with PCD inserts; 100th anniversary.
- 2020
New production hall for turning with PV system.
- 2022
Renovation of a production hall from 1964 with ventilation and air-conditioning system.