Manufacturer of crane wheels, wheel assemblies, wheel blocks, buffers and rope sheaves for crane and machinery construction
Karl Georg GmbH
Ingelbach-Bahnhof (headquarters and plant)New on Amplifa
About Karl Georg
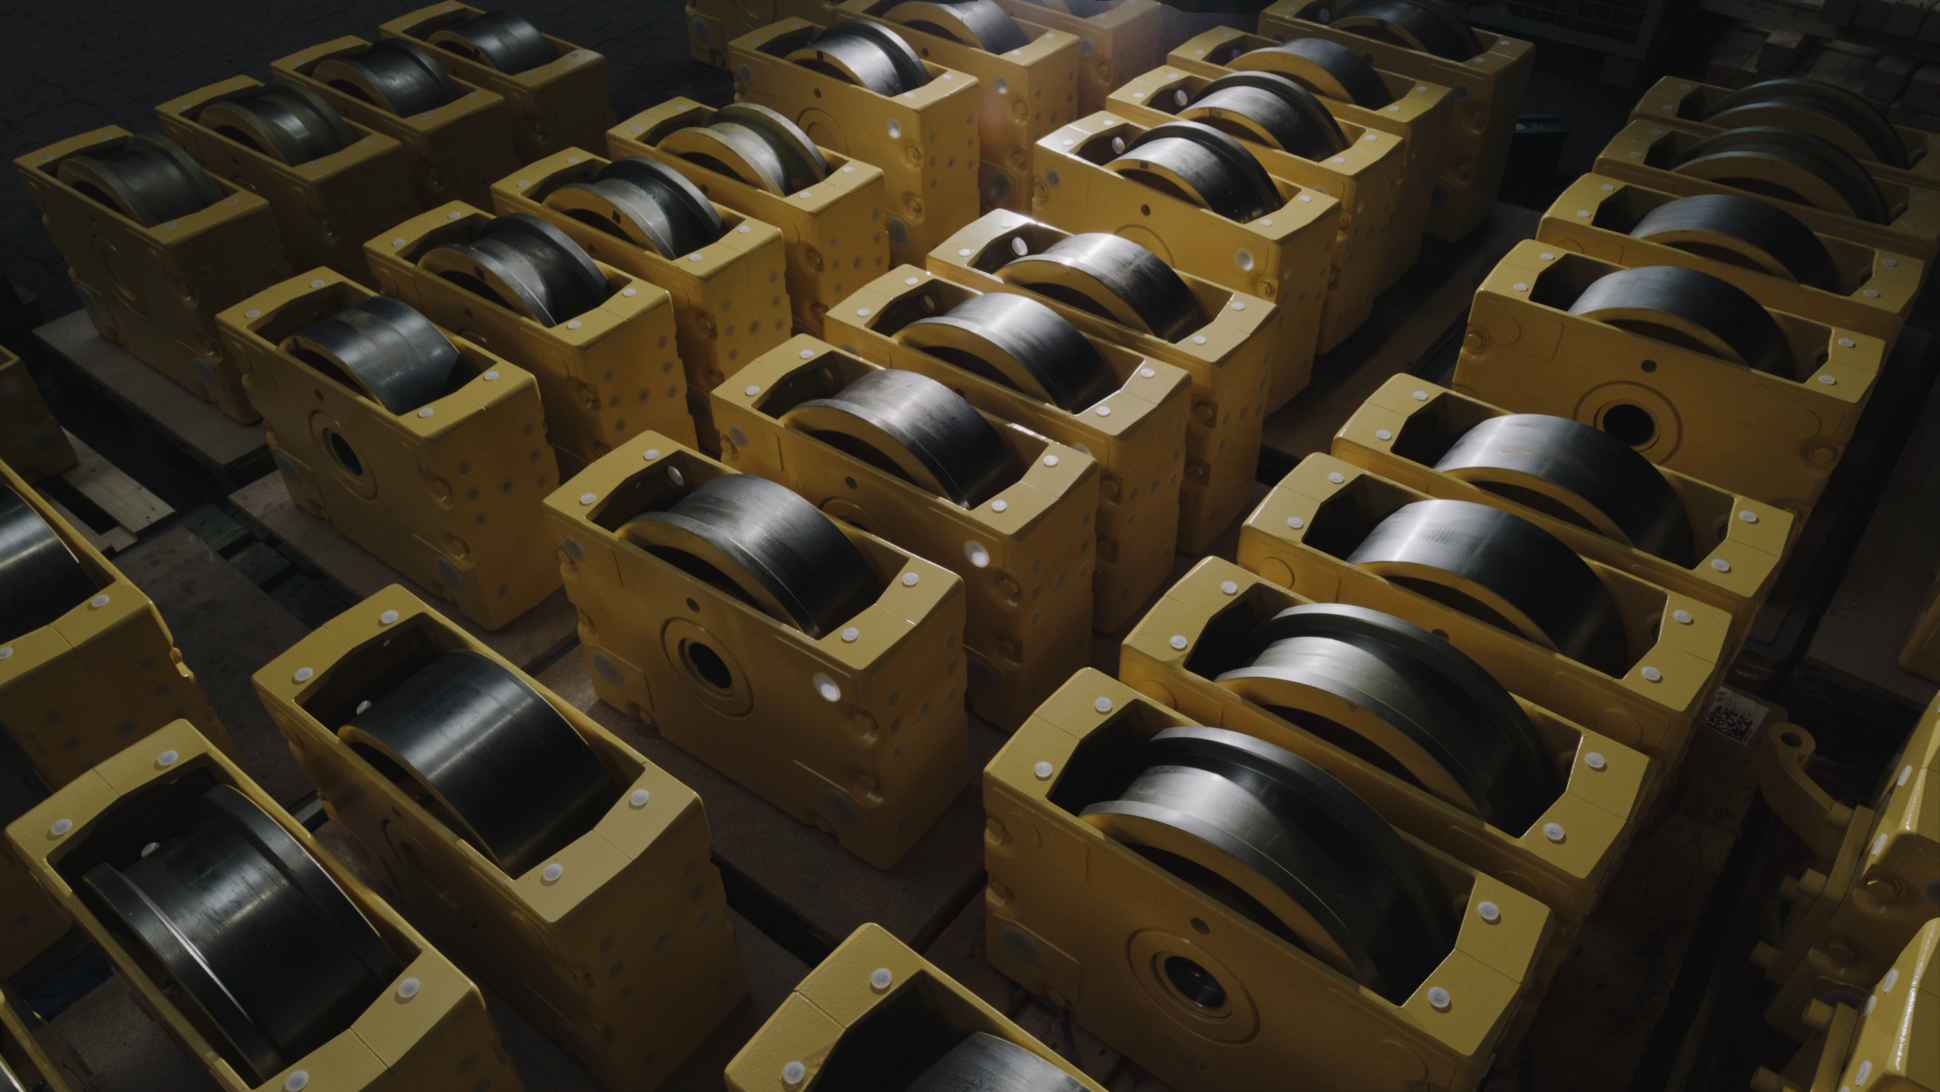
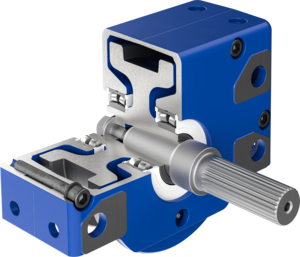
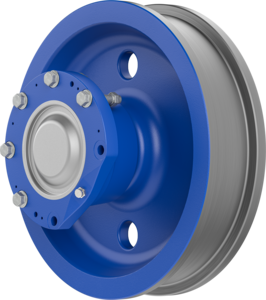
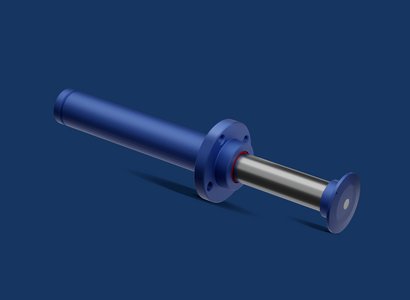
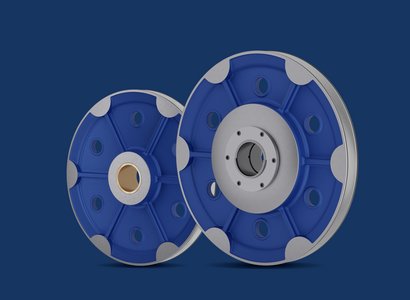
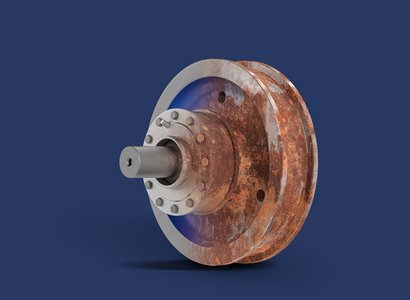
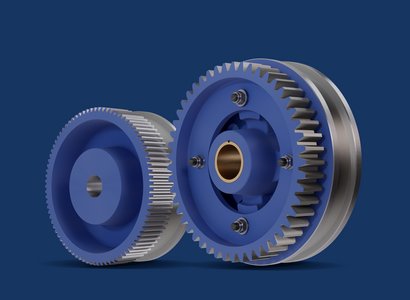
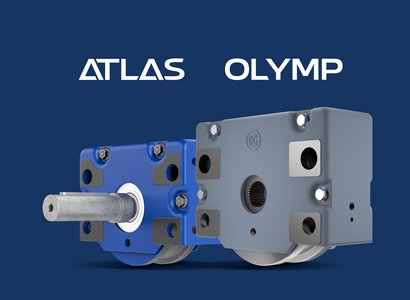
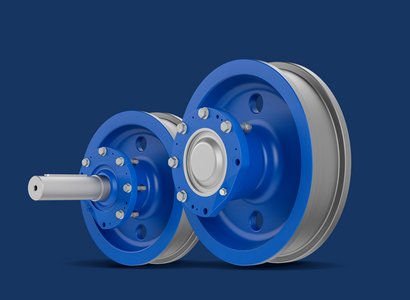
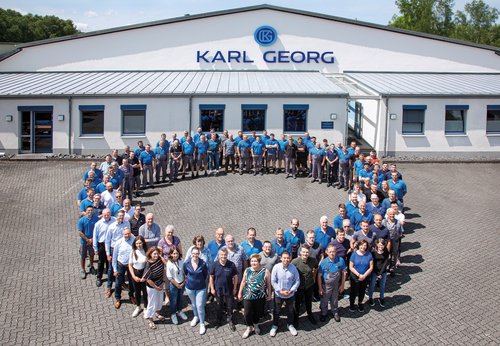
Karl Georg GmbH is a family-owned manufacturer of crane components headquartered in Ingelbach-Bahnhof in the Westerwald region. The company produces crane wheels with diameters from 100 to 1250 mm, drive and idler wheel assemblies, the ready-to-install wheel block systems ATLAS and OLYMP, hydraulic and elastomer buffers as well as rope sheaves to DIN 15417/15418/15421/15422. Production is carried out from forged steel, cast steel and spheroidal graphite cast iron according to DIN, TGL or in-house standards or to customer drawings from lot size 1. The in-house manufacturing depth includes CNC machining, gear production (module up to 14), slip-free hardening of running surfaces, painting as well as maintenance, repair and general overhaul, including of third-party products. Customers include crane manufacturers, plant and machinery builders and operators from sectors such as the energy industry, mining, conveying systems and ironworks; the KARL GEORG GROUP supplies more than 3,000 OEM customers in 55 countries.
- Site
- Ingelbach-Bahnhof
- Processes
- Manufacture of crane wheels (DIN, in-house standard, TGL, to customer drawing), Machining (CNC turning and milling machines), Forging (die forging, open-die forging), Casting (cast steel, spheroidal graphite cast iron), Slag/steel mill (own electric steel mill, historical), Heat treatment (slip-free hardening of running surface/rope groove), Gear production (gear rims, pinions, hub gearing, module up to 14), Painting/Coating (modern painting and drying system)
- Materials
- Forged steel, Cast steel, Spheroidal graphite cast iron, C45 (die-forged), GE420 (GS-70), G42CrMo4+QT, 42CrMo4+QT (die-forged), C45 N
- Certificates
- ISO 9001:2015, ISO 14001:2015, ISO 45001, DIN EN 16247-1
- Founded
- 1925
- Employees
- approx. 145–150
- Industries
- Crane construction, Plant construction, Mechanical engineering, Automotive, Energy sector, Mining
- 01
Forging/Casting
- 02
Heat treatment
- 03
CNC machining
- 04
Gear production
- 05
Painting/Coating
- 06
Testing
- 07
Assembly
- 08
Maintenance/Repair
Materials & Processes
C45 (die-forged)
Wheel body Ø 160–500 mm, running surface slip-free hardened (HRc 38–46, hardening depth 3–4 mm).
42CrMo4+QT (die-forged)
Quenched and tempered forged steel for highly stressed wheel bodies of crane wheels and wheel assemblies.
GE420 (GS-70) cast steel
Wheel body material for wheels from Ø 630 mm and TGL versions.
G42CrMo4+QT (GS-42CrMo4V) cast steel
Quenched and tempered cast steel as an alternative wheel body material.
S355J2 G3 (St 52-3)
Material for corner brackets according to TGL 34 968.
Spheroidal graphite cast iron
Cast material for wheels according to DIN, TGL or customer drawing.
Vulkollan (coating)
Running surface coating for horizontal roller guides.
PA12G (coating)
Plastic coating for horizontal roller guides.
Heat treatment (slip-free hardening)
Slip-free hardening of running surfaces and rope grooves, hardening depth 3–4 mm.
Sites
Ingelbach-Bahnhof
DEHeadquarters with production, administration and quality management
- Lot size
- Lot size 1 to series production
- Materials
- Forged steel, cast steel, spheroidal graphite cast iron
- CNC lathes
- CNC milling machines
- Painting and drying system with energy recovery
- Solar system approx. 800–850 kWp
Components
Inside the production
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Manufacture of crane wheels (DIN, in-house standard, TGL, to customer drawing)Machining | – | – | – | Lot size 1 | Forged steel, Cast steel, Spheroidal graphite cast iron, C45, GE420 (GS-70), G42CrMo4+QT (GS-42CrMo4V), 42CrMo4+QT |
| Machining (CNC turning and milling machines)Machining | – | – | – | – | Steel |
| Forging (die forging, open-die forging)Forming | – | – | – | – | Forged steel, C45, 42CrMo4+QT |
| Casting (cast steel, spheroidal graphite cast iron)Casting | – | – | – | – | GE420 (GS-70), Cast steel, Spheroidal graphite cast iron |
| Slag/steel mill (own electric steel mill, historical)Casting | – | – | – | – | Steel |
| Heat treatment (slip-free hardening of running surface/rope groove)Heat treatment | Hardening depth 3 – 4 mm | – | – | – | C45, Cast steel, Forged steel |
| Gear production (gear rims, pinions, hub gearing, module up to 14)Machining | – | – | – | – | Steel |
| Painting/Coating (modern painting and drying system)Surface | – | – | – | – | Steel |
| Ultrasonic testing (UT)Testing | – | – | – | – | Steel |
| Crack testing MT/PT (magnetic particle/dye penetrant testing)Testing | – | – | – | – | Metallic workpieces |
| Hardness testingTesting | – | – | – | – | Steel |
| Material inspection certificates 2.1 to 3.2 according to DIN EN 10204Testing | – | – | – | – | Metallic workpieces |
| Assembly of wheel assemblies, wheel blocks, travel gearAssembly | – | – | – | – | Steel |
| Maintenance, repair, general overhaul of crane wheels, wheel assemblies, wheel blocks, travel gearAssembly | – | – | – | – | Steel |
| Manufacture of hydraulic buffers (CERTUS) and elastomer buffersAssembly | – | – | – | – | – |
| Manufacture of rope sheaves according to DIN 15417/15418/15421/15422Machining | – | – | – | – | Cast steel, Forged steel |
| Design/development of crane components (custom manufacturing to customer drawing)Engineering | – | – | – | Quantity 1 | – |
6 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| CNC lathes | – | – | – | – | Ingelbach-Bahnhof |
| CNC milling machines | – | – | – | – | Ingelbach-Bahnhof |
| Open-die forge | – | – | – | – | Neitersen (historical) |
| Electric steel mill | – | – | – | 1965 | Neitersen |
| Painting and drying system with energy recovery | – | 1 | – | – | Ingelbach-Bahnhof |
| Solar system (production energy) | – | – | 800–850 kWp | – | Ingelbach-Bahnhof |
Additional services
Reference customers
Quality
Quality control with certified testing methods Level 2: ultrasonic testing (UT), dye penetrant testing (PT), magnetic particle crack testing (MT), hardness testing (HRC/HV/HB) and optical 3D measurement. Material inspection certificates 2.1–3.2 according to DIN EN 10204 as well as re-stamping authorization for metallic materials.
| Evidence | Ingelbach-Bahnhof |
|---|---|
| ISO 9001:2015 | |
| ISO 14001:2015 | |
| ISO 45001 | |
| DIN EN 16247-1 |
History
- 1925
Karl Georg founds the company in Neitersen; production of buffers, truck trailers and rubber-tired farm wagons with its own smithy and steel mill.
- 1940
Start of production of sleeve buffers for railway wagons.
- 1945
Destruction of the plant by bombing on 21.02.1945; rebuilding between the B 256 and the railway line.
- 1965
Commissioning of the only steel mill in the Westerwald to this day, in Neitersen.
- 1966
Start of crane wheel production in Neitersen; production begins at the Ingelbach site.
- 1975
Production of the first wheels with gearing.
- 1985
Michael Schnaufer, grandson of the founder, takes over the company.
- 1993
Development of the first detachable wheel block.
- 1998
Relocation of Karl Georg Stahlherstellungs- und Verarbeitungs GmbH to Ingelbach-Bahnhof.
- 2022
Renaming to Karl Georg GmbH with a new corporate appearance.
- 2023
Receipt of ISO 14001 certification (March 2023).
- 2025
100th anniversary; founding of companies in India and Spain; Kathrin Schnaufer takes over; new products (OLYMP wheel block) and construction of a new production hall and administration building.
- 2026
ISO 45001 certification (March 2026); farewell to Tim Winkel as Managing Director at the beginning of the year.