Development and manufacturing of technical springs, fine-blanked and stamped parts, and plastic-metal assemblies for international industries.
KERN LIEBERS GmbH & Co. KG
Schramberg · Göppingen · Villingen-Schwenningen · Wuppertal · Schwabmünchen · Rieden · Schalksmühle · Hardt · Reutlingen · Myszków (PL) · České Budějovice (CZ) · Sancraiu de Mures (RO) · Rayong (TH)New on Amplifa
About KERN LIEBERS
KERN LIEBERS is a globally active manufacturer of technical springs, stamped, fine-blanked and stamped-bent parts, and plastic and metal assemblies headquartered in Schramberg. The company manufactures to customer specifications – from prototypes and lot size 1 through to high-volume series – including tension, compression, torsion, wave, power spring, power strip and contact springs, precision-machined components and fully automated assembled modules. Manufacturing depth ranges from fine blanking, stamping, coiling and winding, laser technology (welding, cutting, drilling, hardening, marking) and precision machining (turning, milling, multi-spindle drilling, ultra-precision thickness grinding) to heat treatment, surface treatment, plastic injection moulding and assembly. Materials include hot-rolled and cold-rolled strip, stainless steels, non-ferrous and non-precious metals, specialty materials, aluminium and copper alloys as well as plastics. Products are used in mobility/automotive, electromobility, energy and building technology, medical technology, machinery and plant engineering, precision mechanics, the watch industry, household appliances and consumer goods. The KERN LIEBERS Group employs around 5,850 people at more than 35 locations in Europe, North and South America and Asia.
- Site
- Schramberg
- Processes
- Fine blanking, Stamping, Stamped bending, Coiling (CNC coiling machines for tension, compression and torsion springs), Winding of wire springs, Winding of strip springs (power springs), Wire bending (including 3D bent parts, up to 21 CNC axes), Laser welding (continuous wave and pulsed, up to 8 kW, infrared and green)
- Materials
- Hot- and cold-rolled strip, Stainless steels, Non-ferrous metals, Non-precious metals, Specialty materials, Gilded copper, Bronze, Spring steel (with coatings)
- Certificates
- IATF 16949:2016, ISO 9001:2015 (group certificate), ISO 9001:2015 (Kern Liebers Göppingen GmbH), IATF 16949:2016 (Kern Liebers Göppingen GmbH), ISO 14001 (group certificate), ISO 50001 (group certificate), ISO 14064 + GHG Protocol, ISO 14067, ISO 13485 (KERN LIEBERS Schwabmünchen GmbH / Lienberg GmbH), ISO 9001, IATF 16949, ISO 13485, ISO 14001, ISO 50001
- Employees
- 5,850
- Industries
- Mobility / Automotive, Electromobility, Energy & Building Technology, Medical Technology, Machinery & Plant Engineering, Consumer Goods
- 01
Research & Development
- 02
Engineering (special-purpose machinery, materials engineering, prototype
- 03
Fine blanking / stamping / stamped-bending or coiling & winding / wire bending
- 04
Laser technology & precision machining
- 05
Heat treatment
- 06
Surface treatment
- 07
Joining technology & assembly of modules
- 08
Analysis & Testing
- 09
Cleaning & Packaging
Components
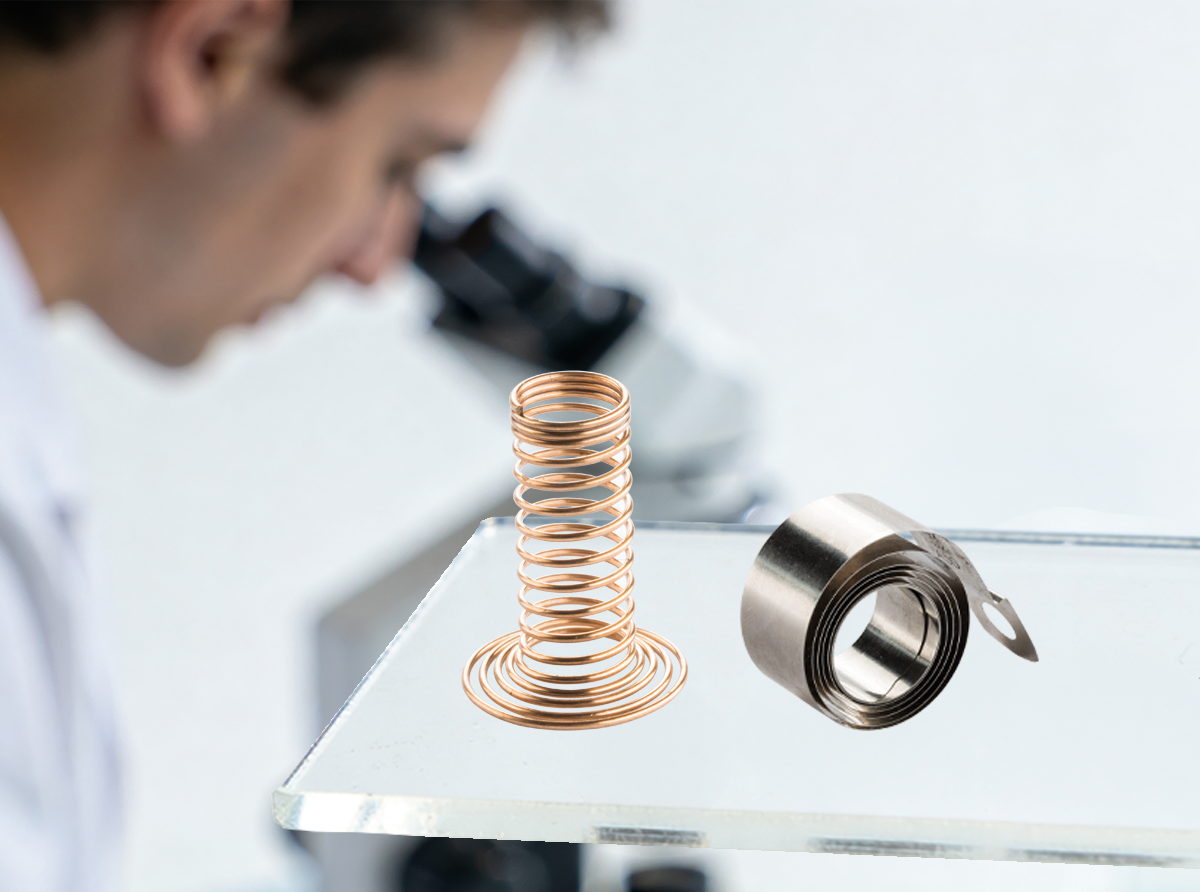
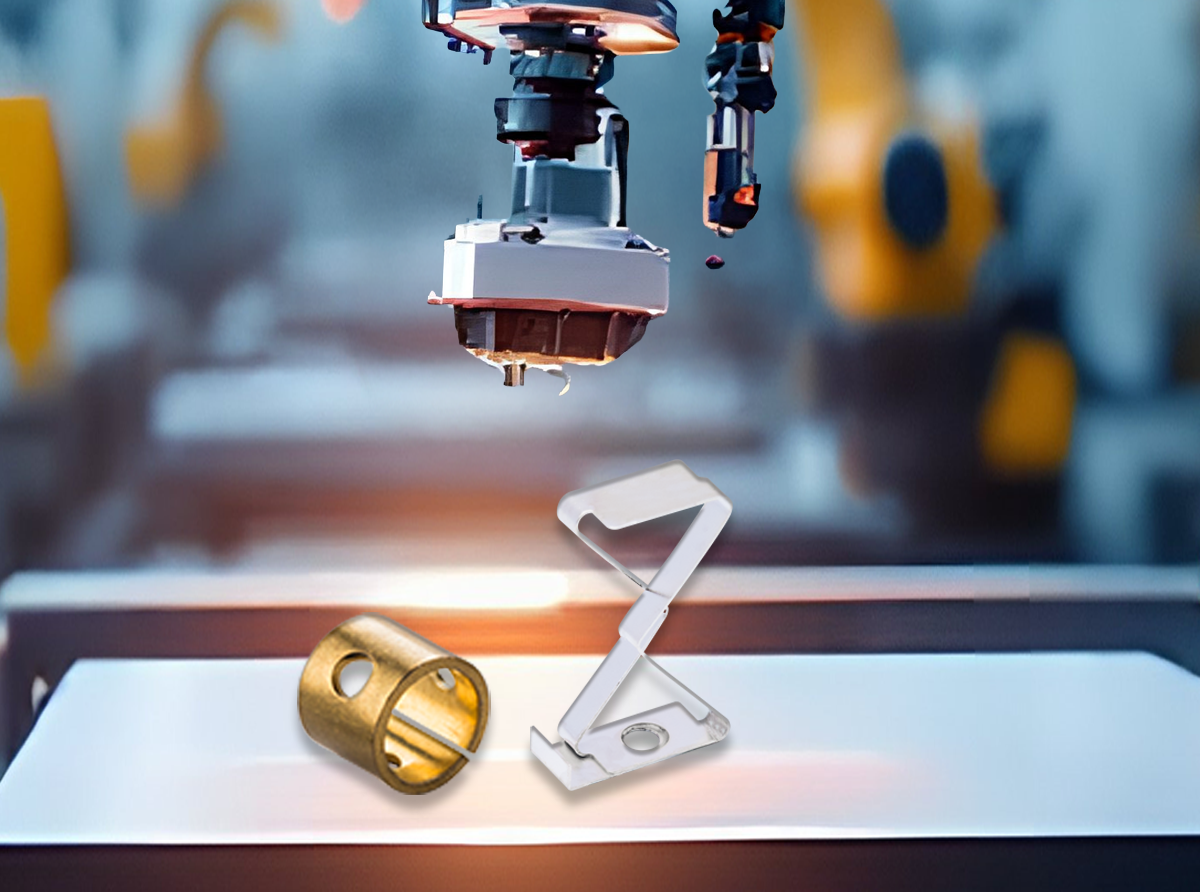
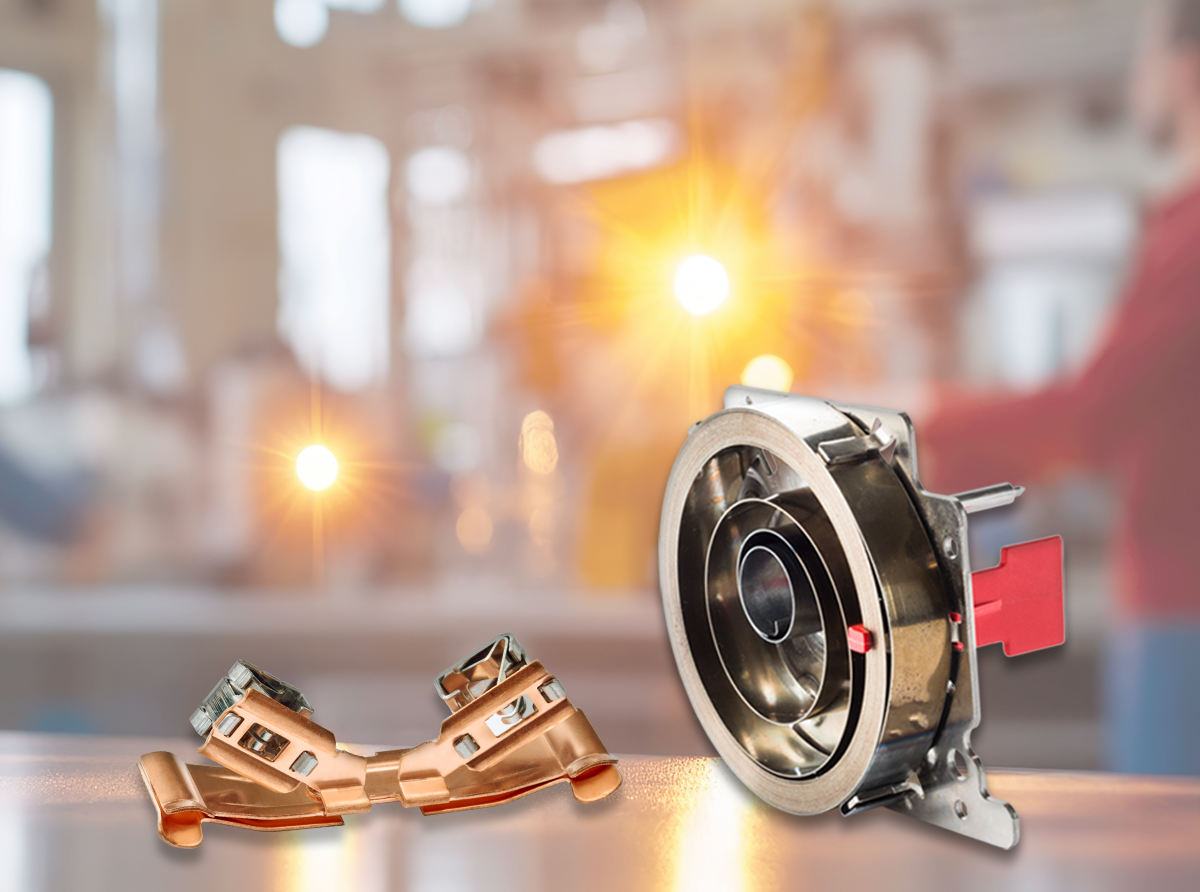
Inside the production
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Fine blankingForming | – | – | – | – | Hot- and cold-rolled strip, Stainless steels, Non-ferrous metals, Non-precious metals |
| StampingForming | – | – | – | – | Hot- and cold-rolled strip, Stainless steels, Non-ferrous metals, Non-precious metals, Specialty materials |
| Stamped bendingForming | – | – | – | – | Hot- and cold-rolled strip, Stainless steels, Non-ferrous metals, Non-precious metals, Specialty materials |
| Coiling (CNC coiling machines for tension, compression and torsion springs)Forming | – | – | 0.3 mm wire diameter – 13 mm wire diameter (end grinding | – | Spring steel, stainless wires, special alloys |
| Winding of wire springsForming | – | – | – | – | Wire spring materials |
| Winding of strip springs (power springs)Forming | – | – | – | – | Strip steel |
| Wire bending (including 3D bent parts, up to 21 CNC axes)Forming | – | – | – | – | Wire, pre-coated wires |
| Laser welding (continuous wave and pulsed, up to 8 kW, infrared and green)Joining | – | – | – | – | Steel alloys, Aluminium alloys, Copper alloys |
| Laser drilling (diameter 30–100 µm)Machining | – | – | – | – | Stainless steel |
| Laser marking (DMC, QR codes, barcodes, plain text)Surface | – | – | – | – | Steel alloys, Aluminium alloys, Copper alloys |
| Laser hardening (up to 2 kW)Heat treatment | – | – | – | – | Steel (carbon) |
| Laser cutting (up to 8 kW)Machining | – | – | – | – | Steel alloys, Aluminium alloys, Copper alloys |
| Laser deburringSurface | – | – | – | – | Stainless steel |
| Machining – turningMachining | IT 7 (18 µm in the diameter range up to 25 mm) | – | 2.5 mm – 10 mm (small-part range medical/watch | – | Stainless steels, Non-precious metals, Special alloys |
| Milling / multi-spindle milling (up to 4 workpieces simultaneously, 5-axis machining)Machining | – | – | – | – | – |
| Multi-spindle drilling / cam-controlled multi-spindle drilling (up to 50 parallel tools)Machining | – | – | – | – | – |
| Spring end grinding (through-feed grinding from 0.3 mm to 1.5 mm wire diameter; end grinding up toMachining | – | – | – | – | patented drawn wires, oil-hardened and tempered wires, stainless wires, special alloys |
| Ultra-precision thickness grinding (Ø 4–80 mm, thickness 0.2–5 mm)Machining | Thickness, parallelism, flatness < 2 µm · Rz < 0.6, Ra < 0.1 | – | – | – | Stainless steels, Non-precious metals, Special alloys |
| Electro-/chemical deburringSurface | – | – | – | – | – |
| PolishingSurface | – | – | – | – | – |
| Ball and glass bead blastingSurface | – | – | – | – | – |
| Tumble finishing/vibratory finishingSurface | – | – | – | – | – |
| Oiling and greasing (corrosion protection)Surface | – | – | – | – | – |
| Cleaning (hydrocarbons, modified alcohols, aqueous media, ultrasonic; residual dirt according toSurface | – | – | – | – | – |
| Electroplated surface coatingSurface | – | – | – | – | – |
| Gas nitriding and gas nitrocarburizingHeat treatment | – | – | – | – | – |
| Nitriding of corrosion-resistant steelsHeat treatment | – | – | – | – | corrosion-resistant steels |
| Plasma nitriding and plasma nitrocarburizingHeat treatment | – | – | – | – | – |
| Expanite process (nitrocarburizing and carburizing of corrosion-resistant steels)Heat treatment | – | – | – | – | corrosion-resistant steels |
| Case hardening, hardening, deep-freezing and temperingHeat treatment | – | – | – | – | – |
| Vacuum hardeningHeat treatment | – | – | – | – | – |
| Induction hardeningHeat treatment | – | – | – | – | – |
| Hot setting & hot pre-stressingHeat treatment | – | – | – | – | – |
| Plastic injection mouldingPlastics | – | – | – | – | – |
| Joining technologyJoining | – | – | – | – | – |
| Assembly of plastic and metal modules (manual and fully automated assembly)Assembly | – | – | – | – | Plastic, Metal |
| Research & Development, Engineering (special-purpose machinery, materials engineering, prototypeEngineering | – | – | – | – | – |
| Analysis & Testing (inspection and analysis procedures)Testing | – | – | – | – | – |
13 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| CNC coiling machines | – | – | – | – | – |
| CNC winding machines | – | – | – | – | – |
| CNC and stamping-bending machines (up to 21 CNC axes, 3D bent parts) | – | – | – | – | – |
| Stamping machines (max. 250 strokes/min, 25–320 t, tool length max. 2,500 mm) | – | – | – | – | – |
| Fine-blanking presses (max. 130 strokes/min, 40–700 t, tool length max. 600 mm) | – | – | – | – | – |
| Stamping-bending machines (max. 700 strokes/min, 120 t, tool length max. 2,000 mm) | – | – | – | – | – |
| Laser welding systems (up to 8 kW, infrared and green) | – | – | – | – | – |
| Laser hardening systems (up to 2 kW) | – | – | – | – | – |
| Turning systems with flexible robotic loading | – | – | – | – | – |
| Multi-spindle machining centres (5-axis machining, up to 4 workpieces simultaneously) | – | – | – | – | – |
| Cam-controlled linear transfer machines / in-house-built multi-spindle drilling systems (up to 50 | KERN LIEBERS (in-house construction) | – | – | – | – |
| Circulating air, protective gas and vacuum furnaces (up to 1350°C) | – | – | – | – | – |
| Hot-setting furnace with presses | – | – | – | – | – |
Additional services
Quality & Certifications
Quality is assured through comprehensive inspection and analysis procedures, including 100% in-line inspections (laser, camera, force and length measurement), a materials laboratory with cross-sections and micro-hardness testing, as well as residual dirt analysis according to VDA Volume 19. The group is certified to ISO 9001 and IATF 16949 at nearly all locations; several plants hold ISO 13485, ISO 14001 and ISO 50001.
| Evidence | Schramberg | Göppingen | Villingen-Schwenningen | Schwabmünchen | Rieden |
|---|---|---|---|---|---|
| ISO 9001 | |||||
| IATF 16949 | |||||
| ISO 13485 | |||||
| ISO 14001 | |||||
| ISO 50001 |
History
Founded by Hugo Kern after his apprenticeship with a watch spring maker; production of tension springs for the domestic watch industry
- 1911
Second factory extension, doubling of production floor space; son Ernst Hugo Kern joins the company
Ernst Hugo Kern takes over management of the company, conversion into Hugo Kern KG, expansion by two new buildings until 1930
Dr. rer. pol. Kurt Steim takes over management after the death of Ernst Hugo Kern and lays the foundation for the company's present size
Reconstruction after the Second World War; due to lack of raw materials, production of garden tools, stove cranks, shoe fittings and saws
The Hugo Kern KG is designated for total dismantling by the Allies (reduced to 30%); start of production of precision stamped parts for knitting machines