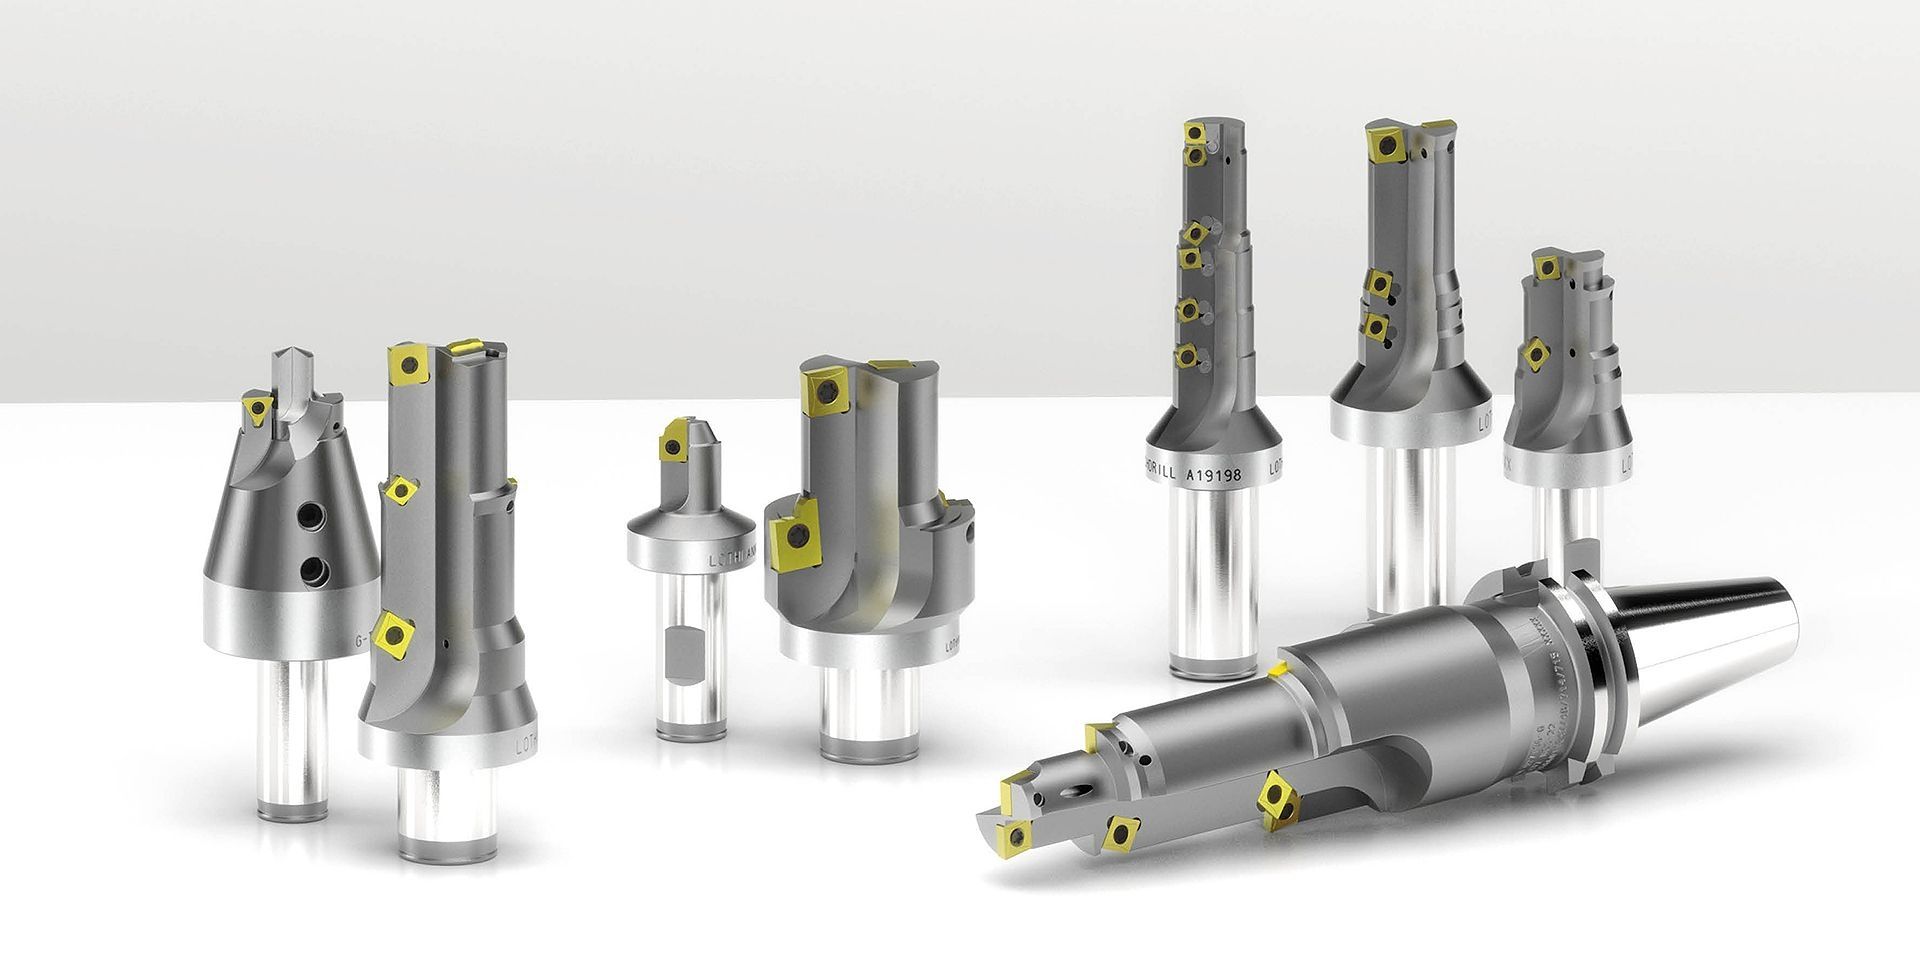
Custom special tools for drilling, countersinking, chamfering, turning and back counterboring – manufactured in Ludwigsburg.
Lothmann Werkzeugtechnik GmbH & Co. KG
Ludwigsburg (DE)New on Amplifa
About Lothmann Werkzeugtechnik
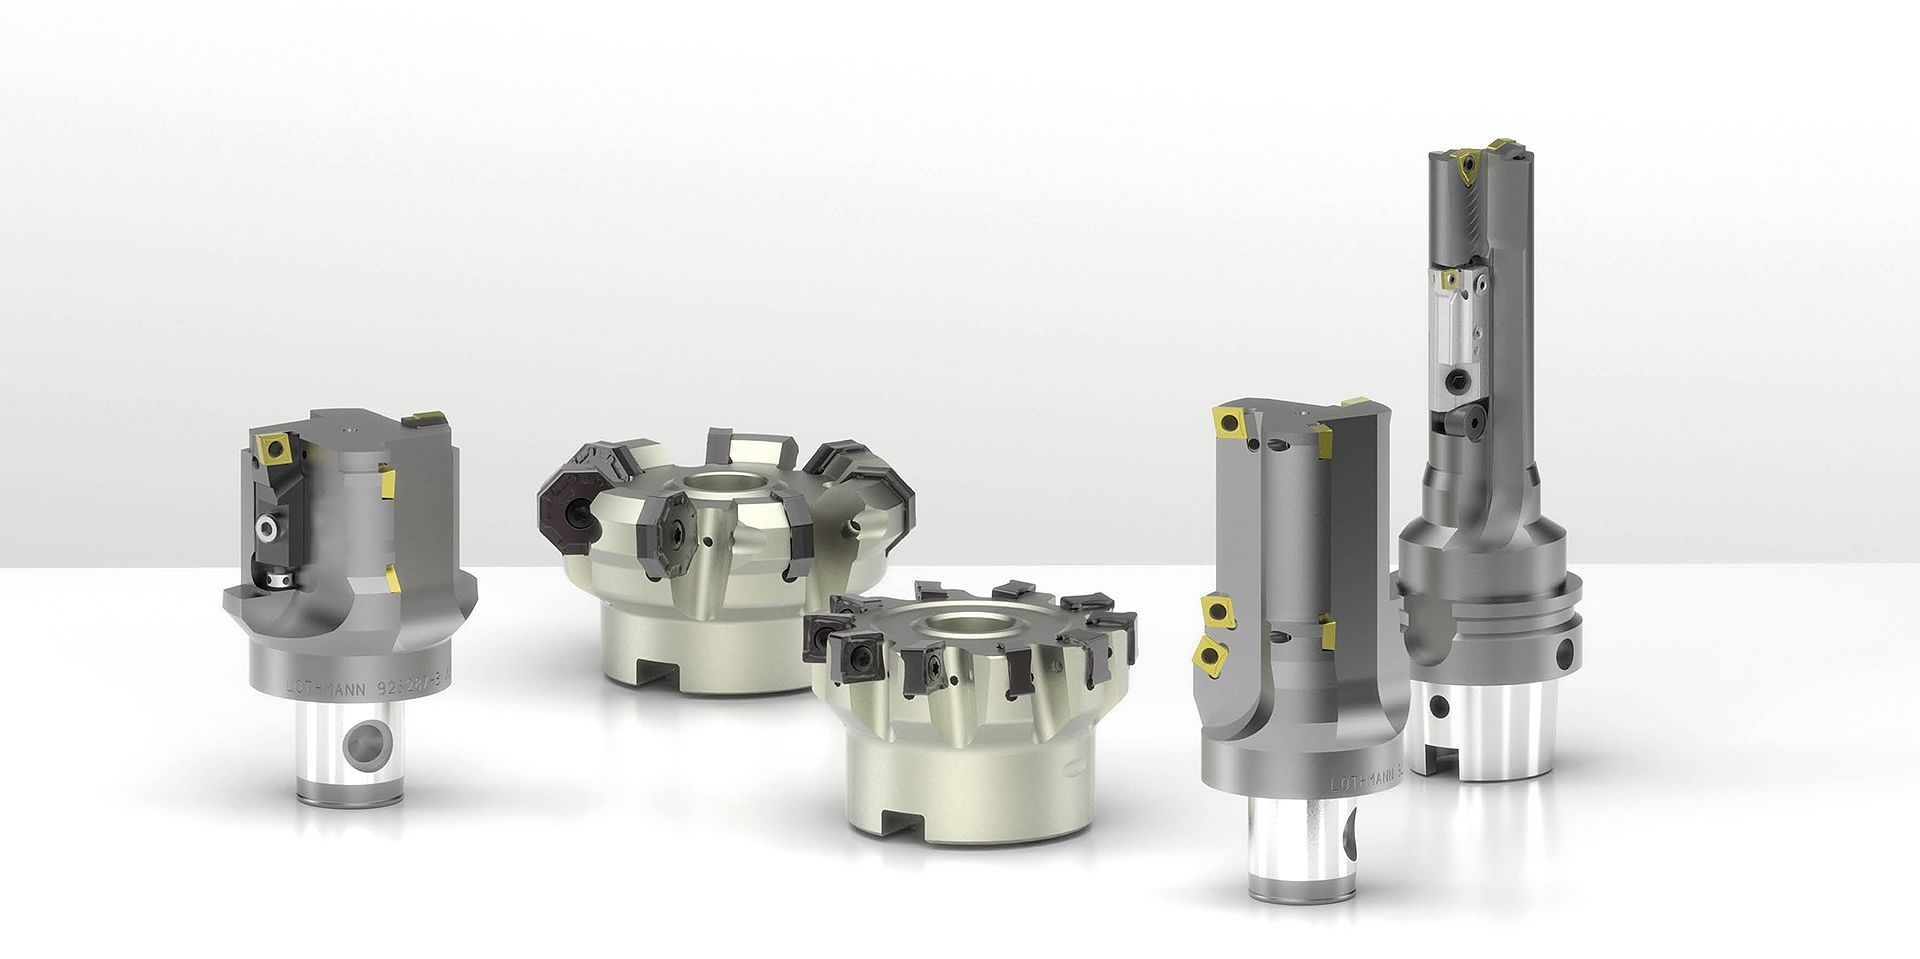
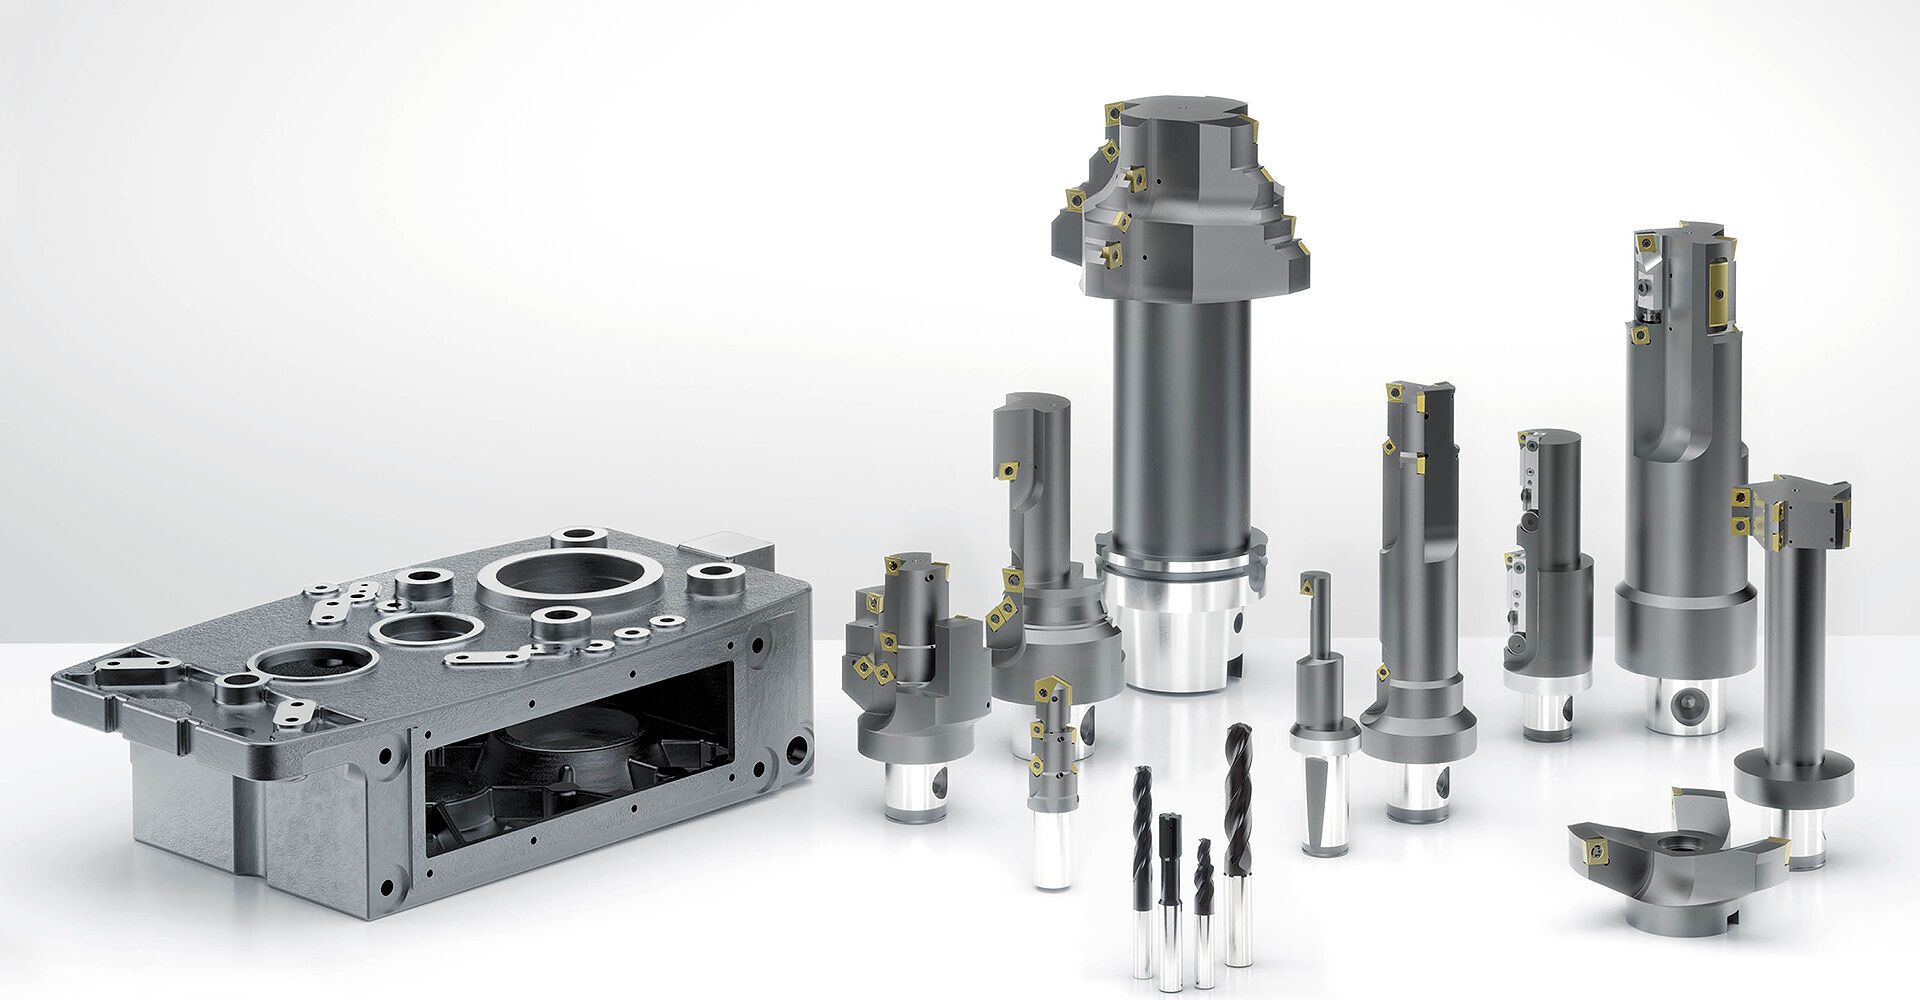
Lothmann Werkzeugtechnik GmbH & Co. KG, based in Ludwigsburg, has been developing and manufacturing custom special tools for hole machining since 1987, including step drills, step countersinks, solid drills, back counterbores, bell-type and countersinking tools. The tools are fitted with exchangeable ISO indexable inserts made of carbide, PKD or CBN and enable multiple machining operations in a single pass. Production is carried out entirely under CIM control based on a proprietary database with CAD/CAM integration, including 3D simulation of the tools before production. Milling is performed on 4- and 5-axis machining centers as well as a 5-axis turn-mill center; an NC-controlled cylindrical grinding machine is also available. Every tool undergoes a one hundred percent final inspection on fully automatic presetting devices. In addition to special tools, Lothmann distributes standard tools, tool holders and reamers from MAPAL. Customers come from hydraulics, automotive supply, mechanical engineering, pump and drive technology, and aerospace.
- Site
- Ludwigsburg
- Processes
- Manufacture of custom special tools (step drills, step countersinks, solid drills,, CNC production of special tools (turning and milling on 5-axis turn-mill center, milling of the, Cylindrical grinding (NC-controlled cylindrical grinding machine), 100% dimensional inspection / final inspection on Kelch and Mapal presetting devices, Manufacture of indexable inserts in special designs (grooving, turning, drilling, milling, Engineering/design of special tools in the CAD/CAM process (3D CAD simulation, proprietary, Distribution of standard tools: solid carbide drills (solid drilling, pilot drills, step drills,, Distribution of high-performance reamers FXR series (MAPAL), diameter range 2,800 to 20,200 mm
- Materials
- Steel (low- and high-alloy), stainless steel, Grey cast iron, Spheroidal graphite cast iron, Cast steel, Structural steel, Aluminium, Copper alloys
- Certificates
- ISO 9001:2015, VDA 6.7
- Founded
- 1987
- Employees
- 13
- Industries
- Metals industry/machining, Hydraulics, Automotive suppliers, Automotive industry, Mechanical engineering, Forklifts/intralogistics vehicles
- 01
Inquiry and consulting
- 02
Design in the CAD/CAM process (proprietary database, 3D simulation)
- 03
CAM-controlled production (turning, milling on 4-/5-axis machining centers)
- 04
Cylindrical grinding
- 05
Assembly and fitting with indexable inserts
- 06
100% final inspection
- 07
Shipping
Materials and Manufacturing Processes
Solid carbide (VHM)
Cutting material for indexable inserts and standard drilling and milling programs.
Carbide (sintered, fine-grained)
Material of the special indexable inserts, with PVD coatings for longer tool life.
Polycrystalline diamond (PCD)
For high cutting speeds when machining aluminium and non-ferrous metals.
Cubic crystalline boron nitride (CBN)
Enables the machining of hardened steel.
High-speed steel (HSS)
Available in the standard program; special tools with indexable inserts replace HSS form tools.
Steel (low- and high-alloy, heat-treatable steel)
Tool bodies and workpiece materials to be machined.
Stainless steel
Workpiece material to be machined, among others with FXR reamers.
Grey cast iron (GG25)
Typical workpiece material in gearbox and machine housings.
Spheroidal graphite cast iron (GGG40, GGG50)
Mainly hydraulic blocks and housing components.
Cast steel
Workpiece material, among others for valve housings.
Aluminium
Machinable by exchanging the indexable insert on the tool.
Copper alloys
Machinable with suitable indexable inserts.
Locations
Ludwigsburg
DEHeadquarters, production and administration
- Lot size
- Custom-made products, individual parts up to large series (tools)
- Materials
- Steel, heat-treatable steel, cast materials, stainless steel, aluminium, copper alloys, carbide, PCD, CBN
- 5-axis turn-mill center
- 4-axis machining centers
- NC-controlled cylindrical grinding machine Kellenberger KEL-VISTA
- 3 tool measuring machines
- Fully automatic measuring machine for final inspection
- Kelch and Mapal presetting devices
Components and Tools
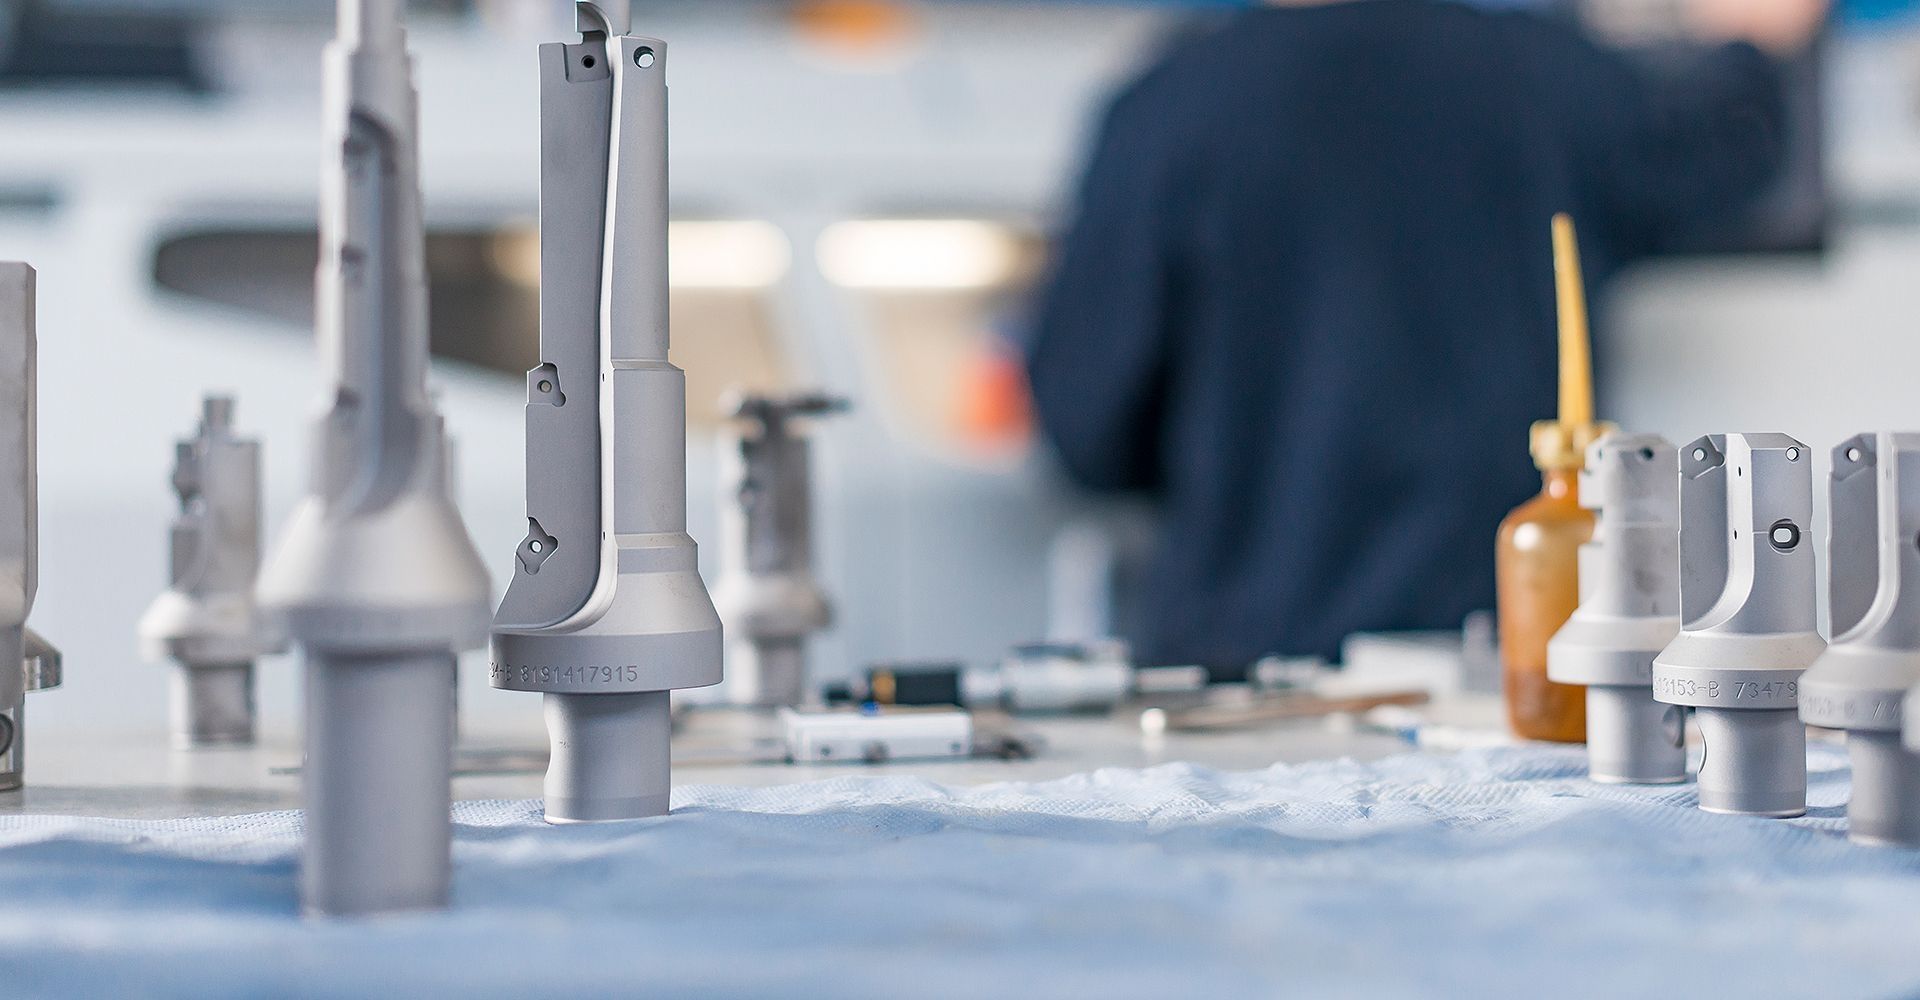
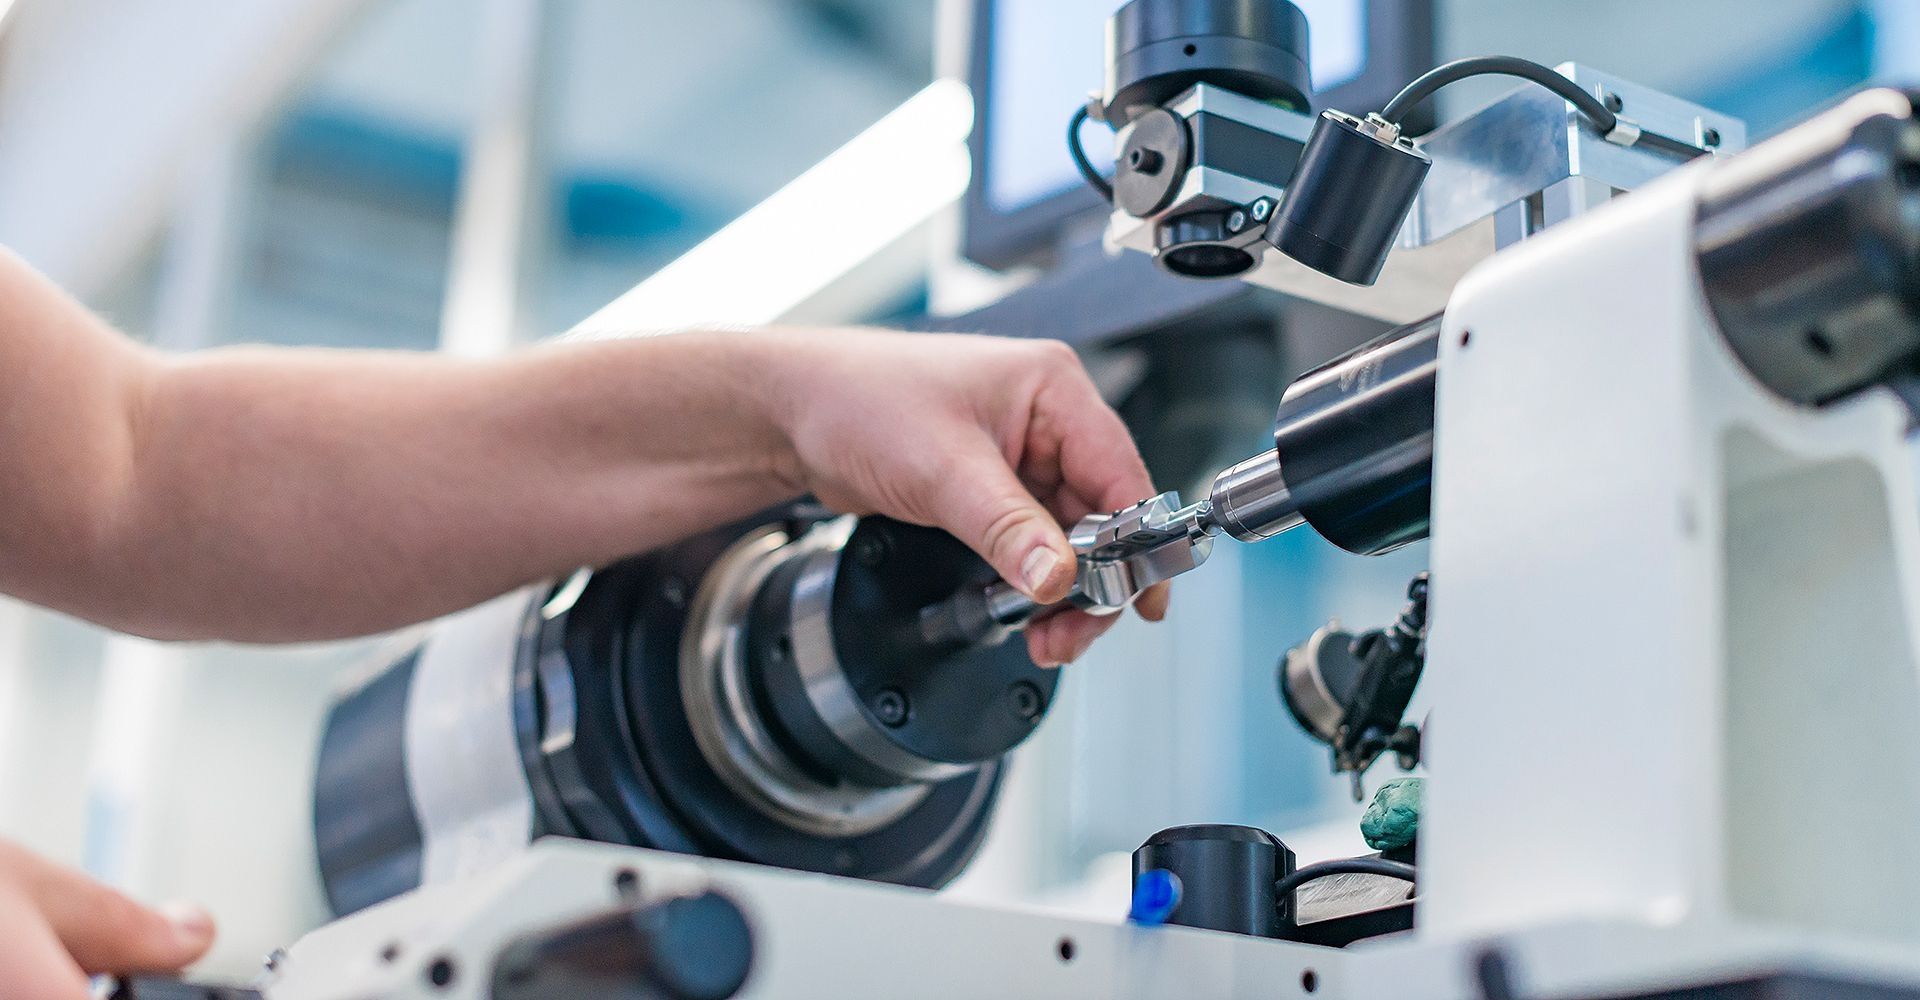
Inside the production
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Manufacture of custom special tools (step drills, step countersinks, solid drills,Machining | ±0.1 mm (sintered indexable inserts), ±0.01 mm with | – | – | – | Steel (low- and high-alloy), stainless steel, grey cast iron, spheroidal graphite cast iron, cast materials, aluminium, copper alloys, non-ferrous metals |
| CNC production of special tools (turning and milling on 5-axis turn-mill center, milling of theMachining | – | – | – | – | heat-treatable steel, carbide |
| Cylindrical grinding (NC-controlled cylindrical grinding machine)Machining | – | – | – | – | – |
| 100% dimensional inspection / final inspection on Kelch and Mapal presetting devicesTesting | – | – | – | – | – |
| Manufacture of indexable inserts in special designs (grooving, turning, drilling, millingMachining | ر0.05 mm (without adjusting elements), ر0.01 mm (with | – | – | – | carbide, PCD, CBN |
| Engineering/design of special tools in the CAD/CAM process (3D CAD simulation, proprietaryEngineering | – | – | – | – | – |
| Distribution of standard tools: solid carbide drills (solid drilling, pilot drills, step drills,Machining | ±0.003 mm and H7 (Tritan-Drill-Reamer) | – | – | – | cast materials, non-ferrous metals, steels, lightweight materials, difficult-to-machine materials |
| Distribution of high-performance reamers FXR series (MAPAL), diameter range 2,800 to 20,200 mmMachining | IT7, diameters configurable in 0.001 mm increments | 2,800 to 20,200 mm (diameter) | – | – | steel, cast iron, stainless steel |
| Distribution of tool holders/clamping technology (Hydrodehn clamping system UNIQ, MillChuck HB,Assembly | Runout accuracy < 3 μm (HTC) | – | – | – | – |
9 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| 5-axis turn-mill center | – | – | – | – | Ludwigsburg |
| 4-axis vertical center (machining center) | – | – | – | – | Ludwigsburg |
| 4-axis machining center | – | 2 | – | 1999 | Ludwigsburg |
| 5-axis machining center | – | 1 | – | 2006 | Ludwigsburg |
| NC-controlled cylindrical grinding machine | Kellenberger KEL-VISTA | 1 | – | 2016 | Ludwigsburg |
| CNC milling machine (used, start of in-house production) | Maho | 1 | – | 1989 | Ludwigsburg |
| Tool measuring machine | – | 3 | – | 2012 | Ludwigsburg |
| Fully automatic presetting devices for final inspection | Kelch / Mapal | – | – | – | Ludwigsburg |
| Fully automatic measuring machine (final inspection) | – | 1 | – | 1999 | Ludwigsburg |
Additional services
Reference customers
Quality
All special tools undergo a one hundred percent final inspection on fully automatic Kelch and Mapal presetting devices; results are documented and archived. The company is certified according to ISO 9001:2015 and VDA 6.7 and grants a functional guarantee for its tools.
| Evidence | Ludwigsburg |
|---|---|
| ISO 9001:2015 | |
| VDA 6.7 |
History
- 1987
Founded by Rainer Lothmann on 02.01.1987; initially a trading business for cutting tools, then design of special tools with carbide indexable inserts with outsourced production.
- 1989
Start of in-house tool production with a used Maho CNC milling machine in Stuttgart-Stammheim; development of a proprietary CAM system.
- 1990
First employee, relocation to Asperg, first automatic CAD drawing generation.
- 1992
First 4-axis machining center.
- 1996
Transfer of all customer and tool data into a central database with CAD/CAM integration.
- 1999
Relocation to Ludwigsburg (Teinacher Straße), two 4-axis machining centers, fully automatic measuring machine; 4 employees.
- 2000
Start of automatic 3D design; CNC programs are simulated in advance.
- 2006
First 5-axis machining center; all production operations (except heat treatment) in-house; delivery time reduced from 4 to 3 weeks.
- 2007
Relocation to the company's own building on Robert-Mayer-Straße in Ludwigsburg.
- 2012
Acquisition of three tool measuring machines; development of proprietary archiving software.
- 2013
Andreas Ott joins the company as a partner.
- 2016
Acquisition of an NC-controlled cylindrical grinding machine Kellenberger KEL-VISTA.
- 2017
Rainer Lothmann sells his company shares to MAPAL; Andreas Ott takes over management.
- 2018
Certification according to VDA 6.7.
- 2019
Certification according to ISO 9001:2015 and introduction of a QM system; 13 full- and part-time employees.