Manufacturing and repair of machine components by thermal spraying, machining and coating
M&P Thermische Spritz- und Oberflächentechnik GmbH
Kirchhundem · Hagen im BremischenNew on Amplifa
About us
M&P Thermische Spritz- und Oberflächentechnik GmbH was founded in 1994 in Hagen im Bremischen and, with its headquarters in Kirchhundem, operates as a manufacturing partner for mechanical engineering companies. The company manufactures new parts and machine assemblies and repairs worn machine components through thermal spraying and mechanical machining. Spraying processes offered include wire, powder and rod flame spraying, high-velocity oxy-fuel spraying (HVOF) and atmospheric plasma spraying; these are complemented by hardfacing welding of hard materials and electroplated coatings. Mechanical machining includes CNC turning, turning on a facing lathe up to Ø 1100 x 9000 mm, 5-axis milling, cylindrical external and internal grinding, cross and surface grinding as well as lapping, belt finishing and superfinishing. With more than 100 coating materials, including ceramics such as chromium oxide and aluminum oxide as well as the hard material WcCoCr, wear-protection, corrosion-protection and anti-friction coatings with thicknesses of 0.01 to 8 mm are applied. Customers come, among others, from machine tool manufacturing, plant engineering, turbine and compressor manufacturing, rolling mill technology and shipping; acceptance per Inspection Certificate 3.2 by ship classification societies is possible.
- Site
- Kirchhundem
- Processes
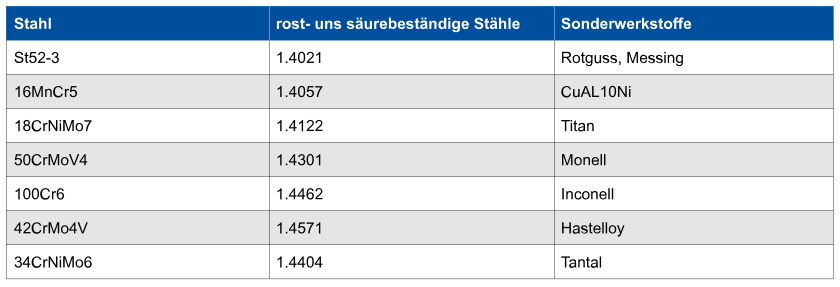
- Thermal spraying (metal spraying technology), Wire flame spraying (WFS), Powder flame spraying (PFS), High-velocity oxy-fuel spraying (HVOF), Rod flame spraying (StFL), Plasma spraying (APS), Hardfacing welding of hard materials, Mechanical manufacturing / CNC turning
- Materials
- 34CrNiMo6V, 42CrMoV4, 1.4462, 1.4571, CuAl10Ni (aluminum bronze), White metal, Molybdenum, Zinc
- Certificates
- DIN EN ISO 9001, DIN EN ISO 14922:2022-02 QAL-S (WFS, PFS, HVOF, APS), GTS-QM guideline GTSPSA 003 (personnel and procedure qualification), Bureau Veritas Mode II Recognition (thermal spraying and mechanical engineering), ISO 9001 (DVS certification), GTS-QM guideline GTSPSA 003, Bureau Veritas Mode II Recognition
- Founded
- 1994
- Industries
- Mechanical engineering, Machine tool manufacturing, Plant engineering, Turbine and compressor manufacturing, Rolling mill technology, Shipbuilding/ship classification
- 01
Design and production planning
- 02
Mechanical manufacturing (turning, milling)
- 03
Thermal spraying / hardfacing welding / electroplated coatings
- 04
Grinding, lapping, superfinishing
- 05
Induction hardening
- 06
Production-accompanied Inspection Certificate 3.2 (on request)
- 07
Shipping and logistics
Locations
Kirchhundem
DEHeadquarters, management, manufacturing, quality, southern sales
- Part weight / size
- Shafts up to Ø 1100 x 9000 mm · Coating thicknesses 0.01–8
- Lot size
- Single parts and series
- Materials
- Steel, stainless steel, copper alloys, ceramics, hard materials
- 5-axis milling machine (X 3600/3030 mm, Y 900 mm, rotary table Ø 900 mm)
- Facing lathe up to Ø 1100 x 9000 mm
- CNC lathes up to Ø 1000 x 3000 mm
- Cylindrical grinding machines up to Ø 2200 x 600 mm
- Internal grinding machines up to Ø 2100 x 600 mm
- Systems for WFS, PFS, HVOF, APS, StFL
Hagen im Bremischen
DENorthern site (plant management), founding site 1994
Components and Applications
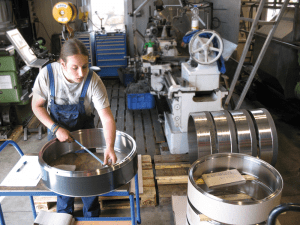
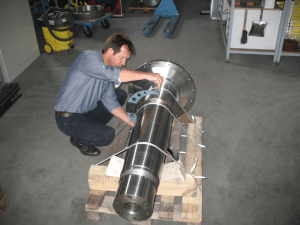
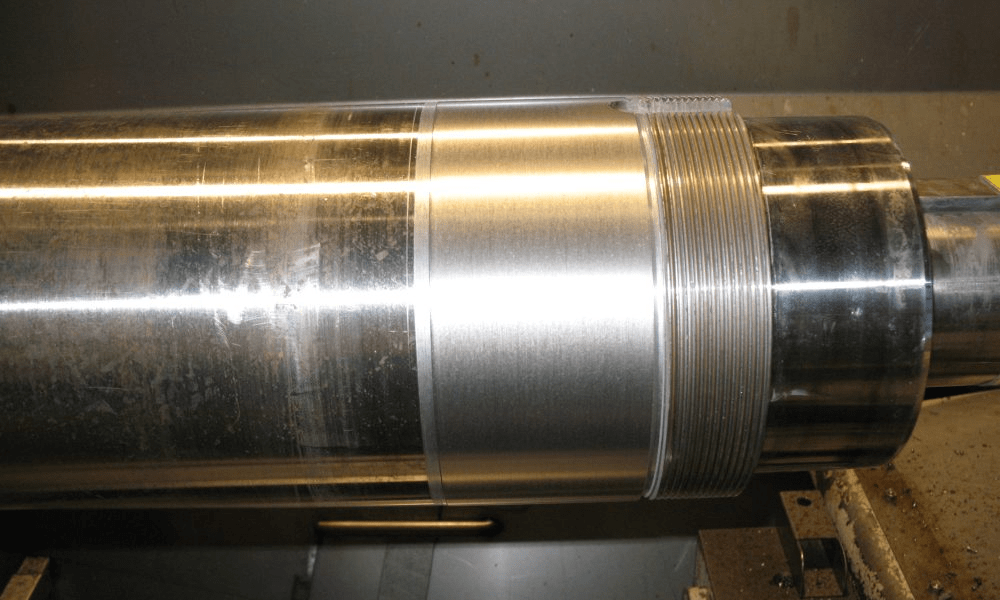
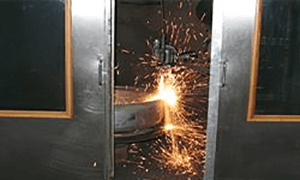
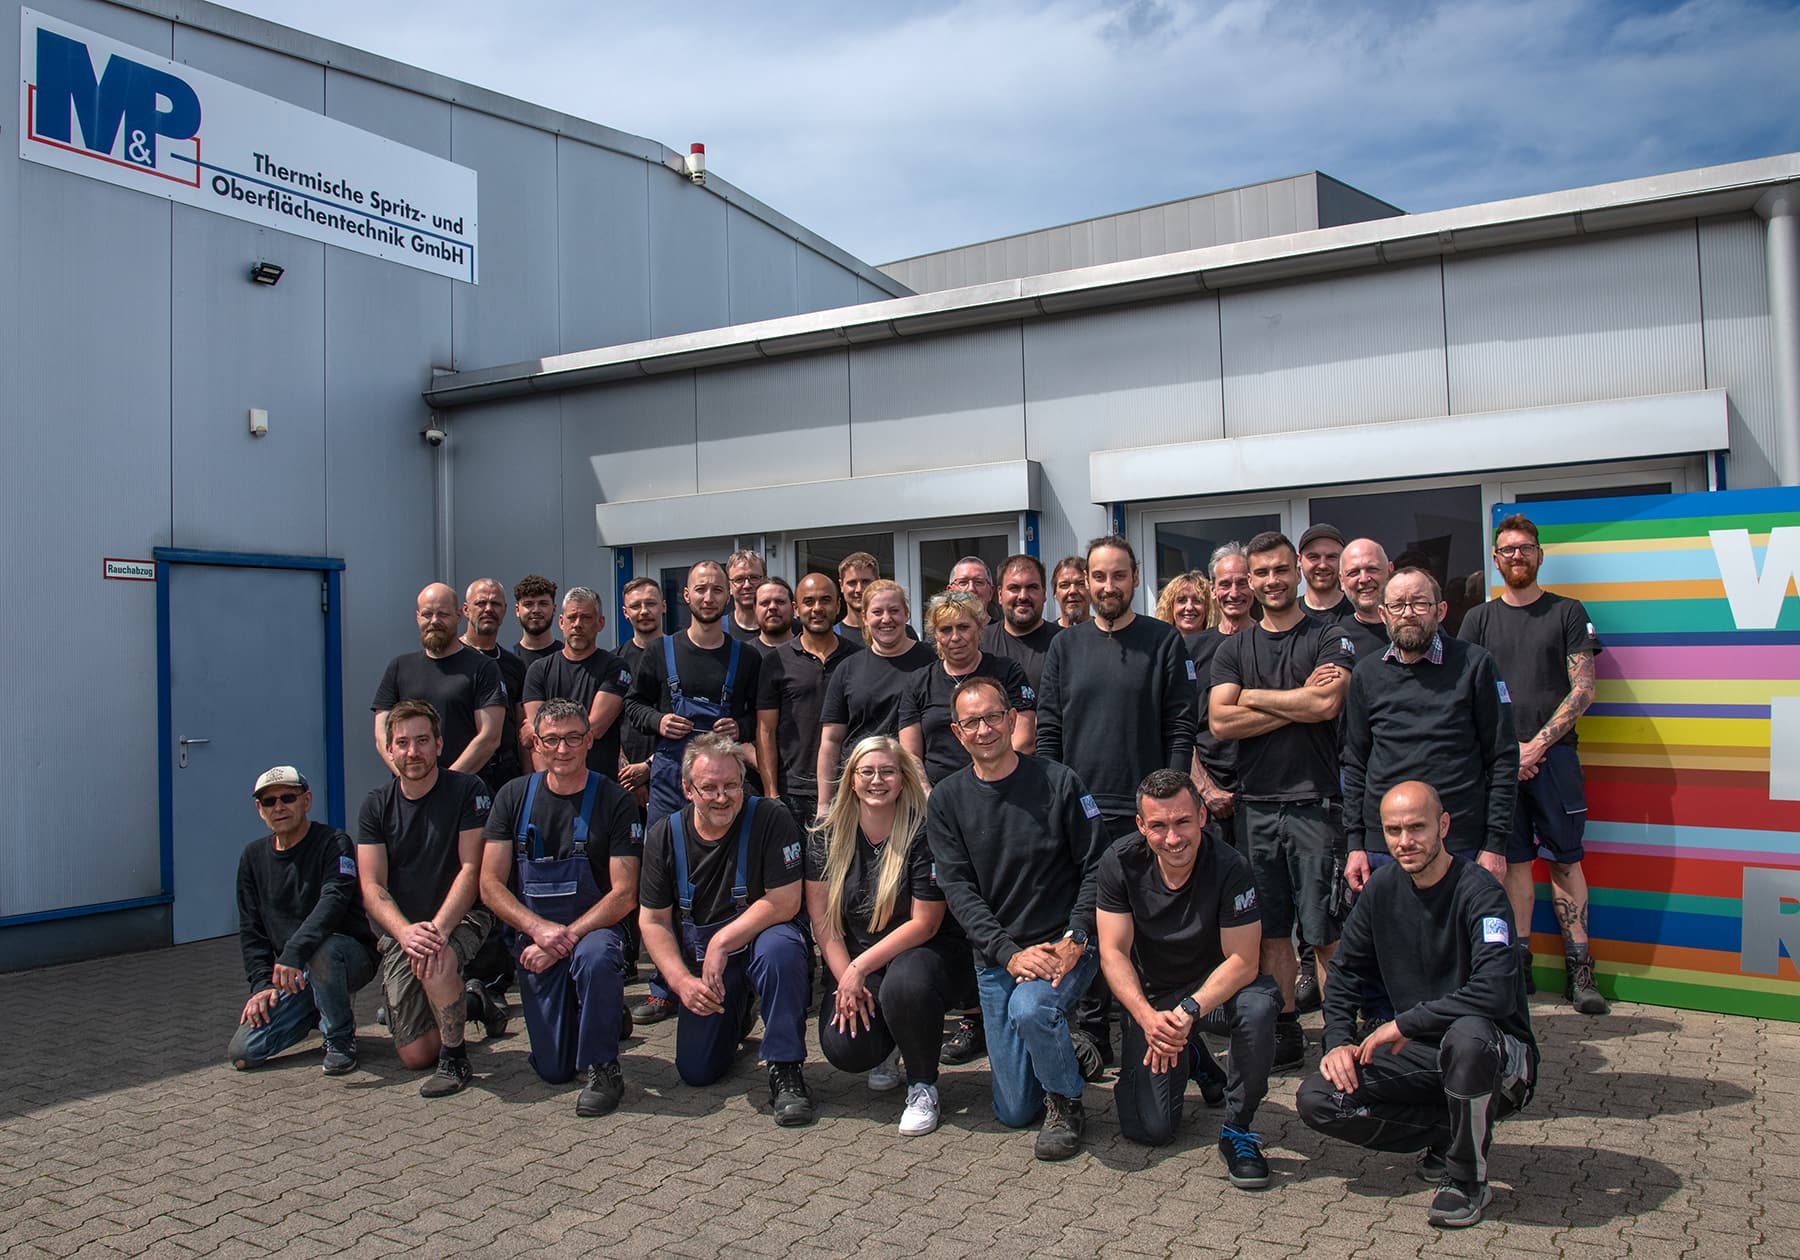
Inside the production
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Thermal spraying (metal spraying technology)Surface | – | – | – | – | Metals, Ceramics, Hard materials, more than 100 coating materials |
| Wire flame spraying (WFS)Surface | – | – | – | – | – |
| Powder flame spraying (PFS)Surface | – | – | – | – | – |
| High-velocity oxy-fuel spraying (HVOF)Surface | – | – | – | – | WcCoCr |
| Rod flame spraying (StFL)Surface | – | – | – | – | – |
| Plasma spraying (APS)Surface | – | – | – | – | Chromium oxide Cr2O3, Aluminum oxide |
| Hardfacing welding of hard materialsJoining | – | – | – | – | Hard materials |
| Mechanical manufacturing / CNC turningMachining | – | 2700 mm (shafts up to 9000 mm overall | – | – | 34CrNiMo6V, 42CrMoV4, 1.4462, 1.4571, CuAl10Ni |
| 5-axis millingMachining | – | 3600 mm (X vertical) × 900 mm (Y axis) × 1005 mm (Z axis horizontal) | – | – | – |
| Cylindrical external grindingMachining | Runout and axial deviation less than 0.01 mm | 2000 mm × Ø 2200 mm | – | – | – |
| Cylindrical internal grindingMachining | – | 600 mm × Ø 2100 mm | – | – | – |
| Cross grindingMachining | – | – | – | – | – |
| Surface grindingMachining | – | – | – | – | – |
| Lapping, belt finishing, superfinishingMachining | – | – | – | – | – |
| Induction hardeningHeat treatment | – | – | – | – | 34CrNiMo6V |
| Electroplated coatingSurface | – | – | – | – | – |
| Repair service for worn machine componentsSurface | – | – | – | – | Steel, Ceramics, Hard materials, White metal |
| New-part manufacturing of complete machine componentsAssembly | – | – | – | – | – |
| Machining / Non-Destructive Testing (BV-certified)Testing | – | – | – | – | – |
5 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| 5-axis milling machine | – | – | X 3600/3030 mm (V/H), Y 900 mm, Z 900/1005 mm (V/H), rotary table Ø 900 mm, collision circle Ø 1250 | – | – |
| Facing lathe | – | – | up to Ø 1100 x 9000 mm, Ø 1600 x 2700 mm, Ø 630 x 3560 mm, Ø 560 x 4200 mm | – | – |
| CNC lathe | – | – | Ø 1000 x 1000 mm, Ø 300 x 2000 mm, Ø 420 x 3000 mm | – | – |
| Cylindrical external grinding machine | – | – | Ø 900 x 750 mm to Ø 2200 x 600 mm | – | – |
| Internal grinding machine | – | – | Ø 1400 x 600 mm to Ø 2100 x 600 mm | – | – |
Additional services
Reference customers
Quality
All operations, methods and processes are continuously checked for correctness, process capability and sustainability. The quality management system is regularly audited by independent experts; the GTS and ship classification requirements include procedure and personnel qualification tests that exceed the requirements of DIN ISO 9001.
| Evidence | Kirchhundem |
|---|---|
| ISO 9001 (DVS certification) | |
| DIN EN ISO 14922:2022-02 QAL-S (WFS, PFS, HVOF, APS) | |
| GTS-QM guideline GTSPSA 003 | |
| Bureau Veritas Mode II Recognition |
History
- 1994
Founded in Hagen im Bremischen
- 2004
Commissioning of the Kirchhundem site
- 2025
Approval by Bureau Veritas for thermal spraying and mechanical engineering (valid until 05.10.2029)
- 2026
Certification according to DIN EN ISO 14922:2022-02 QAL-S for WFS, PFS, HVOF and APS
- 2026
Certification according to GTS-QM guideline GTSPSA 003 with personnel and procedure qualification
- 2026
Certification of the quality management system according to DIN EN ISO 9001 by the DVS