Manufactures special machines for leak testing, assembly technology and automation – from single machines to complete production lines.
Paul Köster GmbH
Medebach · SuzhouNew on Amplifa
About us
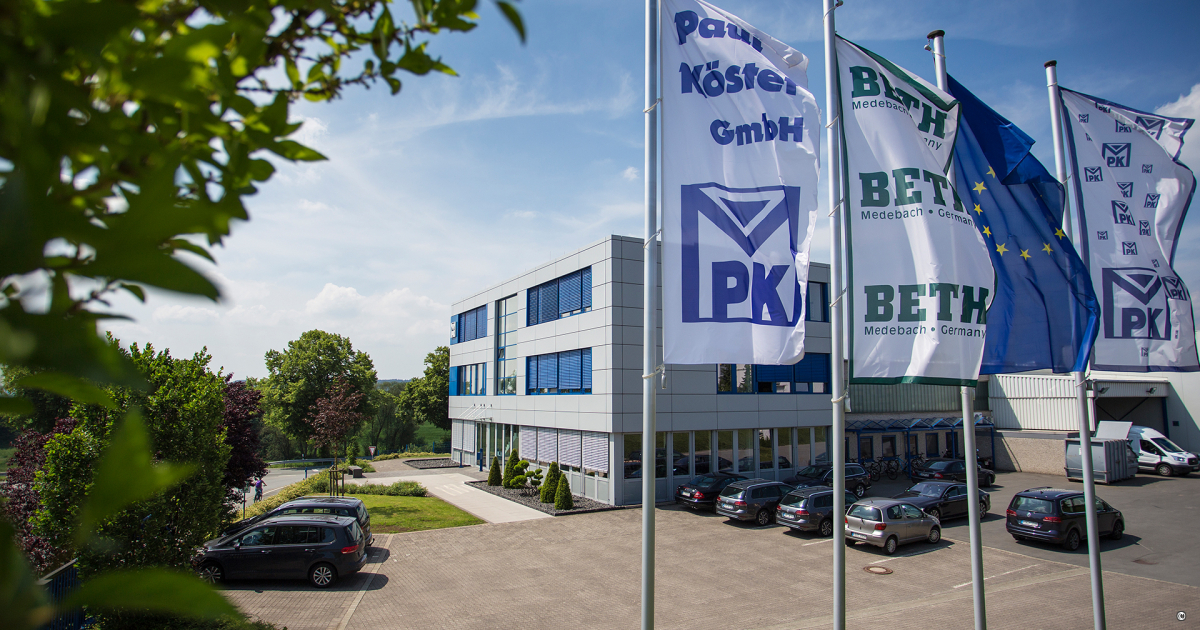
Paul Köster GmbH is a family-owned company from Medebach in the Sauerland region and has been active in mechanical engineering since 1907. The company manufactures complex special machines and turn-key solutions in its core areas of leak testing, assembly technology, industrial automation and AI-based visual inspection. Its range extends from single machines to complete, linked production lines with multiple robots. The value chain covers design, in-house software development, mechanical and electrical manufacturing with high in-house production depth, installation, commissioning as well as service and spare parts supply. Reference customers come from the automotive industry, medical technology, industrial valves, data centers, defense and security technology as well as energy and battery applications, including AUDI, GF Casting Solutions and ABB. Around 300 employees work at the headquarters in Medebach; with its subsidiary Suzhou LK Special Automation Equipments Ltd., the company is also represented in China.
- Site
- Medebach
- Processes
- Leak testing (mass flow method / air testing method), Leak testing of XXL battery housings (air, low test pressures), Leak localization using the helium sniffer method (gas testing method), Leak testing using the pressure difference method (oil chamber), Cylinder head assembly (16 robots, cycle time <2.88 min, 18 individual operations), Automated assembly & leak testing of cylinder heads (nitrogen cooling, cycle time <78 sec.), Joining with inductive heating (stator housings, housing heated to over 200°C), Joining with inductive heating (cooling bodies, bushings)
- Materials
- Aluminum (battery housings, implied), Aluminum die casting (housings AUDI e-mobility, GF Casting Solutions), Steel, Aluminum, Aluminum die casting, Inductive heating, Leak testing (mass flow / pressure difference method), Helium sniffer method
- Certificates
- DIN EN ISO 9001, DIN EN 1090, DIN ISO 3834
- Founded
- 1907
- Employees
- 300
- Industries
- Automotive, Medical technology, Industrial valves, Data centers, Industrial module construction, Defense and security technology
- 01
Design (mechanical & electrical)
- 02
Software development (own software department)
- 03
Manufacturing with high in-house production depth
- 04
Assembly and system construction
- 05
Installation and commissioning at the customer's site
- 06
Service and spare parts supply
Materials & Processes
Steel
Conformity certificates according to DIN EN 1090 and DIN ISO 3834 for load-bearing steel components in plant engineering.
Aluminum
Load-bearing aluminum components according to DIN EN 1090; aluminum die-cast housings, e.g. from e-mobility, as testing and assembly objects.
Aluminum die casting
Processed cast components (e.g. e-mobility housings, battery housings) in assembly and leak testing systems.
Inductive heating
Joining processes with housings inductively heated to over 200 °C (e.g. stator housings of electric motors).
Leak testing (mass flow / pressure difference method)
Air-based testing methods for component validation, also for XXL components such as battery housings.
Helium sniffer method
Gas-based testing method for leak localization on components found to be defective.
Visual Inspection
AI-based final inspection and camera position control in production systems.
Locations
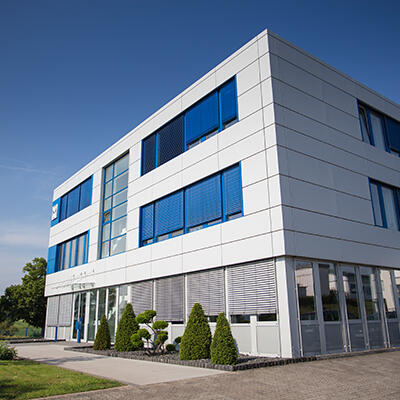
Medebach
DEHeadquarters, engineering, manufacturing and plant construction
- Materials
- Steel, aluminum
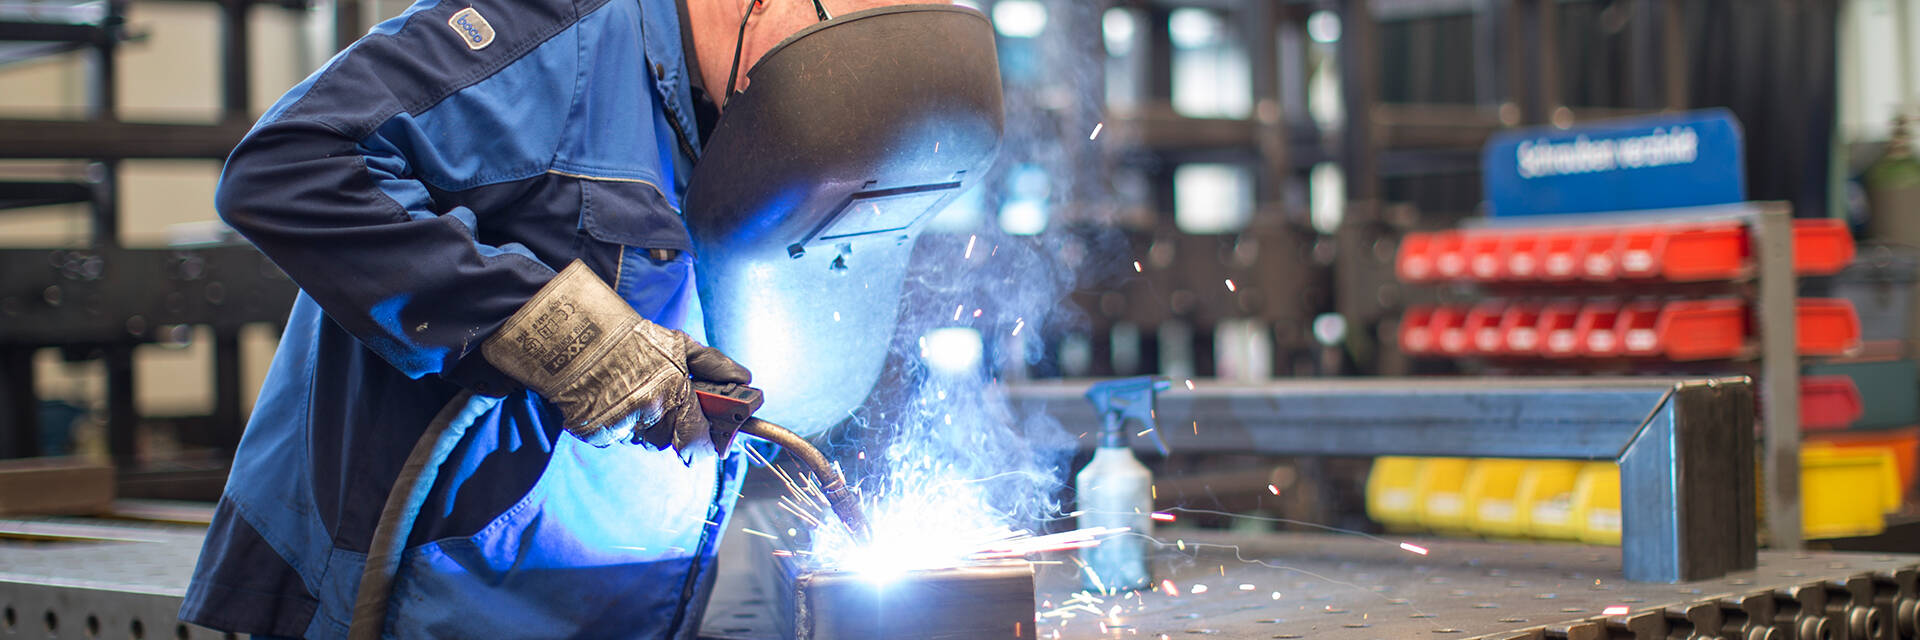
- Welding fabrication (DIN EN 1090 / ISO 3834)
- Design and software department
- Manufacturing with high in-house production depth
- Photovoltaic systems Plant 1 and Plant 3
Suzhou
CNSubsidiary Suzhou LK Special Automation Equipments Ltd., local support in the Asian region
Components & Systems
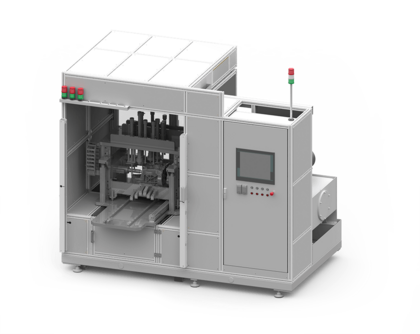
Inside the production
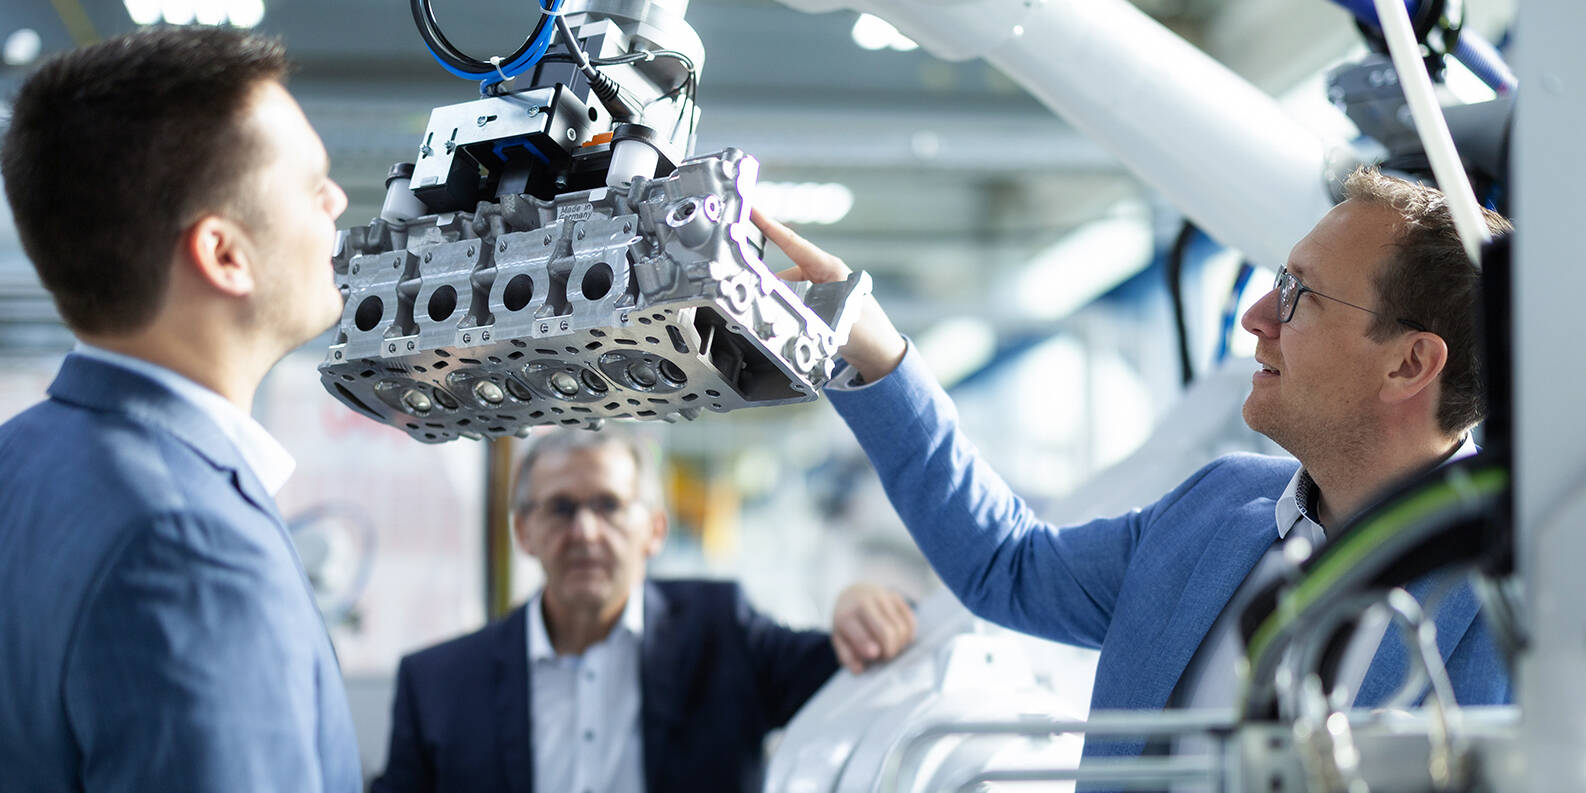
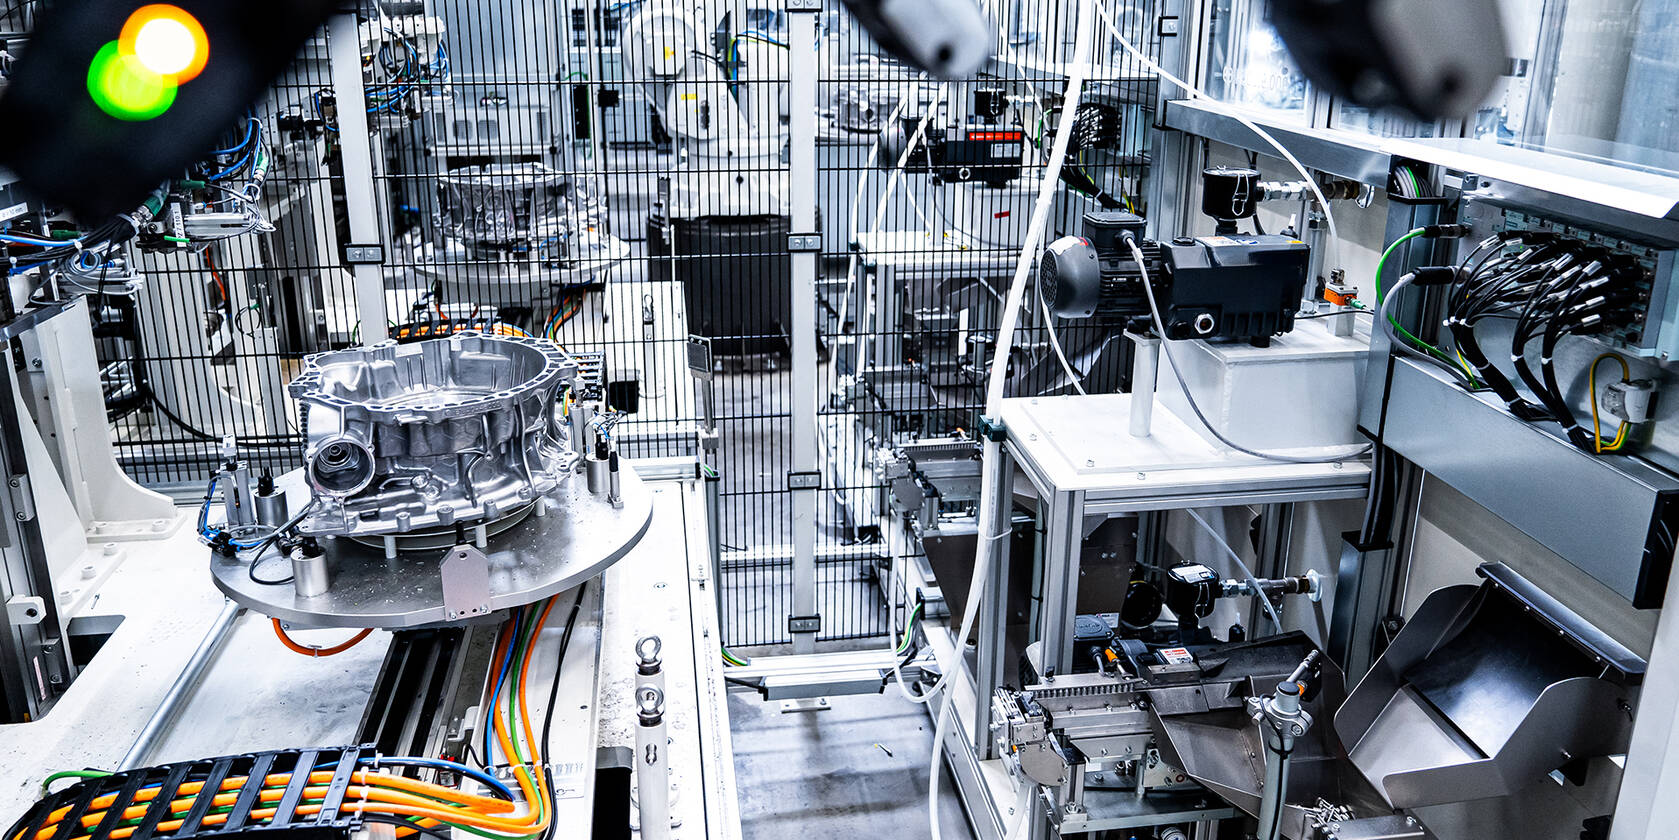
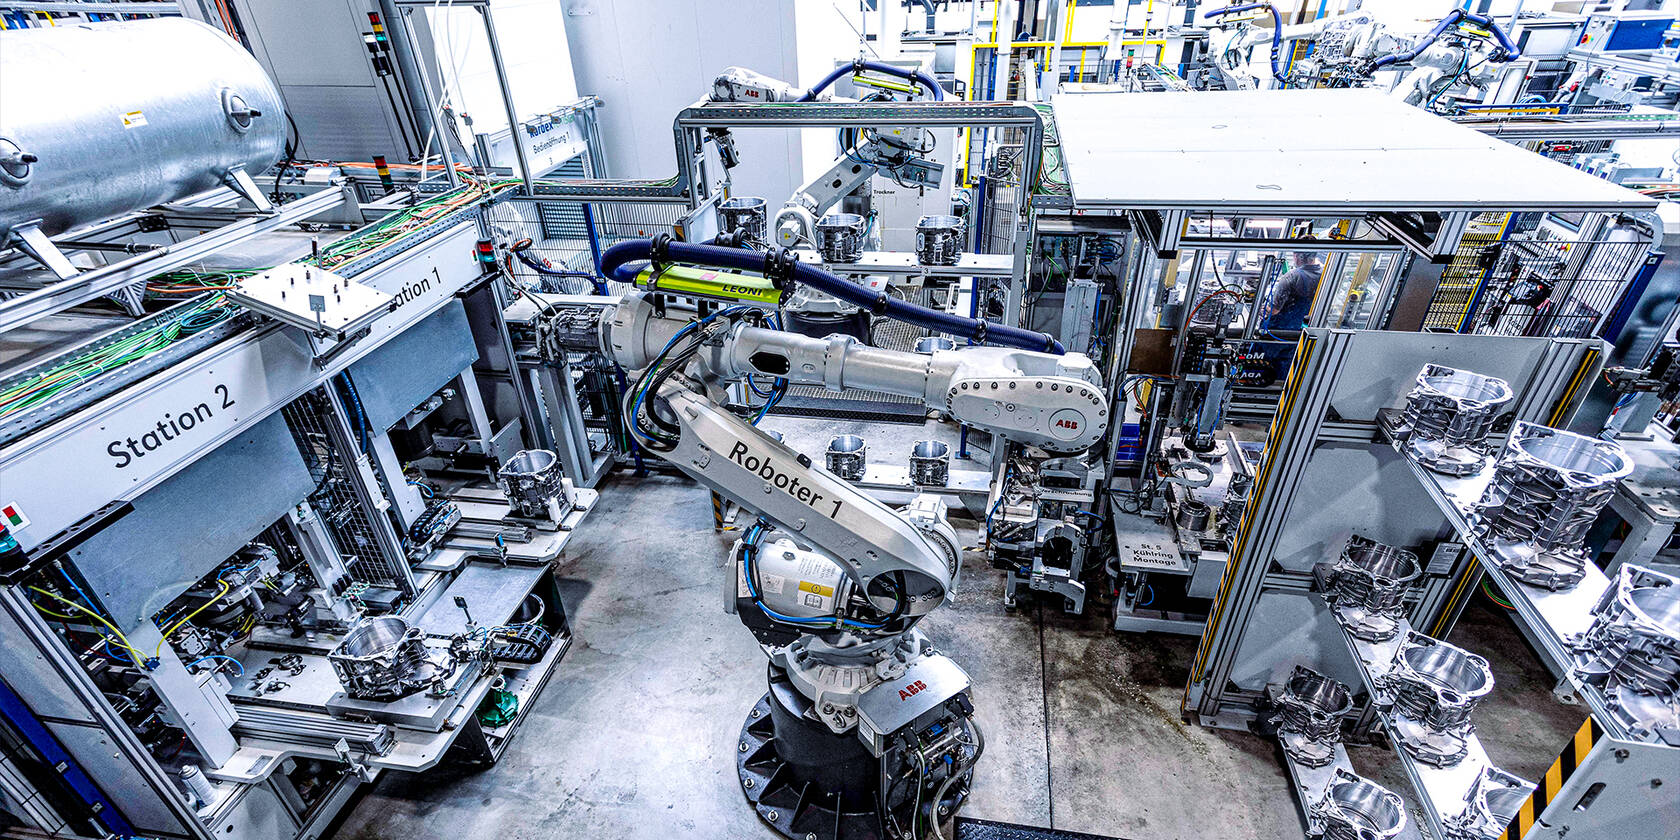
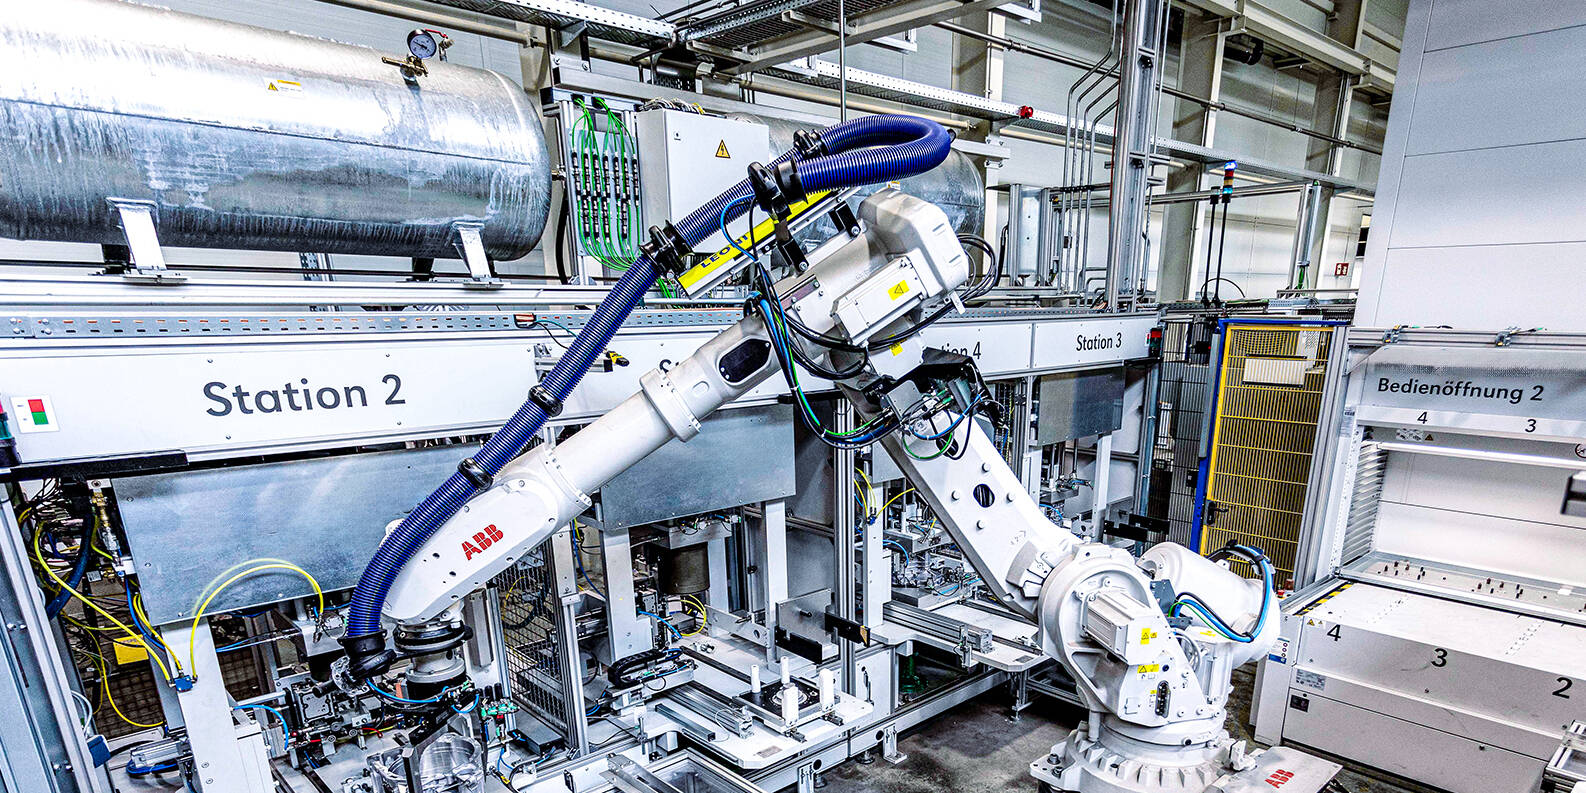
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Leak testing (mass flow method / air testing method)Testing | – | – | – | – | – |
| Leak testing of XXL battery housings (air, low test pressures)Testing | – | ca. 6,5 m (sealing contour) | – | – | – |
| Leak localization using the helium sniffer method (gas testing method)Testing | – | – | – | – | – |
| Leak testing using the pressure difference method (oil chamber)Testing | – | – | – | – | – |
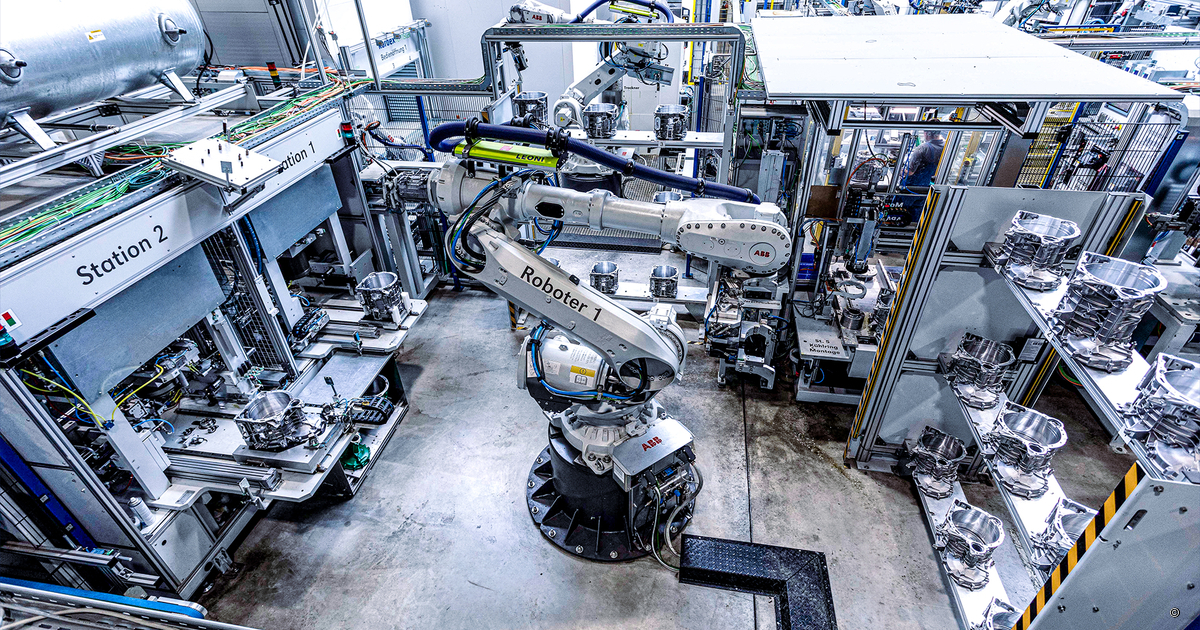
| Cylinder head assembly (16 robots, cycle time <2.88 min, 18 individual operations)Assembly | – | ca. 25 m (system length) | – | – | – |
| Automated assembly & leak testing of cylinder heads (nitrogen cooling, cycle time <78 sec.)Assembly | – | – | – | – | Valve seat rings, Valve guides, Threaded bushings, Closure covers, Injector sleeves |
| Joining with inductive heating (stator housings, housing heated to over 200°C)Joining | – | – | – | – | – |
| Joining with inductive heating (cooling bodies, bushings)Joining | – | – | – | – | – |
| Automated assembly system for e-mobility housings (14 robots, 16 assemblies, 8 test stations)Assembly | – | – | – | – | E-mobility housing, Cooling body, Bushings, Sheet metal cover, Cooling ring, Closure plug |
| Sealant application (fully automated) incl. inspection using 3D camera/3D scannerJoining | – | – | – | – | – |
| Cleaning (pre-cleaning of coolant-contaminated parts, wash cell, drying)Surface | – | – | – | – | – |
| Laser marking / laser labelingSurface | – | – | – | – | – |
| Visual inspection / camera position control / visual inspection (AI-based)Testing | – | – | – | – | – |
| Special machine engineering (turn-key solutions, single machines to complete production lines)Engineering | – | – | – | – | – |
| Assembly technology (automated assembly systems)Assembly | – | – | – | – | – |
| Industrial automation / automation systemsEngineering | – | – | – | – | – |
| Screwing with parameter monitoringJoining | – | – | – | – | – |
| Pressing-in/hammering-in of components (valves, nitrogen-cooled at -195,8 °C)Joining | – | – | – | – | Valve seat rings, Valve guides |
| Impregnation (in automated production line for QA)Surface | – | – | – | – | – |
| Component handling with handling robots (incl. vacuum grippers)Engineering | – | – | approx. 30 kg (component) | – | – |
| Screwing/sealant application: fully automated application of individual adhesive beadsJoining | – | – | – | – | – |
7 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| Assembly system for electric motors (inductive heating, joining axis) | – | 1 | – | – | at the customer's site (hybrid/e-mobility) |
| Production system for leak testing of battery housings (XXL) | – | 1 | Component size according to vehicle platform | – | at the customer's site |
| Automated production system for cylinder head assembly (16 robots, approx. 25 m long) | – | 1 | approx. 25 m system length | – | at the customer's site (automotive supplier in southern Germany) |
| Automated assembly system for e-mobility housings (14 robots, 6 cells) | – | 1 | Gantry with 3 robots and working range of 50 meters | – | GF Casting Solutions, customer's production hall |
| Automated assembly & leak testing system for cylinder heads (5 robots, liquid nitrogen tank) | – | 1 | – | – | at the customer's site (commercial vehicle manufacturer) |
| Automated assembly machine for truck wheel hubs | – | 1 | – | – | at the customer's site |
| Automated production line for quality assurance (machining, assembly, leak testing, | – | 3 | – | – | at the customer's site |
Additional services
Reference customers
Quality
Since April 2003 the company has been certified by TÜV Süd according to DIN EN ISO 9001; in addition, certificates according to DIN EN 1090 and DIN ISO 3834 exist for load-bearing steel and aluminum components. Skilled personnel, seamless documentation and integrated measuring and testing systems (including DIATEST measuring systems, camera and AI-based visual inspection) ensure process quality.
| Evidence | Medebach |
|---|---|
| DIN EN ISO 9001 | |
| DIN EN 1090 | |
| DIN ISO 3834 |
History
- 1907
Foundation of the family-owned company in Medebach
- 1991
The brothers Paul, Friedrich and Ernst Köster take over the management of the traditional company
- 2003
First certification according to DIN EN ISO 9001 by TÜV Süd
- 2025
Generational change in the management; restructuring to secure business succession