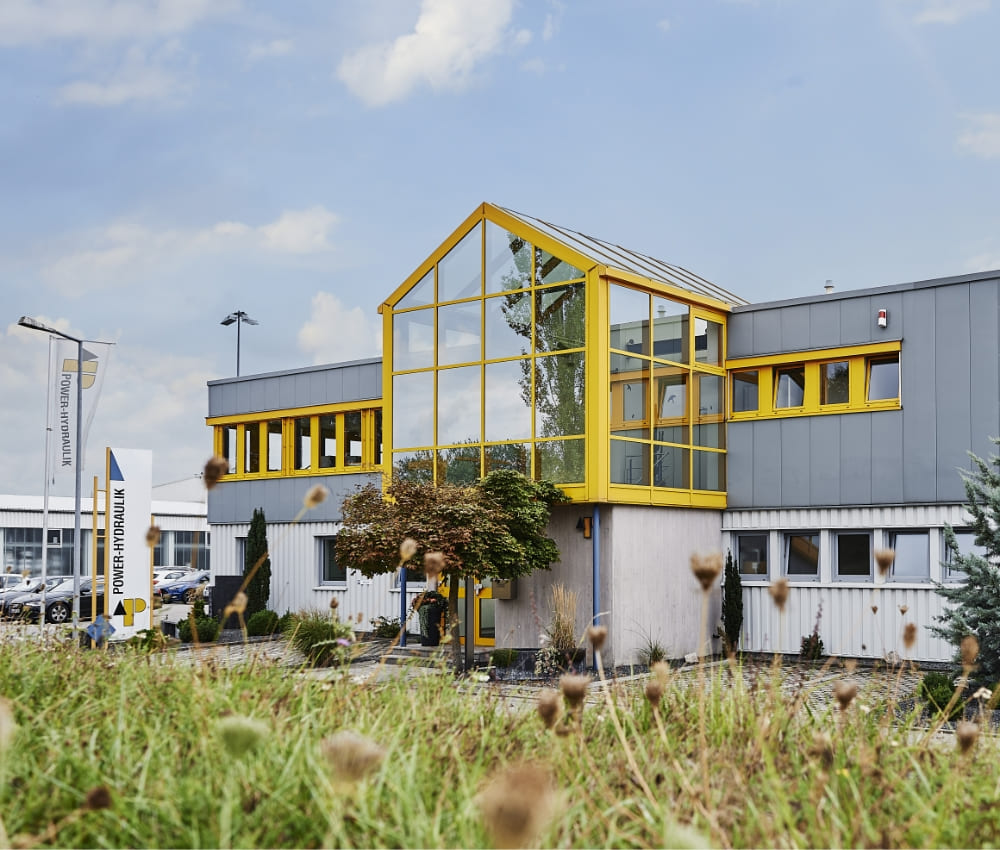
Design and CNC manufacturing of custom hydraulic control blocks and complete systems up to 1 tonne in weight.
POWER-HYDRAULIK GmbH
Sulz am Neckar (72172) · GermanyNew on Amplifa
About POWER-HYDRAULIK
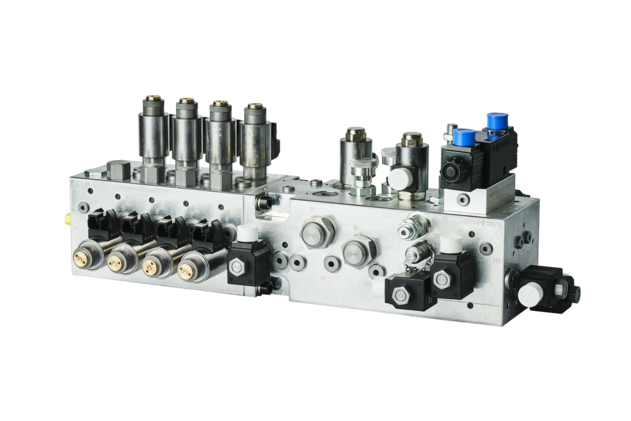
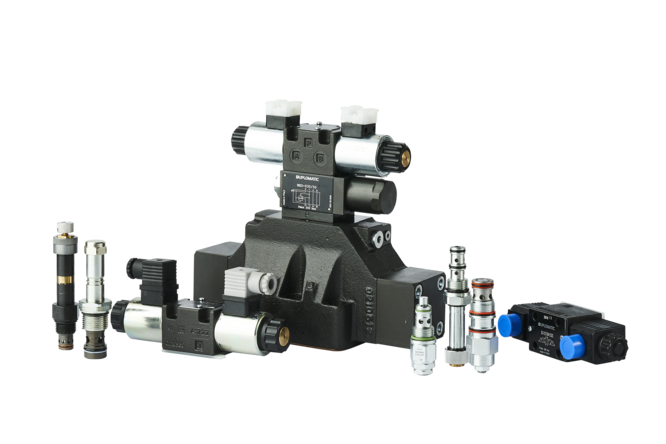
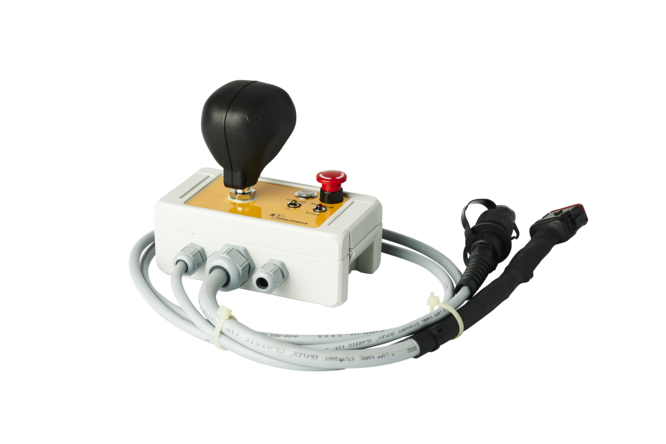
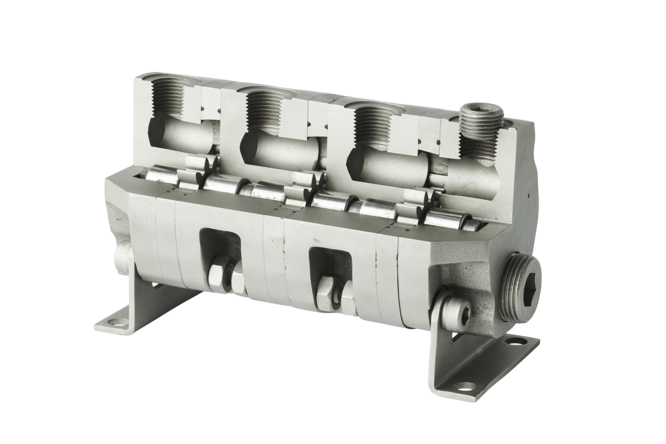
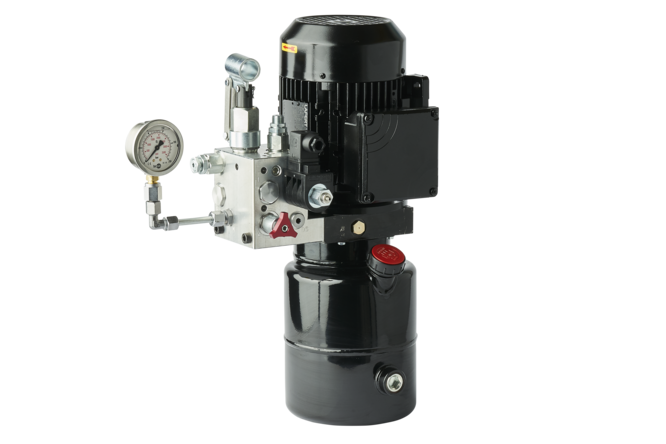
POWER-HYDRAULIK GmbH is a family-run mid-sized company founded in 1977 in Sulz am Neckar, specialising in the design and manufacture of hydraulic control blocks, prototypes and complete systems. The product range includes complex control blocks from the size of a cigarette pack up to 1,000 mm edge length and 1 tonne in weight, made from aluminium, cast iron and steel, as well as complementary valve technology, electronic controls with joysticks, gear flow dividers and small AC/DC power units. The value chain extends from CAD design (Top Solid V6, data import as Inventor IPT, STEP, DXF) via CAM programming and CNC manufacturing on seven Heller 4-axis machining centres, a Hermle 3-axis machine for prototypes and a Hermle 5-axis machine with automation, through to deep-hole drilling (6 x D to 30 x D, up to 800 mm depth, 75 mm diameter, Rz < 4). This is followed by manual and thermal deburring, cleaning including high-pressure lances, finishing, assembly and function testing. Customers come from agricultural machinery, construction machinery, municipal technology, conveying technology and stationary machinery — from car lifting platforms to tunnel boring machines. The company has been certified to DIN EN ISO 9001 since 1997.
- Site
- Sulz am Neckar
- Processes
- CNC machining (cutting) of control blocks, single-part/prototype/series production, Deep-hole drilling (6 x D to 30 x D), Deep-hole drilling on Heller machining centres, Manual deburring, Thermal deburring, Machine washing and drying of the control blocks after each setup (including high-pressure lances), Surface treatment/finishing: painting, anodising, galvanising, nitro-carburising, oxidising, CAD design of custom control blocks (Top Solid V6, data import Inventor IPT, STEP, DXF)
- Materials
- Aluminium, Cast iron, Steel, Deep-hole drilling, CNC machining, Thermal deburring, Surface finishing, Gear flow divider
- Certificates
- DIN EN ISO 9001
- Founded
- 1977
- Industries
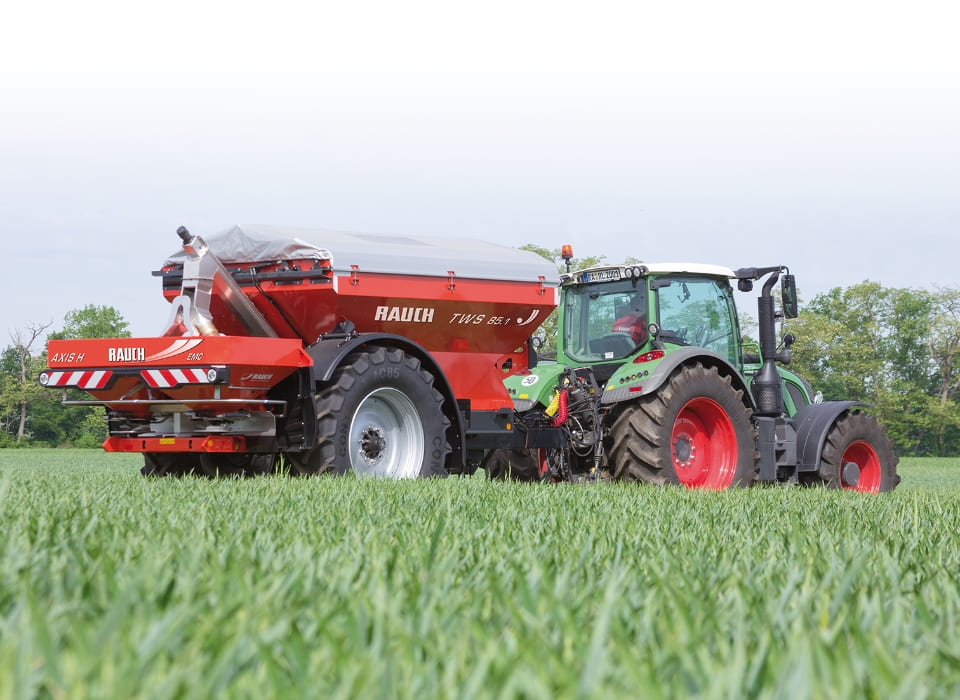
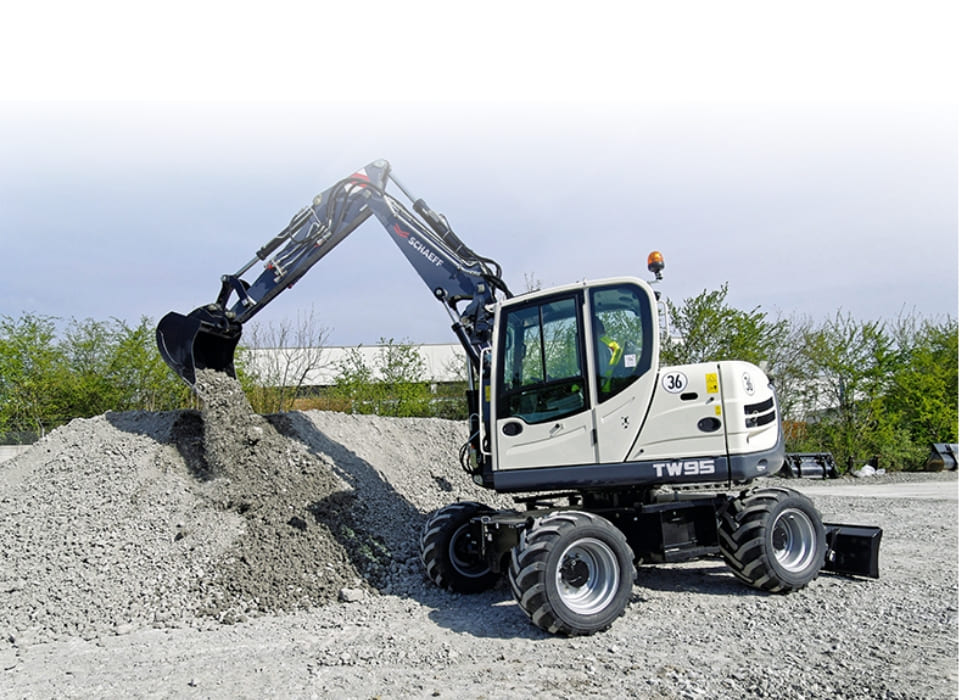
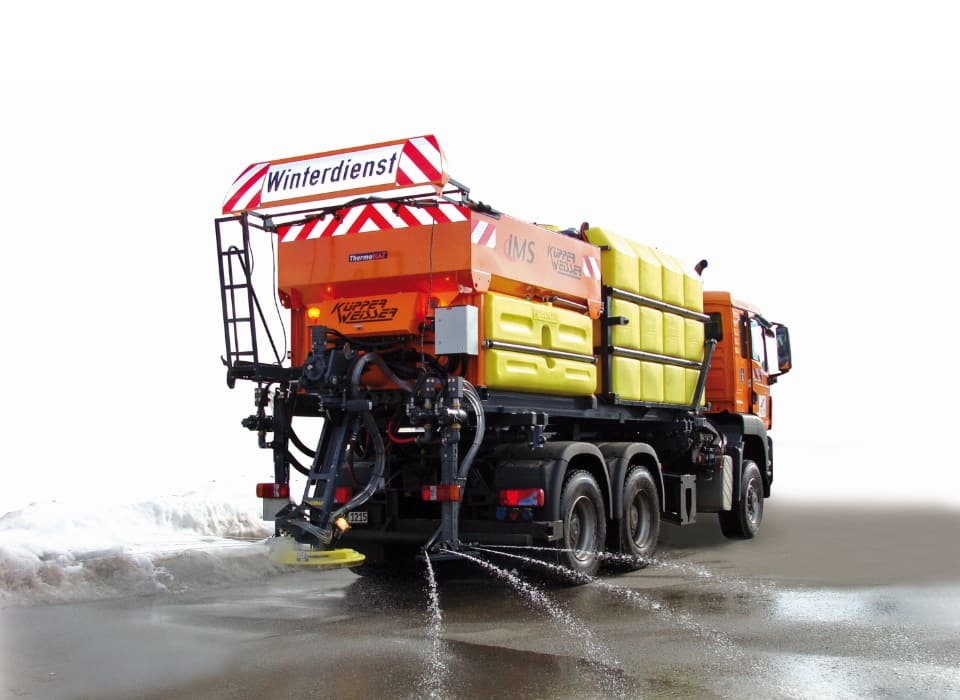
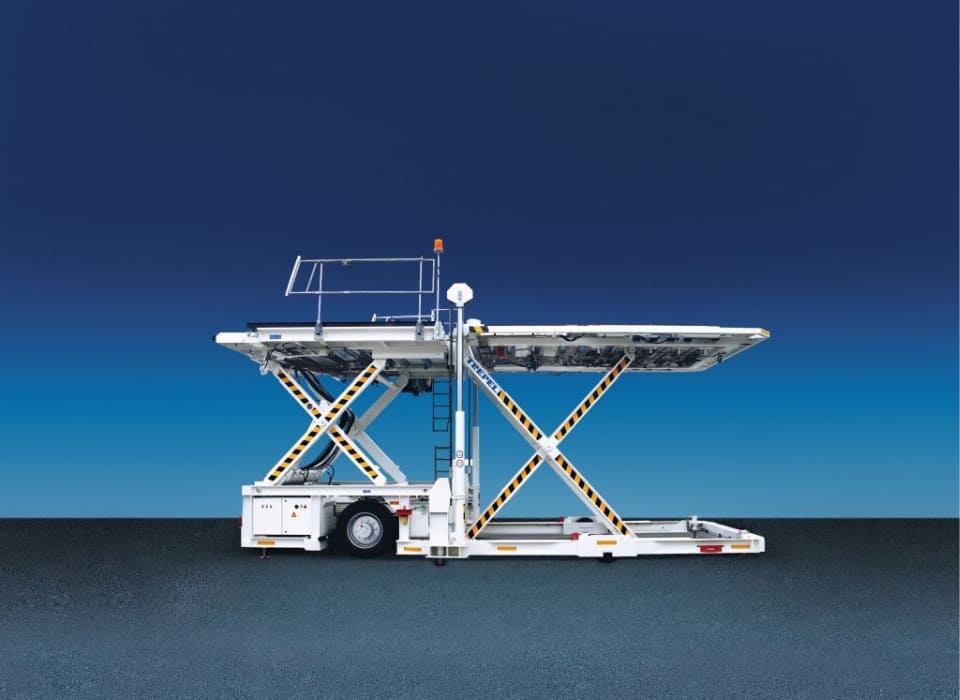
- Agricultural technology, Construction machinery, Municipal technology, Conveying technology, Stationary machinery, Car lifting platforms
- 01
Design (CAD)
- 02
CAM programming & simulation
- 03
CNC machining & deep-hole drilling
- 04
Deburring (manual/thermal)
- 05
Washing & drying
- 06
Surface finishing
- 07
Assembly
- 08
Function testing & on-site commissioning
Materials & Processes
Aluminium
Material for control blocks with deep-hole drillings up to 800 mm depth.
Cast iron
For control blocks and cast housings of the gear flow dividers.
Steel
For heavily stressed control blocks in heavy-duty machining.
Deep-hole drilling
6 x D to 30 x D, up to 800 mm depth and 75 mm drill diameter at Rz < 4.
CNC machining
Single-part, prototype and series production on 7 Heller 4-axis and Hermle machining centres.
Thermal deburring
Optional processes for deburring hard-to-reach drillings.
Surface finishing
Painting, anodising, galvanising, nitro-carburising, oxidising and zinc-nickel with external specialists.
Gear flow divider
2–12 partial flows, approx. 2–400 l/min, max. 210 bar (high-pressure series 240 bar).
Site
Sulz am Neckar
DEHeadquarters, administration and production
- Part weight / size
- up to 1,000 kg / 1,000 mm edge length
- Lot size
- Individual parts, prototypes, series
- Materials
- Aluminium, cast iron, steel
- 7 x Heller 4-axis machining centres (clamping weight up to 1,000 kg, magazine of 425 tools)
- 1 x Hermle 3-axis machining centre (prototypes)
- 1 x Hermle 5-axis machine with automation (2020)
- FASTEMS flexible manufacturing system (2006)
- TDM tool management
- Washing and drying system with high-pressure lances
Products & Components
Inside the production
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| CNC machining (cutting) of control blocks, single-part/prototype/series productionMachining | Rz < 4 (for deep-hole drilling) | 1,000 mm edge length | 1,000 kg (1 tonne) | Series | Aluminium, Cast iron, Steel |
| Deep-hole drilling (6 x D to 30 x D)Machining | Rz < 4 | 800 mm drilling depth × 75 mm drill diameter | – | – | Aluminium, Cast iron, Steel |
| Deep-hole drilling on Heller machining centresMachining | Rz < 4 | 800 mm × 75 mm | – | – | Aluminium, Cast iron, Steel |
| Manual deburringSurface | – | – | – | – | Aluminium, Cast iron, Steel |
| Thermal deburringSurface | – | – | – | – | Aluminium, Cast iron, Steel |
| Machine washing and drying of the control blocks after each setup (including high-pressure lances)Surface | – | – | – | – | Aluminium, Cast iron, Steel |
| Surface treatment/finishing: painting, anodising, galvanising, nitro-carburising, oxidisingSurface | – | – | – | – | Aluminium, Cast iron, Steel |
| CAD design of custom control blocks (Top Solid V6, data import Inventor IPT, STEP, DXF)Engineering | – | 1,000 mm edge length | 1 tonne | – | Aluminium, Cast iron, Steel |
| CAD/CAM programming with NC data generation, program simulations, TDM tool managementEngineering | – | – | – | – | Aluminium, Cast iron, Steel |
| Assembly of control blocks with screw-in and stack valves, fittings, pressure switchesAssembly | – | – | 1 tonne | – | Aluminium, Cast iron, Steel |
| Function testing of prototypes, control blocks and complete systemsTesting | – | – | – | – | – |
| Endoscopic inspection of drillings (up to 800 mm depth)Testing | – | 800 mm | – | – | Aluminium, Cast iron, Steel |
| Design and manufacture of complex control blocks and prototypesJoining | – | 1,000 mm edge length | 1 tonne | – | Aluminium, Cast iron, Steel |
| Assembly of the appropriate valves according to customer specifications, individual adjustment ofAssembly | – | – | – | – | – |
| Development of electronic controls and operating elements (joysticks), programming ofEngineering | – | – | – | – | – |
| Manufacture of AC rotating/alternating current small power units (tank, pump, motor, optionallyAssembly | – | – | – | Tank size 4 - 12 litres – Tank size 4 - 12 litres | – |
| Manufacture of DC small power units (DC motor)Assembly | – | – | – | – | – |
| Manufacture of gear flow dividers (2-12 partial flows, 2-400 l/min, max. 210 bar; high-pressureForming | – | – | – | – | Cast iron |
4 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| Heller 4-axis machining centre | Heller | 7 | Clamping weight up to 1000 kg, edge length up to 1000 mm, tool magazine with 425 tools, drilling | – | Sulz am Neckar |
| Hermle 3-axis machining centre (prototype manufacturing) | Hermle | 1 | – | – | Sulz am Neckar |
| Hermle 5-axis machine with automation | Hermle | 1 | – | 2020 | Sulz am Neckar |
| FASTEMS flexible manufacturing system | FASTEMS | 1 | – | 2006 | Sulz am Neckar |
Additional services
Quality
Since 1997 the company has been certified to DIN EN ISO 9001; function testing of prototypes, control blocks and complete systems as well as endoscopic inspections of drillings up to 800 mm depth are part of the testing scope.
| Evidence | Sulz am Neckar |
|---|---|
| DIN EN ISO 9001 |
History
- 1977
Founded by Roland Dreher; Rainer Schlagenhauf becomes the first employee.
- 1984
Move to the current company building in Sulz am Neckar.
- 1995
Extension of the production area by 290 m²; renovation of the office building.
- 1997
Certification to DIN EN ISO 9001; Rainer Schlagenhauf becomes shareholder and managing director.
- 2006
Commissioning of the FASTEMS flexible manufacturing system.
- 2012
Carina Katz née Schlagenhauf becomes managing director.
- 2014
Modernisation of the offices on the ground floor.
- 2018
Carina Katz and Patrick Schlagenhauf take over the shares from Roland Dreher.
- 2020
Commissioning of a Hermle 5-axis machine with automation.
- 2021
Extension of the management to include Patrick Schlagenhauf.